ARTE
BELLEZZA E BENESSERE
MESTIERE
CULTURA E STORIA
DIVERTIMENTO
AMBIENTE
CIBO E BEVANDE
INGEGNERIA INVERSA
SCIENZE
SPORT
TECNOLOGIA
INDOSSABILI


Bearing Steel Wire (52100): Drawn from Bar Through a Drawplate
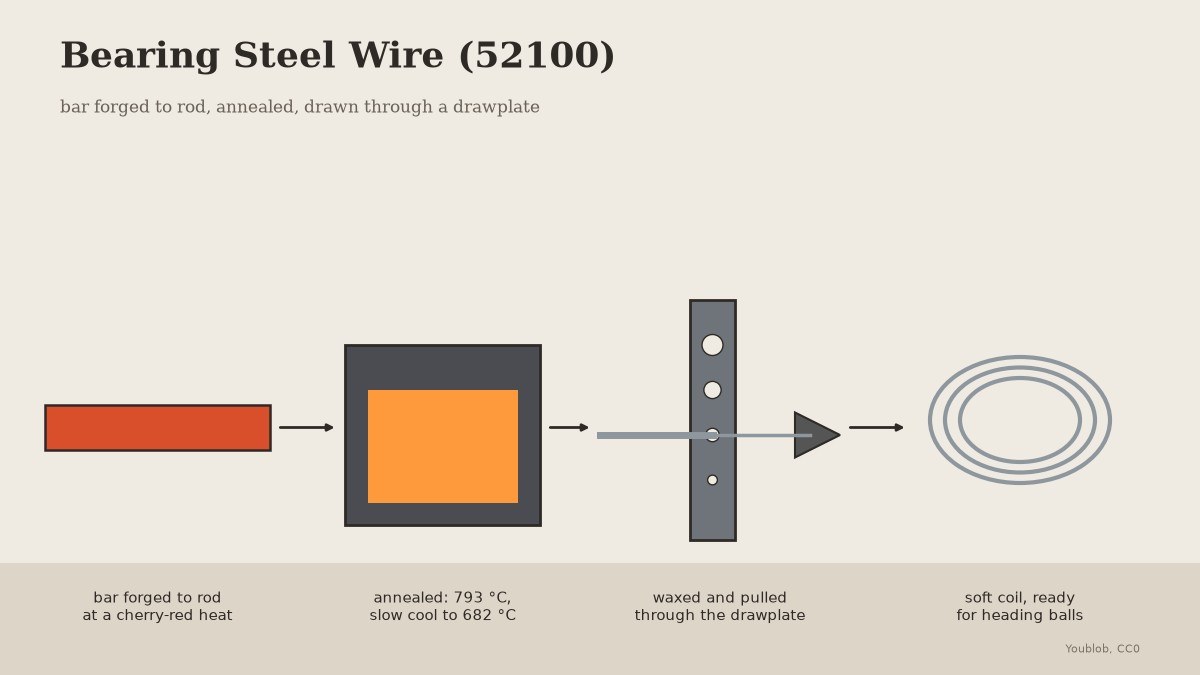
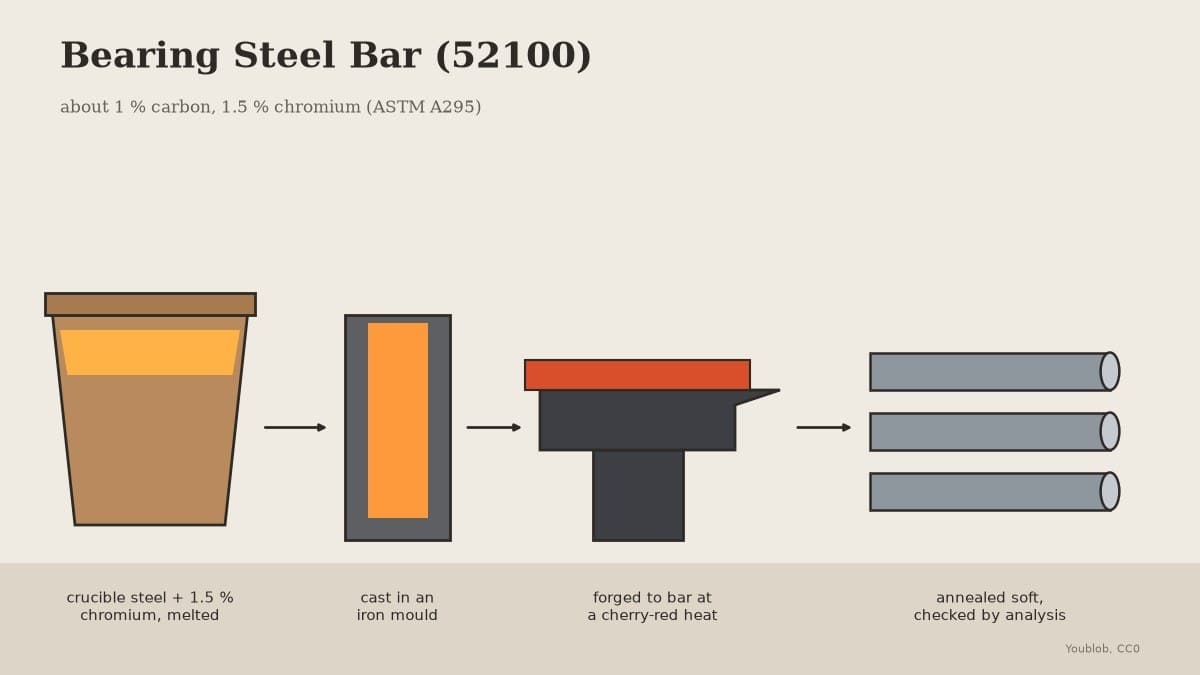
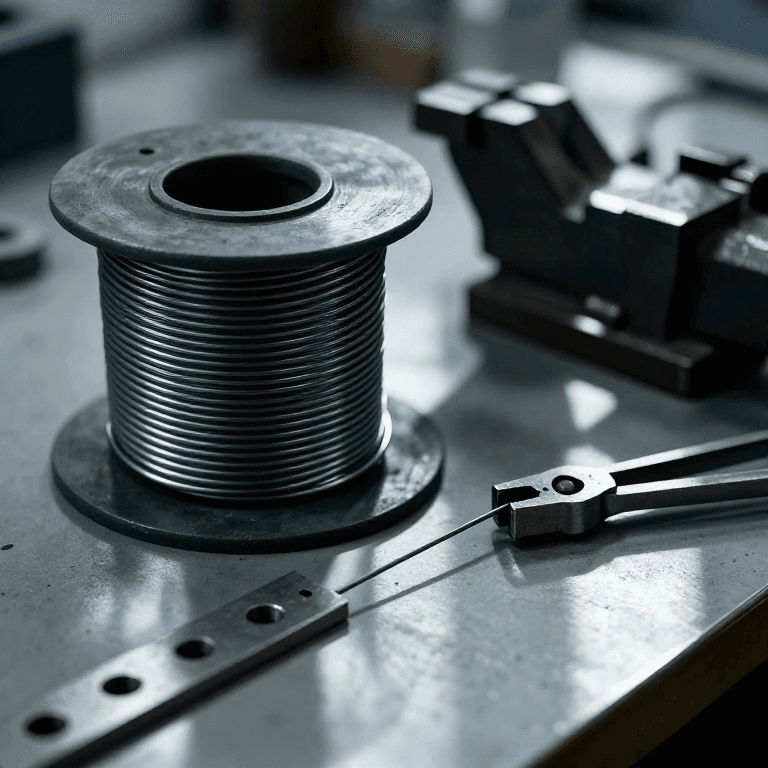
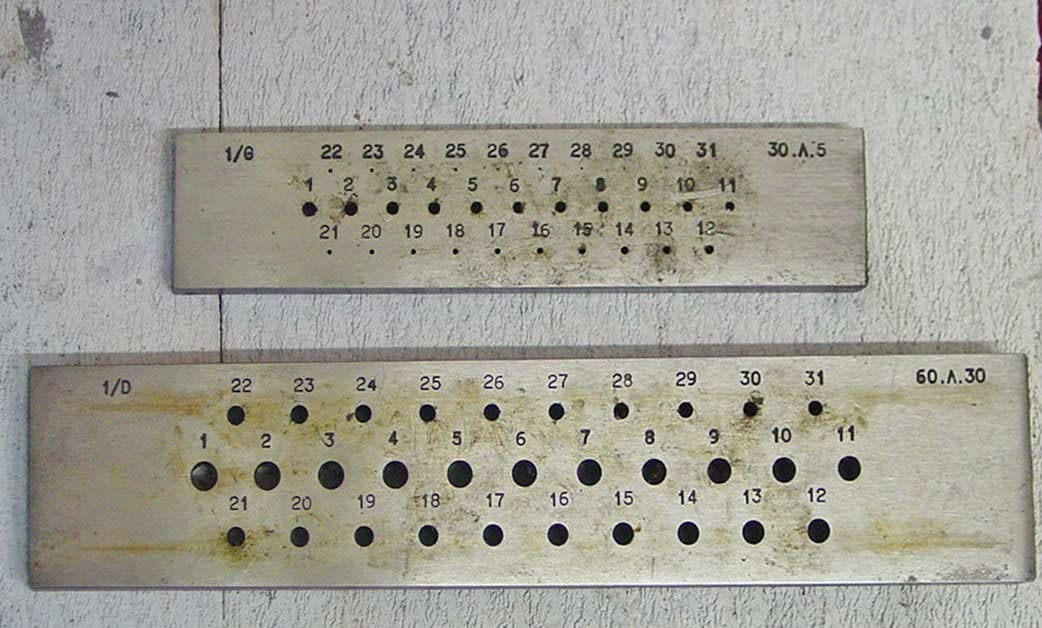
Bearing balls are headed from thick wire of 52100 steel. Here 52100 bar is forged to rod and drawn through a drawplate. At 1 % carbon it is much harder than mild steel, so it is annealed soft before drawing and again after every two holes, using the 52100 anneal Verhoeven recommends.
The picture: our drawing, bar to coil.
Avanzato
2 days
Istruzioni
1
1
Forge to rod
Forge to rod
Heat the bar to a cherry-red heat and no hotter, and draw it out round on the anvil to a rod a little thicker than the drawplate's largest hole.
Materiali per questo passaggio:
 Barra in acciaio per cuscinetti (52100)1 kg
 Carbone di legna1 as required
Strumenti necessari:
 Forgia da fabbro
 Incudine
 Martello a penna trasversale
 Tenaglie da fabbro
 Guanti da saldatore
 Occhiali di sicurezza
2
2
Anneal
Anneal
In the oven, hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
Strumenti necessari:
 Forno per trattamenti termici
 Termocoppia con lettoreTenaglie da fabbroGuanti da saldatore
3
3
Clean and taper
Clean and taper
Brush off all the scale, then file a long taper on the first 3 cm so it passes the first hole.
Strumenti necessari:
 Set di spazzole metalliche
 Serie di lime
 Morsa da banco
4
4
Wax and draw
Wax and draw
Clamp the drawplate in the vise. Wax the rod, push the taper through the first hole it does not slip through, and pull straight out with the draw tongs in one steady pull.
Materiali per questo passaggio:
 Cera d'api20 g
Strumenti necessari:
 Filiera d'acciaio
 Tenaglie da tiraggioMorsa da banco
 Guanti da lavoro in pelle
5
5
Anneal every two holes
Anneal every two holes
Draw through each next hole without skipping. After every two holes, coil the wire and anneal it again: hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
Materiali per questo passaggio:
Cera d'api1 pezzoStrumenti necessari:
Filiera d'acciaioTenaglie da tiraggioForno per trattamenti termiciTermocoppia con lettore6
6
Finish soft
Finish soft
Stop at the diameter your balls need, checked with the caliper, and give the coil a last anneal so it is soft for heading.
Strumenti necessari:
 Calibro digitale da 6 polliciForno per trattamenti termiciTermocoppia con lettore
7
7
Troubleshooting
Troubleshooting
Bearing steel wire troubleshooting.
Flow
Loading...
Materiali
3- Segnaposto
- 1 as requiredSegnaposto
- 1 pezzoSegnaposto
Strumenti richiesti
15- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
- Segnaposto
Questo progetto realizza
Blueprint correlati
Questi blueprint condividono conoscenze — tecniche, materiali o principi
CC0 Pubblico dominio
Questo progetto è rilasciato sotto CC0. Sei libero di copiare, modificare, distribuire e utilizzare quest'opera per qualsiasi scopo, senza chiedere permesso.
Supporta il Maker acquistando prodotti tramite il suo progetto dove guadagna una Commissione Maker stabilita dai venditori, oppure crea una nuova iterazione di questo progetto e includilo come collegamento nel tuo progetto per condividere i ricavi.