
ARTE
BELLEZZA E BENESSERE
MESTIERE
CULTURA E STORIA
DIVERTIMENTO
AMBIENTE
CIBO E BEVANDE
INGEGNERIA INVERSA
SCIENZE
SPORT
TECNOLOGIA
INDOSSABILI
Designing For the Process: A Printable Part Is a Different Shape
3DBonanza

Creato da

3DBonanza

24. settembre 2026US
21
0
0
0
0

Designing For the Process: A Printable Part Is a Different Shape

A model drawn without thinking about printing can usually be printed. A model drawn WITH the process in mind prints faster, stronger, with no supports and a better surface — from the same amount of design effort. Every rung before this one is a constraint: layers are weak in one direction, overhangs have a limit, holes come out small, corners warp, walls carry the load. Design is where those stop being problems to work around and become the rules the shape is drawn to. That is the same move as designing a casting with draft angles, or a timber frame with wood movement allowed for. The process has a grain, and a good design runs with it.
Avanzato
4 hours

Istruzioni

1

Chamfer the bottom, fillet the rest

A 45-degree CHAMFER on the bottom edge of a part is self-supporting, removes the elephant-foot bulge, and makes the part easier to insert into anything. It is close to free and almost always an improvement. Fillets elsewhere reduce stress concentration and warping, exactly as a radiused corner does on any other part. Internal corners especially: a sharp internal corner is where a printed part cracks. But do NOT fillet the bottom edge — a bottom fillet is an overhang that starts at 90 degrees, which is the one angle nothing can print. Chamfer at the bottom, fillet above it, and that single rule removes a lot of support material.

Materiali per questo passaggio:

Filamento per stampa 3D (PLA)Filamento per stampa 3D (PLA)1 pezzo

Strumenti necessari:

Computer da tavoloComputer da tavolo
Software di slicing per file 3MFSoftware di slicing per file 3MF
SbavatoreSbavatore
2

Turn overhangs into bridges and teardrops

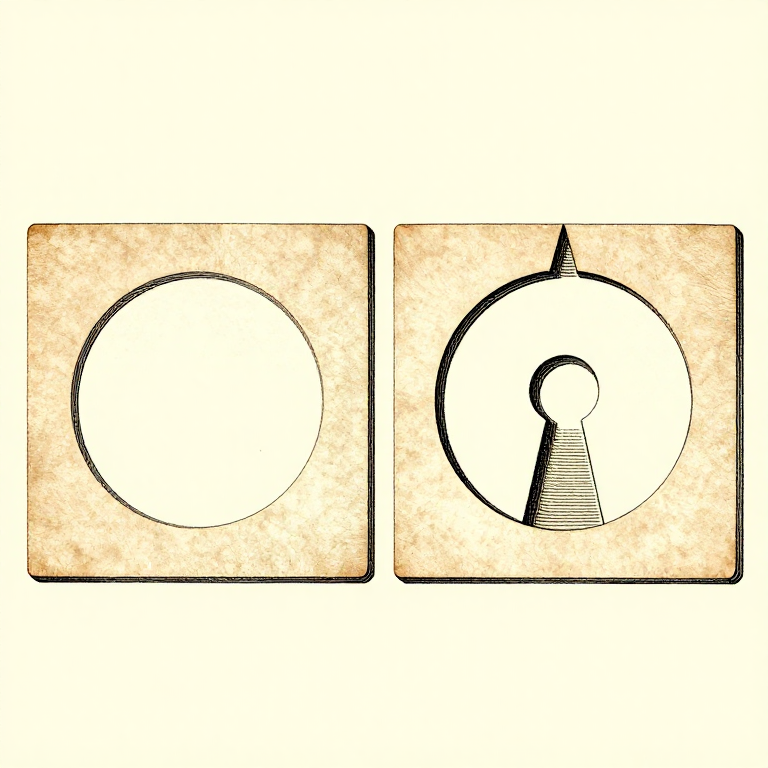
A horizontal hole printed round has an unsupported arch at the top that sags. Printed as a TEARDROP — a circle with a 45-degree point on top — it is entirely self-supporting and needs no support at all. A hexagonal hole does the same job and takes a nut. So does simply making the top of the hole a flat bridge rather than a curve, which prints well for the reasons the overhang rung gives. The general form: wherever the model has a surface between 45 and 90 degrees, ask whether it can become a chamfer, a bridge, or a shape with a point on top. Nearly always it can, and nearly always the result is better than supporting it.

Materiali per questo passaggio:

Filamento per stampa 3D (PLA)Filamento per stampa 3D (PLA)1 pezzo

Strumenti necessari:

Computer da tavoloComputer da tavolo
Software di slicing per file 3MFSoftware di slicing per file 3MF
Calibro digitale da 6 polliciCalibro digitale da 6 pollici
3

Split the part where splitting helps

A part that needs supports, or warps, or is too tall to be stable, can often be cut into two pieces that each print flat and are then glued or bolted. Put the split where a joint is natural — at a change of section, behind a flange — and add a locating feature, a peg and socket or a dovetail, so the two halves cannot be assembled wrong. Design the clearance into one side only, as the tolerance rung sets out. Splitting also lets each half be oriented for its own load path, which the orientation rung says is the highest-leverage decision available. A part split into two well-oriented halves can be stronger than the same part printed whole.

Materiali per questo passaggio:

Filamento per stampa 3D (PLA)Filamento per stampa 3D (PLA)1 pezzo

Strumenti necessari:

Computer da tavoloComputer da tavolo
Software di slicing per file 3MFSoftware di slicing per file 3MF
Calibro digitale da 6 polliciCalibro digitale da 6 pollici
SbavatoreSbavatore
4

Use real hardware where it belongs

Printed threads are weak, printed bearings wear, and printed springs creep. Heat-set brass inserts, steel pins, real bearings and real fasteners cost very little and remove the weakest parts of a printed assembly. Design the pocket for them from the start: a straight bore for an insert, a captive hex pocket for a nut, a shoulder for a bearing to seat against. A pocket designed in prints perfectly; one drilled afterwards splits the part along a layer. Which is the whole argument of this batch. The printer is one process among several, it has specific strengths and specific limits, and the best results come from using it for what it is good at and something else for the rest.

Materiali per questo passaggio:

Filamento per stampa 3D (PLA)Filamento per stampa 3D (PLA)1 pezzo
Filamento PETG con fibra di carbonioFilamento PETG con fibra di carbonio1 pezzo

Strumenti necessari:

Computer da tavoloComputer da tavolo
Calibro digitale da 6 polliciCalibro digitale da 6 pollici
Kit di attrezzi per stampante 3DKit di attrezzi per stampante 3D

Materiali

2

Strumenti richiesti

5

CC0 Pubblico dominio

Questo progetto è rilasciato sotto CC0. Sei libero di copiare, modificare, distribuire e utilizzare quest'opera per qualsiasi scopo, senza chiedere permesso.

Supporta il Maker acquistando prodotti tramite il suo progetto dove guadagna una Commissione Maker stabilita dai venditori, oppure crea una nuova iterazione di questo progetto e includilo come collegamento nel tuo progetto per condividere i ricavi.

Commenti

(0)

Accedi per partecipare alla discussione

Caricamento commenti...