アート
美容とウェルネス
工芸
文化と歴史
エンターテインメント
環境
食品と飲料
リバースエンジニアリング
科学
スポーツ
テクノロジー
ウェアラブル
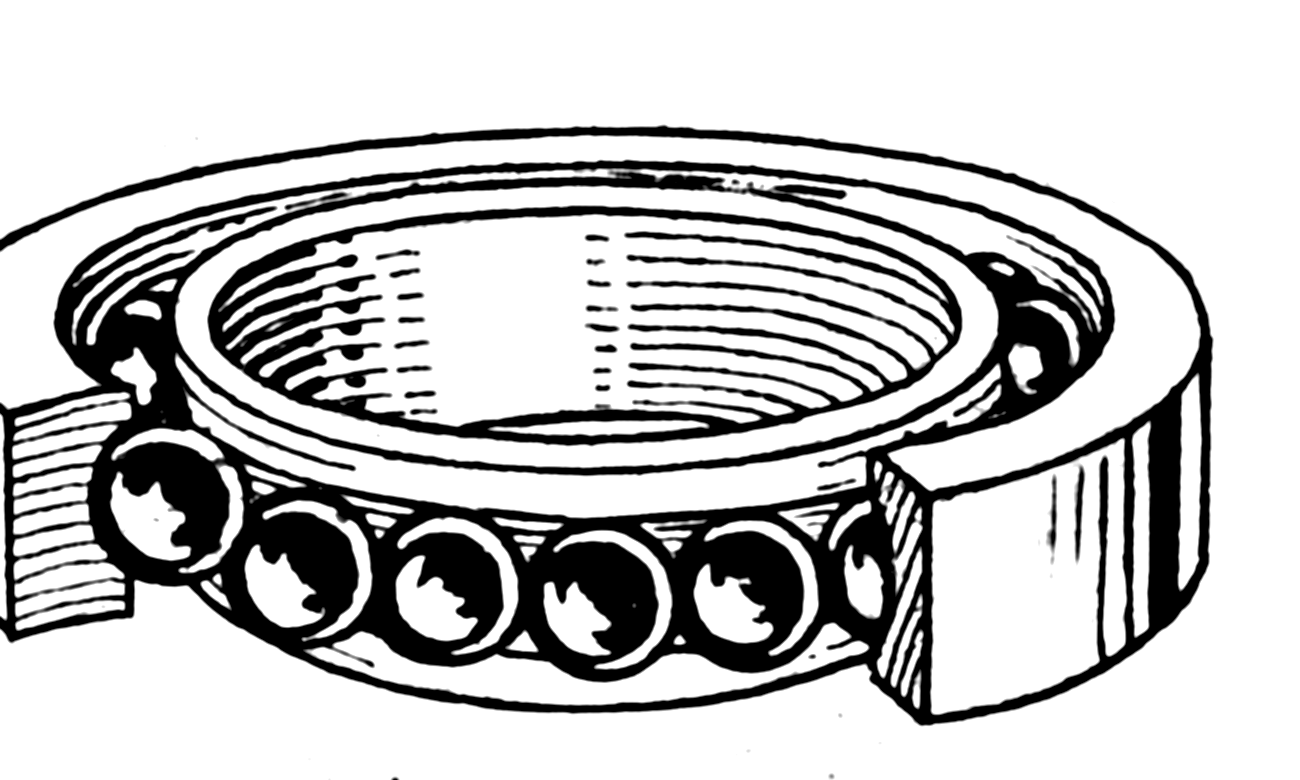

Ball Bearings: Races, Balls and Cage
A ball bearing has four parts: an outer race, an inner race, the balls that roll between them, and a cage that keeps the balls evenly spaced. Almost all of it is steel, usually 52100 (1.5% chromium, 1% carbon), which can be made very hard and tough by heat treating; 440C stainless is used where rust is a problem. The races are turned from tubing, the balls are cold headed from thick wire, both are hardened, tempered, ground and lapped to an almost mirror finish, and the cage is stamped from thin sheet. Even an inexpensive bearing's balls may be out of round by no more than 25 millionths of an inch; precision bearings allow five millionths.
上級者
Factory process
手順
1
1
Turn the races
Turn the races
Cut the basic shape of both races from steel tubing on automatic lathe-like machines, leaving every dimension slightly oversize: the steel usually warps in heat treatment.
このステップの材料:
 軸受鋼管(52100)1 as required
必要な工具:
 自動旋盤
2
2
Harden and temper the races
Harden and temper the races
Heat to about 843 °C (1,550 °F) for up to several hours depending on size, then quench in oil: hard but brittle. Temper at about 149 °C (300 °F) and let cool in air: hard and tough.
必要な工具:
 油焼入れ付き連続焼入れ炉
 焼戻し炉
3
3
Grind and lap the races
Grind and lap the races
The hardened steel is too hard to cut, so grind almost every surface: the fitting surfaces round, the sides flat. Grind the ball track, then lap it for several hours with a very fine abrasive slurry to an almost mirror finish.
必要な工具:
 軸受軌道輪研削盤
 軌道ラッピング盤
 ラッピングコンパウンド
4
4
Cold head the balls
Cold head the balls
Feed thick wire from a roll into a machine that cuts off a short piece and smashes both ends in toward the middle between two dies, without heating. The ball comes out with a ring of "flash" round its middle.
このステップの材料:
 軸受鋼線(52100)1 as required
必要な工具:
 冷間圧造機
5
5
Remove the flash
Remove the flash
Run the balls many times round rough grooves between two cast-iron discs, one turning and one fixed, until the flash is gone and they are nearly round. Leave about 0.008 in (0.2 mm) for finishing.
必要な工具:
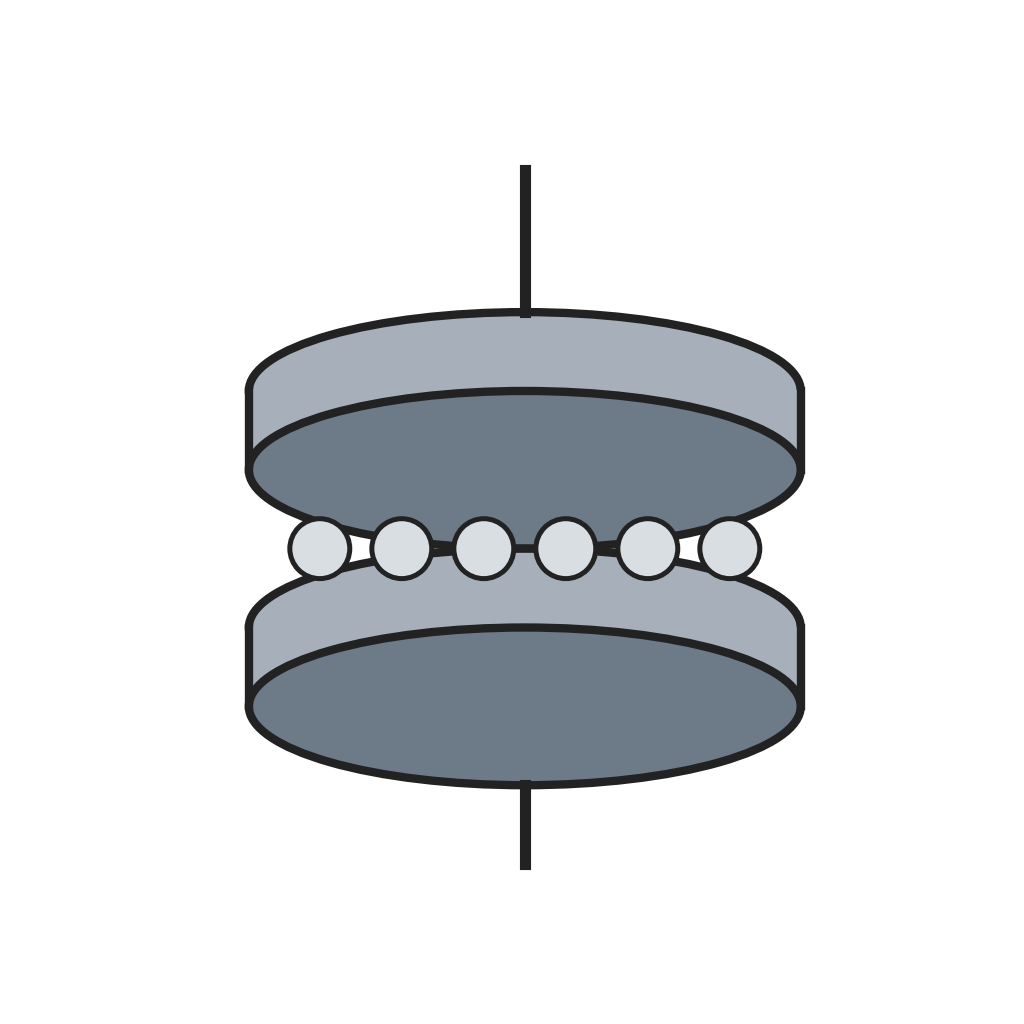 鋼球バリ取り機
6
6
Harden, grind and lap the balls
Harden, grind and lap the balls
Heat treat and temper the balls like the races. Grind them in the same kind of disc machine with grinding wheels to within a few ten-thousandths of an inch, then lap them 8–10 hours on cast-iron wheels with lapping compound.
必要な工具:
油焼入れ付き連続焼入れ炉焼戻し炉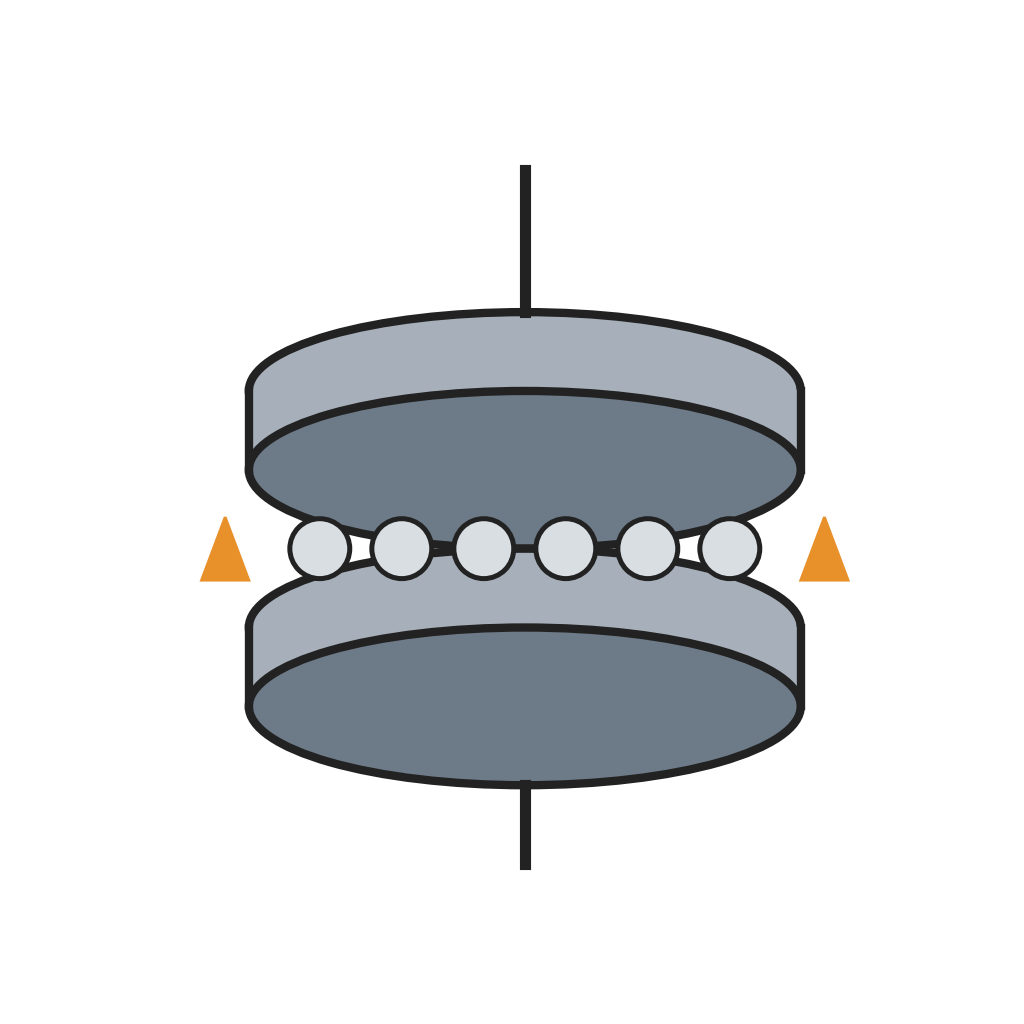 鋼球研削盤
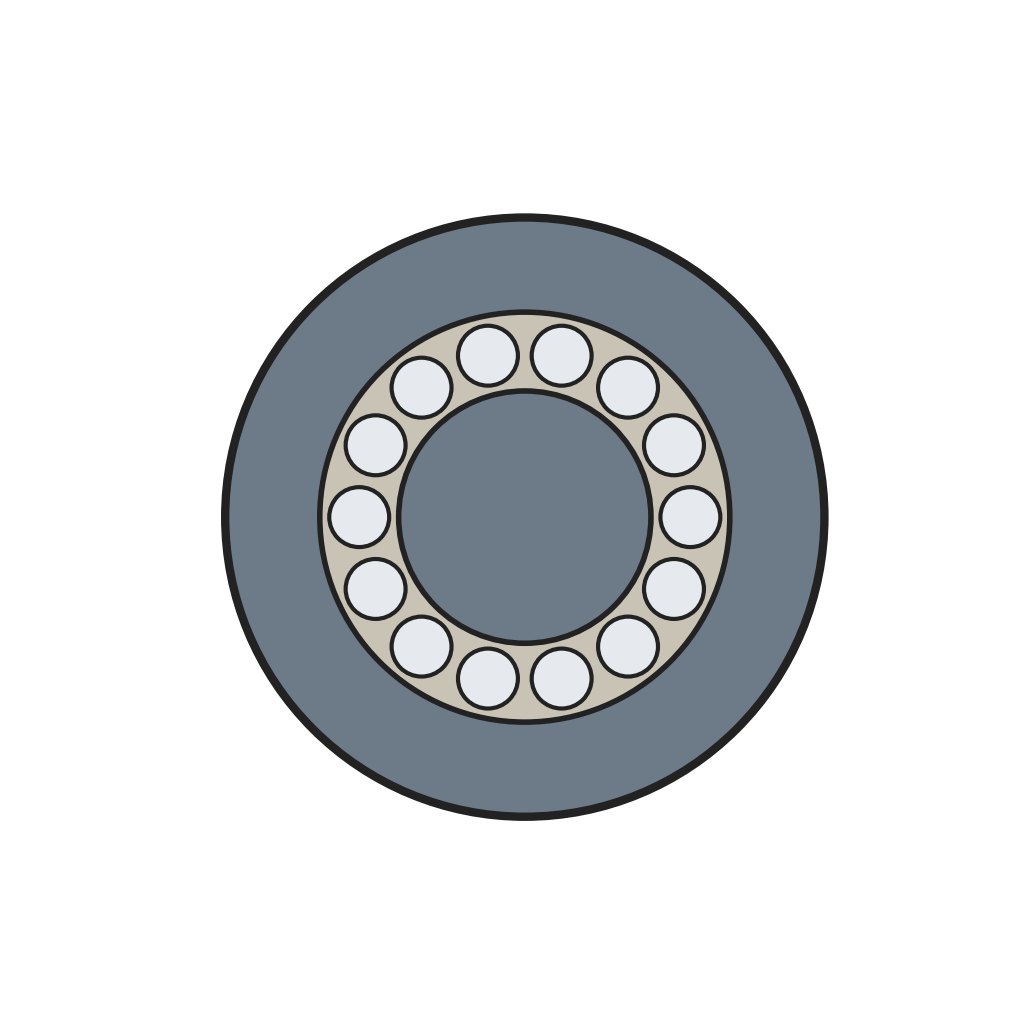 鋼球ラッピング盤ラッピングコンパウンド
7
7
Stamp the cage
Stamp the cage
Stamp the cage halves from thin steel sheet and bend them to shape in a die. (Plastic cages are injection moulded instead.)
このステップの材料:
 鋼板1 as required
必要な工具:
 金属プレス機
8
8
Assemble
Assemble
Put the inner race inside the outer race, pushed as far to one side as it goes, and drop the balls into the gap opposite. Centre the races and spread the balls evenly, fit the cage (steel cages riveted, plastic ones snapped in) and coat the bearing with a thin film of petroleum jelly against rust.
このステップの材料:
 鋼製リベット1 as required
 ワセリン1 as required
材料
5- 1 as requiredプレースホルダー
- 1 as requiredプレースホルダー
- 1 as requiredプレースホルダー
- 1 as requiredプレースホルダー
- 1 as requiredプレースホルダー
関連ブループリント
これらのブループリントは知識を共有しています — 技術、材料、原理
CC0 パブリックドメイン
このブループリントはCC0で公開されています。許可を求めずに、自由にコピー、修正、配布、あらゆる目的で使用できます。
メイカーを応援するには、ブループリント経由で製品を購入してください。メイカーには メイカーコミッション がベンダーにより設定されています。または、このブループリントの新しいイテレーションを作成し、自分のブループリントにコネクションとして含めて収益を共有できます。