コラボレーション
アート
美容とウェルネス
工芸
文化と歴史
エンターテインメント
環境
食品と飲料
リバースエンジニアリング
科学
スポーツ
テクノロジー
ウェアラブル
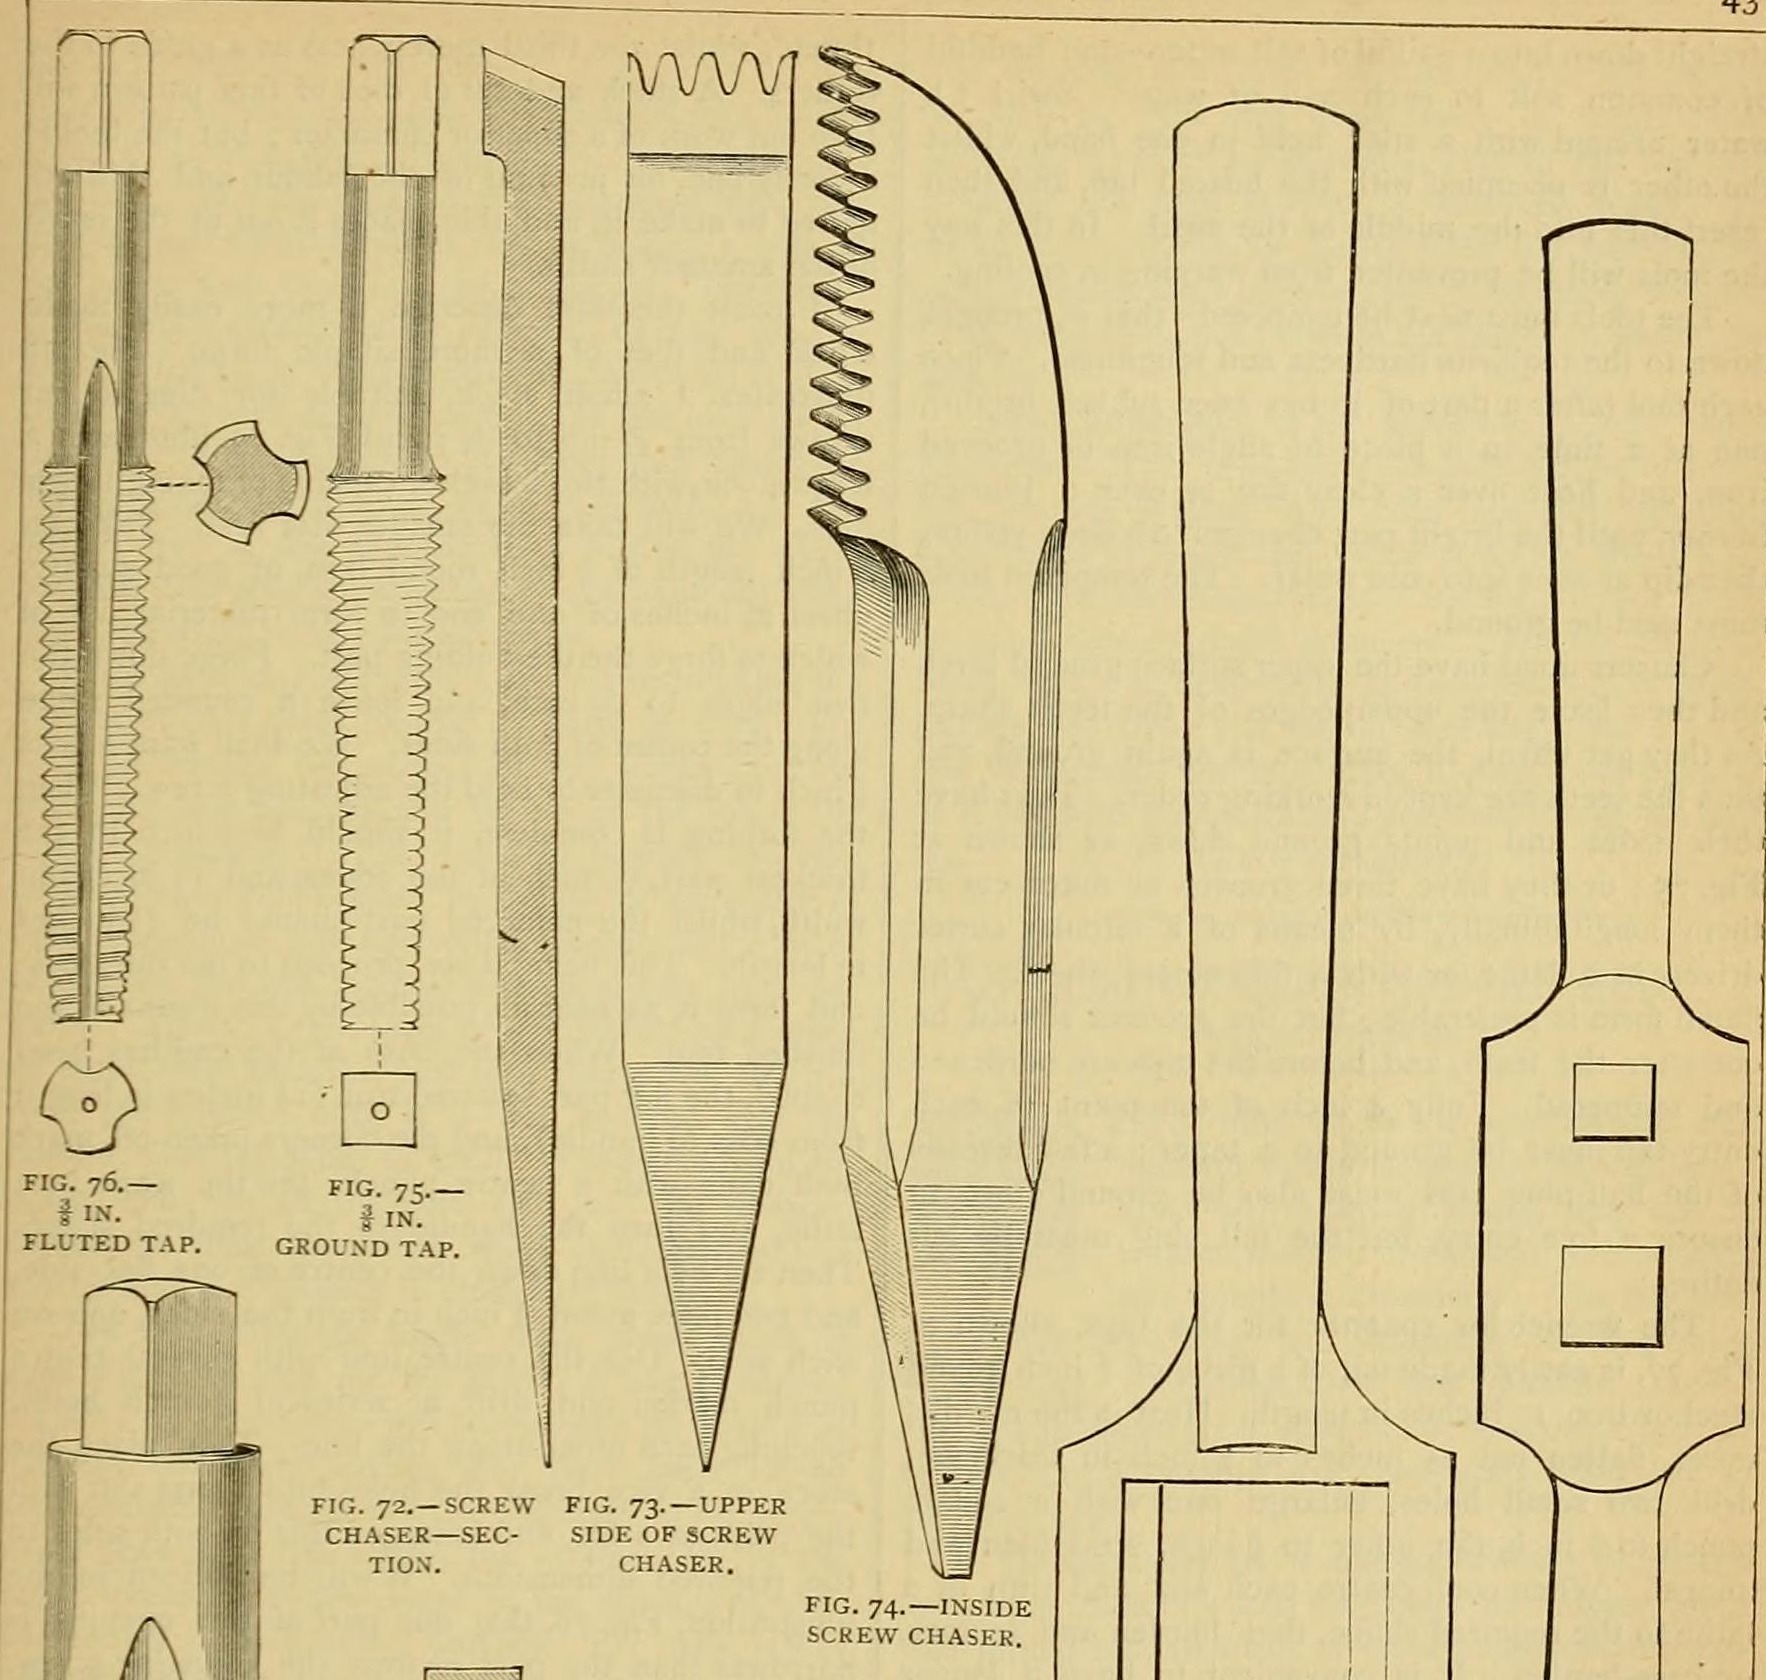


Whitworth Taps from Cast Tool Steel: Turned, Chased, Fluted and Hardened in Salt Water, with Their Wrench (Edwinson, 1886)
George Edwinson's instructions (Amateur Work, 1886) for a home-made set of Whitworth taps, 3/16 to 1 inch, in entry, half-plug and full-plug form: cast tool steel annealed, turned, roughed with a single-point tool and finished with home-made chasers in a screw-cutting lathe, fluted, hardened in swirled salt water and tempered deep yellow; plus the two-hole tap wrench. The dies and stock are in the companion blueprint.
上級者
Several days for a set of thirty
手順
1
1
His tables
His tables
Jupyter ノートブックを読み込み中…
2
2
Read Edwinson
Read Edwinson
"There is only one perfect method of making a good tap, and that is by turning the metal ... and cutting the thread in a screw-cutting lathe."
3
3
Cut and anneal the blanks
Cut and anneal the blanks
Cut the best 1 in. square cast tool steel into 3 1/2 in. lengths for the large taps, and 1/2 in. steel into 3 in. lengths for the small ones (a full set takes 5 ft 6 in. of the first and 3 ft of the second). Anneal: blood red, cooled slowly in hot ashes. File the ends square, centre-punch, and drill the centres 1/16 in. (small) or 1/8 in. (large) deep.
このステップの材料:
 工具鋼丸棒1 個
必要な工具:
 熱間たがね
 鍛冶炉
 やすり(手やすり)
 センターポンチ
 ボール盤
4
4
Rough out the taps
Rough out the taps
Turn the corners off. Mark each tap: entry 1/2 in. head, 3/4 in. shank; half plug 1/2 in. head, 1 in. shank; full plug 1/2 in. head, 1 1/4 in. shank; the rest is thread (for the 1 in. set; 7/8 the same, smaller sets in proportion with shanks turned down for clearance). Below 1/2 in. make the square heads 3/8 or 3/16 in. to fit the wrench. Anneal again, turn true and smooth, and finish with a fine file.
必要な工具:
 金属旋盤やすり(手やすり)鍛冶炉
5
5
Make the chasers
Make the chasers
From flat tool steel forge one chaser per size, the largest 1 in. wide, 1/4 in. thick and 5 in. long, the rest a little smaller, with 3 1/2 or 4 1/2 teeth across the width and a tang for a wooden handle (fig. 72). Upset the point, grind, anneal, file the teeth, and finish them by running the chaser against a full plug tap or hub of that pitch in the lathe. Inside chasers: against a left-handed hub, or file off the lower leading edge of each tooth (fig. 74).
このステップの材料:
工具鋼丸棒1 個必要な工具:
鍛冶炉 金床
 ハンマーやすり(手やすり)金属旋盤
6
6
Cut the threads
Cut the threads
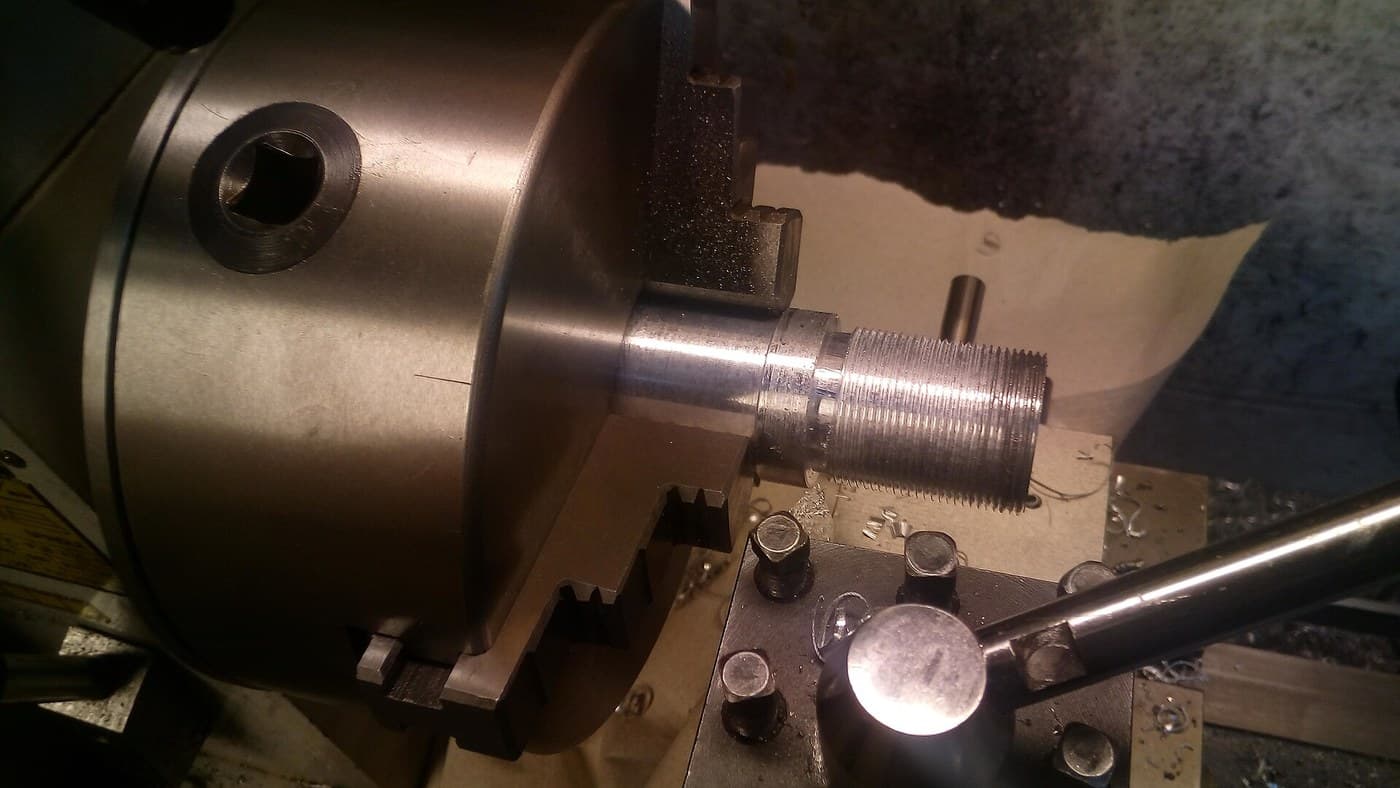
Rough each thread with a single fine-point tool in the slide rest of a screw-cutting lathe, set with the change wheels for its pitch (notebook), then finish with the chaser. Whitworth form: 55 degree angle, one-sixth rounded off top and bottom. Stamp each tap with its size and threads per inch.
必要な工具:
金属旋盤ハンマー7
7
Flute and point
Flute and point
Cut three flutes along each tap with a circular cutter in the lathe or a thin emery wheel (before hardening), or grind the sides flat (fig. 75). Grind fully 1/2 in. of each entry tap to a taper and the first few threads of the half plug; leave the full plug entire.
必要な工具:
金属旋盤 卓上グラインダー
8
8
Harden and temper
Harden and temper
Heat each tap or chaser to blood red and plunge it straight down into a pail of water with a handful of common salt, swirled with a stick, into the middle of the swirl so it does not warp. Rub part bright, lay it in angle or grooved iron over a clear fire or a Bunsen burner until the bright part is deep yellow, then dip it in cold water. Grind the chaser tops level.
このステップの材料:
 塩1 個
 水1 個
必要な工具:
鍛冶炉 バケツ
 ブンゼンバーナー卓上グラインダー
9
9
Make the tap wrench
Make the tap wrench
Take 10 in. of 3/4 in. round steel or iron. Heat the middle, upset it and flatten 2 1/2 in. to 1/2 in. thick. Drill two small holes and open them with a square punch, one to 3/8 in. and one to 1/4 in. Straighten, anneal, centre the ends and turn them in the lathe, then harden and temper. A longer, heavier wrench with one 1/2 in. hole suits the big taps.
このステップの材料:
工具鋼丸棒1 個必要な工具:
鍛冶炉金床 大ハンマーボール盤金属旋盤
10
10
Troubleshooting
Troubleshooting
Tap troubleshooting.
Flow
Loading...
11
11
History and honest limits
History and honest limits
From George Edwinson, "Smithing and Forging" V, **Amateur Work, Illustrated**, vol. V (1886), pp. 434-438 and figs. 71-77 (checked on the archive.org scan amateurworkillus05lond). He himself advised buying Whitworth gear rather than making it. Metric conversions and the tools listed are ours.
関連ブループリント
これらのブループリントは知識を共有しています — 技術、材料、原理

CC0 パブリックドメイン
このブループリントはCC0で公開されています。許可を求めずに、自由にコピー、修正、配布、あらゆる目的で使用できます。
メイカーを応援するには、ブループリント経由で製品を購入してください。メイカーには メイカーコミッション がベンダーにより設定されています。または、このブループリントの新しいイテレーションを作成し、自分のブループリントにコネクションとして含めて収益を共有できます。