アート
美容とウェルネス
工芸
文化と歴史
エンターテインメント
環境
食品と飲料
リバースエンジニアリング
科学
スポーツ
テクノロジー
ウェアラブル

The Living Hinge: Strong Because It Is Thin
The lid of a mint box, a shampoo cap, a toolbox, a DVD case: a hinge moulded in one piece with the parts it joins, with no pin, no bearing and no assembly, that folds a million times and does not break.
It works for the same reason the bottle in the previous rung holds five bar. A fold puts a strain on the outer surface equal to the thickness divided by twice the bend radius — so making the web **thin** is what makes the strain survivable. And on the first few folds the polymer yields and its chains draw into alignment across the hinge, so the hinge ends up **stronger than it was moulded**.
It also only really works in one family of polymers, which is a useful thing to know before you design one.
初心者
About 2 hours
手順
1
1
Find five hinges and measure them
Find five hinges and measure them
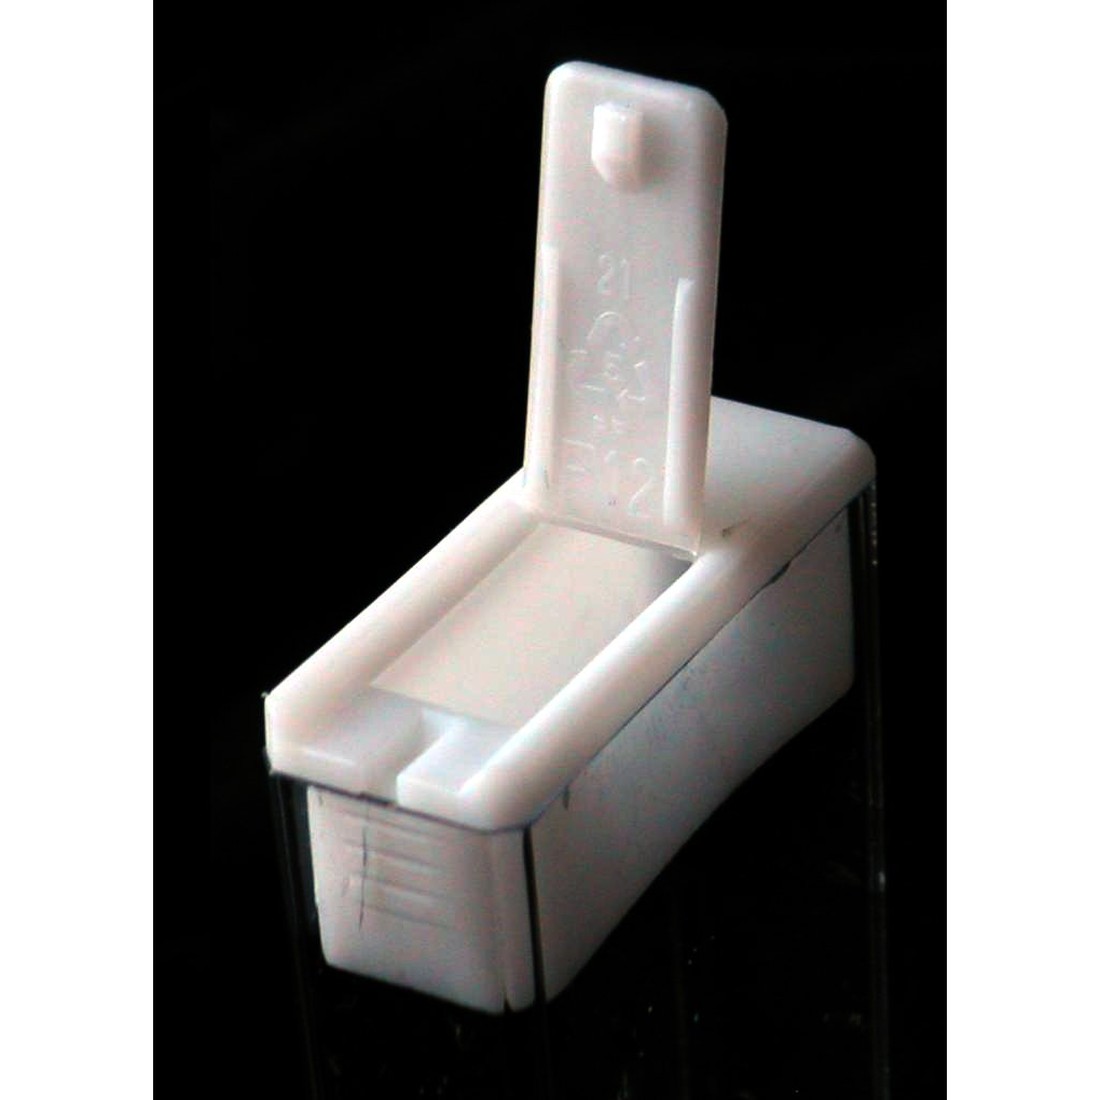
Collect five moulded living hinges from things you already own: a mint or pill box, a flip-top cap, a takeaway container, a cable tidy, a tool case. The photograph on this page is a mint box lid and it is a good example of the type.
For each one, measure or observe:
- **Web thickness** at the thinnest point, with the micrometer if you can reach it or by sectioning a spare with a craft knife. Expect 0.25 to 0.5 mm, and be surprised by how consistent that is across wildly different products.
- **The land** — the flat length of thin web, usually a millimetre or two. A hinge is not a knife edge; it is a short flat valley.
- **The shape of the transition.** Generous radii into the web on both sides. Look for a sharp notch and you will not find one, because a notch is a crack waiting.
- **The recycling mark**, if moulded in. It will almost always be **5 — PP**.
Then fold each one slowly and watch the surface at the fold. On a well-used hinge you can often see a faint whitened band: that is the drawn, oriented material, and it is the strongest part of the part.
必要な工具:
 マイクロメータ
 デジタルノギス 6インチ
 クラフトナイフ
 デジタル顕微鏡
2
2
Cycle one to death, and one the right way
Cycle one to death, and one the right way
Take two identical fresh hinges — two mint boxes, two caps.
**The first one**, fold and unfold steadily, counting, and inspect every hundred cycles under the microscope. A polypropylene hinge will pass a thousand cycles without visible change and keep going far past where you lose patience. Note what does change: the hinge gets **easier** and the white band gets clearer.
**The second one**, put in the freezer for an hour first, then fold it once, cold and fast. Polypropylene's ductile-to-brittle transition is near 0 °C, and a cold hinge that has never been flexed will often crack on that first fold. If it survives, fold it ten times cold and look again.
That pair is the whole practical rule for anyone designing one: **flex the hinge while it is warm, immediately after moulding**, before the part is ever cooled and packed. A production line does this automatically at the machine, and it is not a quality check — it is a manufacturing step that creates the orientation the hinge depends on.
Finally, abuse one in the other direction: fold it back on itself the wrong way, hard. The hinge is designed for one direction and the moulded radii are asymmetric; the wrong way puts the stress concentration on the sharp side.
必要な工具:
デジタル顕微鏡デジタルノギス 6インチ ストップウォッチ
 赤外線温度計
 ばねばかり(力計)
 実験ノート(複写式)
3
3
Print hinges in four polymers and watch three of them fail
Print hinges in four polymers and watch three of them fail
Design a simple test part: two 30 × 30 mm flat panels joined by a hinge web, with the web printed at four thicknesses — 0.25, 0.4, 0.6 and 1.0 mm — and generous radii either side.
Print the set in **PLA**, in **PETG**, in **ABS** and, if you can get it, in **polypropylene filament**. Print the hinge web so the layer lines run **along** the hinge axis, not across it: a printed hinge folded across its layer lines is folding along its weakest plane and will delaminate on the first cycle. That single orientation decision matters more than the material.
Fold each and count. Expect, roughly:
- **PLA** — a handful of cycles, then a clean brittle crack. Everyone who has printed a hinge has found this.
- **ABS** — better, but it crazes: fine white cracks appear and grow.
- **PETG** — better again, and it yields rather than snapping.
- **Polypropylene** — keeps going, and whitens exactly as the moulded ones did.
Plot cycles-to-failure against web thickness for each material. The thin webs win in every material, which is step 4's arithmetic showing up, and the polymer ranking is a property of the chemistry rather than of your printer.
The honest conclusion is one worth stating plainly: **a printed living hinge is a compromise**. The mechanism needs a polymer that cold-draws and a web free of layer boundaries, and FDM gives you neither perfectly. Design a printed hinge as a flexure with a limited life, or use a strip of PP sheet as an insert.
このステップの材料:
 PLA フィラメント1 個
 PETGフィラメント1 個
 ABS フィラメント1 個
 ポリプロピレン板1 個
必要な工具:
 3D プリンターデジタルノギス 6インチマイクロメータデジタル顕微鏡ばねばかり(力計)
 方眼紙
 透明保護メガネ実験ノート(複写式)
4
4
Bending strain, and why only some polymers survive it
Bending strain, and why only some polymers survive it
Jupyter ノートブックを読み込み中…
必要な工具:
方眼紙5
5
History and context
History and context
**Attribution, stated honestly.** No patent is asserted for this rung. The living hinge arrives with **polypropylene**, which Giulio Natta's group polymerised in 1954 and which was in commercial production by 1957, and the hinge appears in moulded products through the 1960s as designers discovered what the new polymer would tolerate. Many filings cover particular hinge geometries and particular products; none is the origin, and the mechanism — thin web, generous radii, orientation on first flex — was worked out in moulding shops rather than in a single invention.
**Why polypropylene and almost nothing else.** The hinge needs a polymer that **yields and cold-draws** instead of cracking, and that recovers its shape afterwards. Polypropylene's combination of a glass transition below room temperature and a semi-crystalline structure that reorganises under strain is close to unique among cheap commodity polymers. Polyethylene works but is floppy; nylon works but moves with humidity; the amorphous polymers craze.
**The idea to carry.** This is the third time in this batch that **deforming a polymer has made it stronger** — the film in rung 6, the bottle in rung 7, the hinge here. That is a genuinely different relationship with deformation from the one metals have, and it is worth holding as a principle: in a polymer, controlled strain is a processing step, not damage.
**Honest limits.** A living hinge is a one-direction, one-axis device with no load capacity across the hinge line and no tolerance for being pulled apart. It is sensitive to temperature — brittle near freezing, floppy when hot — and to UV, which embrittles polypropylene faster than most people expect outdoors. It cannot be repaired. And it has to be moulded correctly with the melt flowing **across** the hinge rather than along it, because flow direction sets the initial chain alignment; a hinge gated the wrong way fails early no matter how well its thickness was calculated.
材料
4- 1 個プレースホルダー
- 1 個プレースホルダー
- 1 個プレースホルダー
- 1 個プレースホルダー
関連ブループリント
これらのブループリントは知識を共有しています — 技術、材料、原理


CC0 パブリックドメイン
このブループリントはCC0で公開されています。許可を求めずに、自由にコピー、修正、配布、あらゆる目的で使用できます。
メイカーを応援するには、ブループリント経由で製品を購入してください。メイカーには メイカーコミッション がベンダーにより設定されています。または、このブループリントの新しいイテレーションを作成し、自分のブループリントにコネクションとして含めて収益を共有できます。