Ushirikiano
SANAA
UREMBO NA USTAWI
UJANJA
UTAMADUNI NA HISTORIA
BURUDANI
MAZINGIRA
CHAKULA NA VINYWAJI
UHANDISI WA KINYUME
SAYANSI
MICHEZO
TEKNOLOJIA
VAZI
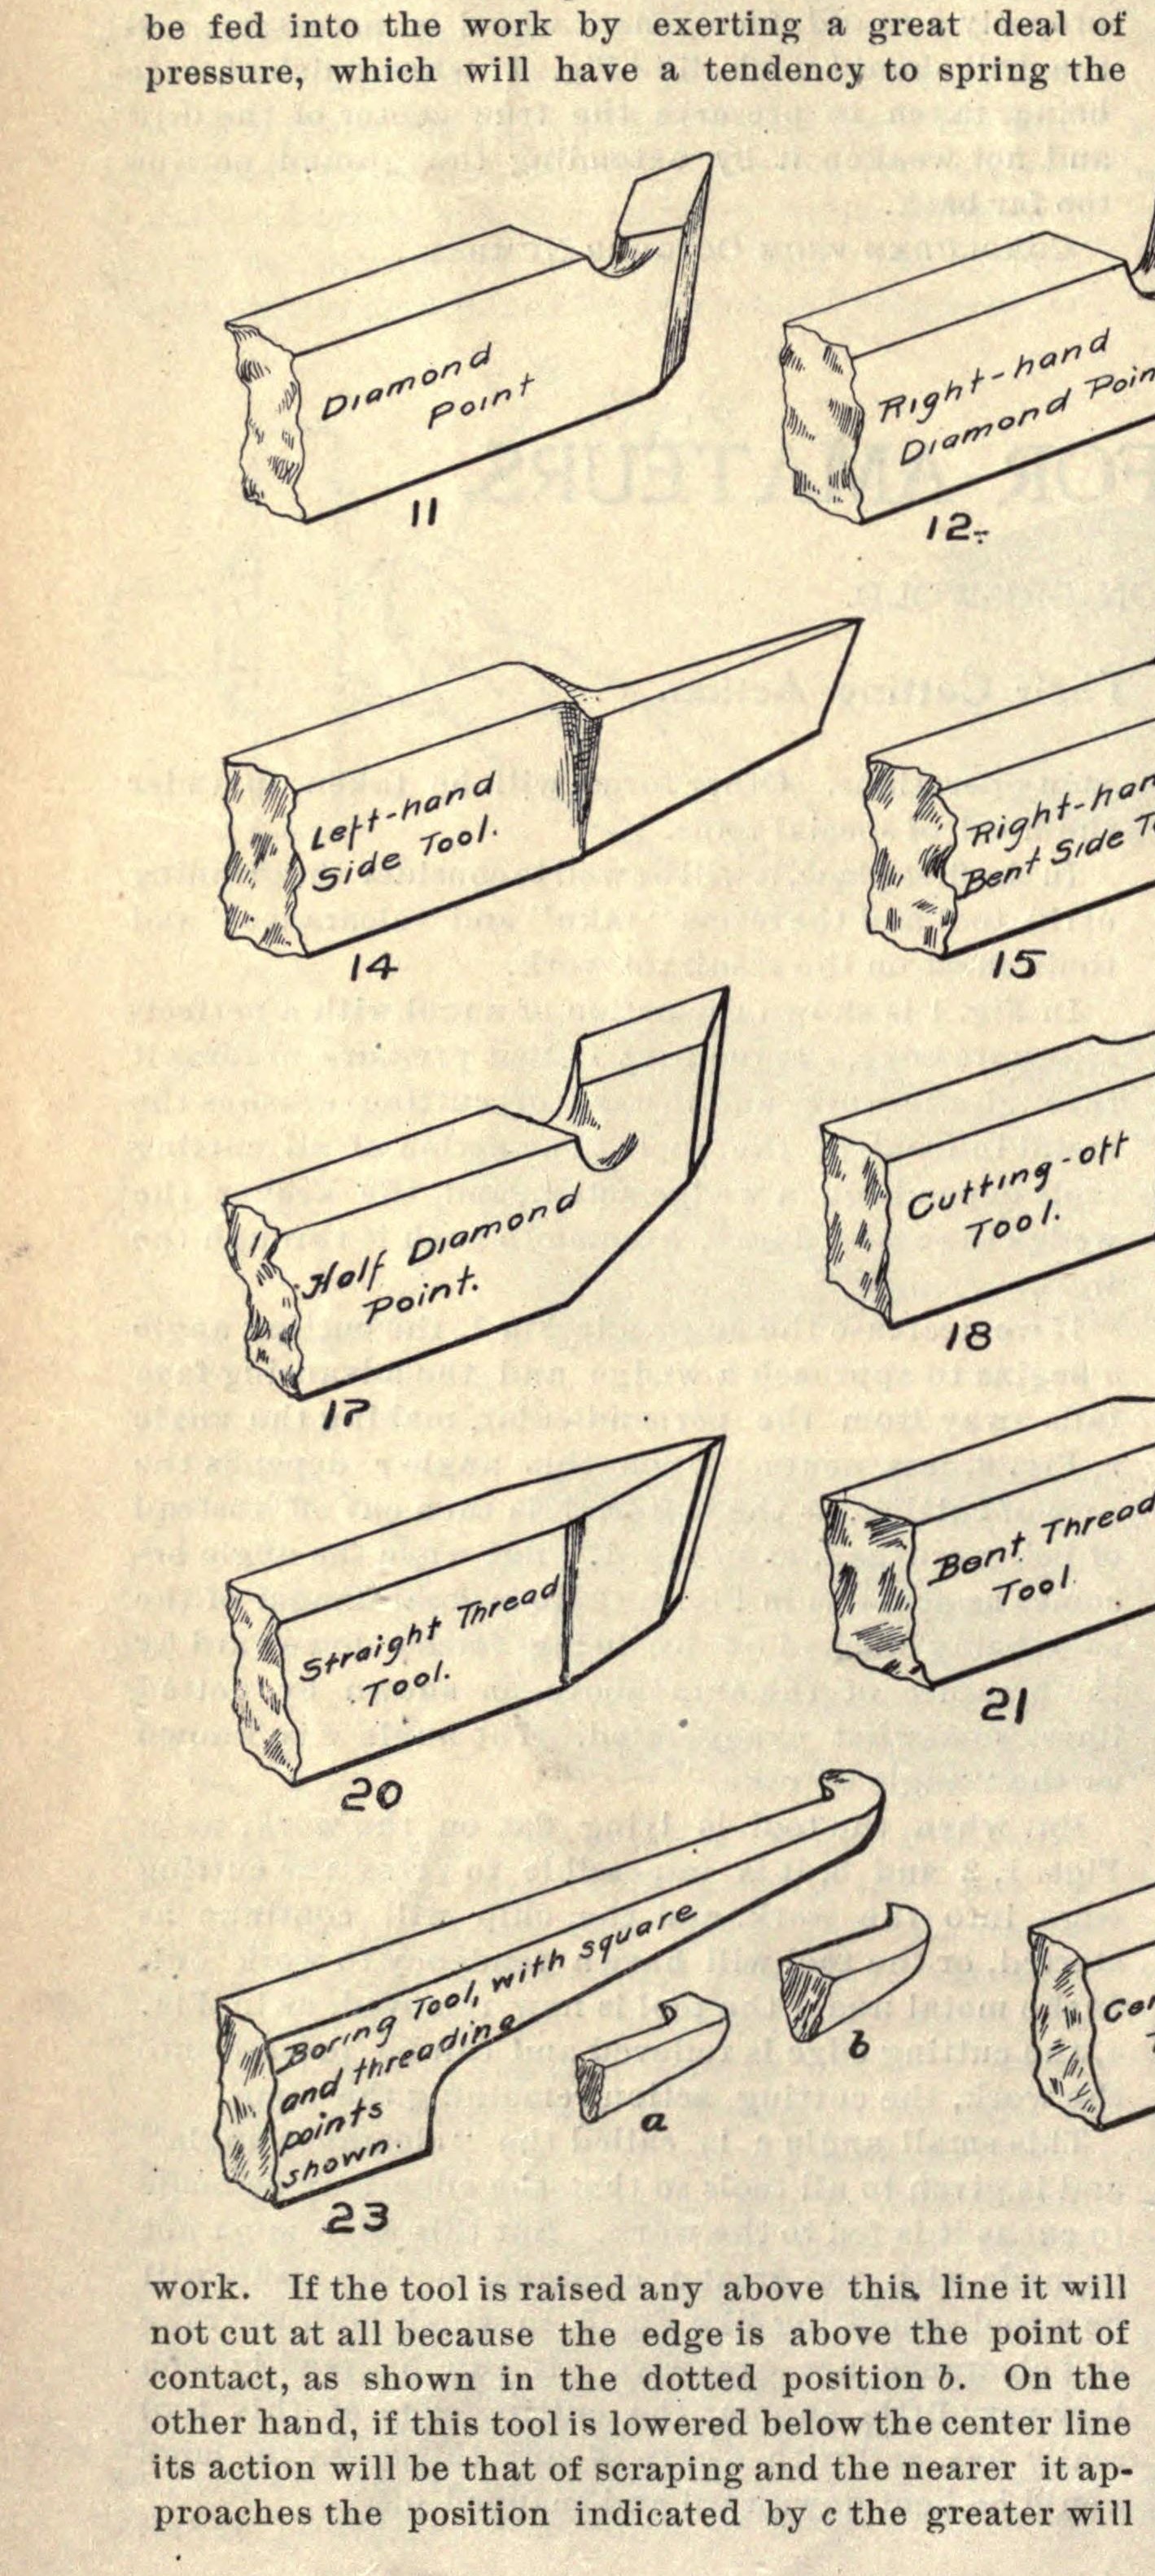

Forged Lathe Tools: Narrow Cutting-Off Tool and Bent-Tip Inside Boring Tool, Ground to Rake and Clearance (Griswold, 1904)
Two of the forged lathe tools in Robert Gibson Griswold's Tool Making for Amateurs (Boston, 1904): a cutting-off (parting) tool deep under a very narrow edge with relieved sides and a chip-splitting groove, and an inside boring and threading tool drawn to a long taper with the tip bent left; both ground to 3-5 degree clearance and the rake suited to the metal.
Juu
Half a day per tool
Maagizo
1
1
His angles
His angles
Inapakia daftari la Jupyter…
2
2
Read Griswold
Read Griswold
"The writer uses a tool slightly less than 1-16 in. wide and 1 in. deep for short cuts."
3
3
Forge the cutting-off tool
Forge the cutting-off tool
Forge tool steel (stock size ours, to suit your tool post) into a blade deep under the cutting edge, with the point the widest part and the sides relieved behind it so it cannot bind (his fig. 18): slightly under 1/16 in. wide and 1 in. deep for work up to 1/2 in., about 3/32 in. wide for work up to 2 in.
Vifaa kwa hatua hii:
 Fito ya chuma cha zana1 kipande
Zana zinazohitajika:
 Fua ya mhunzi
 Fuawe
 Nyundo
 Koleo za mhunzi
4
4
Forge the boring tools
Forge the boring tools
Draw three blanks to a long tapering end and bend the extreme tip to the left (fig. 23).
Vifaa kwa hatua hii:
Fito ya chuma cha zana1 kipandeZana zinazohitajika:
Fua ya mhunziFuaweNyundoKoleo za mhunzi5
5
Harden and temper
Harden and temper
Carbon tool steel: harden the ends (ours: cherry red into water) and temper in the yellows. Self-hardening steel must never be quenched in water.
Vifaa kwa hatua hii:
 Maji1 kipande
 Kitambaa cha emeri1 kipande
Zana zinazohitajika:
Fua ya mhunzi Ndoo
6
6
Grind the cutting-off tool
Grind the cutting-off tool
Give it front and side clearance of 3-5 degrees and little top rake. For larger work grind a round groove in the facing edge so the chip splits into two strings.
Zana zinazohitajika:
 Kisagia cha meza
7
7
Grind the boring points
Grind the boring points
Grind one boring tool as a diamond point, one as a small square point that works into corners, and one as a 60 degree thread point. Rake 3-10 degrees for iron and steel, little or none for brass and copper; hone the edges.
Zana zinazohitajika:
Kisagia cha meza Jiwe la kunoa
8
8
Troubleshooting
Troubleshooting
Lathe tool troubleshooting.
Flow
Loading...
9
9
History and honest limits
History and honest limits
From Robert Gibson Griswold, "Tool Making for Amateurs" IV, **Amateur Work** (Boston), vol. IV (1904-05), pp. 23-26 and figs. 11-25 (checked on the archive.org scan amateurwork04bostrich). He shows a full set (diamond point, side, round-nose, thread, centering, brass tools); this blueprint makes the two our heads need. Stock size and quench are ours.
Vifaa
3- 1 kipandeKishikilia Nafasi
- 1 kipandeKishikilia Nafasi
- 1 kipandeKishikilia Nafasi
Mchoro huu unatengeneza
Blueprint zinazohusiana
Blueprint hizi zinashiriki maarifa — mbinu, vifaa au kanuni
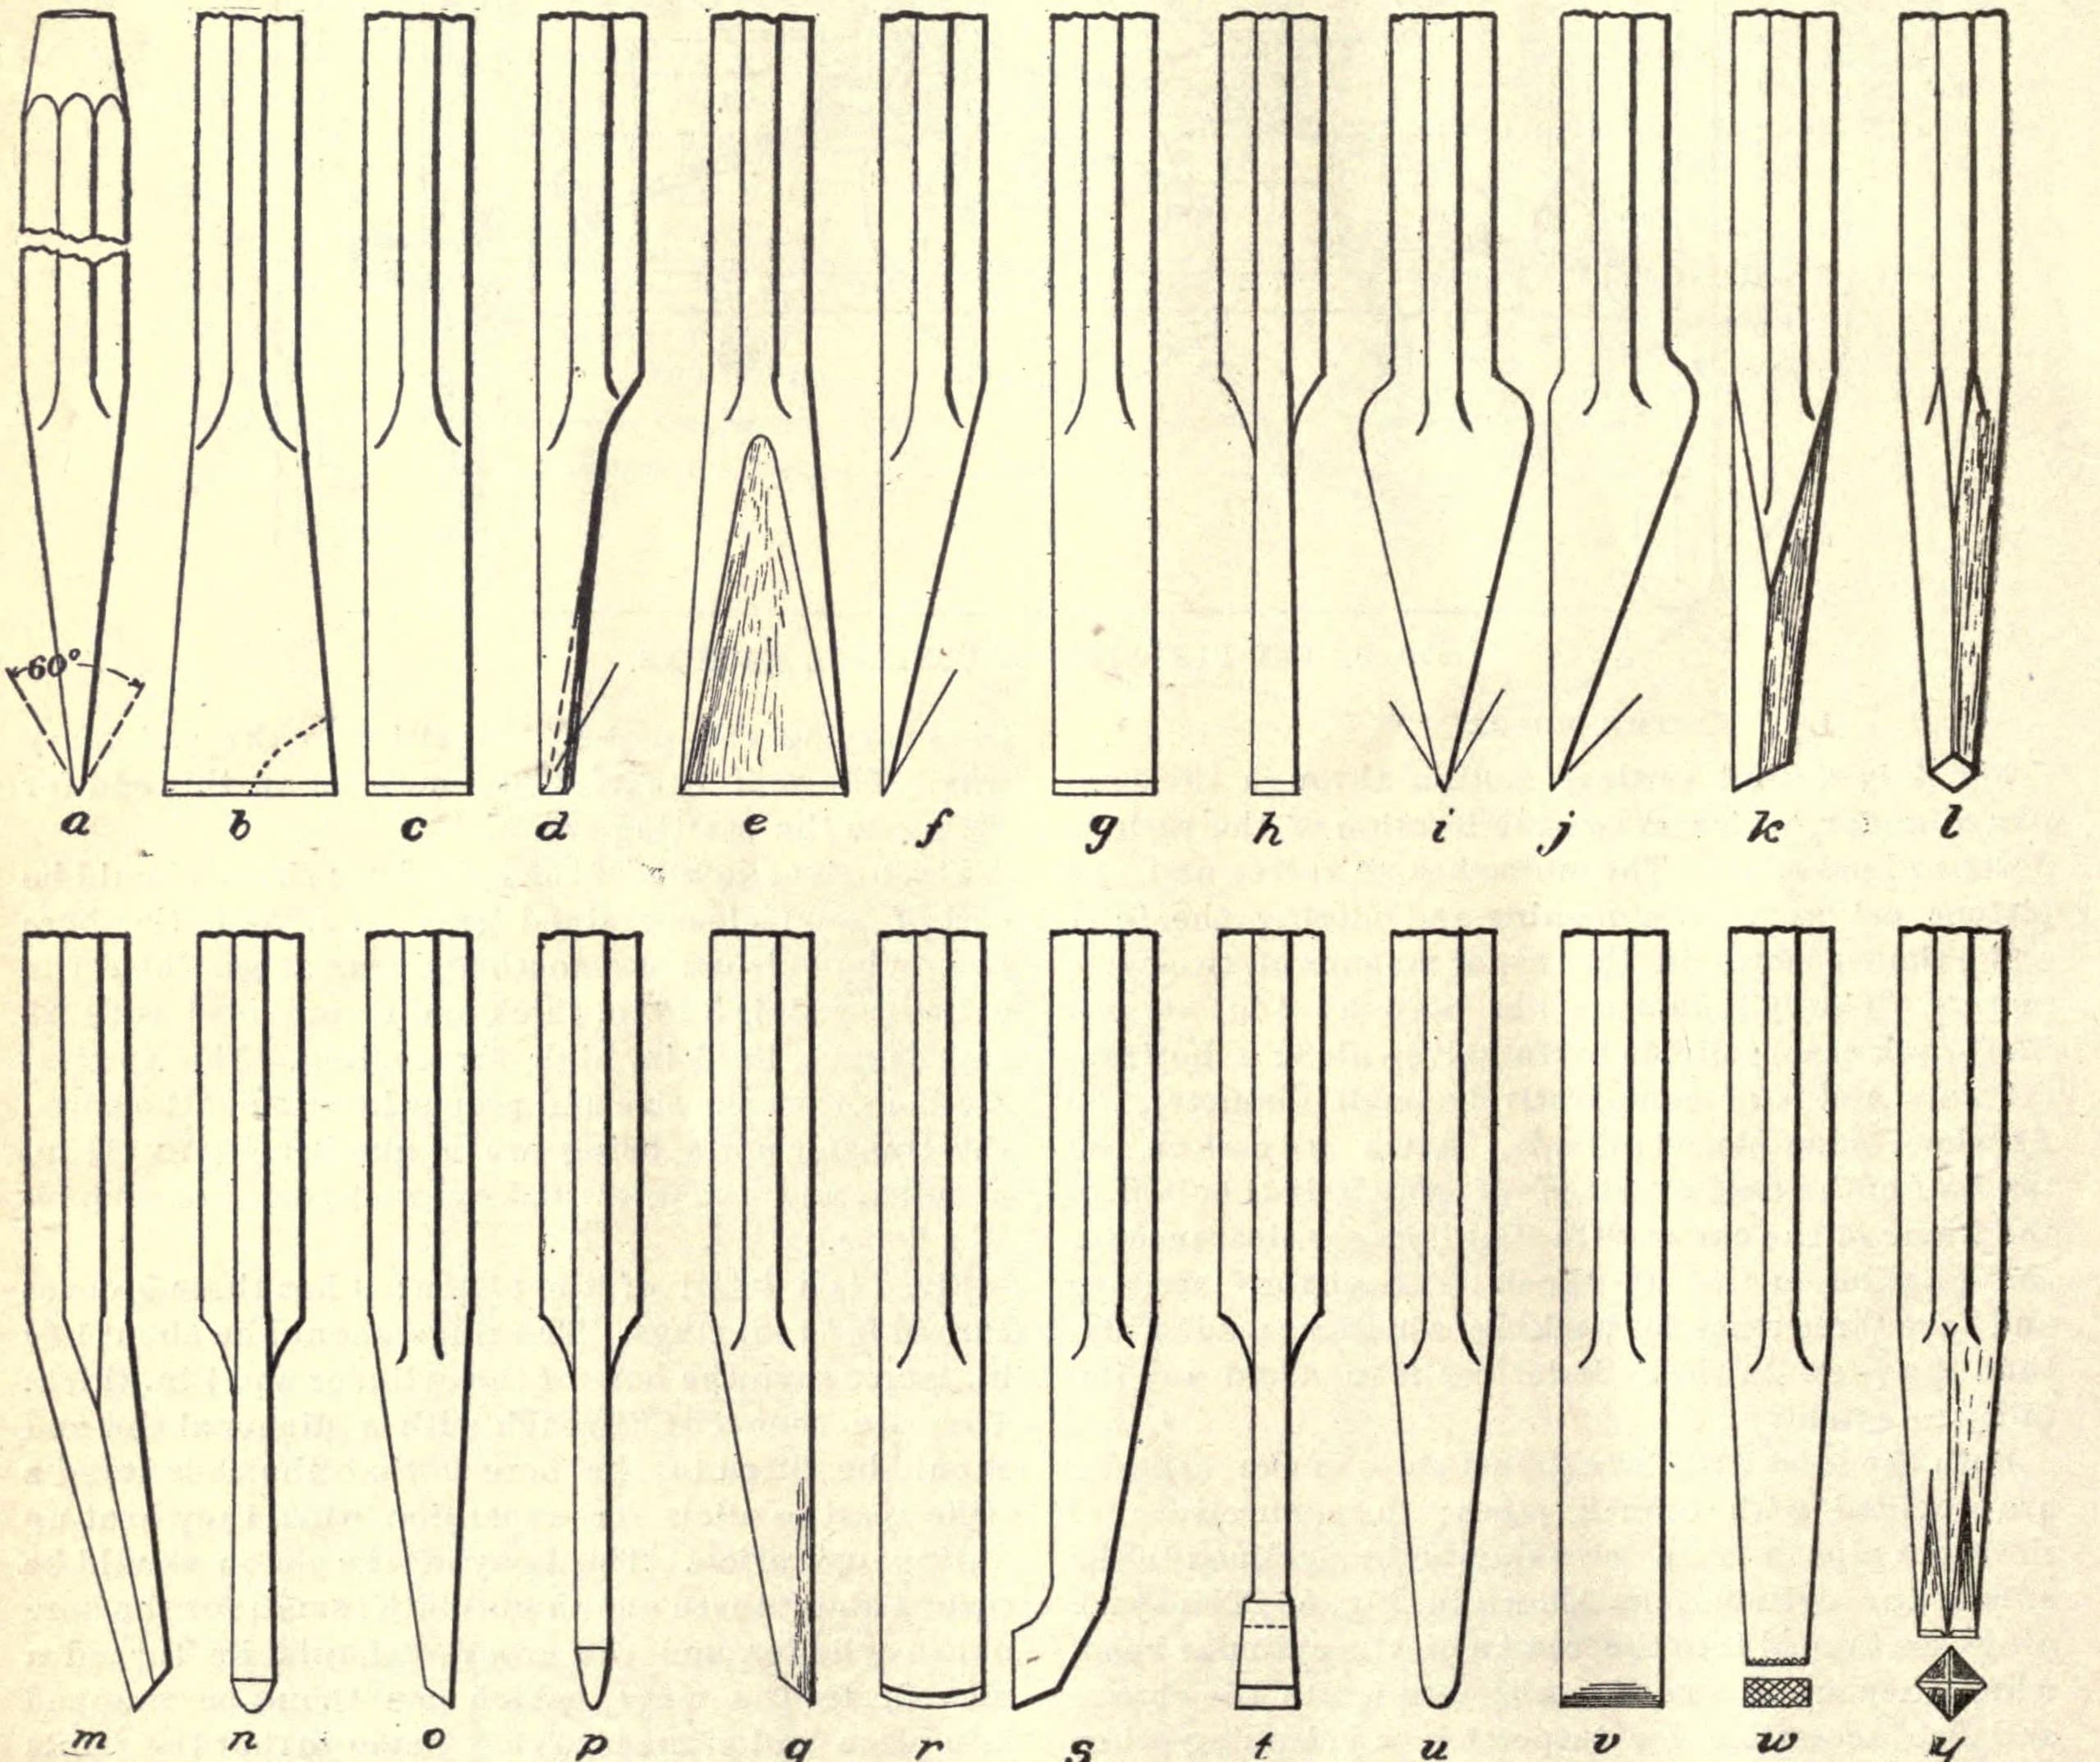
A Set of Cold Chisels: Flat, Gouge, Side, Cape, Diamond-Point and Round-Nose, Edge Hardened Only, Tempered Purple (Griswold, 1904)
na Forge
Uchimbaji chuma
9
0
0
0
0
0
Half-Round Taper Reamer: Tool Steel Turned to the Taper, Filed Flat to the Centre Line, Hardened (Griswold, Amateur Work, 1905)
na Forge
Uchimbaji chuma
9
0
0
0
0
0
CC0 Umma Wote
Mchoro huu umetolewa chini ya CC0. Uko huru kunakili, kubadilisha, kusambaza, na kutumia kazi hii kwa madhumuni yoyote, bila kuomba ruhusa.
Saidia Mtengenezaji kwa kununua bidhaa kupitia Mchoro wao ambapo wanapata Kamisheni ya Mtengenezaji iliyowekwa na Wachuuzi, au unda marudio mapya ya Mchoro huu na uiunganishe kama kiungo katika Mchoro wako kuchangia mapato.