Ushirikiano
SANAA
UREMBO NA USTAWI
UJANJA
UTAMADUNI NA HISTORIA
BURUDANI
MAZINGIRA
CHAKULA NA VINYWAJI
UHANDISI WA KINYUME
SAYANSI
MICHEZO
TEKNOLOJIA
VAZI
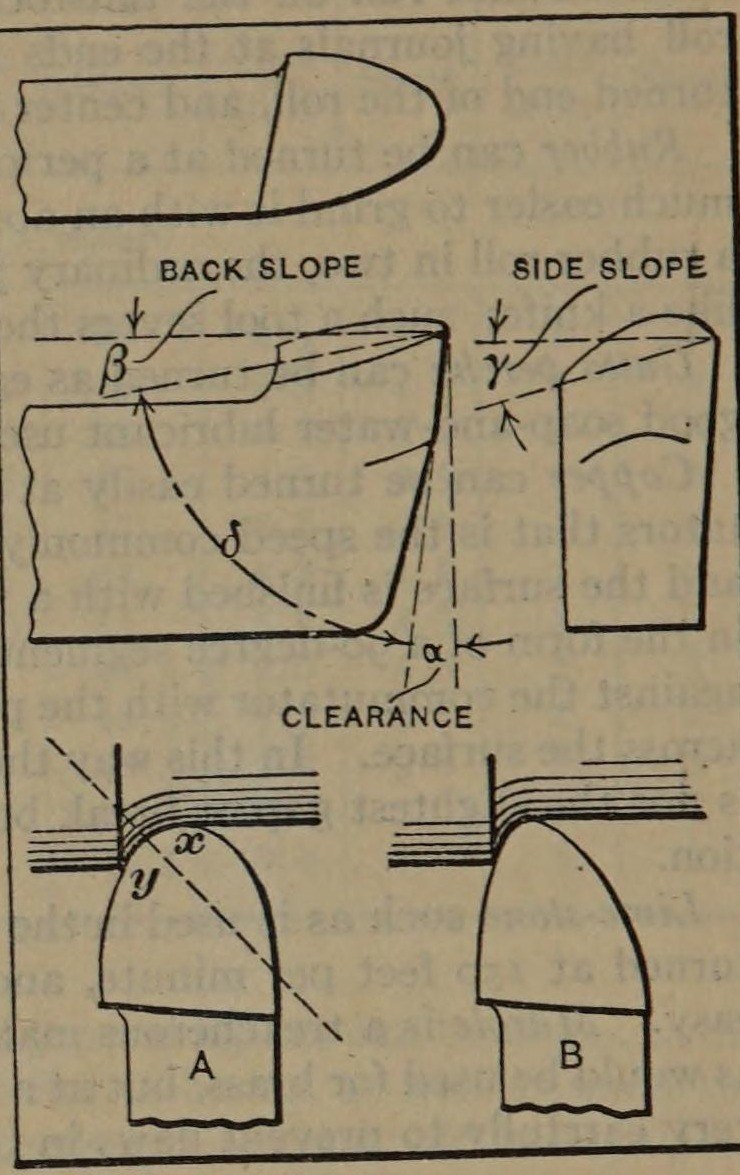


Lathe Cutting Tool: Ground to the Clearance and Slope for Each Metal (Machinery's Handbook, 1924)
A lathe turning tool ground from tool steel bar. Three things decide how well it cuts: the shape of the edge seen from above, the clearance under the edge, and the slope of the top the chip slides over. The Handbook gives the angles for each kind of metal to be turned.
Variable: the metal to be turned. Clearance 8 to 10° for general work, 12 to 14° for brass. Soft steel: back slope 8°, side slope 14 to 20°. Very hard steel: 5° and 9°. Brass: flat on top.
Source: Machinery's Handbook (1924), pp. 887-889, Tool Grinding. Unknown: the steel and the bar size. Picture: the Handbook's figure.
Kati
Unknown
Maagizo
1
1
Choose the edge shape
Choose the edge shape
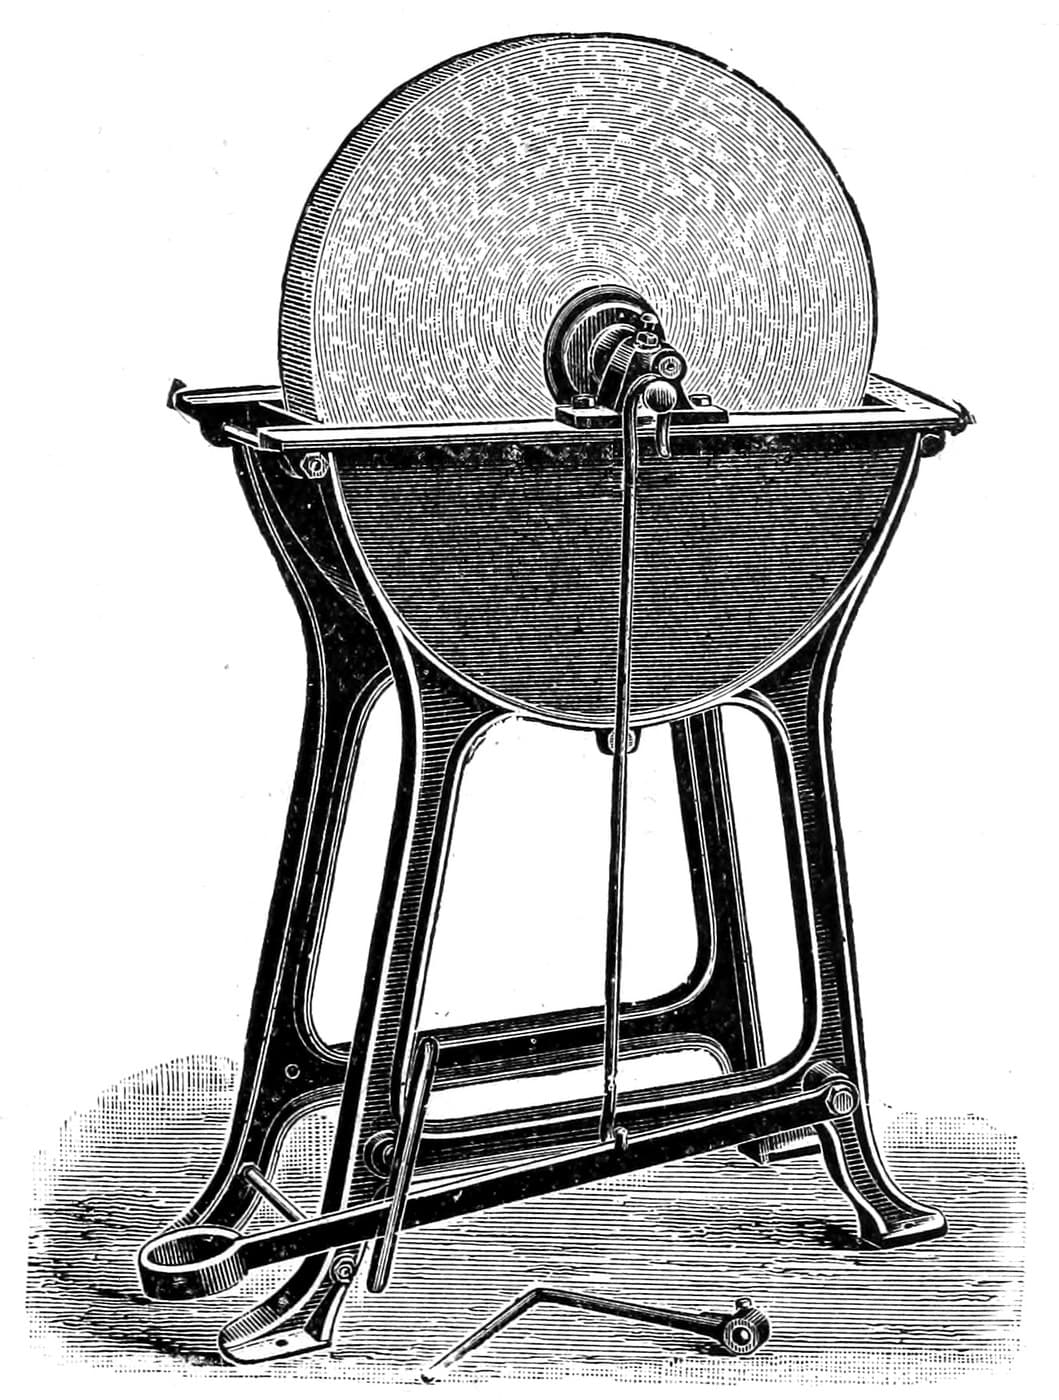
Grind the edge, seen from above, to suit the job. A large-radius edge roughs and keeps its edge at higher speed; a smaller point is better on flexible work that would chatter. A parting tool must be widest at the cutting edge so it does not bind in its groove. Ours: square tool steel bar. Not given: the steel, the bar size.
Vifaa kwa hatua hii:
 Kipande cha mraba cha feleji ya zana1 tool blank
Zana zinazohitajika:
 Jiwe la kunoa la gurudumu
 Maji
2
2
Grind the clearance and the slope
Grind the clearance and the slope
Grind clearance under the edge: 8 to 10° for general turning, 12 to 14° for brass and soft metals; too much weakens the edge. Slope the top away from the working part of the edge. A roughing tool for medium or soft steel gets a back slope of 8° and a side slope of 14 to 20°; for very hard steel, 5° and 9°. A broad finishing tool slopes straight back. Thread tools and tools for brass or chilled iron are flat on top; very hard metals get almost no slope and little clearance. Roughing tools cut fastest with a lip angle near 61°, but cast iron cuts better at about 68°.
Zana zinazohitajika:
Jiwe la kunoa la gurudumu Kipima-pembe
3
3
Grind without burning
Grind without burning
Press the tool only moderately against the wheel and draw it away often, especially when grinding a broad flat face, so the edge does not overheat and burn. Keep the wheel supplied with plenty of cooling water.
Zana zinazohitajika:
Jiwe la kunoa la gurudumuMajiVifaa
1- 1 tool blankKishikilia Nafasi
Vifaa vya Michoro Iliyounganishwa

Mchoro huu unatengeneza

CC0 Umma Wote
Mchoro huu umetolewa chini ya CC0. Uko huru kunakili, kubadilisha, kusambaza, na kutumia kazi hii kwa madhumuni yoyote, bila kuomba ruhusa.
Saidia Mtengenezaji kwa kununua bidhaa kupitia Mchoro wao ambapo wanapata Kamisheni ya Mtengenezaji iliyowekwa na Wachuuzi, au unda marudio mapya ya Mchoro huu na uiunganishe kama kiungo katika Mchoro wako kuchangia mapato.