SANAA
UREMBO NA USTAWI
UJANJA
UTAMADUNI NA HISTORIA
BURUDANI
MAZINGIRA
CHAKULA NA VINYWAJI
UHANDISI WA KINYUME
SAYANSI
MICHEZO
TEKNOLOJIA
VAZI


Tool-Steel Bar: Crucible Steel Drawn Out at a Cherry-Red Heat
Sheffield poured its crucible cast steel into octagonal or rectangular iron moulds and drew the ingots out into rods under the tilt hammer. That bar, eight-sided or square, was the stock for chisels, punches, files and blades. Andrew Ure's 1839 warning still holds: this steel must not go much above a cherry-red heat, or it turns brittle.
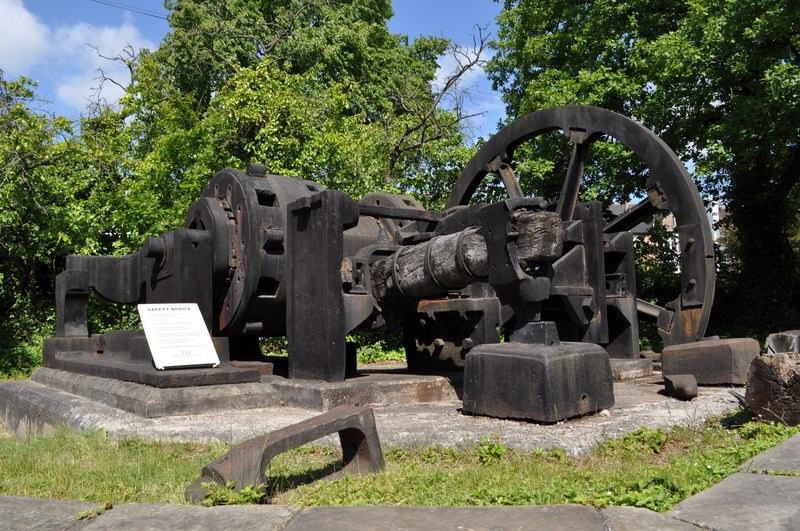
The picture: a water-driven tilt hammer at Abbeydale Industrial Hamlet, Sheffield.
Juu
A day at the forge
Maagizo
1
1
Heat gently to cherry red
Heat gently to cherry red
Bring the crucible-steel ingot up slowly in the forge to a cherry-red heat and no hotter. Ure: in its usual state cast steel will not bear much more without becoming brittle, and it will not take a welding heat.
Vifaa kwa hatua hii:
 Feleji ya kalibu2 kg
 Mkaa1 as required
Zana zinazohitajika:
 Fua ya mhunzi
 Koleo za mhunzi
 Glavu za kulehemu
 Aproni ya Ngozi
 Miwani ya usalama
2
2
Draw out a billet
Draw out a billet
On the anvil, with a striker on the sledge, draw the ingot out square, turning it a quarter after each pair of blows. Reheat as soon as the colour drops below red; never hammer it cold. Stop at a square billet of the size you need, or carry on drawing it flat into a rectangular bar for axe heads and picks.
Vifaa kwa hatua hii:
Mkaa1 as requiredZana zinazohitajika:
 Fuawe
 Nyundo kubwa
 Nyundo yenye kichwa cha msalabaKoleo za mhunziGlavu za kulehemuAproni ya NgoziMiwani ya usalama
3
3
Knock the corners to an octagon
Knock the corners to an octagon
For octagon bar, set the square bar on a corner and hammer the four corners down evenly until all eight faces are equal, finishing in the matching groove of a swage block.
Zana zinazohitajika:
FuaweNyundo yenye kichwa cha msalaba Kibao cha kutengeneza chenye matunduKoleo za mhunziGlavu za kulehemuAproni ya NgoziMiwani ya usalama
4
4
Check and cool slowly
Check and cool slowly
Check the size across the flats with a caliper, then let the bar cool slowly in the dying forge (our choice, to leave it soft for cutting and filing).
Zana zinazohitajika:
 Kipima-unene cha dijitali cha inchi 6Fua ya mhunzi
Zana Zinazohitajika
10- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
Mchoro huu unatengeneza

Blueprint zinazohusiana
Blueprint hizi zinashiriki maarifa — mbinu, vifaa au kanuni


CC0 Umma Wote
Mchoro huu umetolewa chini ya CC0. Uko huru kunakili, kubadilisha, kusambaza, na kutumia kazi hii kwa madhumuni yoyote, bila kuomba ruhusa.
Saidia Mtengenezaji kwa kununua bidhaa kupitia Mchoro wao ambapo wanapata Kamisheni ya Mtengenezaji iliyowekwa na Wachuuzi, au unda marudio mapya ya Mchoro huu na uiunganishe kama kiungo katika Mchoro wako kuchangia mapato.