សិល្បៈ
សម្រស់ និង សុខុមាលភាព
សិប្បកម្ម
វប្បធម៌ និង ប្រវត្តិសាស្ត្រ
ការកម្សាន្ត
បរិស្ថាន
ម្ហូប និង ភេសជ្ជៈ
វិស្វកម្មបញ្ច្រាស
វិទ្យាសាស្ត្រ
កីឡា
បច្ចេកវិទ្យា
ប្រដាប់ដែលស្លៀក

Faraday's Law: The One Process You Can Calculate Exactly
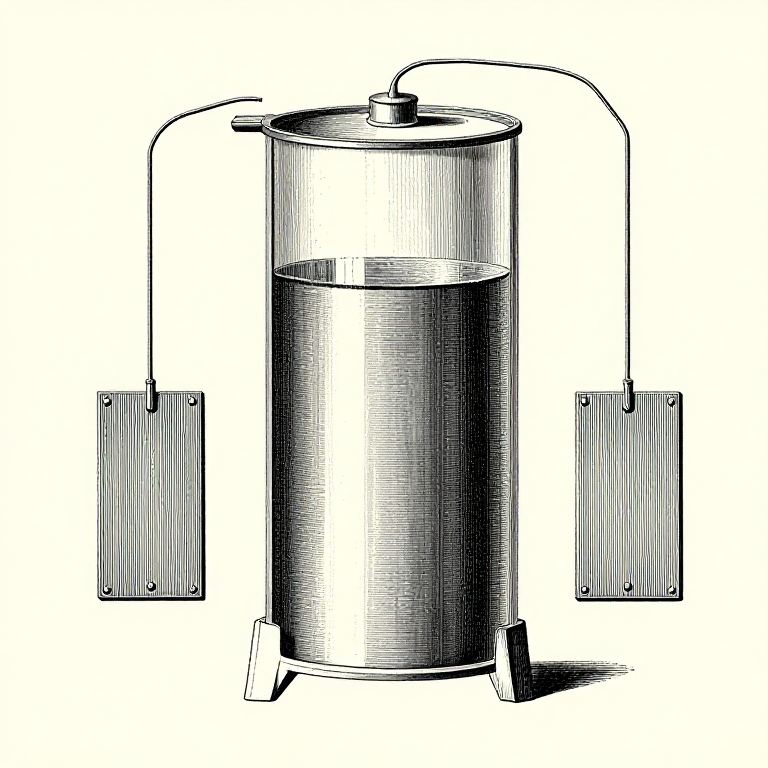
Electroplating is unusual among manufacturing processes: the amount of metal deposited can be calculated exactly, in advance, from the current and the time.
Each metal ion needs a fixed number of electrons to become an atom, so the charge that passes is a direct count of the atoms deposited. Faraday worked this out in the 1830s and it has not needed amending.
What the calculation does not give for free is the **current efficiency** — the fraction of the current that actually deposits metal rather than splitting water. For nickel it is about 95%; for chromium it is about 15%, which is why chrome plating is slow, hot and extravagant.
មធ្យម
3 hours
ការណែនាំ
1
1
Setting up so the numbers mean something
Setting up so the numbers mean something
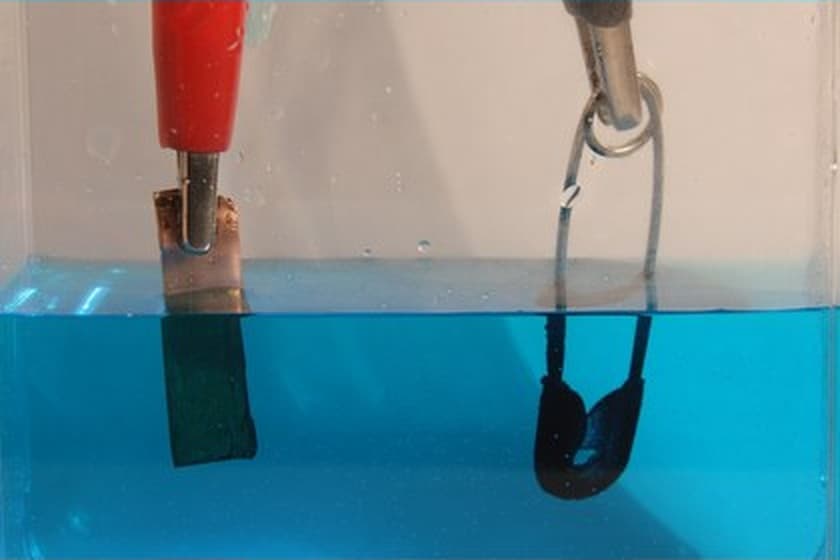
**The part is the cathode**, connected to the negative terminal. Metal ions in solution are positive, so they are attracted to it and are reduced to metal there.
**The anode is usually the same metal being plated**, and it dissolves at the same rate as the cathode gains, keeping the bath concentration constant. That is why a nickel bath has nickel anodes and a copper bath has copper.
**An inert anode** — lead, platinised titanium, graphite — is used where a soluble one would not work, chromium being the main case. Then the bath is depleted as plating proceeds and must be topped up.
**Measure the current, do not assume it.** A bench supply's display is a guide; a meter in series is the measurement. Every number in this rung depends on the current actually being what it says.
**Measure the area properly**, including both faces and the edges of a flat part. A part plated at "1 amp" with its area guessed at half its real value gets half the thickness intended.
**Agitate.** Solution next to the cathode is depleted of ions as it plates, and without movement the deposit goes rough and burnt. A magnetic stirrer, air sparging, or moving the work — every real plating bath moves.
សម្ភារៈសម្រាប់ជំហាននេះ៖
 ស៊ុលហ្វាតស្ពាន់ (កម្រិតមន្ទីរពិសោធន៍)1 ដុំ
 សន្លឹកស្ពាន់ក្រហម2 ដុំ
 ទឹកចម្រោះ1 ដុំ
ឧបករណ៍ដែលត្រូវការ៖
 ប្រភពថាមពលតុការងារអាចលៃបាន
 ម៉ាល់ទីម៉ែត្រឌីជីថល — ជួរស្វ័យប្រវត្តិ RMS ពិត
 កែវប៊ីកឃ័របូរ៉ូស៊ីលីកាត
 ចានកម្តៅមានឧបករណ៍កូរម៉ាញេទិក
2
2
The calculation, and the thicknesses actually used
The calculation, and the thicknesses actually used
កំពុងផ្ទុកសៀវភៅ Jupyter…
ឧបករណ៍ដែលត្រូវការ៖
 កុំព្យូទ័រតុ
3
3
Measuring what actually happened
Measuring what actually happened
The calculation predicts; the balance confirms. Doing both is how the current efficiency of a particular bath is discovered, and after that the calculation can be trusted.
**Weigh before and after**, dry, on a scale reading to a milligram for a small part. The gain is the metal deposited.
**Compare with the prediction.** The ratio is the current efficiency of that bath at that current density and temperature, and it is worth writing on the tank.
**An efficiency above 100% means something is wrong** — the part was not dry, or it gained weight some other way, or the current was higher than recorded. It is the same impossible-number rule as a chemical yield.
**Measure the thickness directly** where it matters: a micrometer across a flat part before and after, which works down to a few microns; or a magnetic or eddy current gauge, which is what industry uses; or a cross-section under a microscope, which is destructive and definitive.
**Expect the thickness to vary across the part**, and that is not an error in the calculation — Faraday's law gives the TOTAL metal deposited, and the distribution is the next rung's subject.
សម្ភារៈសម្រាប់ជំហាននេះ៖
 សន្លឹកនីកែល1 ដុំ
 បន្ទះដែកថែបទន់1 ដុំ
ឧបករណ៍ដែលត្រូវការ៖
 ជញ្ជីងល្អិត
 មីក្រូម៉ែត្រ
 ជញ្ជីងវាស់ឌីជីថល ៦ អ៊ីញ
4
4
Running a bath: temperature, pH and what to log
Running a bath: temperature, pH and what to log
A plating bath is a chemical system with a working window, and drifting outside it degrades the deposit long before the bath stops working.
**Temperature.** Higher temperature allows higher current density and gives a softer, less stressed deposit; too cold and the deposit is brittle and burns at modest current. A Watts nickel bath runs at 45 to 60 C.
**pH.** Nickel wants about 4.0 to 4.5. Too low and the efficiency falls as more current goes to hydrogen; too high and basic salts precipitate into the deposit as roughness.
**Concentration.** Falls as the bath is used if the anodes cannot keep up, and low metal concentration shows up first as burning at the edges.
**Additives.** Brighteners, levellers and wetting agents. They are consumed, they break down into products that accumulate, and they are the usual reason a bath that worked last month does not now.
**Log every run:** date, part, area, current, time, temperature, pH, and the measured weight gain. Six lines, and they turn "the plating has gone dull" into a curve with a cause.
**A Hull cell** is the standard diagnostic: a small tank shaped so one test panel sees a whole range of current densities at once. One panel shows the bath's working range, where it burns and where it is too thin — and it uses a few hundred millilitres of solution.
សម្ភារៈសម្រាប់ជំហាននេះ៖
 នីកែលស៊ុលហ្វាតហ៊ិចសាអ៊ីដ្រាត1 ដុំ
 ឈុតស្រោបលោហៈដោយអគ្គិសនី1 ដុំ
ឧបករណ៍ដែលត្រូវការ៖
 ទែម៉ូម៉ែត្រមន្ទីរពិសោធន៍ប្រភពថាមពលតុការងារអាចលៃបានម៉ាល់ទីម៉ែត្រឌីជីថល — ជួរស្វ័យប្រវត្តិ RMS ពិត
សម្ភារៈ
7- កន្លែងទុក
- 2 ដុំកន្លែងទុក
- 1 ដុំកន្លែងទុក
- 1 ដុំកន្លែងទុក
- 1 ដុំកន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
ឧបករណ៍ចាំបាច់
9- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
ប្លង់ពាក់ព័ន្ធ
ប្លង់ទាំងនេះចែករំលែកចំណេះដឹង — បច្ចេកទេស សម្ភារៈ ឬគោលការណ៍
CC0 សាធារណៈ
ប្លង់នេះត្រូវបានចេញផ្សាយក្រោម CC0។ អ្នកមានសិទ្ធិចម្លង កែប្រែ ចែកចាយ និងប្រើប្រាស់ដោយមិនចាំបាច់សុំអនុញ្ញាត។
គាំទ្រអ្នកបង្កើតដោយទិញផលិតផលតាមរយៈប្លង់របស់ពួកគេ ដែលពួកគេទទួលបាន កម្រៃជើងសារអ្នកបង្កើត កំណត់ដោយអ្នកលក់ ឬបង្កើតកំណែថ្មីនៃប្លង់នេះ ហើយបញ្ចូលជាការតភ្ជាប់ក្នុងប្លង់របស់អ្នកដើម្បីចែករំលែកចំណូល។