សិល្បៈ
សម្រស់ និង សុខុមាលភាព
សិប្បកម្ម
វប្បធម៌ និង ប្រវត្តិសាស្ត្រ
ការកម្សាន្ត
បរិស្ថាន
ម្ហូប និង ភេសជ្ជៈ
វិស្វកម្មបញ្ច្រាស
វិទ្យាសាស្ត្រ
កីឡា
បច្ចេកវិទ្យា
ប្រដាប់ដែលស្លៀក
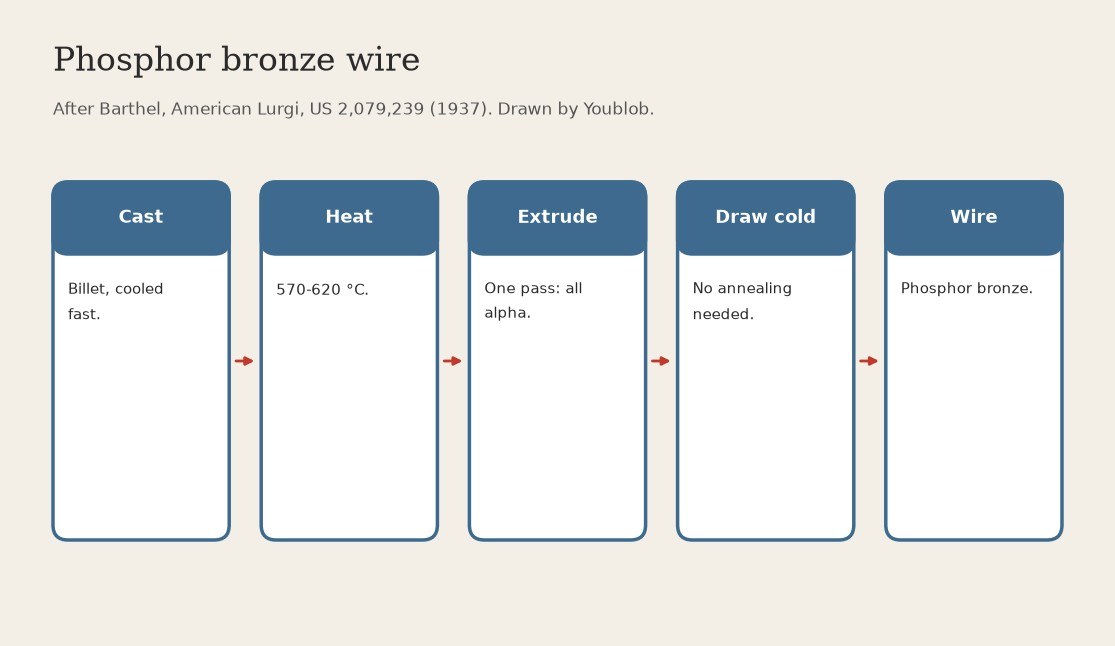

Phosphor Bronze Wire: Cast Billet Extruded at 570-620 °C, then Cold Drawn without Annealing (Barthel, Lurgi, US 2,079,239)
Cast phosphor bronze holds a brittle tin-rich phase that made wire drawing a long round of drawing and annealing. Barthel found that extruding the casting at 570-620 °C kneads it into one soft, even phase, after which it draws straight down to wire.
Result: phosphor bronze wire, drawn without intermediate annealing.
Source: Barthel, US 2,079,239 (American Lurgi, 1937). His temperature is for about 8 % tin; our ingot has about 9 %, so the same range is ours. Not given: extrusion ratio, die sizes. Picture drawn by Youblob.
កម្រិតខ្ពស់
2 days
ការណែនាំ
1
1
Cast a billet and cool it fast
Cast a billet and cool it fast
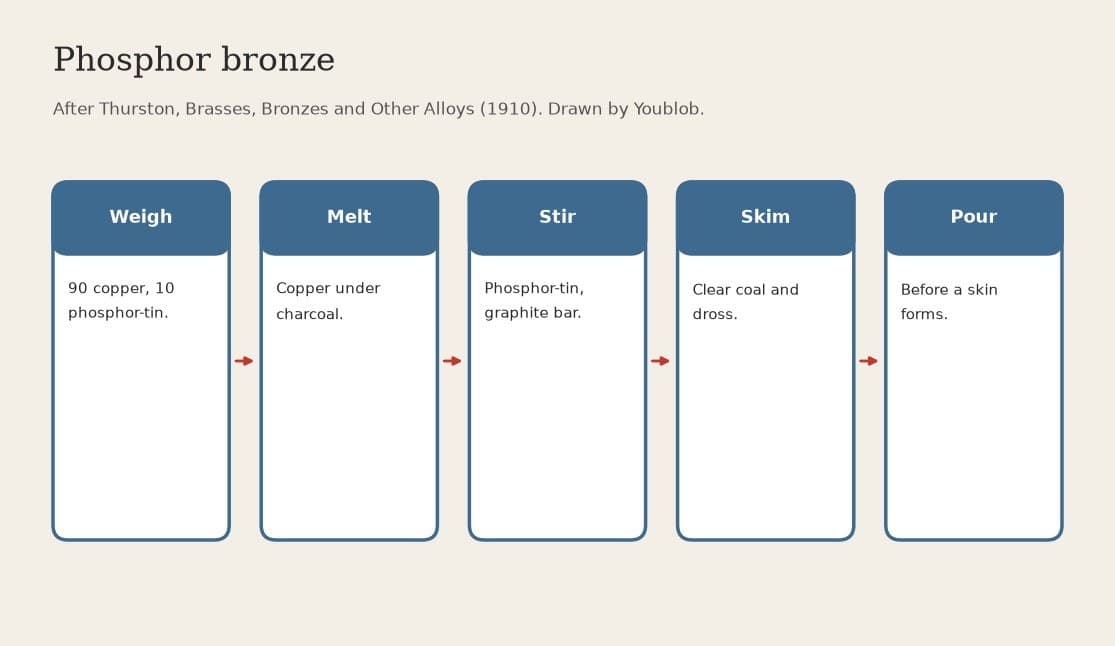
Melt the phosphor bronze and cast it into a billet, cooling it rapidly. Ours: cast in an ingot mould and quench.
សម្ភារៈសម្រាប់ជំហាននេះ៖
 ដុំសំរិទ្ធផូស្វ័រ1 as required
ឧបករណ៍ដែលត្រូវការ៖
 ឆ្នាំងក្រាប់ហ្វីតលាយដីឥដ្ឋ
 ឡរលាយលោហៈក្នុងឆ្នាំង
 ពុម្ពចាក់ដុំលោហៈ
 ធុងជ្រលក់ត្រជាក់
2
2
Heat the billet to 570-620 °C
Heat the billet to 570-620 °C
Heat the billet to between about 570 and 620 °C (Barthel's range for about 8 % tin and 0.3 % phosphorus). Temperature: 500-650 °C overall; the less tin, the hotter (about 650 °C for 6 % tin).
ឧបករណ៍ដែលត្រូវការ៖
 ឡដុតមូហ្វល
 ពីរ៉ូម៉ែត្រ
3
3
Extrude it in one pass
Extrude it in one pass
Extrude the hot billet in an extrusion press. The kneading makes the metal even all through, practically all alpha. For thick products with little reduction, cold-press the billet 10-20 % first.
ឧបករណ៍ដែលត្រូវការ៖
 ម៉ាស៊ីនសង្កត់ច្របាច់អ៊ីដ្រូលិក
4
4
Cold draw to wire without annealing
Cold draw to wire without annealing
Draw the extruded rod cold through dies down to wire; Barthel's metal needs no annealing between draws. Ours: a steel drawplate with drawing lubricant, one hole smaller each pass.
ឧបករណ៍ដែលត្រូវការ៖
 បន្ទះទាញលួសដែក
 ប្រេងរំអិលសម្រាប់ទាញលួស
សម្ភារៈ
1- 1 as requiredកន្លែងទុក
ឧបករណ៍ចាំបាច់
9- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
ប្លង់នេះធ្វើ
ប្លង់ពាក់ព័ន្ធ
ប្លង់ទាំងនេះចែករំលែកចំណេះដឹង — បច្ចេកទេស សម្ភារៈ ឬគោលការណ៍
CC0 សាធារណៈ
ប្លង់នេះត្រូវបានចេញផ្សាយក្រោម CC0។ អ្នកមានសិទ្ធិចម្លង កែប្រែ ចែកចាយ និងប្រើប្រាស់ដោយមិនចាំបាច់សុំអនុញ្ញាត។
គាំទ្រអ្នកបង្កើតដោយទិញផលិតផលតាមរយៈប្លង់របស់ពួកគេ ដែលពួកគេទទួលបាន កម្រៃជើងសារអ្នកបង្កើត កំណត់ដោយអ្នកលក់ ឬបង្កើតកំណែថ្មីនៃប្លង់នេះ ហើយបញ្ចូលជាការតភ្ជាប់ក្នុងប្លង់របស់អ្នកដើម្បីចែករំលែកចំណូល។