예술
뷰티 및 웰니스
공예
문화 및 역사
엔터테인먼트
환경
음식 및 음료
역공학
과학
스포츠
기술
웨어러블
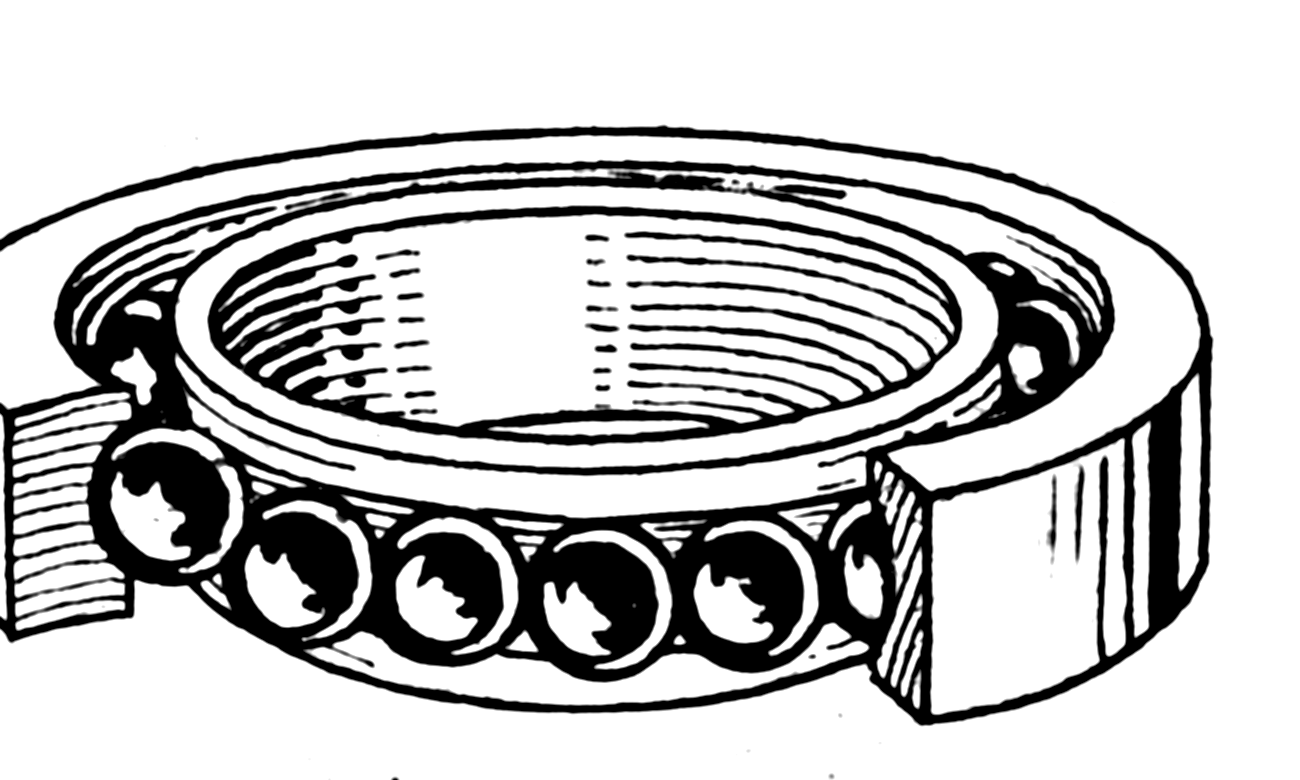

Ball Bearings: Races, Balls and Cage
A ball bearing has four parts: an outer race, an inner race, the balls that roll between them, and a cage that keeps the balls evenly spaced. Almost all of it is steel, usually 52100 (1% chromium, 1% carbon), which can be made very hard and tough by heat treating; 440C stainless is used where rust is a problem. The races are turned from tubing, the balls are cold headed from thick wire, both are hardened, tempered, ground and lapped to an almost mirror finish, and the cage is stamped from thin sheet. Even an inexpensive bearing's balls may be out of round by no more than 25 millionths of an inch; precision bearings allow five millionths.
고급
Factory process
안내
1
1
Turn the races
Turn the races
Cut the basic shape of both races from steel tubing on automatic lathe-like machines, leaving every dimension slightly oversize: the steel usually warps in heat treatment.
이 단계의 재료:
 베어링강 관(52100)1 as required
필요한 도구:
 자동 선반
2
2
Harden and temper the races
Harden and temper the races
Heat to about 843 °C (1,550 °F) for up to several hours depending on size, then quench in oil: hard but brittle. Temper at about 149 °C (300 °F) and let cool in air: hard and tough.
필요한 도구:
 유랭 연속 담금질로
 뜨임로
3
3
Grind and lap the races
Grind and lap the races
The hardened steel is too hard to cut, so grind almost every surface: the fitting surfaces round, the sides flat. Grind the ball track, then lap it for several hours with a very fine abrasive slurry to an almost mirror finish.
이 단계의 재료:
 래핑 컴파운드1 as required
필요한 도구:
 베어링 궤도륜 연삭기
 궤도 래핑기
4
4
Cold head the balls
Cold head the balls
Feed thick wire from a roll into a machine that cuts off a short piece and smashes both ends in toward the middle between two dies, without heating. The ball comes out with a ring of "flash" round its middle.
이 단계의 재료:
 베어링강 선재(52100)1 as required
필요한 도구:
 냉간 압조기
5
5
Remove the flash
Remove the flash
Run the balls many times round rough grooves between two cast-iron discs, one turning and one fixed, until the flash is gone and they are nearly round. Leave about 0.008 in (0.2 mm) for finishing.
필요한 도구:
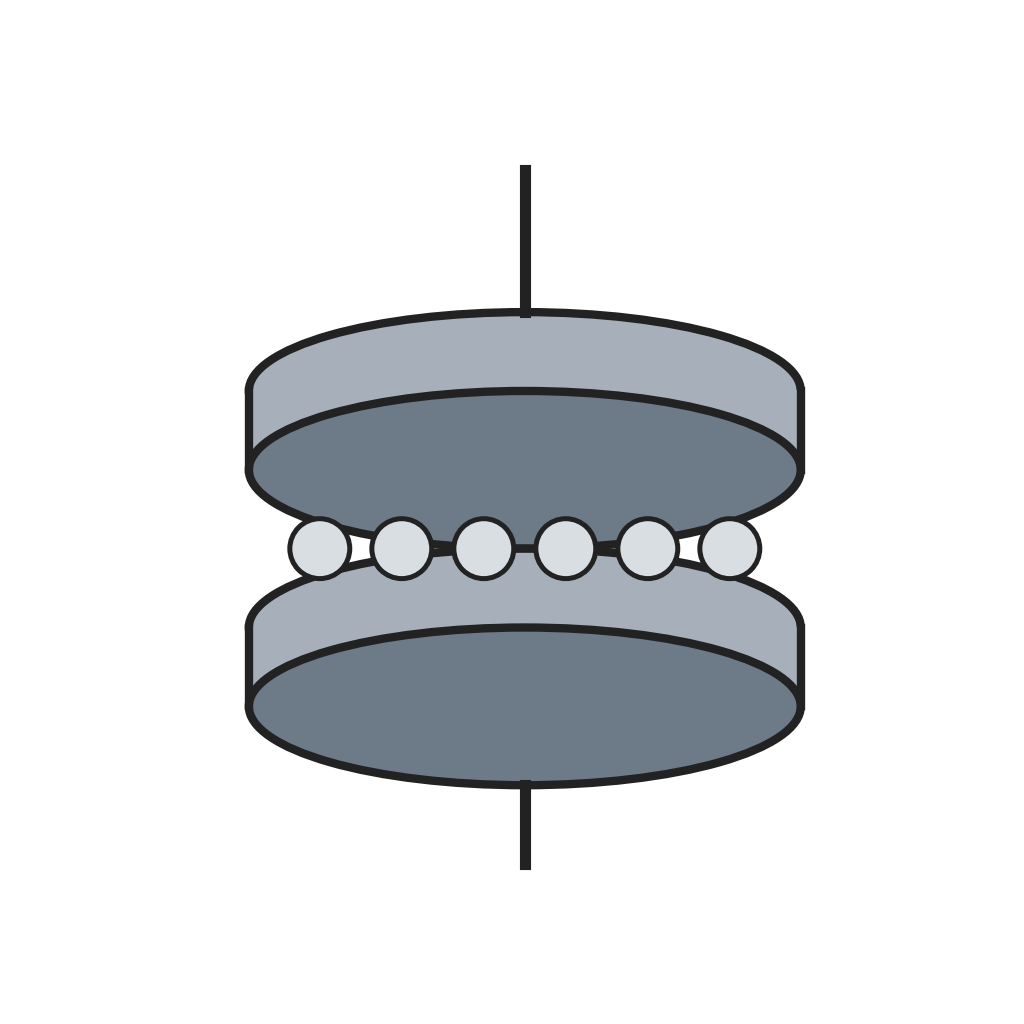 볼 버 제거기
6
6
Harden, grind and lap the balls
Harden, grind and lap the balls
Heat treat and temper the balls like the races. Grind them in the same kind of disc machine with grinding wheels to within a few ten-thousandths of an inch, then lap them 8–10 hours on cast-iron wheels with lapping compound.
이 단계의 재료:
래핑 컴파운드1 as required필요한 도구:
유랭 연속 담금질로뜨임로 볼 연삭기
 볼 래핑기
7
7
Stamp the cage
Stamp the cage
Stamp the cage halves from thin steel sheet and bend them to shape in a die. (Plastic cages are injection moulded instead.)
이 단계의 재료:
 강판1 as required
필요한 도구:
 스탬핑 프레스
8
8
Assemble
Assemble
Put the inner race inside the outer race, pushed as far to one side as it goes, and drop the balls into the gap opposite. Centre the races and spread the balls evenly, fit the cage (steel cages riveted, plastic ones snapped in) and coat the bearing with rust preventive.
이 단계의 재료:
 강철 리벳1 as required
 방청제1 as required
재료
6- 1 as required플레이스홀더
- 2 as required플레이스홀더
- 1 as required플레이스홀더
- 1 as required플레이스홀더
- 1 as required플레이스홀더
- 1 as required플레이스홀더
이 블루프린트로 만드는 것
관련 블루프린트
이 블루프린트들은 지식을 공유합니다 — 기술, 재료 또는 원리
CC0 퍼블릭 도메인
이 블루프린트는 CC0로 공개되었습니다. 어떤 목적으로든 자유롭게 복사, 수정, 배포 및 사용할 수 있습니다.
제품 구매를 통해 메이커를 지원하세요. 판매자가 설정한 메이커 커미션 을 받거나, 이 블루프린트의 새로운 반복을 만들어 연결로 포함시킬 수 있습니다.