예술
뷰티 및 웰니스
공예
문화 및 역사
엔터테인먼트
환경
음식 및 음료
역공학
과학
스포츠
기술
웨어러블
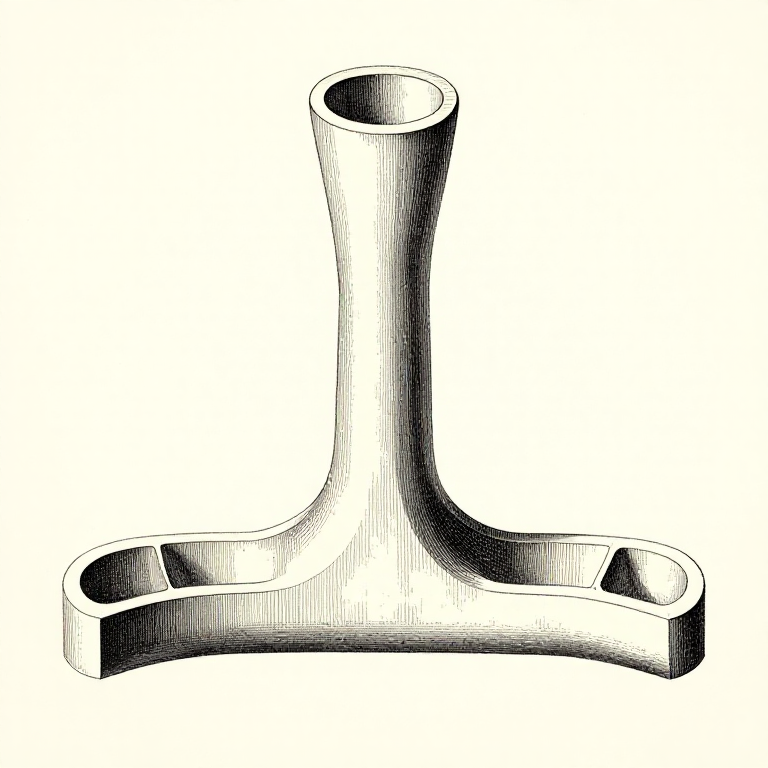


Gating: Getting the Metal In Without Wrecking the Mould
Molten metal poured straight into a cavity arrives fast, turbulent and full of air. It washes sand off the mould walls, folds oxide skin into itself, and the casting is full of inclusions before it has even frozen.
The GATING SYSTEM exists to prevent that. A sprue to take the metal down, a runner to carry it sideways and slow it, and gates to let it into the cavity smoothly — each part doing one job.
The governing principle is that the system should fill and stay full. A gating system running only partly full drags air in with the metal, which is precisely what it was built to avoid.
고급
3 hours
안내
1
1
Sprue, runner, gate — three parts, three jobs
Sprue, runner, gate — three parts, three jobs
The SPRUE is the vertical channel the metal is poured into. It should be TAPERED, wider at the top, because falling metal accelerates and narrows — a parallel sprue leaves a gap around the stream that sucks in air.
The RUNNER is the horizontal channel at the bottom. It distributes metal and slows it down, and it is usually in the drag with the gates in the cope so that any floating dross stays in the runner.
The GATES are the small openings from runner into cavity. Several small gates fill more gently than one large one and let the mould fill from more than one place, which matters on anything long or thin.
이 단계의 재료:
 주물사1 kg
필요한 도구:
 주형틀(상형과 하형)
 자
 디지털 캘리퍼스 6인치
2
2
Choke the system, and where
Choke the system, and where
Jupyter 노트북 불러오는 중…
이 단계의 재료:
 청동 주괴1 개주물사1 kg
필요한 도구:
 데스크톱 컴퓨터디지털 캘리퍼스 6인치주형틀(상형과 하형)
3
3
Traps, filters and a pouring basin
Traps, filters and a pouring basin
A POURING BASIN at the top of the sprue lets you fill it and keep it full, so the sprue never runs empty mid-pour. Pouring straight into a bare sprue hole guarantees an interrupted, air-entraining stream at the start.
A runner extension beyond the last gate — a DIRT TRAP — gives the first, dirtiest metal somewhere to go that is not the casting. It costs a few centimetres of runner and catches the slag that came down the sprue first.
Ceramic foam FILTERS do the same job far better and are cheap. They also slow and smooth the flow, which is why a filter often improves a casting for two reasons at once.
이 단계의 재료:
주물사1 kg필요한 도구:
주형틀(상형과 하형)자 고운 그물 뜰채
4
4
Pour steadily and keep the basin full
Pour steadily and keep the basin full
Start the pour and bring the basin up to full quickly, then hold it there until the mould is full. A pour that starts timidly and then speeds up entrains air at the very start, which is the metal that ends up deepest in the casting.
Never stop and restart. A pause lets the stream break, lets air in, and can leave a COLD SHUT where the metal that stopped has skinned over before the rest arrives.
Have enough metal melted before you start. Running out halfway is the single most avoidable failure in a foundry, and it is prevented by weighing the pattern, multiplying by the alloy's density ratio, and adding a generous allowance for the gating and risers — which is usually a third of the total again.
이 단계의 재료:
청동 주괴1 개 덩어리 숯1 개
필요한 도구:
 주조용 국자
 도가니 집게
 단조용 차광 고글
 긴 소매 가죽 장갑
관련 블루프린트
이 블루프린트들은 지식을 공유합니다 — 기술, 재료 또는 원리


CC0 퍼블릭 도메인
이 블루프린트는 CC0로 공개되었습니다. 어떤 목적으로든 자유롭게 복사, 수정, 배포 및 사용할 수 있습니다.
제품 구매를 통해 메이커를 지원하세요. 판매자가 설정한 메이커 커미션 을 받거나, 이 블루프린트의 새로운 반복을 만들어 연결로 포함시킬 수 있습니다.