예술
뷰티 및 웰니스
공예
문화 및 역사
엔터테인먼트
환경
음식 및 음료
역공학
과학
스포츠
기술
웨어러블

Speeds, Feeds, and What the Chip Is Telling You
Every cutting tool has a speed at which it works and a speed at which it dies, and the difference between them is often a factor of two. Run high-speed steel at carbide speeds and it will be blunt in seconds; run carbide at high-speed-steel speeds and it will chip because it never gets hot enough to cut properly.
The number that matters is not the spindle's revolutions but the SURFACE SPEED — how fast the metal passes the cutting edge. That depends on diameter, so the same tool on the same machine needs a different spindle speed for every size of work, and a part whose diameter changes needs the speed changed with it.
The arithmetic is one formula. The judgement is reading the chip, which tells you what is really happening at the edge where you cannot see.
중급
3 hours
안내
1
1
One formula, and the reason it has a diameter in it
One formula, and the reason it has a diameter in it
Jupyter 노트북 불러오는 중…
필요한 도구:
 금속 선반
 계산기
 공책
2
2
Feed decides the finish, not depth of cut
Feed decides the finish, not depth of cut
Jupyter 노트북 불러오는 중…
필요한 도구:
금속 선반계산기3
3
Read the chip
Read the chip
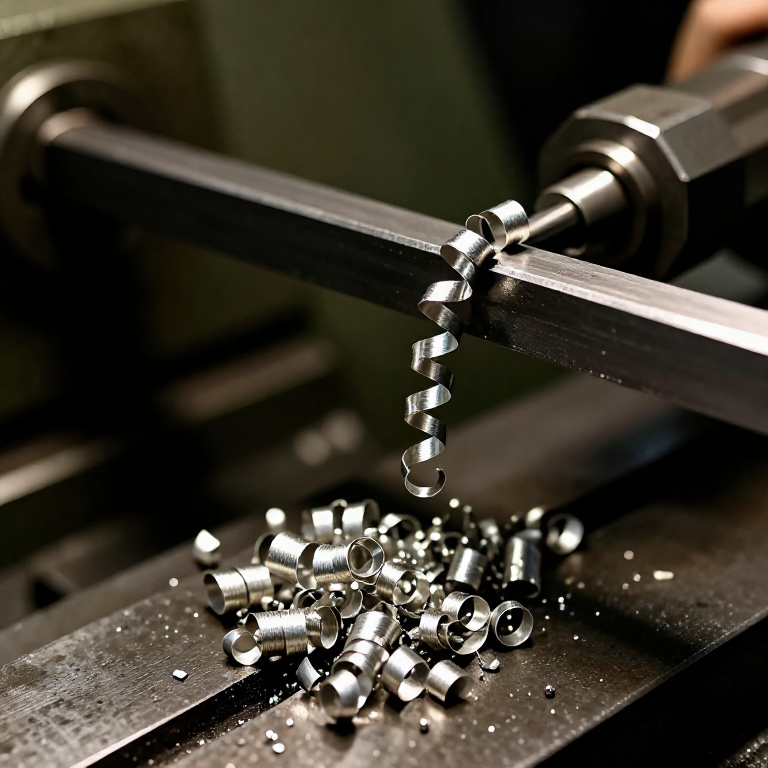
Stop and look at what is coming off. The chip is the only direct report you get from the cutting edge, and it is unambiguous once you know the vocabulary.
SHORT TIGHT CURLS, warm and silver-grey: correct. LONG STRINGY RIBBONS that wrap the work: feed too light or no chipbreaker, and dangerous — they are razor-sharp and they will grab. DARK BLUE OR STRAW chips: the cut is running hot, speed too high for the tool, and on HSS you are minutes from a blunt edge. DUST rather than chips on steel: the tool is already blunt and rubbing.
A chip that changes colour part way through a job is telling you the tool is wearing, not that the metal changed. Listen too: a steady hiss is a cut, a rhythmic chatter is the tool or work springing and needs less stick-out, a slower speed or a smaller nose radius.
이 단계의 재료:
 연강 환봉1 개
필요한 도구:
금속 선반 선반 공구 세트 (HSS)
 보안경공책
4
4
Cutting fluid, and when it does harm
Cutting fluid, and when it does harm
Flood steel generously with cutting oil. It cools the edge, floats the chip out of the cut and stops material welding to the tool, and it buys a large multiple of tool life on stainless in particular.
Cast iron is cut DRY. Its graphite lubricates the cut by itself, and fluid turns the fine dusty swarf into an abrasive paste that gets into the slideways and wears the machine.
The one rule that matters with carbide: apply fluid steadily or not at all. An intermittent squirt onto a hot carbide tip thermally shocks it and cracks the edge, and a cracked tip fails suddenly rather than gradually. Aluminium wants something to stop it welding to the tool — paraffin or a dedicated aluminium cut fluid works where general cutting oil is indifferent.
이 단계의 재료:
 절삭유1 개
필요한 도구:
금속 선반선반 공구 세트 (HSS)5
5
Write down what worked
Write down what worked
Keep a page per material: tool, diameter, spindle speed, feed, depth of cut, and one word about the chip and the finish. It takes fifteen seconds at the end of a job.
Published cutting-speed tables are a STARTING POINT computed for industrial machines with rigid setups and plenty of power. A small lathe on a bench will often chatter at the book figure and be perfectly happy at two thirds of it. What you actually want is a table for YOUR machine.
After a dozen jobs you will stop calculating for the common cases, which is the point: the formula is how you handle the unfamiliar material, and the notebook is how you stop re-deriving the familiar ones.
필요한 도구:
공책계산기관련 블루프린트
이 블루프린트들은 지식을 공유합니다 — 기술, 재료 또는 원리



CC0 퍼블릭 도메인
이 블루프린트는 CC0로 공개되었습니다. 어떤 목적으로든 자유롭게 복사, 수정, 배포 및 사용할 수 있습니다.
제품 구매를 통해 메이커를 지원하세요. 판매자가 설정한 메이커 커미션 을 받거나, 이 블루프린트의 새로운 반복을 만들어 연결로 포함시킬 수 있습니다.