ศิลปะ
ความงามและสุขภาพ
งานฝีมือ
วัฒนธรรมและประวัติศาสตร์
ความบันเทิง
สิ่งแวดล้อม
อาหารและเครื่องดื่ม
วิศวกรรมย้อนรอย
วิทยาศาสตร์
กีฬา
เทคโนโลยี
อุปกรณ์สวมใส่
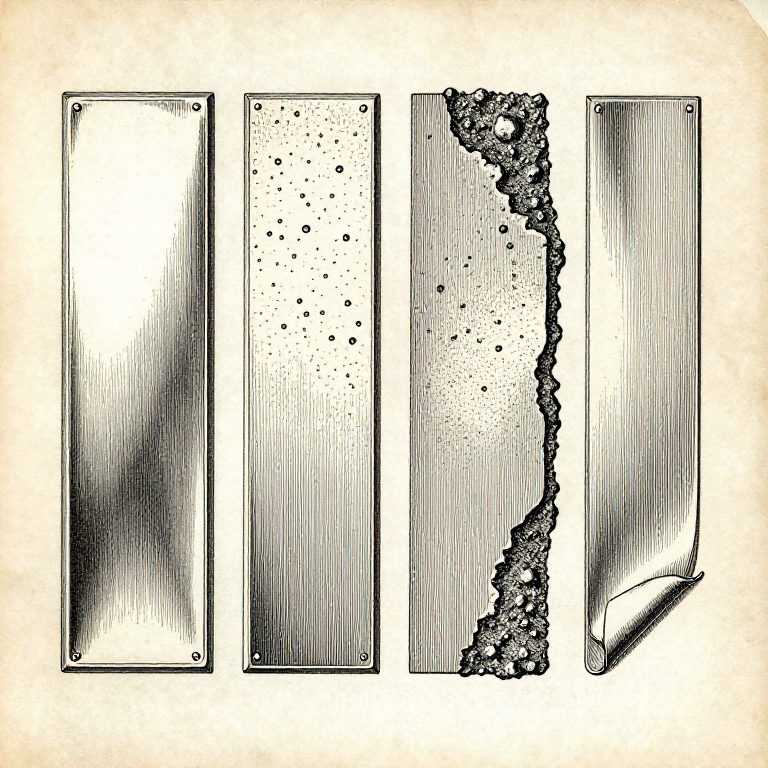

Reading a Plating Fault: Burnt, Pitted, Dull, Peeling
Plating faults have distinct appearances, and each one points at a short list of causes. The diagnosis is quicker than the repair, and it is what stops the same batch being ruined twice.
The first question is always **where** the fault is. A fault at the edges is a current density problem. A fault in a recess is a throwing power problem. A fault in a patch with a defined shape is contamination — and the shape usually says what it was.
A fault over the whole part is the bath.
ระดับกลาง
2 hours
คำแนะนำ
1
1
Burning, and roughness
Burning, and roughness
**Burning** is a dark grey, rough, powdery deposit with poor adhesion, always worst at edges, corners and points. It is a dendritic growth: the deposit has grown faster than ions can arrive, so it has branched out into the solution rather than filling in.
*Causes, in order:* current density too high — either the current was set too high or the area was underestimated; too little agitation; the bath too cold; the metal concentration too low.
*The fix at the edges specifically:* a thief, a shield, or a lower current. The racking rung covers these.
**Roughness** is different — gritty or nodular over the whole surface, with good adhesion. It is particles in the bath being plated over.
*Causes:* particles falling from the anodes, which is why anodes go in bags; precipitated basic salts from a pH that drifted high; dust; filter failure.
*The fix:* filter the bath continuously, bag the anodes, check the pH.
**The two are told apart by adhesion and by location.** Burning is at the extremities and lifts; roughness is everywhere and sticks.
วัสดุสำหรับขั้นตอนนี้:
 แผ่นเหล็กกล้าละมุน2 ชิ้น
 นิกเกิลซัลเฟตเฮกซะไฮเดรต1 ชิ้น
เครื่องมือที่ต้องใช้:
 กล้องส่องขยาย
 มัลติมิเตอร์ดิจิทัล — เลือกย่านอัตโนมัติ ค่า RMS แท้
2
2
Pitting, and why hydrogen causes it
Pitting, and why hydrogen causes it
**Pitting** is small round holes or craters in the deposit, often in trails running upwards, and it has one dominant cause: **a hydrogen bubble stuck to the surface**. Where a bubble sits, no metal deposits, and the deposit grows around it into a pit.
The trails happen because the bubble slides upwards as it grows.
*Causes and fixes:*
**Poor wetting** — the commonest. A wetting agent in the bath lowers the surface tension so bubbles release instead of clinging. Its exhaustion is the usual reason a bath starts pitting after months of working.
**Too little agitation** — bubbles are not swept away.
**Organic contamination** — oil in the bath, often from a part that was not properly degreased, stabilises the bubbles. Carbon treatment removes it.
**Low current efficiency** — more hydrogen produced in the first place, which is why chrome pits so readily.
**A horizontal surface facing upwards pits worst**, because bubbles settle on it. Rotating or tilting the work during plating is a genuine fix and costs nothing.
วัสดุสำหรับขั้นตอนนี้:
แผ่นเหล็กกล้าละมุน2 ชิ้นเครื่องมือที่ต้องใช้:
กล้องส่องขยาย เตาให้ความร้อนพร้อมเครื่องกวนแม่เหล็ก
3
3
Dullness, cloudiness and staining
Dullness, cloudiness and staining
**Dullness where brightness was expected.** The brightener is exhausted, the current density is below the bright range, the temperature is wrong, or the substrate was not polished — a bright bath does not make a dull surface bright unless it is a levelling bath, and even then only up to a point.
**Cloudiness or haze**, especially in low current density areas. Usually organic contamination, and carbon treatment is the answer.
**A milky or smutty grey film** that wipes off. Often a metallic contaminant co-depositing — zinc in a nickel bath, for instance. Dummy plating at low current density for several hours removes it onto a scrap cathode.
**Staining after drying.** Solution not rinsed out, or a hole that weeped after the part was dry, or tap water in the last rinse.
**A rainbow or iridescent sheen on zinc** is the passivation film and is normal — that one is a feature.
**Brown or black streaks running down from a hole** are trapped solution finding its way out after plating. Blow the holes out before drying.
วัสดุสำหรับขั้นตอนนี้:
นิกเกิลซัลเฟตเฮกซะไฮเดรต1 ชิ้น น้ำกลั่น1 ชิ้น
เครื่องมือที่ต้องใช้:
กล้องส่องขยาย บีกเกอร์โบโรซิลิเกต
4
4
The diagnostic sequence, and the log
The diagnostic sequence, and the log
**Start with where.** Edges and points say current density. Recesses and blind areas say throwing power. A patch with a shape — a thumb print, a run mark, a line where the solution level sat — says contamination or handling. Everywhere at once says the bath.
**Then ask when it started.** A fault that appeared suddenly between two otherwise identical runs points at a single change: a new bottle of something, a topped-up bath, a different part, a colder day. A fault that has crept in over weeks points at consumption — brightener, wetting agent, anode area.
**Then run a Hull cell.** One small panel shows the whole current density range at once: where it burns, where it goes dull, where it is bright. It is the single most informative half hour available, and it uses a few hundred millilitres.
**Then treat in the standard order:** filter, carbon treat for organics, dummy plate for metallics, correct the pH, correct the temperature, and only then add brightener. Adding brightener first is the usual instinct and it usually makes things worse, because the additive is rarely the cause.
**Keep the log.** Date, part, area, current, time, temperature, pH, weight gain, and what the deposit looked like. Every diagnosis above is a comparison against a previous run, and without the log there is nothing to compare with.
วัสดุสำหรับขั้นตอนนี้:
 ชุดชุบโลหะด้วยไฟฟ้า (นิกเกิล)1 ชิ้น
เครื่องมือที่ต้องใช้:
 แหล่งจ่ายไฟตั้งโต๊ะปรับค่าได้มัลติมิเตอร์ดิจิทัล — เลือกย่านอัตโนมัติ ค่า RMS แท้
 เทอร์โมมิเตอร์ห้องปฏิบัติการ
วัสดุ
4- 2 ชิ้นตัวยึดตำแหน่ง
- 1 ชิ้นตัวยึดตำแหน่ง
- 1 ชิ้นตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
เครื่องมือที่จำเป็น
6- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
บลูพริ้นท์ที่เกี่ยวข้อง
บลูพริ้นท์เหล่านี้แบ่งปันความรู้ — เทคนิค วัสดุ หรือหลักการ

CC0 สาธารณสมบัติ
พิมพ์เขียวนี้เผยแพร่ภายใต้ CC0 คุณสามารถคัดลอก แก้ไข แจกจ่าย และใช้งานผลงานนี้เพื่อวัตถุประสงค์ใดก็ได้ โดยไม่ต้องขออนุญาต
สนับสนุนเมกเกอร์โดยซื้อสินค้าผ่านพิมพ์เขียวของพวกเขา ซึ่งพวกเขาจะได้รับ ค่าคอมมิชชันเมกเกอร์ ที่ผู้ขายกำหนด หรือสร้างเวอร์ชันใหม่ของพิมพ์เขียวนี้และรวมเป็นการเชื่อมต่อในพิมพ์เขียวของคุณเพื่อแบ่งรายได้