УРЛАГ
ГОО САЙХАН БА ЭРҮҮЛ МЭНД
ГАРААР ХИЙСЭН
СОЁЛ БА ТҮҮХ
ҮЗВЭР НААДАМ
БАЙГАЛЬ ОРЧИН
ХООЛ БА УНДАА
УРВУУ ИНЖЕНЕРЧЛЭЛ
ШИНЖЛЭХ УХААН
СПОРТ
ТЕХНОЛОГИ
ӨМСДӨГ ХЭРЭГСЭЛ
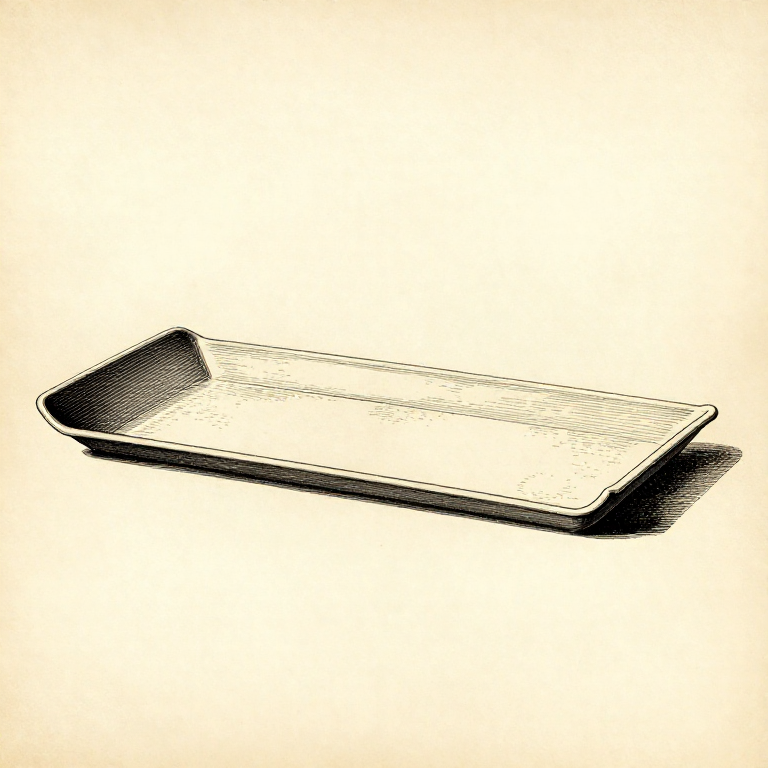


Warping: Why Big Flat Parts Lift at the Corners
Plastic goes down hot and shrinks as it cools. Each new layer shrinks onto the layers below, which have already cooled and cannot follow — so every layer pulls inward on the one beneath it.
Near the middle of a part those pulls cancel. At a corner they do not, and the corner lifts off the plate. That is warping, and it is why it always starts at corners and always on long flat parts.
The cure is not more adhesive. It is keeping the whole part near one temperature so the shrinkage happens evenly — which is what a heated bed does, what an enclosure does, and what choosing PLA over ABS does.
Дунд шат
3 hours
Зааварчилгаа
1
1
Material first: some plastics barely warp
Material first: some plastics barely warp
PLA shrinks very little and warps very little. ABS shrinks several times as much and will warp off an open printer almost regardless of what else you do. PETG and ASA sit between them.
So the first question about a warping part is whether it needs to be in that material at all. A prototype that only has to hold a shape is a PLA part; ABS is chosen for heat resistance or solvent smoothing, and then the warping is a cost accepted in exchange.
Wet filament makes everything worse. Moisture absorbed from the air turns to steam at the nozzle, which gives poor layer welds and a rough surface — and a part with weak layers warps more because the layers cannot hold each other. A filament dryer is not an accessory for hygroscopic materials, it is required.
Энэ алхмын материал:
 3D хэвлэлийн утас (PLA)1 ширхэг
 ABS утас1 ширхэг
 ASA утас1 ширхэг
Шаардлагатай багаж:
 Утас хатаагч
 FDM 3D хэвлэгч
2
2
Keep the part hot: bed, enclosure, no draughts
Keep the part hot: bed, enclosure, no draughts
A heated bed keeps the lower layers above the temperature where the plastic goes rigid, so they can still move as the upper ones shrink. That is why bed temperature matters far beyond the first layer.
An ENCLOSURE does the same for the whole part. It is the single most effective measure for ABS and ASA, and it costs nothing to test — a cardboard box over the printer will tell you in one print whether it is the answer.
And stop the draughts. A printer near an open window or a door will produce a part that warps on one side only, which is a genuinely confusing fault until the cause is noticed. Turning the cooling fan DOWN for ABS is the same idea applied deliberately.
Энэ алхмын материал:
ABS утас1 ширхэгШаардлагатай багаж:
 3D хэвлэгчийн бүрхүүл (галд тэсвэртэй)FDM 3D хэвлэгч
 3D хэвлэгчийн хэвлэх хавтан (PEI бүрсэн пүрш ган)
3
3
Design the corners away
Design the corners away
Warping concentrates at sharp corners, so round them. A 5 mm radius on the corners of a large flat part removes most of the stress concentration and often fixes warping on its own — at no cost in material or time.
MOUSE EARS are the crude version: small thin discs added at each corner that spread the adhesion, printed as part of the model and snapped off afterwards. They are ugly and they work.
A BRIM does the same thing all the way round: a flat skirt of extra first layer attached to the part. A RAFT goes further and prints the whole part on a sacrificial platform, which helps adhesion but adds a rough bottom face — so a brim is usually the better trade.
Энэ алхмын материал:
3D хэвлэлийн утас (PLA)1 ширхэгШаардлагатай багаж:
 3MF файлын зүсэгч программ
 Ширээний компьютер
 Ирмэг цэвэрлэх багаж
4
4
Reduce the area that can pull
Reduce the area that can pull
A long flat part warps because there is a long flat run of cooling plastic pulling on itself. Break that up and the force has nowhere to accumulate.
Splitting a big part into two printed pieces and joining them removes the problem entirely, and often prints faster because both halves can be oriented better. Cutting large windows or lightening holes into a flat panel does the same thing for the same reason.
Lower infill also helps, because there is less material contracting. That is a real trade against strength, and it is the next rung — but it is worth knowing that a warping part and an over-infilled part are often the same part.
Энэ алхмын материал:
3D хэвлэлийн утас (PLA)1 ширхэгШаардлагатай багаж:
3MF файлын зүсэгч программШирээний компьютер Дижитал штангенциркуль 6 инч
Материал
3- 3 ширхэгТүр орлуулагч
- 2 ширхэгТүр орлуулагч
- 1 ширхэгТүр орлуулагч
Шаардлагатай багаж
8- Утас хатаагч10% комиссТүр орлуулагч
- Түр орлуулагч
- 3D хэвлэгчийн бүрхүүл (галд тэсвэртэй)10% комиссТүр орлуулагч
- Түр орлуулагч
- Түр орлуулагч
- Түр орлуулагч
- Түр орлуулагч
- Түр орлуулагч
Холбоотой загварууд
Эдгээр загварууд мэдлэг хуваалцдаг — арга техник, материал эсвэл зарчим


CC0 Нийтийн домэйн
Энэ загвар CC0 дор гаргагдсан. Та зөвшөөрөл авахгүйгээр хуулах, өөрчлөх, түгээх, ашиглах боломжтой.
Загвараар дамжуулан бүтээгдэхүүн худалдаж авч Бүтээгчийг дэмжээрэй Бүтээгчийн шимтгэл Борлуулагчаар тогтоосон, эсвэл энэ загварын шинэ хувилбар үүсгэж орлогоо хуваахын тулд өөрийн загварт холбоос болгон оруулна уу.