IṢẸ́ ỌNÀ
ẸWÀ ÀTI ÌLERA
IṢẸ́ ỌWỌ́
ÀṢÀ ÀTI ÌTÀN
ÌṢERÉ
ÀYÍKÁ
OÚNJẸ ÀTI OHUN MÍMU
REVERSE ENGINEERING
SÁYẸ́ǸSÌ
ERÉ ÌDÁRAYÁ
ÌMỌ̀-Ẹ̀RỌ
ÀWỌN OHUN WÍWỌ̀


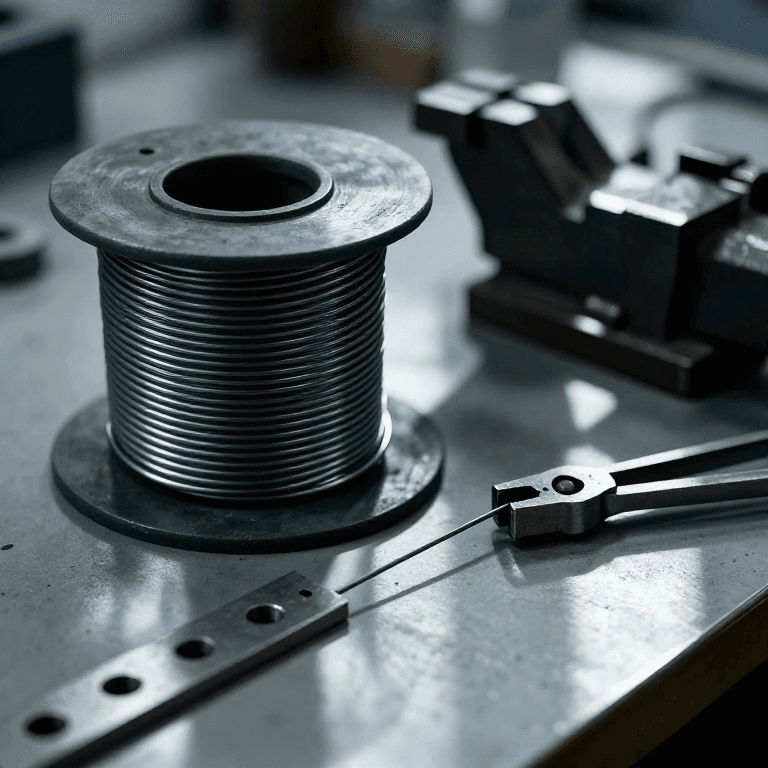
Bearing Steel Wire (52100): Drawn from Bar Through a Drawplate
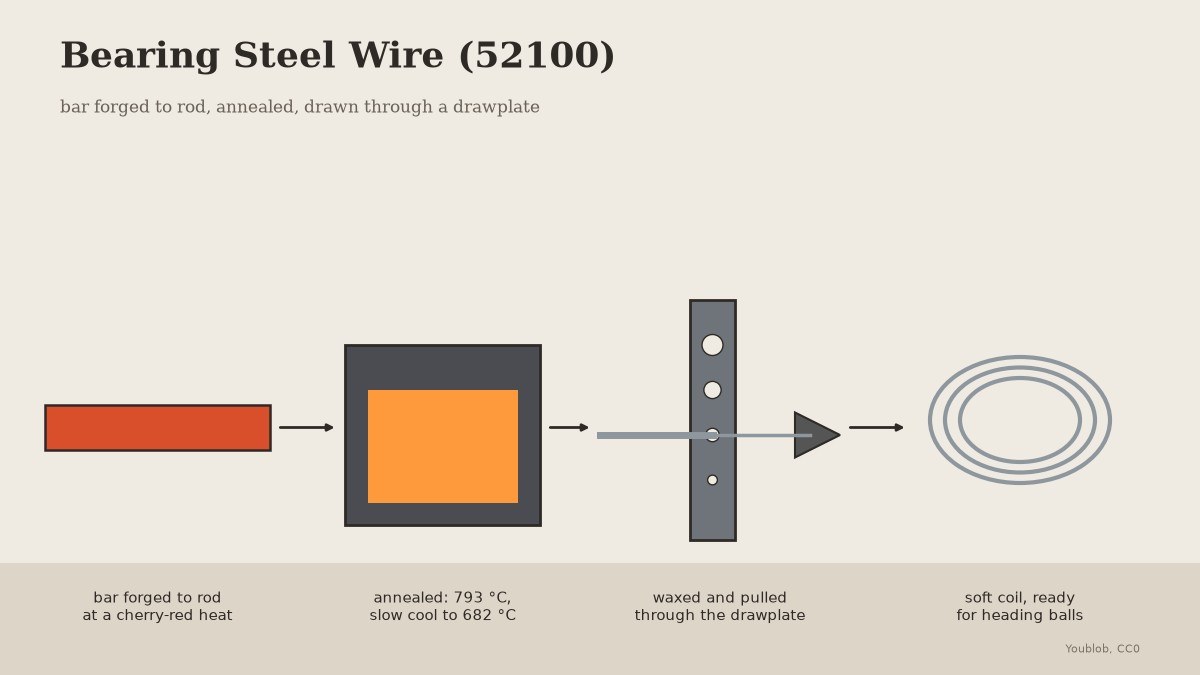
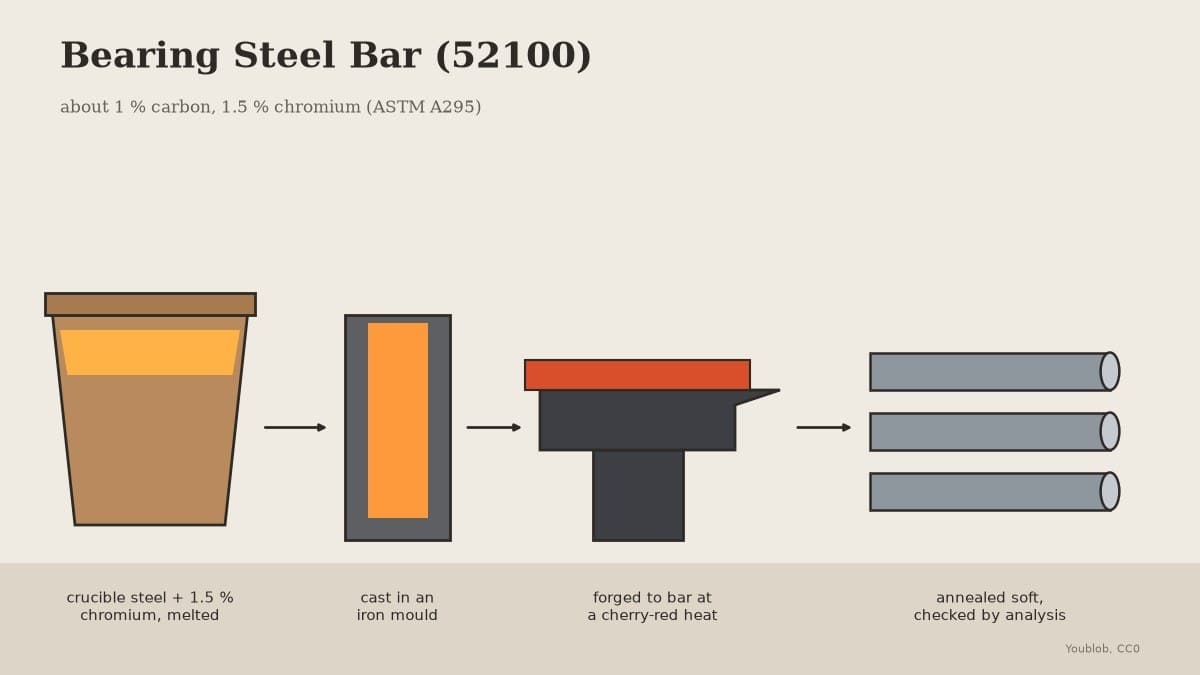
Bearing balls are headed from thick wire of 52100 steel. Here 52100 bar is forged to rod and drawn through a drawplate. At 1 % carbon it is much harder than mild steel, so it is annealed soft before drawing and again after every two holes, using the 52100 anneal Verhoeven recommends.
The picture: our drawing, bar to coil.
Ilọsíwájú
2 days
Ìlànà
1
1
Forge to rod
Forge to rod
Heat the bar to a cherry-red heat and no hotter, and draw it out round on the anvil to a rod a little thicker than the drawplate's largest hole.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Ọ̀pá irin bearing (52100)1 kg
 Èédú1 as required
Àwọn irinṣẹ́ tí a nílò:
 Ìléru alágbẹ̀dẹ
 Ìdí Alágbẹ̀dẹ
 Òòlù olórí ìtẹ̀ ìpakà
 Ẹmú alágbẹ̀dẹ
 Ìbọ̀wọ́ wẹ́lídìn
 Gíláàsì ààbò
2
2
Anneal
Anneal
In the oven, hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
Àwọn irinṣẹ́ tí a nílò:
 Ààrò ìtọ́jú ooru
 Thermocouple pẹ̀lú ìkàẸmú alágbẹ̀dẹÌbọ̀wọ́ wẹ́lídìn
3
3
Clean and taper
Clean and taper
Brush off all the scale, then file a long taper on the first 3 cm so it passes the first hole.
Àwọn irinṣẹ́ tí a nílò:
 Ìṣètò búrọ́ọ̀ṣì okùn
 Àkójọ Ìfá
 Ìdìmú Tábìlì
4
4
Wax and draw
Wax and draw
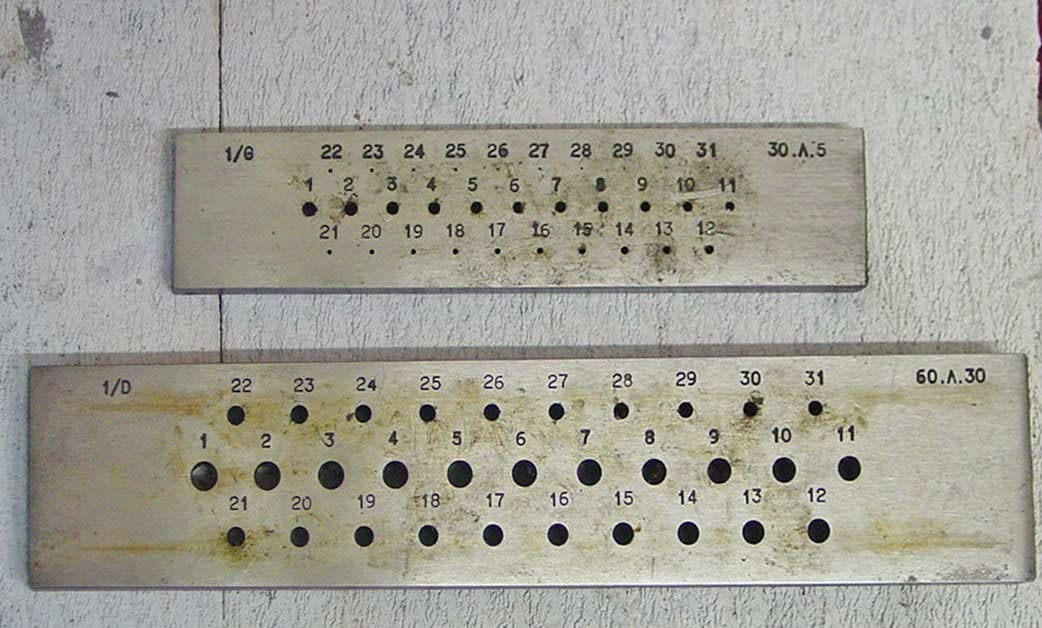
Clamp the drawplate in the vise. Wax the rod, push the taper through the first hole it does not slip through, and pull straight out with the draw tongs in one steady pull.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Ìdí Oyin20 g
Àwọn irinṣẹ́ tí a nílò:
 Àwo ìfàokùn irin
 Ẹmú ìfàgùnÌdìmú Tábìlì
 Ìbọ̀wọ́ Iṣẹ́ Awọ
5
5
Anneal every two holes
Anneal every two holes
Draw through each next hole without skipping. After every two holes, coil the wire and anneal it again: hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Ìdí Oyin1 ẹyọÀwọn irinṣẹ́ tí a nílò:
Àwo ìfàokùn irinẸmú ìfàgùnÀàrò ìtọ́jú ooruThermocouple pẹ̀lú ìkà6
6
Finish soft
Finish soft
Stop at the diameter your balls need, checked with the caliper, and give the coil a last anneal so it is soft for heading.
Àwọn irinṣẹ́ tí a nílò:
 Òṣùwọ̀n Kálípà Díjítà Ìnṣì 6Ààrò ìtọ́jú ooruThermocouple pẹ̀lú ìkà
7
7
Troubleshooting
Troubleshooting
Bearing steel wire troubleshooting.
Flow
Loading...
Àwọn irinṣẹ́ tó nílò
15- Àyè
- Àyè
- Àyè
- Àyè
Ìtọ́nisọ́nà yìí ń ṣe
Blueprint tó jọra
Àwọn blueprint wọ̀nyí pín ìmọ̀ — ọ̀nà, ohun-èlò tàbí ìlànà
CC0 Àgbègbè Gbogbogbò
Blueprint yìí ti jáde lábẹ́ CC0. O lè ṣe àdàkọ, yí padà, pín, àti lò láìsí ìyọ̀ǹda.
Ṣàtìlẹ́yìn Olùṣẹ́dá nípa rírà àwọn ọjà nipasẹ̀ Blueprint wọn Ẹ̀san Olùṣẹ́dá tí àwọn Olùtajà gbé kalẹ̀, tàbí ṣẹ̀dá àtúnṣe tuntun ti Blueprint yìí kí o sì fi sínú Blueprint rẹ gẹ́gẹ́ bí ìsopọ̀ láti pín owó-wíwọlé.