IṢẸ́ ỌNÀ
ẸWÀ ÀTI ÌLERA
IṢẸ́ ỌWỌ́
ÀṢÀ ÀTI ÌTÀN
ÌṢERÉ
ÀYÍKÁ
OÚNJẸ ÀTI OHUN MÍMU
REVERSE ENGINEERING
SÁYẸ́ǸSÌ
ERÉ ÌDÁRAYÁ
ÌMỌ̀-Ẹ̀RỌ
ÀWỌN OHUN WÍWỌ̀
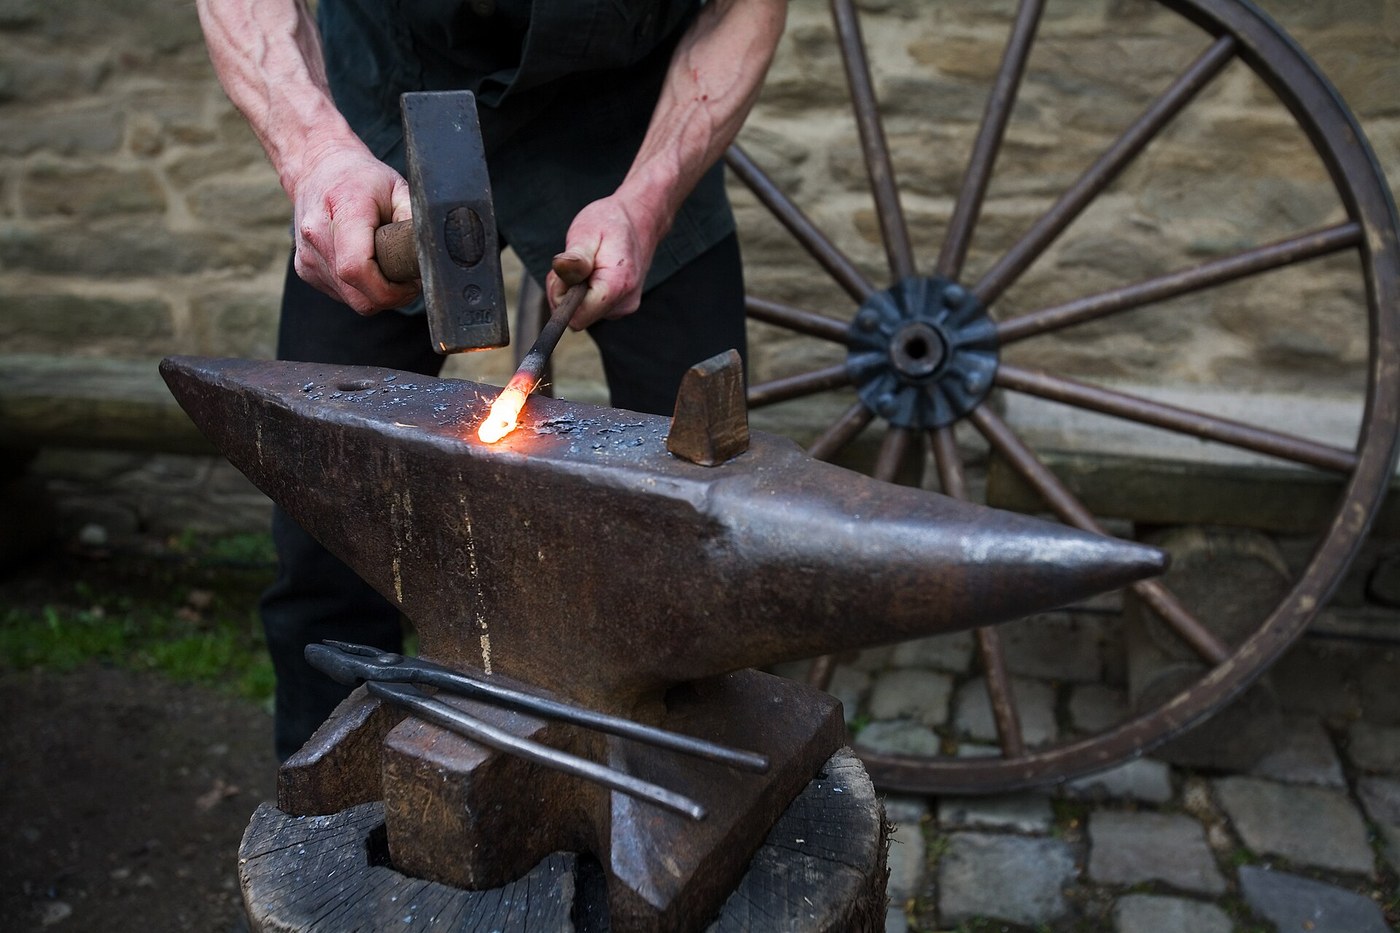


Smith's Top and Bottom Tools: Punch, Drift, Hardy, Fullers, Chisel and Swage
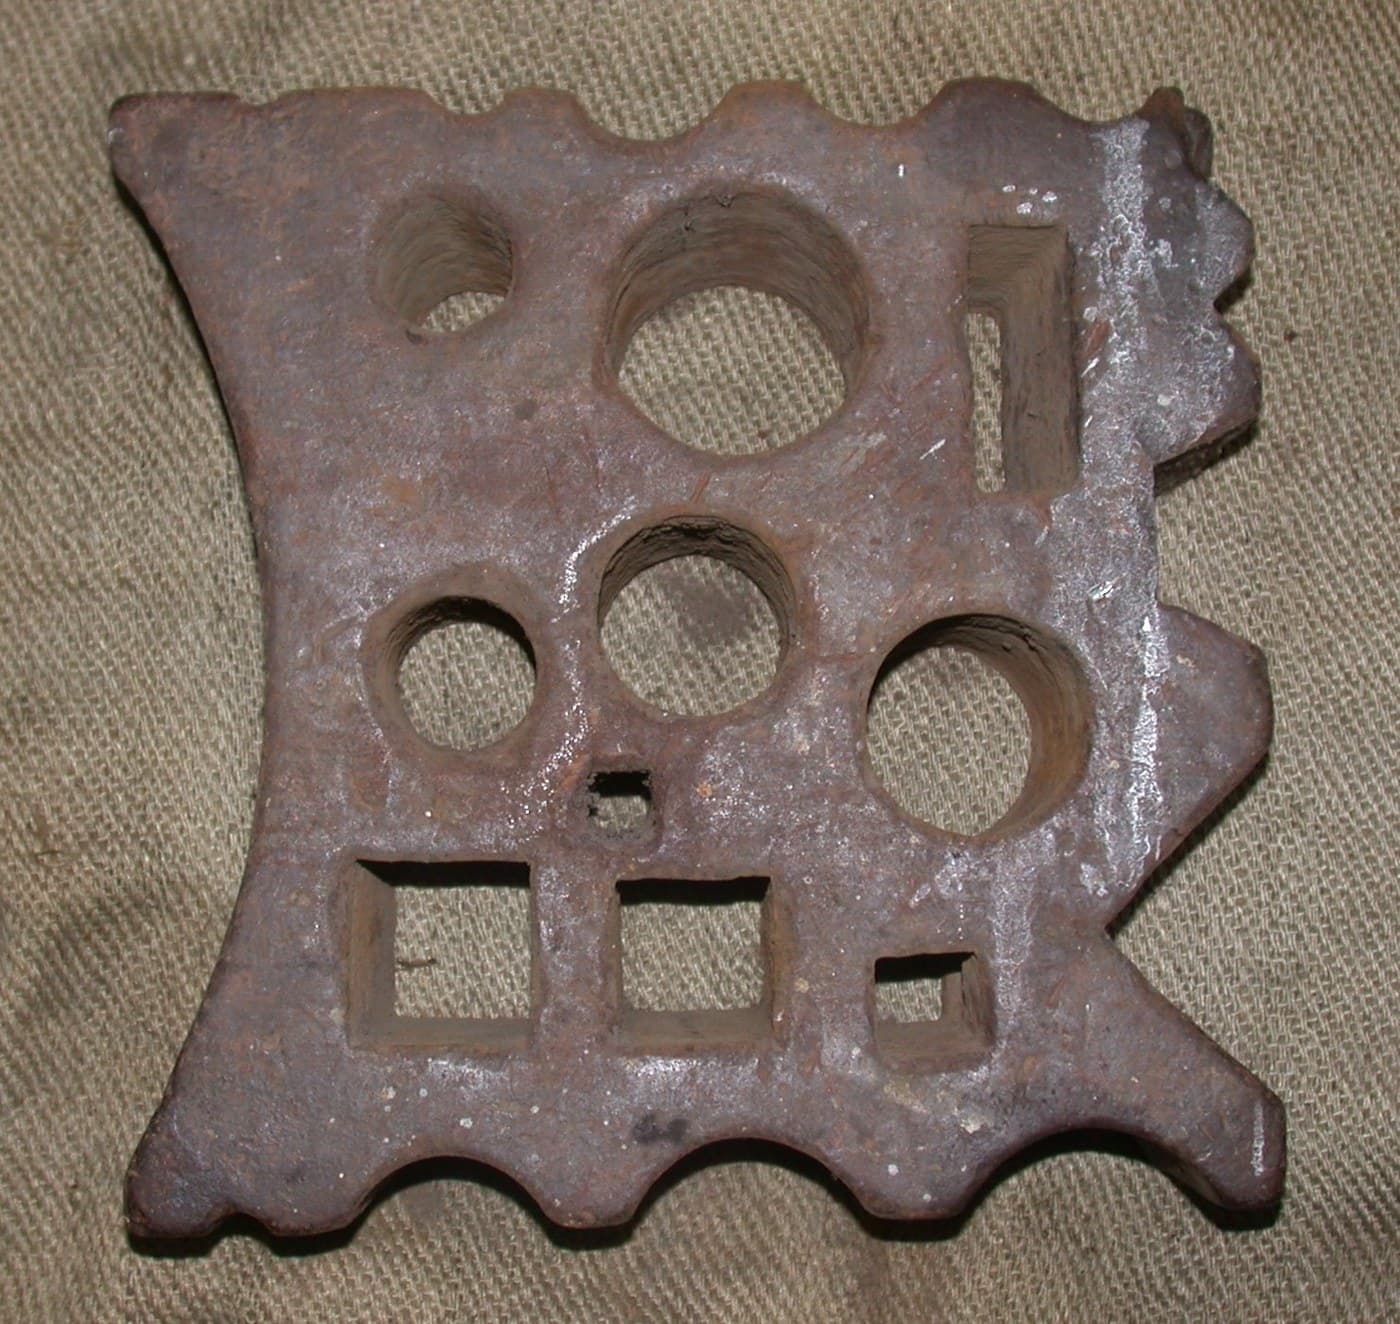
Bottom tools have a square shank that drops into the anvil's hardy hole; top tools have a handle and are held on the work and struck. The hardy cuts hot stock laid over it, the fuller's rounded nose spreads metal, the punch makes a hole and the drift opens it to size, the hot chisel cuts from above, and the bottom swage rounds bar in its groove. Forge them all from tool steel.
The picture: a smith at the anvil, a hardy standing in the hardy hole.
Ilọsíwájú
Two days
Ìlànà
1
1
Shanks for the hardy hole
Shanks for the hardy hole
For each bottom tool, forge a square shank that slips into the hardy hole without rocking, with a shoulder above it that sits on the anvil face.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Ọ̀pá onígun mẹ́jọ irin irinṣẹ́4 kg
 Èédú6 as required
Àwọn irinṣẹ́ tí a nílò:
 Ìléru alágbẹ̀dẹ
 Ìdí Alágbẹ̀dẹ
 Òòlù olórí ìtẹ̀ ìpakà
 Òòlù ńlá
 Ẹmú alágbẹ̀dẹ
 Ìbọ̀wọ́ wẹ́lídìn
 Gíláàsì ààbò
2
2
Hardy and bottom fuller
Hardy and bottom fuller
On one shanked blank forge a wedge with its edge upward: the hot cut hardy. On another, forge a rounded nose: the bottom fuller.
Àwọn irinṣẹ́ tí a nílò:
Ìléru alágbẹ̀dẹÌdí Alágbẹ̀dẹÒòlù olórí ìtẹ̀ ìpakàÒòlù ńláẸmú alágbẹ̀dẹÌbọ̀wọ́ wẹ́lídìnGíláàsì ààbò3
3
Bottom swage
Bottom swage
On a third shanked blank, form a half-round groove by forging a hot bar of the size you want into it with the top swage, then file it clean.
Àwọn irinṣẹ́ tí a nílò:
Ìléru alágbẹ̀dẹÌdí Alágbẹ̀dẹÒòlù olórí ìtẹ̀ ìpakàÒòlù ńláẸmú alágbẹ̀dẹÌbọ̀wọ́ wẹ́lídìnGíláàsì ààbò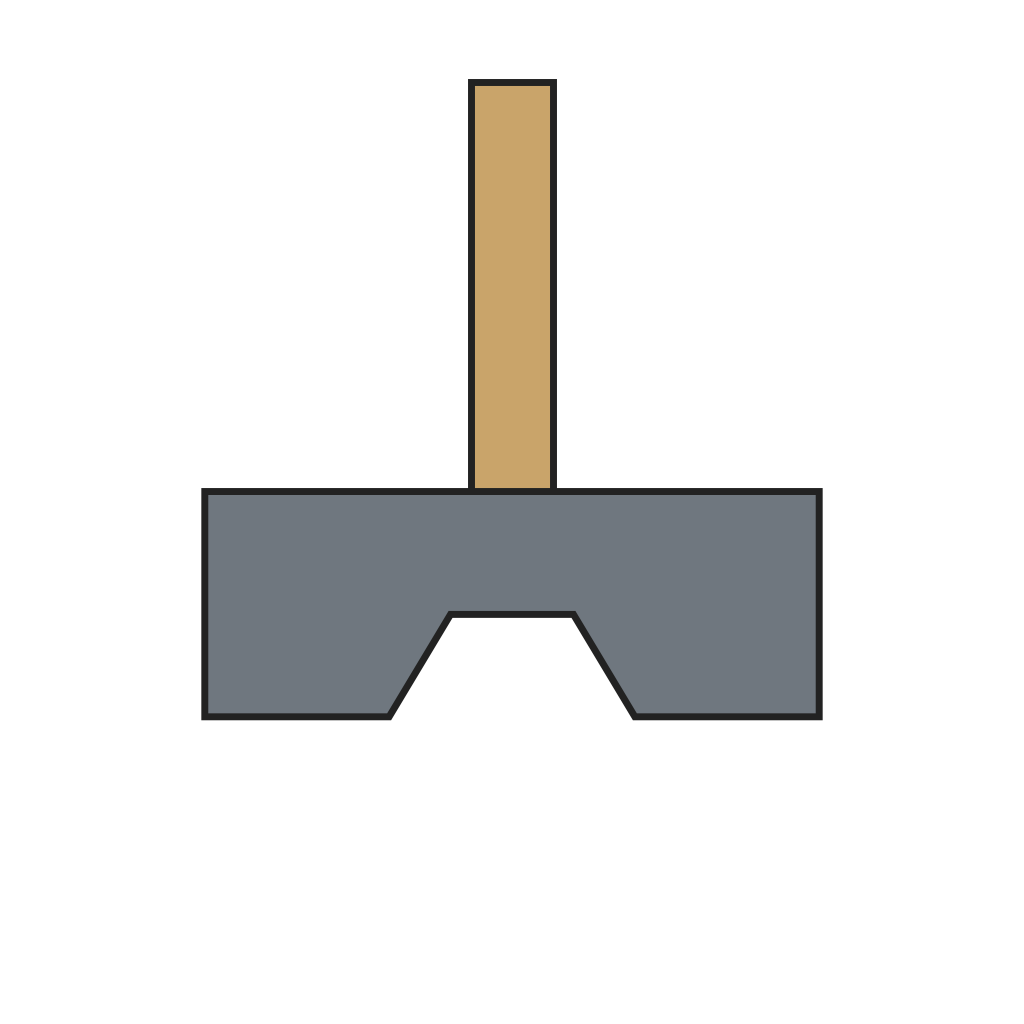 Àwòṣe òkè ìyíká
 Ìfá Irin
4
4
Top tools
Top tools
Forge the top tools from bar: a hot punch tapering to a small flat end, a drift tapering evenly to the size of the finished hole, a top fuller with a rounded nose, and a hot chisel with a thin edge. Leave a flat face on top of each to be struck.
Àwọn irinṣẹ́ tí a nílò:
Ìléru alágbẹ̀dẹÌdí Alágbẹ̀dẹÒòlù olórí ìtẹ̀ ìpakàÒòlù ńláẸmú alágbẹ̀dẹÌbọ̀wọ́ wẹ́lídìnGíláàsì ààbò5
5
Harden the edges and fit handles
Harden the edges and fit handles
Harden the hardy and hot chisel edges in water and temper them to blue; leave the punch, drift and fullers as forged, since they work hot (our practice). Fit ash handles to the hot chisel and top fuller.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Igi ash2 ẹyọ
 Omi10 lítà
Àwọn irinṣẹ́ tí a nílò:
Ìléru alágbẹ̀dẹ Àpótí ìtutù
 Òkúta ìpọ́n oníkẹ̀kẹ́Ẹmú alágbẹ̀dẹÌbọ̀wọ́ wẹ́lídìnGíláàsì ààbò
6
6
Steel for the set
Steel for the set
Ń ṣí ìwé Jupyter…
Àwọn ohun-èlò
4- 6 as requiredÀyè
- 2 ẹyọÀyè
- 10 lítàÀyè
Ìtọ́nisọ́nà yìí ń ṣe
Blueprint tó jọra
Àwọn blueprint wọ̀nyí pín ìmọ̀ — ọ̀nà, ohun-èlò tàbí ìlànà
CC0 Àgbègbè Gbogbogbò
Blueprint yìí ti jáde lábẹ́ CC0. O lè ṣe àdàkọ, yí padà, pín, àti lò láìsí ìyọ̀ǹda.
Ṣàtìlẹ́yìn Olùṣẹ́dá nípa rírà àwọn ọjà nipasẹ̀ Blueprint wọn Ẹ̀san Olùṣẹ́dá tí àwọn Olùtajà gbé kalẹ̀, tàbí ṣẹ̀dá àtúnṣe tuntun ti Blueprint yìí kí o sì fi sínú Blueprint rẹ gẹ́gẹ́ bí ìsopọ̀ láti pín owó-wíwọlé.