
SINING
BEAUTY AT WELLNESS
CRAFTS
KULTURA AT KASAYSAYAN
LIBANGAN
KAPALIGIRAN
PAGKAIN AT INUMIN
REVERSE ENGINEERING
AGHAM
ISPORTS
TEKNOLOHIYA
MGA WEARABLE
Pouring Temperature: Too Cold Misruns, Too Hot Tears the Mould
Forge

Nilikha ni

Forge

24. Setyembre 2026NO
16
0
0
0
0

Pouring Temperature: Too Cold Misruns, Too Hot Tears the Mould

Metal is not poured at its melting point. It is poured at a SUPERHEAT above it — enough that it can travel through the gating and fill the last thin corner before it starts to freeze. Too little superheat and the metal stops before the cavity is full, or two streams meet and fail to fuse. Too much and it dissolves more gas, oxidises harder, burns the sand, and shrinks more on the way down — so the porosity gets worse rather than better. The window is perhaps 100 to 150 degrees wide, it differs by alloy and by casting, and the only way to sit inside it reliably is to MEASURE. Judging melt temperature by colour is the pyrometer rung's warning delivered with molten metal.
Abantado
3 hours

Mga Tagubilin

1

Superheat, by alloy

Naglo-load ng Jupyter notebook…

Mga materyales para sa hakbang na ito:

Bareta ng tanso-lataBareta ng tanso-lata1 piraso
Tinunaw na aluminyo 99.7 % dalisay na 450 gTinunaw na aluminyo 99.7 % dalisay na 450 g1 piraso

Mga kailangang kasangkapan:
PirometroPirometro
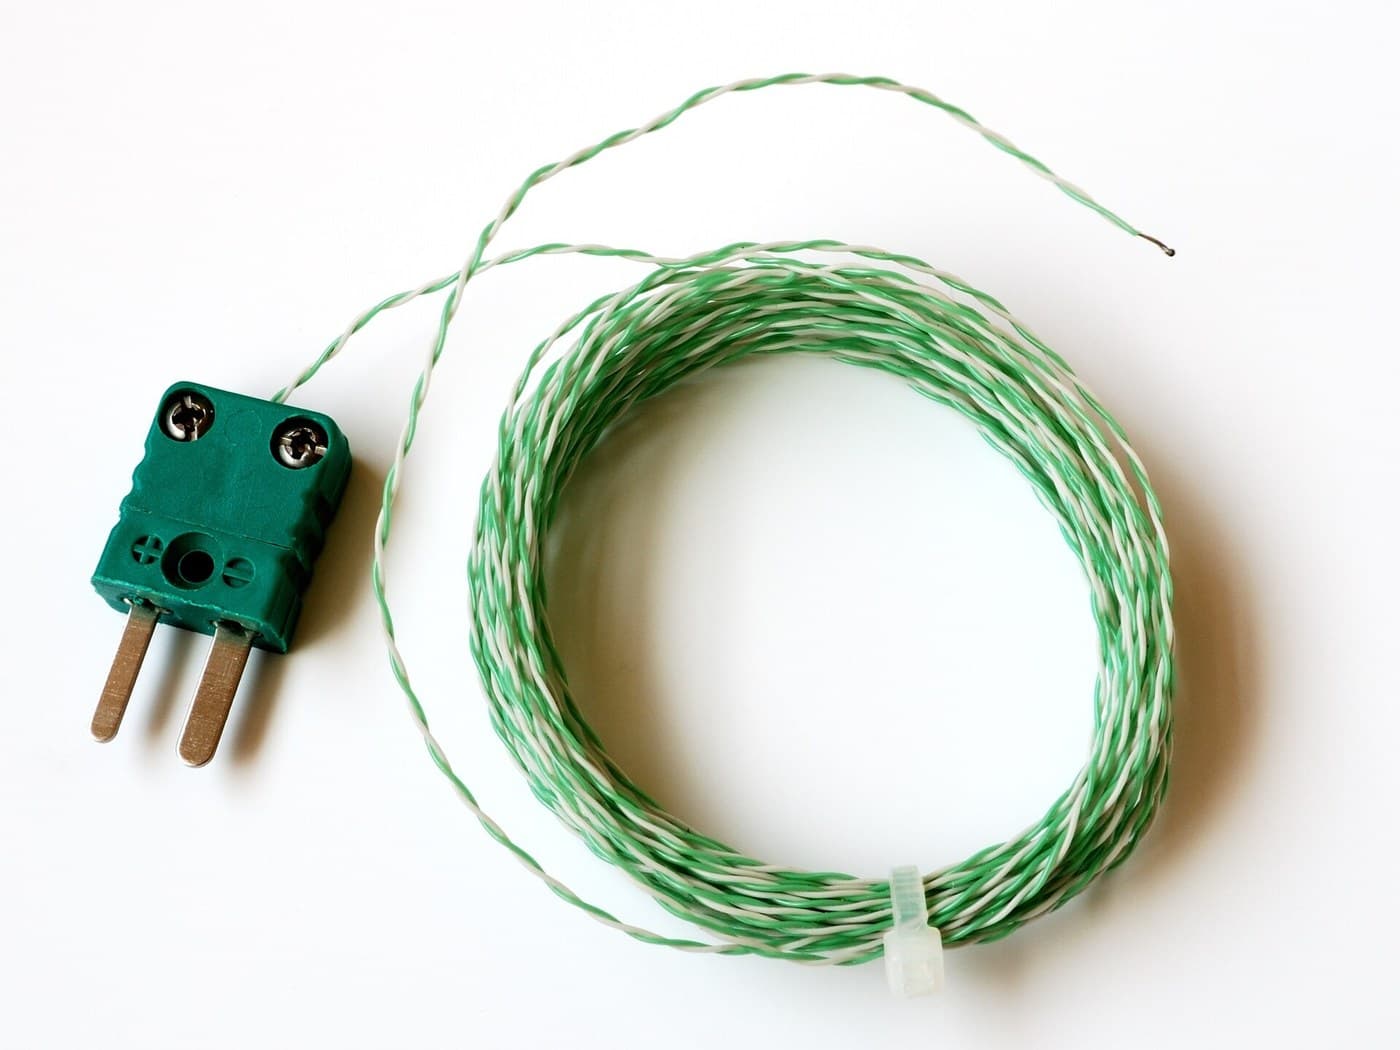
Thermocouple na may basahanThermocouple na may basahan
Desktop na KompyuterDesktop na Kompyuter
2

Skim, and do not stir the dross back in

Oxide and impurities float. Skim them off the surface of the melt immediately before pouring, with a preheated skimmer, and take them right out of the crucible rather than pushing them aside. Preheat every tool that will touch molten metal. A cold skimmer or ladle chills the metal locally and, far worse, any trace of moisture on it flashes to steam instantly — which throws metal. Do not stir after skimming. Stirring folds the remaining surface oxide down into the melt, where it becomes inclusions in the casting. Aluminium is the worst for this: its oxide skin is tough, and every disturbance of the surface makes more of it.

Mga materyales para sa hakbang na ito:

Bareta ng tanso-lataBareta ng tanso-lata1 piraso

Mga kailangang kasangkapan:

Salok na pinong lalaSalok na pinong lala
Sandok ng pagbububo ng metalSandok ng pagbububo ng metal
Sipit ng KrisolSipit ng Krisol
Katad na Gwantes na MahabaKatad na Gwantes na Mahaba
3

Dry everything, and mean it

Water and molten metal is the one genuinely dangerous combination in a foundry. Water turned to steam expands roughly 1,600 times, instantly, and if it is under metal it throws that metal outward. So: preheat and dry the crucible, the tongs, the ladle and every ingot before it goes near the melt. An ingot with condensation on it, or a scrap casting with water trapped in a cavity, is the classic cause. The mould matters too. Green sand contains water by design and that is fine because it is bound in the clay and the mould is permeable — but a sand that is too wet, or a mould left standing so condensation collects, is the same hazard in a different place.

Mga materyales para sa hakbang na ito:

Bareta ng tanso-lataBareta ng tanso-lata1 piraso
Uling na TipakUling na Tipak1 piraso

Mga kailangang kasangkapan:
KrisolKrisol
Sipit ng KrisolSipit ng Krisol
Maitim na salaming pang-pandayanMaitim na salaming pang-pandayan
Katad na Gwantes na MahabaKatad na Gwantes na Mahaba
4

Everything ready before the metal is

Once the metal is at temperature it is losing heat and gaining gas every second. The moulds must be closed, weighted, vented and positioned before the crucible comes out of the furnace. Weight or clamp the cope. Molten metal exerts real upward pressure on the top half of the mould, and an unweighted cope lifts and lets metal run out of the parting line — which is dangerous as well as a lost casting. Have a clear path, a clear floor, and somewhere planned to put the crucible down. The pour itself takes a few seconds; everything that makes it go well or badly was decided in the minutes before it.

Mga materyales para sa hakbang na ito:

Buhangin sa paghuhulmaBuhangin sa paghuhulma1 kg

Mga kailangang kasangkapan:
Kahong panghulma (itaas at ibaba)Kahong panghulma (itaas at ibaba)
Sipit ng KrisolSipit ng Krisol
Maitim na salaming pang-pandayanMaitim na salaming pang-pandayan
Katad na Gwantes na MahabaKatad na Gwantes na Mahaba

Mga Materyales

4

Mga Kinakailangang Kasangkapan

10

CC0 Pampublikong Domain

Ang blueprint na ito ay inilabas sa ilalim ng CC0. Malaya kang kumopya, magbago, mamahagi, at gumamit nang walang pahintulot.

Suportahan ang Maker sa pamamagitan ng pagbili ng mga produkto sa kanilang Blueprint Komisyon ng Maker itinakda ng mga Vendor, o lumikha ng bagong bersyon ng Blueprint na ito at isama bilang koneksyon sa iyong Blueprint upang ibahagi ang kita.

Talakayan

(0)

Mag-login upang sumali sa talakayan

Naglo-load ng mga komento...