تعاون
فن
خوبصورتی اور تندرستی
دستکاری
ثقافت اور تاریخ
تفریح
ماحول
خوراک اور مشروبات
ریورس انجینئرنگ
سائنسز
کھیل
ٹیکنالوجی
پہننے والے آلات
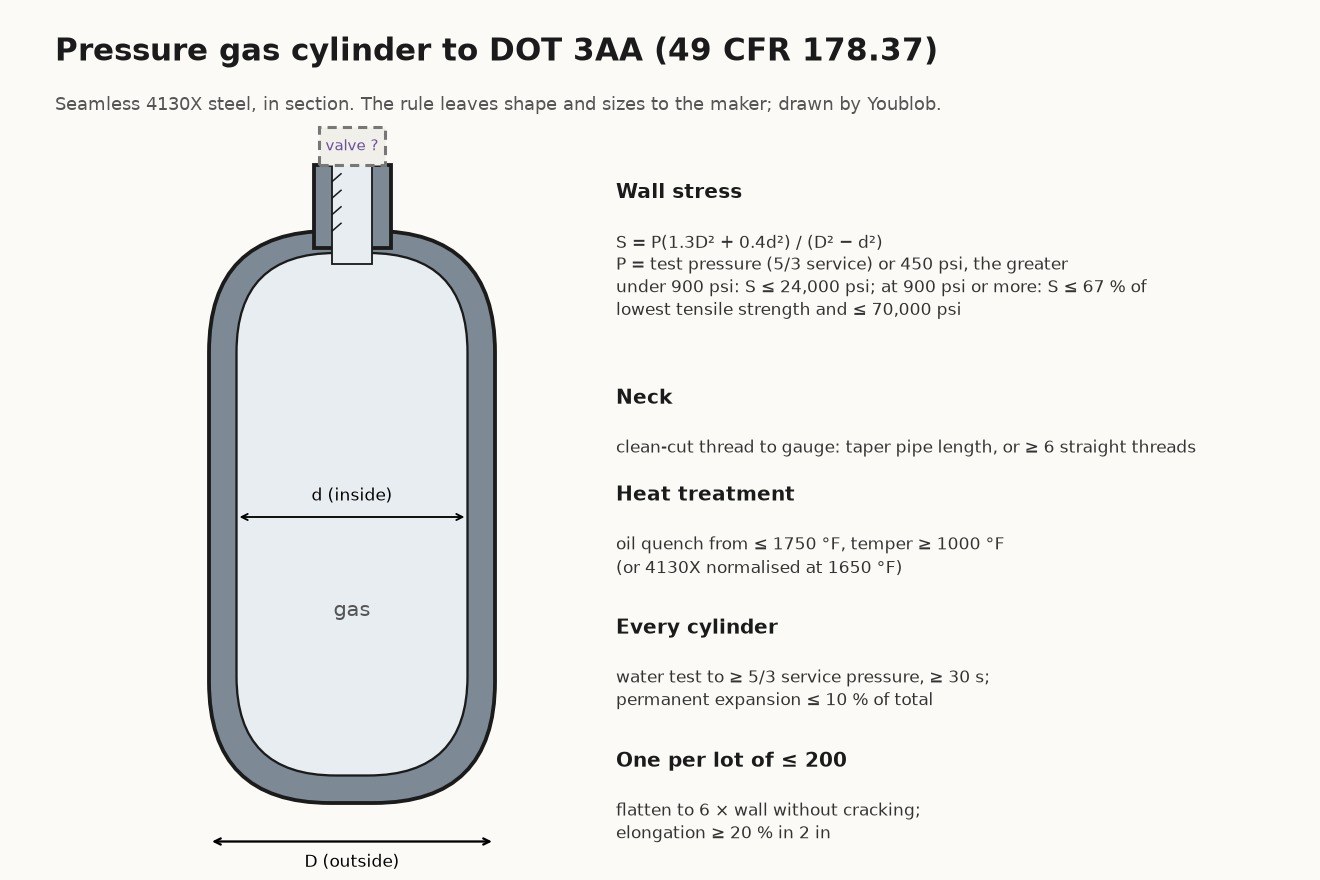


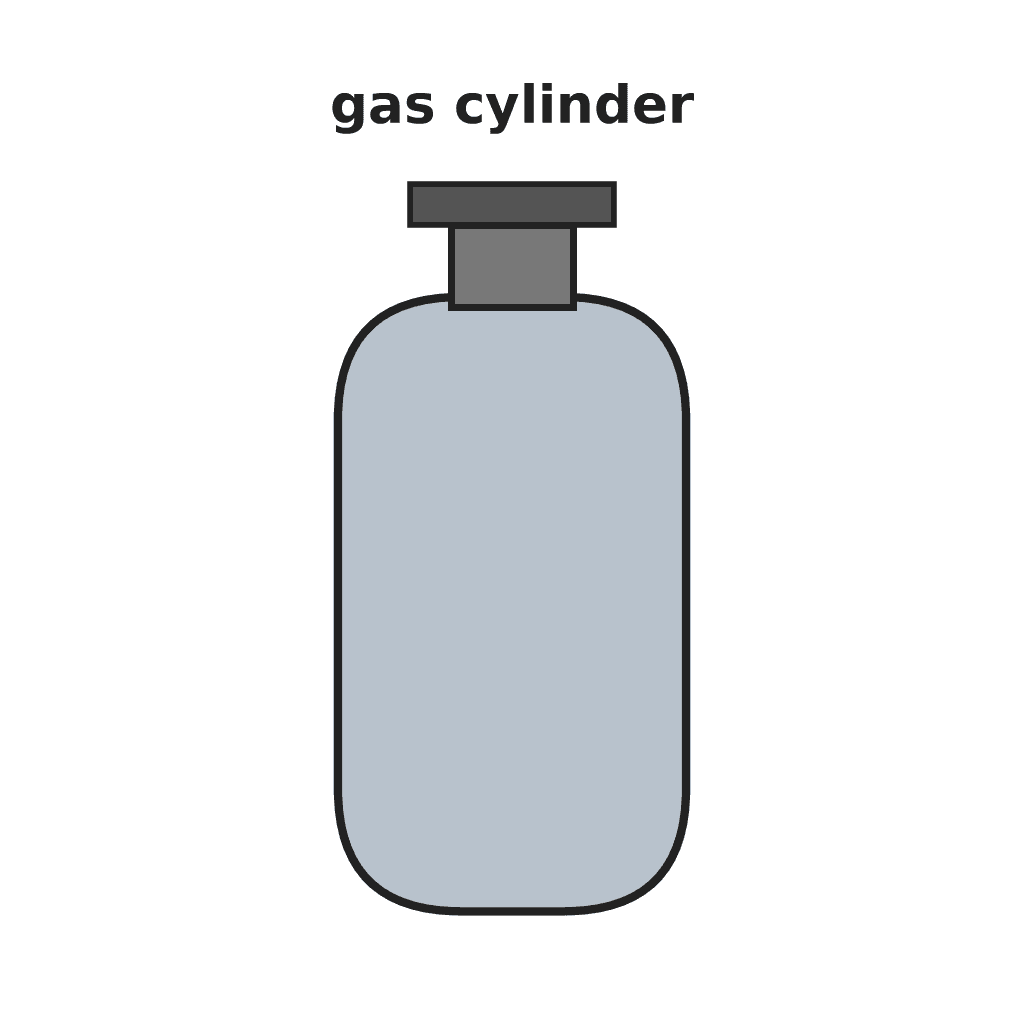
Pressure Gas Cylinder: Seamless 4130X Steel to DOT 3AA (49 CFR 178.37)
A seamless steel cylinder for compressed or liquefied gas, made to the US rule DOT 3AA: at least 150 psi service pressure, up to 1,000 lb of water capacity. The rule gives the steel, a formula for the wall, the heat treatment and the tests every cylinder or lot must pass. It does not say how the shell is formed.
Result: a seamless 4130X steel cylinder, heat-treated and proof-tested to 5/3 of its service pressure, with a threaded neck for its valve.
Source: 49 CFR 178.37, Specification 3AA. Unknown: how the shell is formed, the valve, the test apparatus. Picture drawn by Youblob.
اعلیٰ
Unknown
ہدایات
1
1
Size the wall
Size the wall
Pick the service pressure (at least 150 psi) and the diameter. Find the wall stress S = P(1.3D² + 0.4d²) / (D² − d²), with D and d the outside and inside diameters in inches and P the test pressure (5/3 of service pressure) or 450 psi, whichever is greater. Below 900 psi service, S may not pass 24,000 psi, and a cylinder over 5 in across needs a wall of at least 0.100 in. At 900 psi or more, S may not pass 67 % of the steel's lowest tensile strength, nor 70,000 psi.
درکار اوزار:
 نامعلوم پیمائش
2
2
Get the steel
Get the steel
Use open-hearth, basic oxygen or electric steel of uniform quality, here 4130X: carbon 0.25-0.35 %, manganese 0.40-0.90 %, silicon 0.15-0.35 %, chromium 0.80-1.10 %, molybdenum 0.15-0.25 %, phosphorus 0.04 % and sulphur 0.05 % at most. For hot-drawn cylinders, mark each billet with its heat number.
اس مرحلے کے لیے مواد:
 4130 اسٹیل بلٹ1 per cylinder
درکار اوزار:
نامعلوم پیمائش3
3
Form the seamless shell
Form the seamless shell
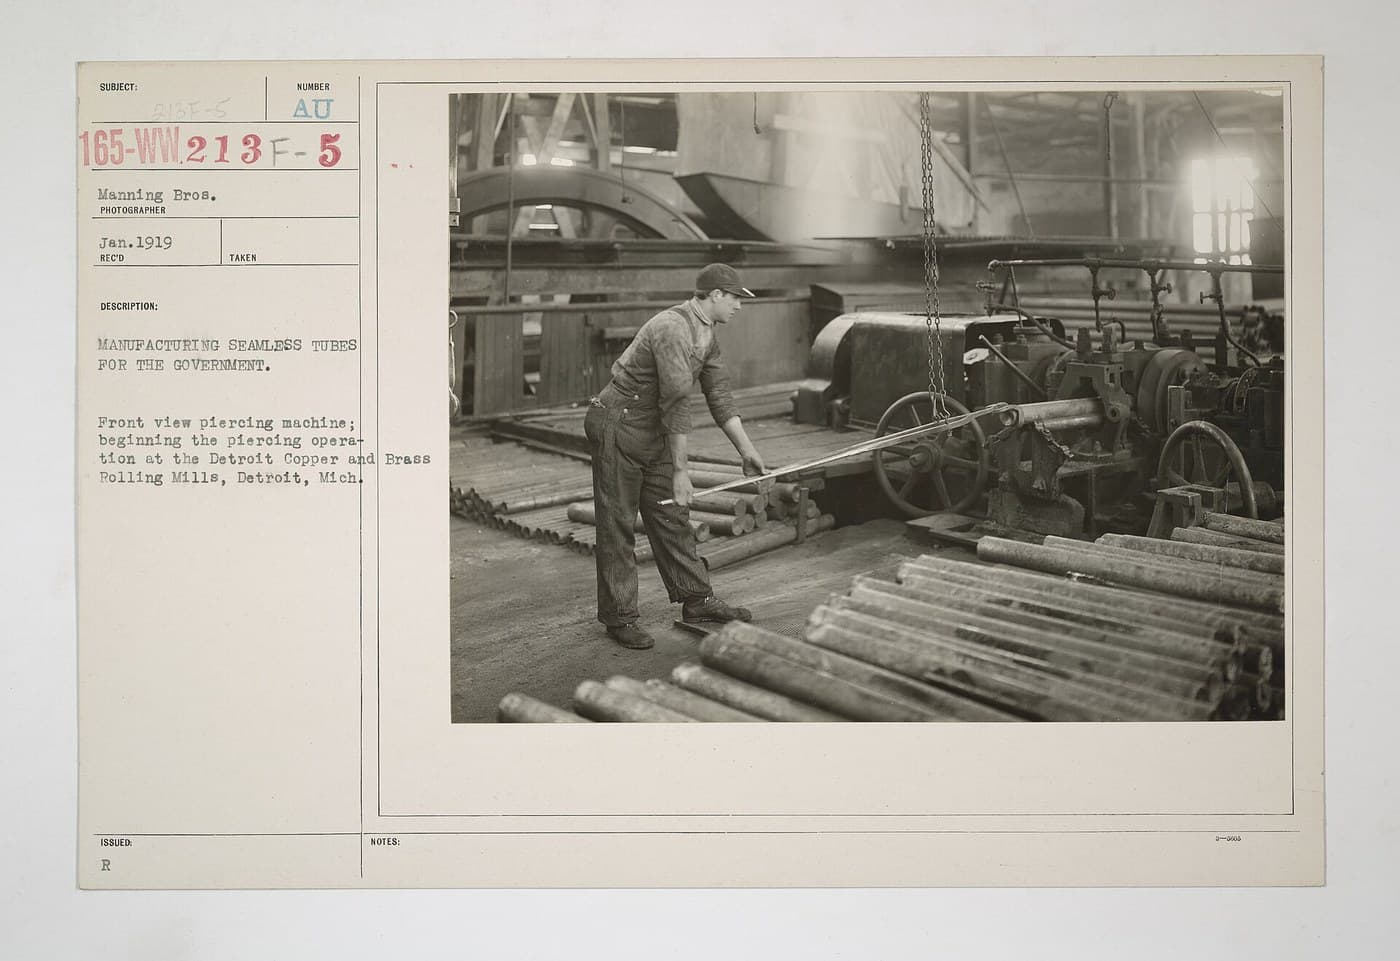
Form the billet into a seamless cylinder with no fissures and a smooth, even surface; machine away any defects. A bottom closed by welding or spinning must be at least twice the minimum wall thick. Do not weld anything else, except neck and foot rings on cylinders of 500 psi or less. Not given: how the shell is formed (the rule names hot drawing from billet or plate, and spinning).
درکار اوزار:
 نامعلوم تشکیل کا طریقہنامعلوم پیمائش
4
4
Thread the neck
Thread the neck
Cut a clean, even thread in the neck opening, to gauge. A taper thread must be at least as long as an American Standard taper pipe thread. A straight thread needs at least six engaged threads, a tight fit, a gasket, and a shear strength of at least ten times the test pressure.
درکار اوزار:
 چُوڑی کاٹنے کا سیٹ
5
5
Heat-treat
Heat-treat
Heat-treat each finished cylinder evenly before testing. Quench it in oil or another suitable medium from the temperature right for the steel, no higher than 1750 °F, then temper at 1000 °F or more. Or normalise 4130X at 1650 °F instead, with no tempering. A cylinder quenched in water, or in anything cooling more than 80 % as fast, must be checked for quench cracks by magnetic particle, dye penetrant or ultrasound; a cracked one is scrapped.
درکار اوزار:
 حرارتی عمل کاری کا تنور
 تیل والا ٹھنڈا کرنے کا حوض
 ٹیمپرنگ اوون
6
6
Pressure-test every cylinder
Pressure-test every cylinder
Test each cylinder with water by the water-jacket or direct-expansion method of CGA C-1, to at least 5/3 of service pressure, held for at least 30 seconds and until it stops expanding. Between heat treatment and this test, never go above 90 % of test pressure. The permanent expansion may not pass 10 % of the total expansion. Not given: the CGA C-1 apparatus.
درکار اوزار:
 ہائیڈرولک دباؤ جانچنے کی کٹ
7
7
Test one from each lot
Test one from each lot
From each lot of 200 or fewer, take one cylinder. Flatten it between two 60° knife edges rounded to ½ in radius, set across its axis: it must reach six times the wall thickness without cracking. Cut two tensile specimens from it: find the yield at 0.2 % offset, moving the cross-head no faster than ⅛ in per minute, and the tensile strength; elongation must be at least 20 % over 2 in (10 % on other gauge lengths). A rejected cylinder may be heat-treated again and retested, never repaired by welding or spinning.
درکار اوزار:
 ہائیڈرولک پریس
 مادّوں کی جانچ کی مشین
8
8
Fit the valve
Fit the valve
Screw the valve into the threaded neck. A cylinder whose bottom was closed by spinning or by a plug must also pass a gas leak test: apply at least service pressure to one side of the clean, dry bottom for at least a minute, with the other side under water, and reject it at any leak. Not given: the valve.
اس مرحلے کے لیے مواد:
 نامعلوم والو1 ٹکڑا
درکار اوزار:
 انگریزی پانا
مواد
2- 1 per cylinderپلیس ہولڈر
- 1 ٹکڑاپلیس ہولڈر
درکار اوزار
10- پلیس ہولڈر
- پلیس ہولڈر
- پلیس ہولڈر
- پلیس ہولڈر
- پلیس ہولڈر
- پلیس ہولڈر
- پلیس ہولڈر
- پلیس ہولڈر
- پلیس ہولڈر
- پلیس ہولڈر
منسلک بلیو پرنٹ مواد


یہ بلوپرنٹ بناتا ہے
متعلقہ بلیو پرنٹ
یہ بلیو پرنٹ علم بانٹتے ہیں — تکنیک، مواد یا اصول
CC0 پبلک ڈومین
یہ بلیو پرنٹ CC0 کے تحت جاری کیا گیا ہے۔ آپ اجازت لیے بغیر اس کام کو نقل، ترمیم، تقسیم اور کسی بھی مقصد کے لیے استعمال کرنے کے لیے آزاد ہیں۔
میکر کی حمایت کریں ان کے بلیو پرنٹ کے ذریعے پروڈکٹس خرید کر جہاں وہ میکر کمیشن وینڈرز کی طرف سے مقرر، کماتے ہیں، یا اس بلیو پرنٹ کی نئی تکرار بنائیں اور آمدنی شیئر کرنے کے لیے اسے اپنے بلیو پرنٹ میں کنکشن کے طور پر شامل کریں۔