Współpraca
SZTUKA
Piękno i dobre samopoczucie
RZEMIOSŁO
KULTURA I HISTORIA
ROZRYWKA
ŚRODOWISKO
JEDZENIE I NAPOJE
INŻYNIERIA ODWROTNA
NAUKI
LEKKOATLETYKA
TECHNOLOGIA
URZĄDZENIA DO NOSZENIA
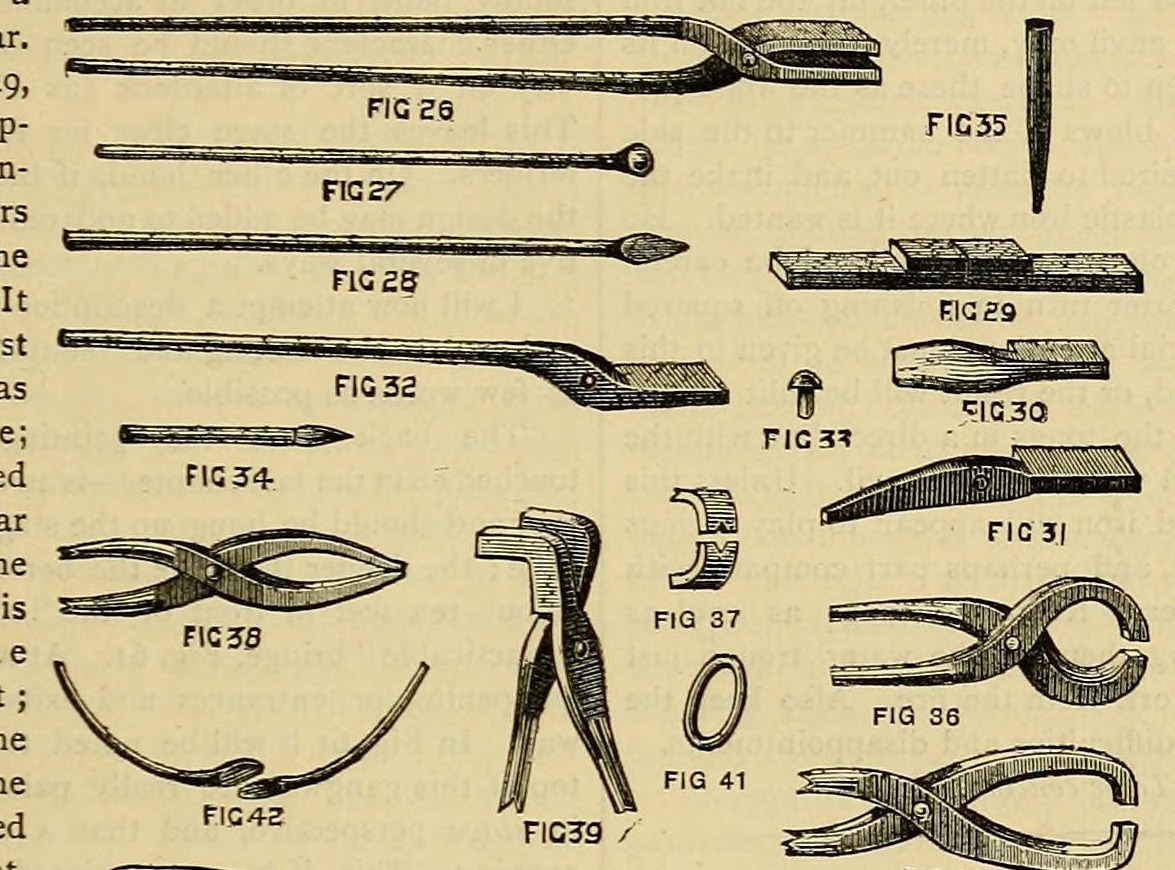


Flat-Bit Tongs and the Tongs Made from Them, down to Crucible Tongs: Welded Reins, Riveted Joint (Edwinson, 1886)
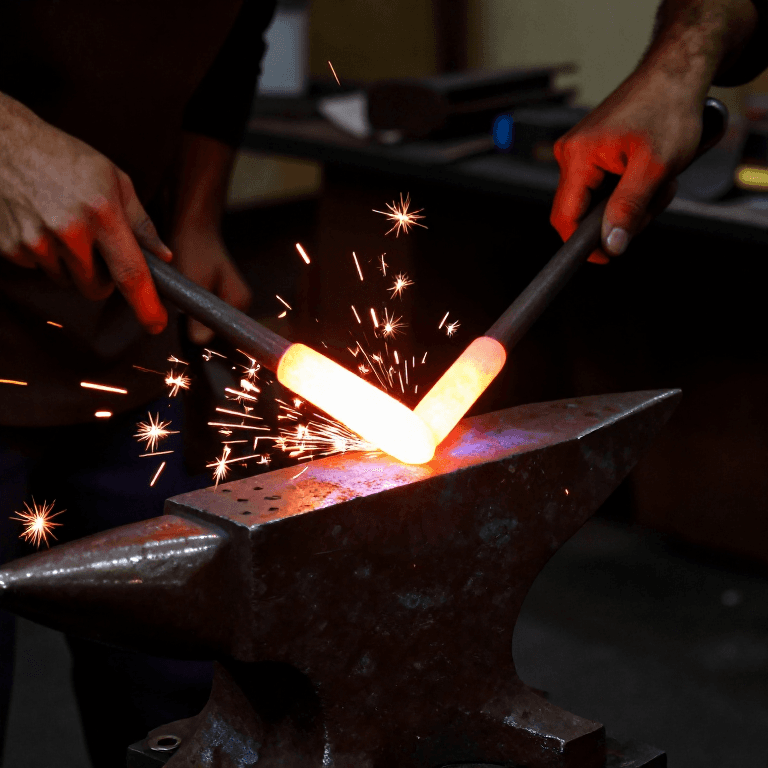
George Edwinson's tong-making lesson from Amateur Work (1886): jaws forged from inch-square iron, reins of 5/8 in. rod scarfed and welded on, the halves riveted with a hot iron pin. The same flat-bit tongs are then reshaped into pincer, hammer and crook-bit tongs, light smith's pliers, and thinned and curved into crucible tongs.
Zaawansowany
A day at the forge
Instrukcje
1
1
His sizes
His sizes
Wczytywanie notatnika Jupyter…
2
2
Read Edwinson
Read Edwinson
"Indeed, the man who can turn out a good pair of tongs may be trusted with almost any job in the smithy."
3
3
Forge the reins
Forge the reins
Cut two pieces of 5/8 in. (16 mm) iron rod, each 2 ft (0.6 m) long, with a cold chisel. Bring one end of each to a white welding heat and draw 3-4 in. down to a taper from 5/8 to 1/2 in., rounded for the hand. Upset the other ends at a white heat and scarf them (his figs. 27-28).
Materiały do tego kroku:
 Pręt z kutego żelaza1 sztuka
Potrzebne narzędzia:
 Przecinak ślusarski
 Kuźnia kowalska
 Kowadło
 Młotek
 Szczypce kowalskie
4
4
Forge the jaws
Forge the jaws
Cut two 6 in. pieces of 1 in. square iron (or one 12 in. bar, worked from each end before cutting, fig. 29). Forge each jaw end 4 in. long, 1 1/4 in. wide and 3/8 in. thick. Flatten the other end to 1/4 in. thick, round it for the joint (fig. 30) and draw it to a slightly rounded taper (fig. 31).
Materiały do tego kroku:
 Pręt kwadratowy ze stali miękkiej1 sztuka
Potrzebne narzędzia:
Kuźnia kowalskaKowadłoMłotekSzczypce kowalskie5
5
Punch the joint
Punch the joint
Mark the hole with a centre punch, heat, and punch a 3/8 in. hole over the anvil's heel hole with an iron punch tapering 1/4 to 1/2 in. (fig. 35), or a steel punch of 5/8 in. tool steel.
Materiały do tego kroku:
 Pręt ze stali narzędziowej1 sztuka
Potrzebne narzędzia:
 PunktakKuźnia kowalskaKowadłoMłotek
6
6
Weld jaw to rein
Weld jaw to rein
Scarf the taper end of each jaw to fit a rein. Heat both to a welding heat in a clear fire, throw on clean fine fresh-water sand and heat until pasty. Tap the scarfs together lightly, return to the fire a moment, and finish the weld. At a red heat forge the square part to blend into the round rein (fig. 32).
Materiały do tego kroku:
 Piasek1 sztuka
Potrzebne narzędzia:
Kuźnia kowalskaKowadłoMłotekSzczypce kowalskie7
7
Rivet the joint
Rivet the joint
Smiths' way: nick a 3/8 in. round iron rod to rivet length, put the halves together, insert the hot end, twist it off, let 1/4 in. stand below, and rivet both sides. (Or make a 3/4 x 3/8 in. button-headed rivet in a 3/8 in. hole in a flat iron.) If the joint locks, reheat jaws and pin to bright red and work them free.
Materiały do tego kroku:
Pręt z kutego żelaza1 sztukaPotrzebne narzędzia:
Kuźnia kowalskaKowadłoMłotek Gwoździownica
8
8
Set the jaws
Set the jaws
Heat the jaws and set them to the width of the stock to be held. Spring them wider with a piece of cold iron between and a few light blows.
Potrzebne narzędzia:
Kuźnia kowalskaKowadłoMłotek9
9
Crucible tongs and other forms
Crucible tongs and other forms
From flat-bit tongs at the fig. 32 stage: lengthen and curve the bits for pincer tongs (angular notches hold round or square bars), more for hammer tongs, bend them sideways for crook-bit tongs. Small flat-bit tongs with lengthened, shaped bits are smith's pliers; thin those out further and curve them like pincers to make crucible tongs for hot crucibles and pots of molten metal. Heavy tongs 2-5 ft long need stouter iron.
Potrzebne narzędzia:
Kuźnia kowalskaKowadłoMłotekSzczypce kowalskie10
10
Troubleshooting
Troubleshooting
Tongs troubleshooting.
Flow
Loading...
11
11
History and honest limits
History and honest limits
From George Edwinson, "Smithing and Forging" III, **Amateur Work, Illustrated**, vol. V (1886), pp. 266-269 (checked on the archive.org scan amateurworkillus05lond). He gives full sizes only for the flat-bit tongs; crucible tong sizes and curvature are left to the work. Metric figures and tools are ours.
Materiały
4- 1 sztukaZastępnik
- Zastępnik
- 1 sztukaZastępnik
- 1 sztukaZastępnik
Według tego planu powstaje

Powiązane blueprinty
Te blueprinty dzielą się wiedzą — technikami, materiałami lub zasadami
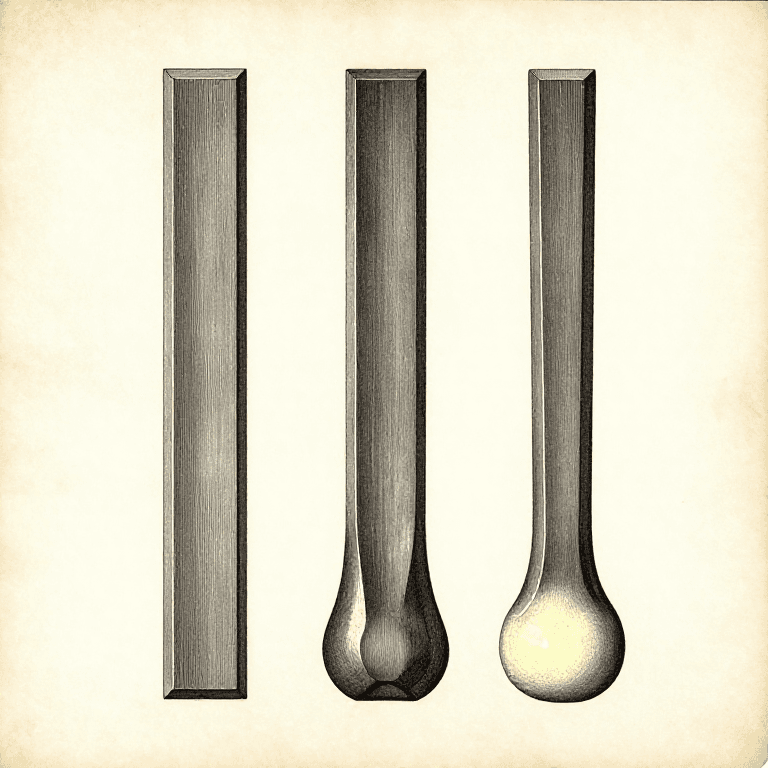
CC0 Domena publiczna
Ten plan jest udostępniany na licencji CC0. Możesz go swobodnie kopiować, modyfikować, rozpowszechniać i wykorzystywać do dowolnych celów, bez konieczności uzyskiwania zgody.
Wesprzyj Makera kupując produkty przez jego plan, za co zarabia Prowizja Makera ustalony przez sprzedawców, lub stwórz nową iterację tego planu i dołącz go jako połączenie w swoim własnym planie, aby dzielić się przychodami.