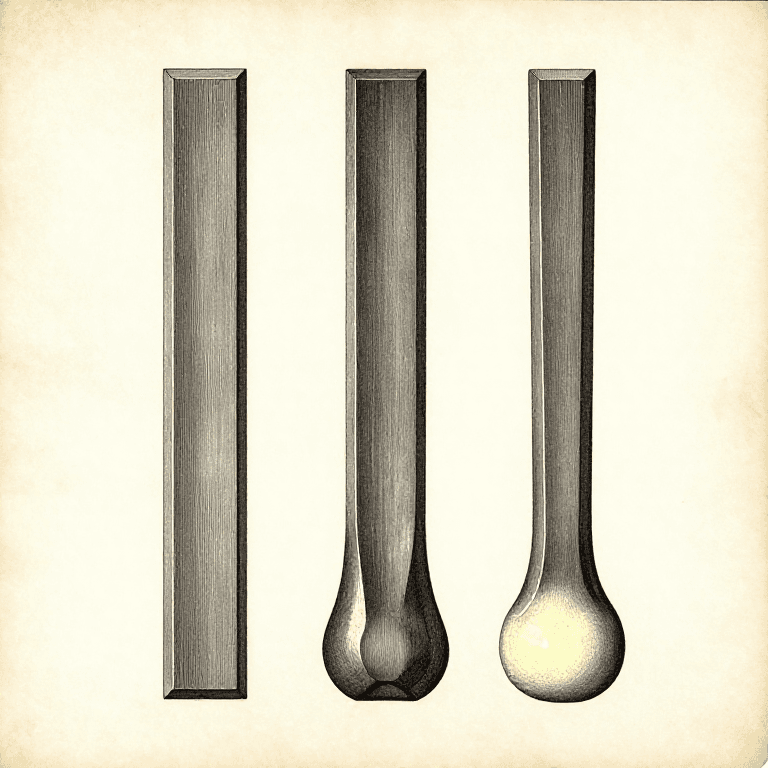

Współpraca
SZTUKA
Piękno i dobre samopoczucie
RZEMIOSŁO
KULTURA I HISTORIA
ROZRYWKA
ŚRODOWISKO
JEDZENIE I NAPOJE
INŻYNIERIA ODWROTNA
NAUKI
LEKKOATLETYKA
TECHNOLOGIA
URZĄDZENIA DO NOSZENIA
Fuller, Pritchel and Hot Setts: Steel Welded into a Split Iron Bar, with Twisted Rod or Withy Handles (Edwinson, 1886)
Forge

Autor

Forge

14. listopad 2026NO
6
0
0
0
0

Fuller, Pritchel and Hot Setts: Steel Welded into a Split Iron Bar, with Twisted Rod or Withy Handles (Edwinson, 1886)

The smith's own top and bottom tools, from George Edwinson's farrier's chapter in Amateur Work (1886): an inch iron bar upset, split into a fork and a steel wedge welded in, then forged into a fuller, pritchel punch, curved or straight hot sett, or a square-tanged bottom sett; the pritchel itself from 1/2 in. square tool steel; handles of twisted iron rod or green withy.
Zaawansowany
A day at the forge for the set

Instrukcje

1

His proportions

Wczytywanie notatnika Jupyter…
2

Read Edwinson

"To make this tool, heat and upset the end of an inch bar of iron; then heat again and split with a sett."
3

Split the iron

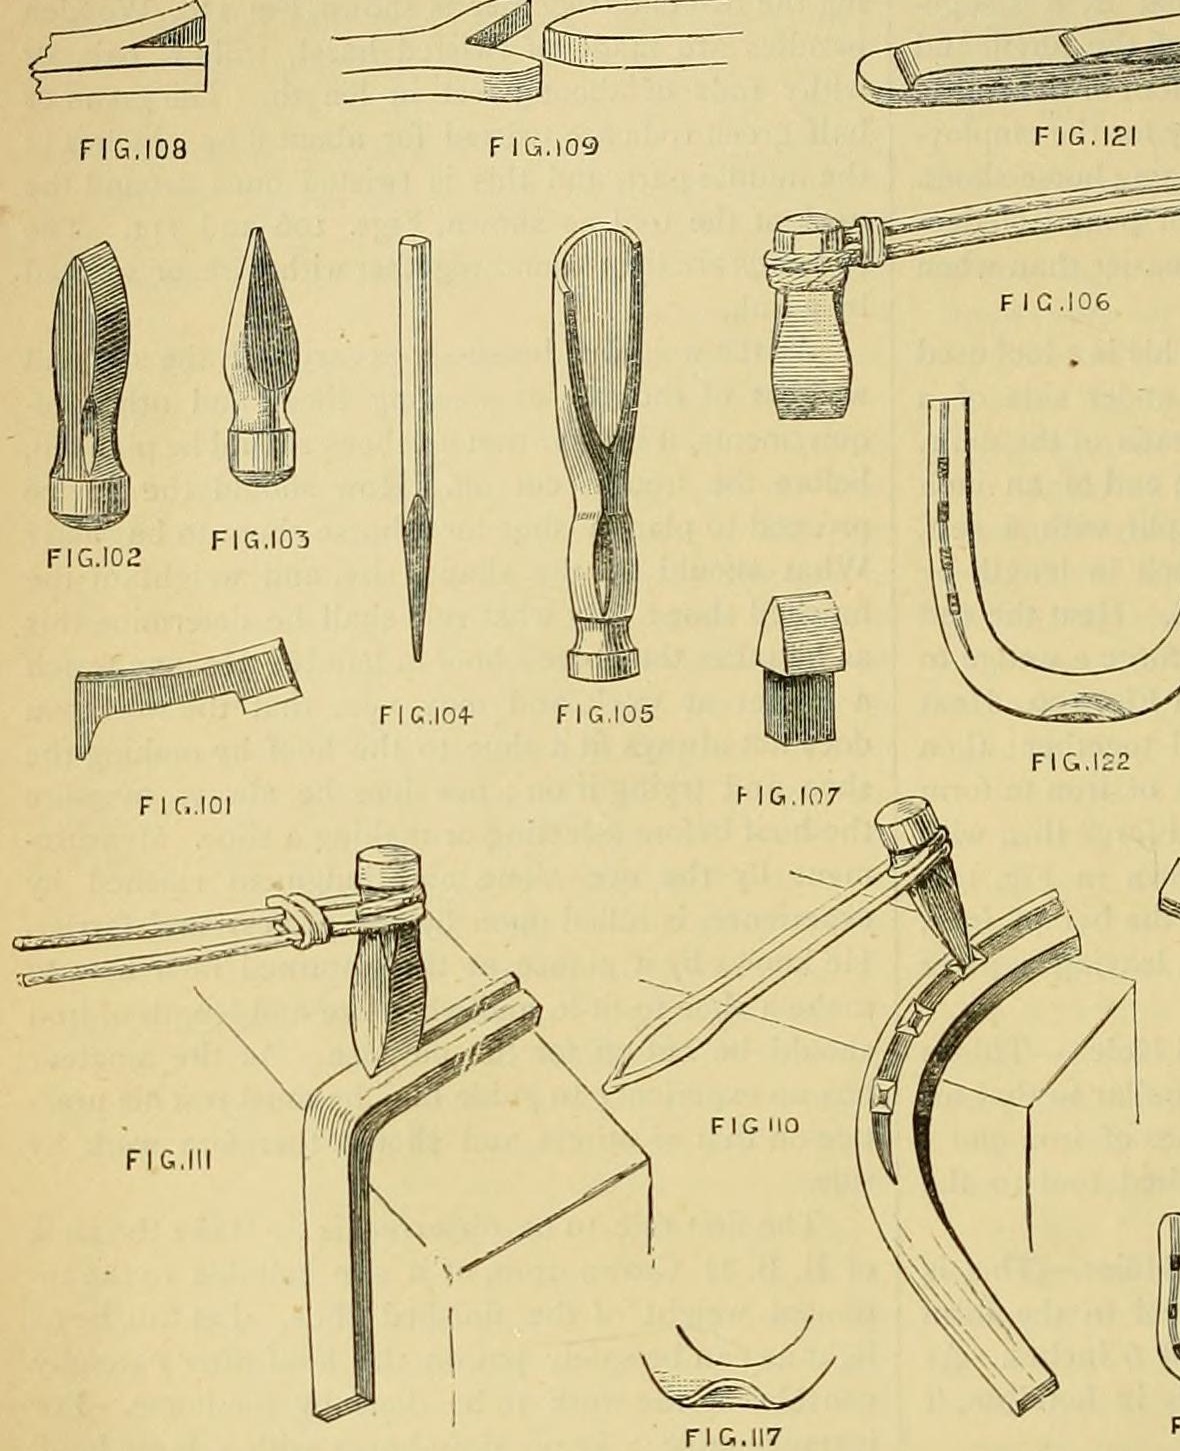
Heat and upset the end of a 1 in. (25 mm) iron bar. Heat again and split it with a hot set into a fork 1 to 1 1/4 in. long by 3/4 in. wide (his fig. 108).

Materiały do tego kroku:

Pręt z kutego żelazaPręt z kutego żelaza1 sztuka

Potrzebne narzędzia:

Kuźnia kowalskaKuźnia kowalska
KowadłoKowadło
Młot dwuręcznyMłot dwuręczny
Przecinak na gorącoPrzecinak na gorąco
Szczypce kowalskieSzczypce kowalskie
4

Weld in the steel

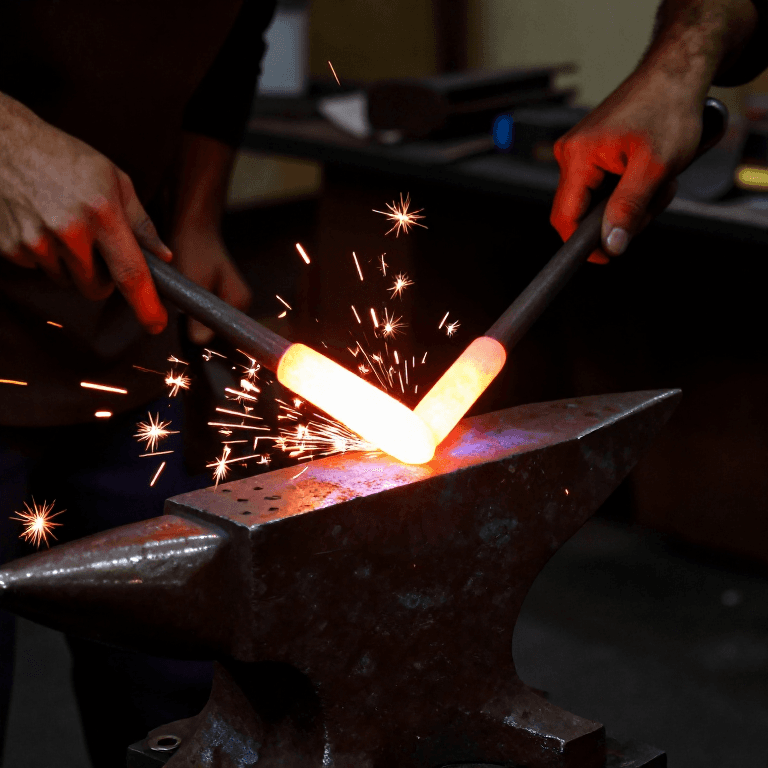
Heat the end of a steel bar of similar size and forge a wedge to fit the fork (fig. 109). Bring both to a welding heat and weld them well together.

Materiały do tego kroku:

Stal tyglowaStal tyglowa1 sztuka
Boraks w proszkuBoraks w proszku1 sztuka

Potrzebne narzędzia:

Kuźnia kowalskaKuźnia kowalska
KowadłoKowadło
Młot dwuręcznyMłot dwuręczny
Szczypce kowalskieSzczypce kowalskie
5

Forge the fuller

Cut off 2 in. of steel and 3 in. of iron for the tool. Forge the steel, with the iron behind it, into the fuller's rounded blade (fig. 102). Make the neck while it is still on the bar, then cut it off leaving a piece of iron for the head.

Potrzebne narzędzia:

Kuźnia kowalskaKuźnia kowalska
KowadłoKowadło
MłotekMłotek
Przecinak na gorącoPrzecinak na gorąco
6

Same blank, other tools

Pritchel punch: about 2 in. of iron and 1 in. of steel, shaped as fig. 103. Curved set: as the fuller but with a gouge-shaped blade (fig. 105). Top hot set: the same, with a chisel or wedge blade (fig. 106). Bottom set: a wedge of steel and iron, edge up, on a square tang that fits the anvil's square hole (fig. 107).

Materiały do tego kroku:

Pręt z kutego żelazaPręt z kutego żelaza1 sztuka
Stal tyglowaStal tyglowa1 sztuka
Boraks w proszkuBoraks w proszku1 sztuka

Potrzebne narzędzia:

Kuźnia kowalskaKuźnia kowalska
KowadłoKowadło
MłotekMłotek
Młot dwuręcznyMłot dwuręczny
Szczypce kowalskieSzczypce kowalskie
7

Forge the pritchel

Forge 1/2 in. (13 mm) square tool steel into the tapered pritchel (fig. 104), 6 in. (150 mm) long. It punches nail holes in hot iron, so it need not be hardened.

Materiały do tego kroku:

Pręt ze stali narzędziowejPręt ze stali narzędziowej1 sztuka

Potrzebne narzędzia:

Kuźnia kowalskaKuźnia kowalska
KowadłoKowadło
MłotekMłotek
Szczypce kowalskieSzczypce kowalskie
8

Fit the handles

Rod handle: twist 3/8 in. iron rod once round the neck and weld the two ends together (fig. 110). Withy handle: take a green or half-green hazel, willow, oak or withy rod about 3 ft long, twist the middle 8-9 in., wrap it once round the neck and bind the two ends with wire or a link (figs. 106, 111).

Materiały do tego kroku:

Pręt okrągły ze stali niskowęglowejPręt okrągły ze stali niskowęglowej1 sztuka
Witki wierzbowe (giętkie)Witki wierzbowe (giętkie)1 sztuka
Drut żelaznyDrut żelazny1 sztuka

Potrzebne narzędzia:

Kuźnia kowalskaKuźnia kowalska
KowadłoKowadło
MłotekMłotek
Szczypce kowalskieSzczypce kowalskie
9

Harden the cutting tools (ours)

He gives no temper for these. Ours: harden and temper the set edges as for other hot-cutting tools, and cool them often in use.

Potrzebne narzędzia:

Kuźnia kowalskaKuźnia kowalska
Kadź hartowniczaKadź hartownicza
10

Troubleshooting

Top-tool troubleshooting.

Flow

Loading...
11

History and honest limits

From George Edwinson, "Smithing and Forging" VII, **Amateur Work, Illustrated**, vol. VI (1886-87), pp. 14-16 and figs. 101-111 (checked on the archive.org scan amateurworkillus06lond). He calls the top hot cutter a "sett"; we map it to the Hot Chisel head and the bottom sett to the Hot Cut Hardy head. Temper, metric figures and tools are ours.

Materiały

7

Wymagane narzędzia

7

CC0 Domena publiczna

Ten plan jest udostępniany na licencji CC0. Możesz go swobodnie kopiować, modyfikować, rozpowszechniać i wykorzystywać do dowolnych celów, bez konieczności uzyskiwania zgody.

Wesprzyj Makera kupując produkty przez jego plan, za co zarabia Prowizja Makera ustalony przez sprzedawców, lub stwórz nową iterację tego planu i dołącz go jako połączenie w swoim własnym planie, aby dzielić się przychodami.

Dyskusja

(0)

Zaloguj się aby dołączyć do dyskusji

Ładowanie komentarzy...