Współpraca
SZTUKA
Piękno i dobre samopoczucie
RZEMIOSŁO
KULTURA I HISTORIA
ROZRYWKA
ŚRODOWISKO
JEDZENIE I NAPOJE
INŻYNIERIA ODWROTNA
NAUKI
LEKKOATLETYKA
TECHNOLOGIA
URZĄDZENIA DO NOSZENIA
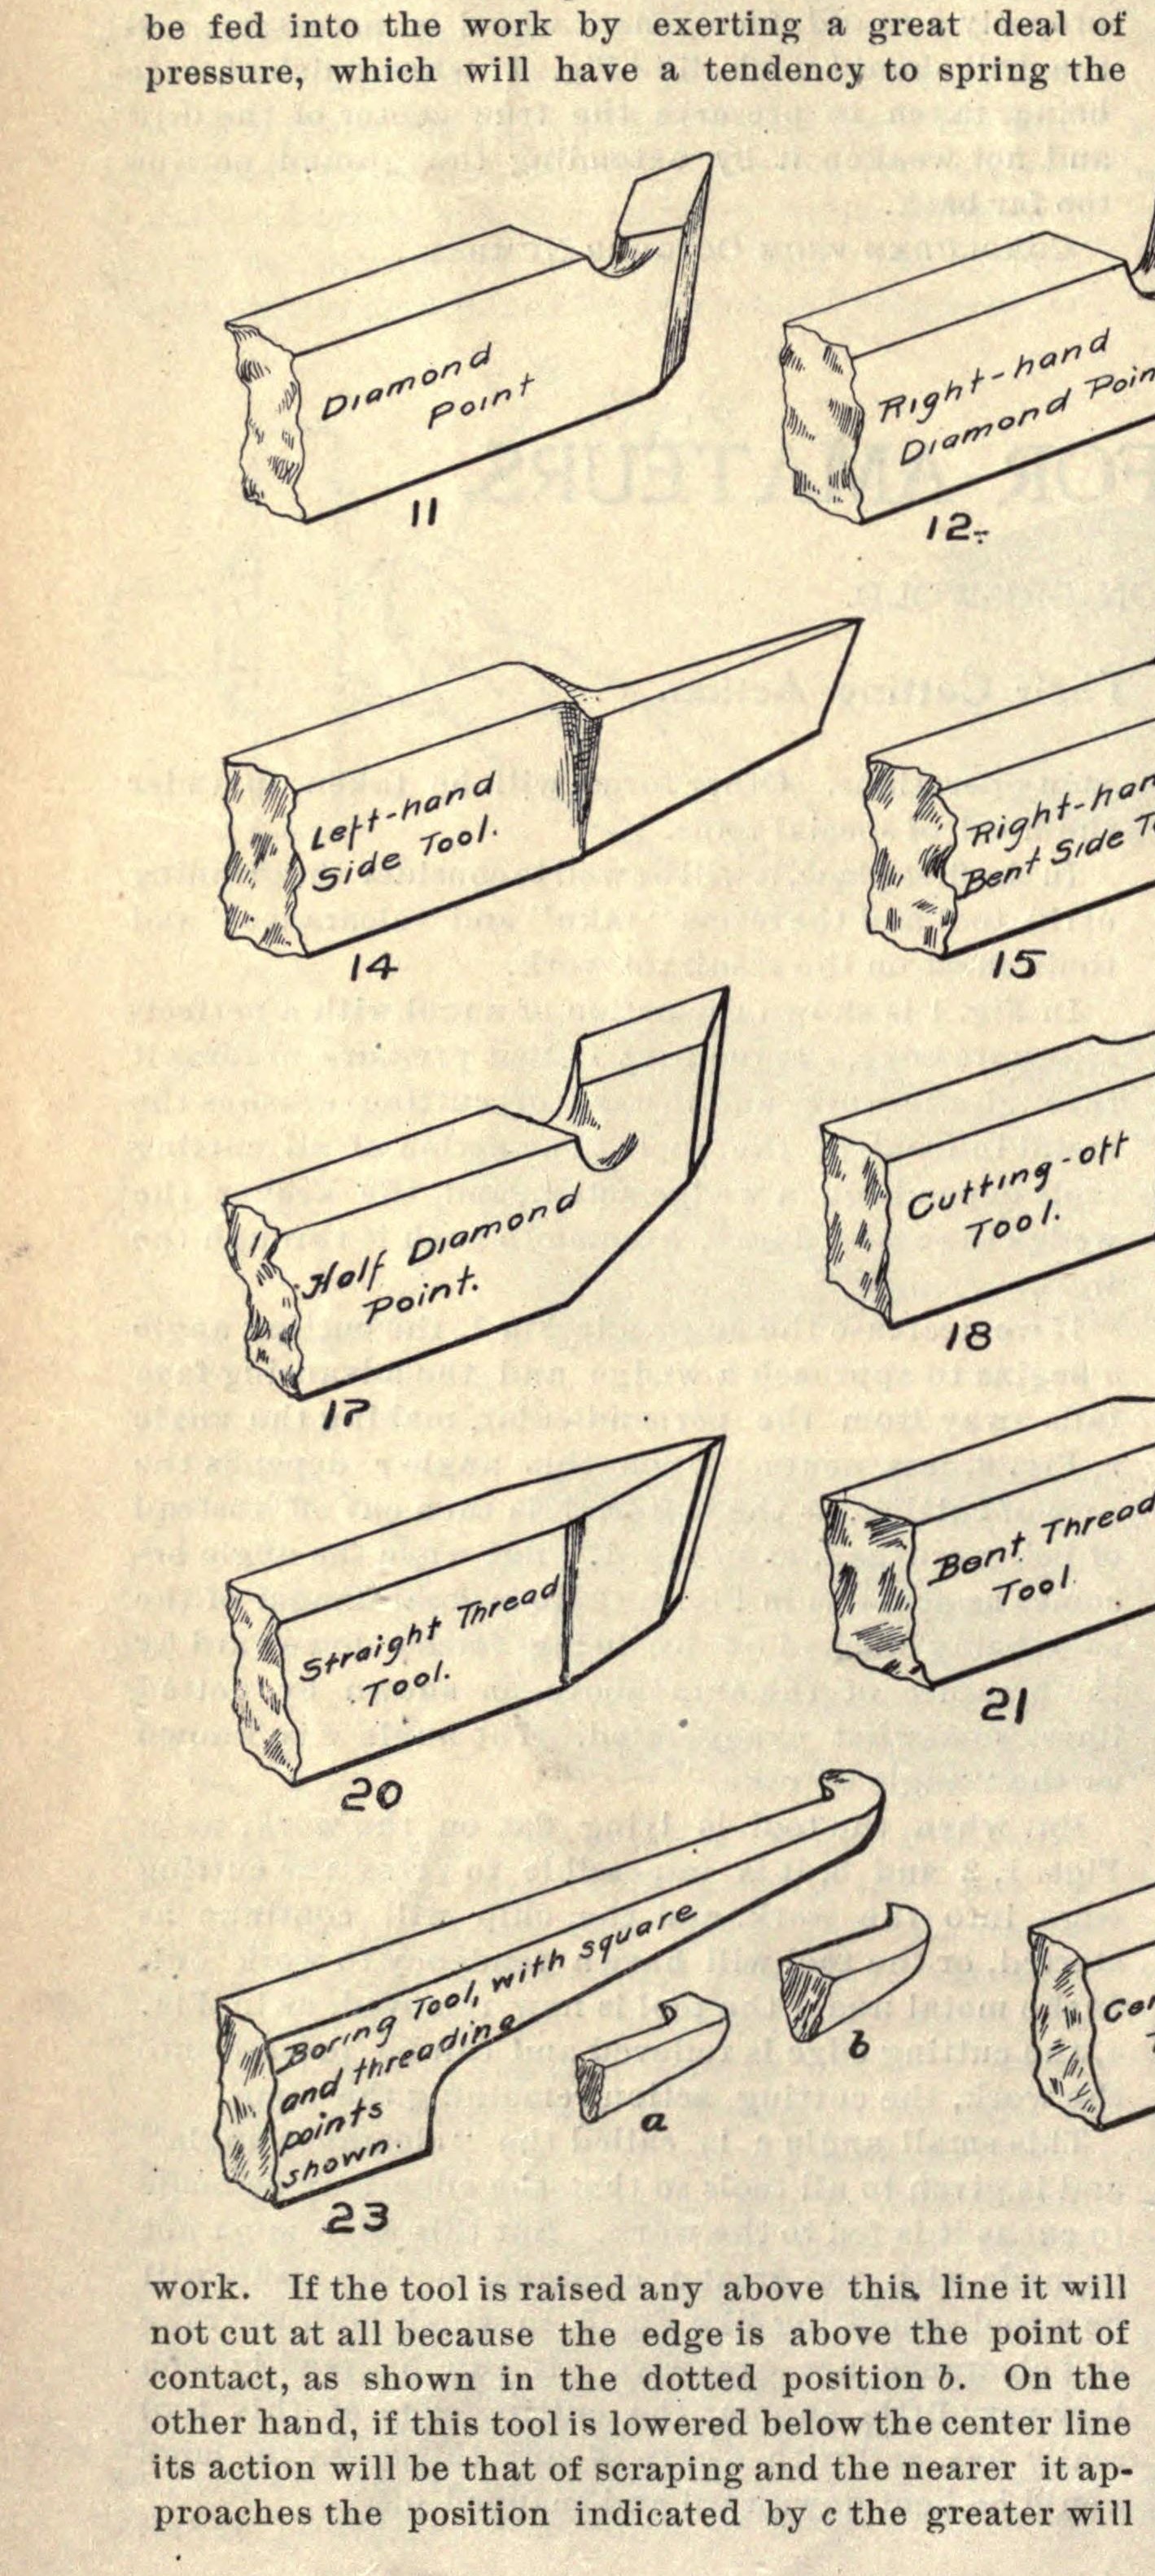

Forged Lathe Tools: Narrow Cutting-Off Tool and Bent-Tip Inside Boring Tool, Ground to Rake and Clearance (Griswold, 1904)
Two of the forged lathe tools in Robert Gibson Griswold's Tool Making for Amateurs (Boston, 1904): a cutting-off (parting) tool deep under a very narrow edge with relieved sides and a chip-splitting groove, and an inside boring and threading tool drawn to a long taper with the tip bent left; both ground to 3-5 degree clearance and the rake suited to the metal.
Zaawansowany
Half a day per tool
Instrukcje
1
1
His angles
His angles
Wczytywanie notatnika Jupyter…
2
2
Read Griswold
Read Griswold
"The writer uses a tool slightly less than 1-16 in. wide and 1 in. deep for short cuts."
3
3
Forge the cutting-off tool
Forge the cutting-off tool
Forge tool steel (stock size ours, to suit your tool post) into a blade deep under the cutting edge, with the point the widest part and the sides relieved behind it so it cannot bind (his fig. 18): slightly under 1/16 in. wide and 1 in. deep for work up to 1/2 in., about 3/32 in. wide for work up to 2 in.
Materiały do tego kroku:
 Pręt ze stali narzędziowej1 sztuka
Potrzebne narzędzia:
 Kuźnia kowalska
 Kowadło
 Młotek
 Szczypce kowalskie
4
4
Forge the boring tools
Forge the boring tools
Draw three blanks to a long tapering end and bend the extreme tip to the left (fig. 23).
Materiały do tego kroku:
Pręt ze stali narzędziowej1 sztukaPotrzebne narzędzia:
Kuźnia kowalskaKowadłoMłotekSzczypce kowalskie5
5
Harden and temper
Harden and temper
Carbon tool steel: harden the ends (ours: cherry red into water) and temper in the yellows. Self-hardening steel must never be quenched in water.
Materiały do tego kroku:
 Woda1 sztuka
 Płótno szmerglowe1 sztuka
Potrzebne narzędzia:
Kuźnia kowalska Wiadro
6
6
Grind the cutting-off tool
Grind the cutting-off tool
Give it front and side clearance of 3-5 degrees and little top rake. For larger work grind a round groove in the facing edge so the chip splits into two strings.
Potrzebne narzędzia:
 Szlifierka stołowa
7
7
Grind the boring points
Grind the boring points
Grind one boring tool as a diamond point, one as a small square point that works into corners, and one as a 60 degree thread point. Rake 3-10 degrees for iron and steel, little or none for brass and copper; hone the edges.
Potrzebne narzędzia:
Szlifierka stołowa Osełka
8
8
Troubleshooting
Troubleshooting
Lathe tool troubleshooting.
Flow
Loading...
9
9
History and honest limits
History and honest limits
From Robert Gibson Griswold, "Tool Making for Amateurs" IV, **Amateur Work** (Boston), vol. IV (1904-05), pp. 23-26 and figs. 11-25 (checked on the archive.org scan amateurwork04bostrich). He shows a full set (diamond point, side, round-nose, thread, centering, brass tools); this blueprint makes the two our heads need. Stock size and quench are ours.
Materiały
3- 1 sztukaZastępnik
- 1 sztukaZastępnik
- 1 sztukaZastępnik
Według tego planu powstaje
Powiązane blueprinty
Te blueprinty dzielą się wiedzą — technikami, materiałami lub zasadami
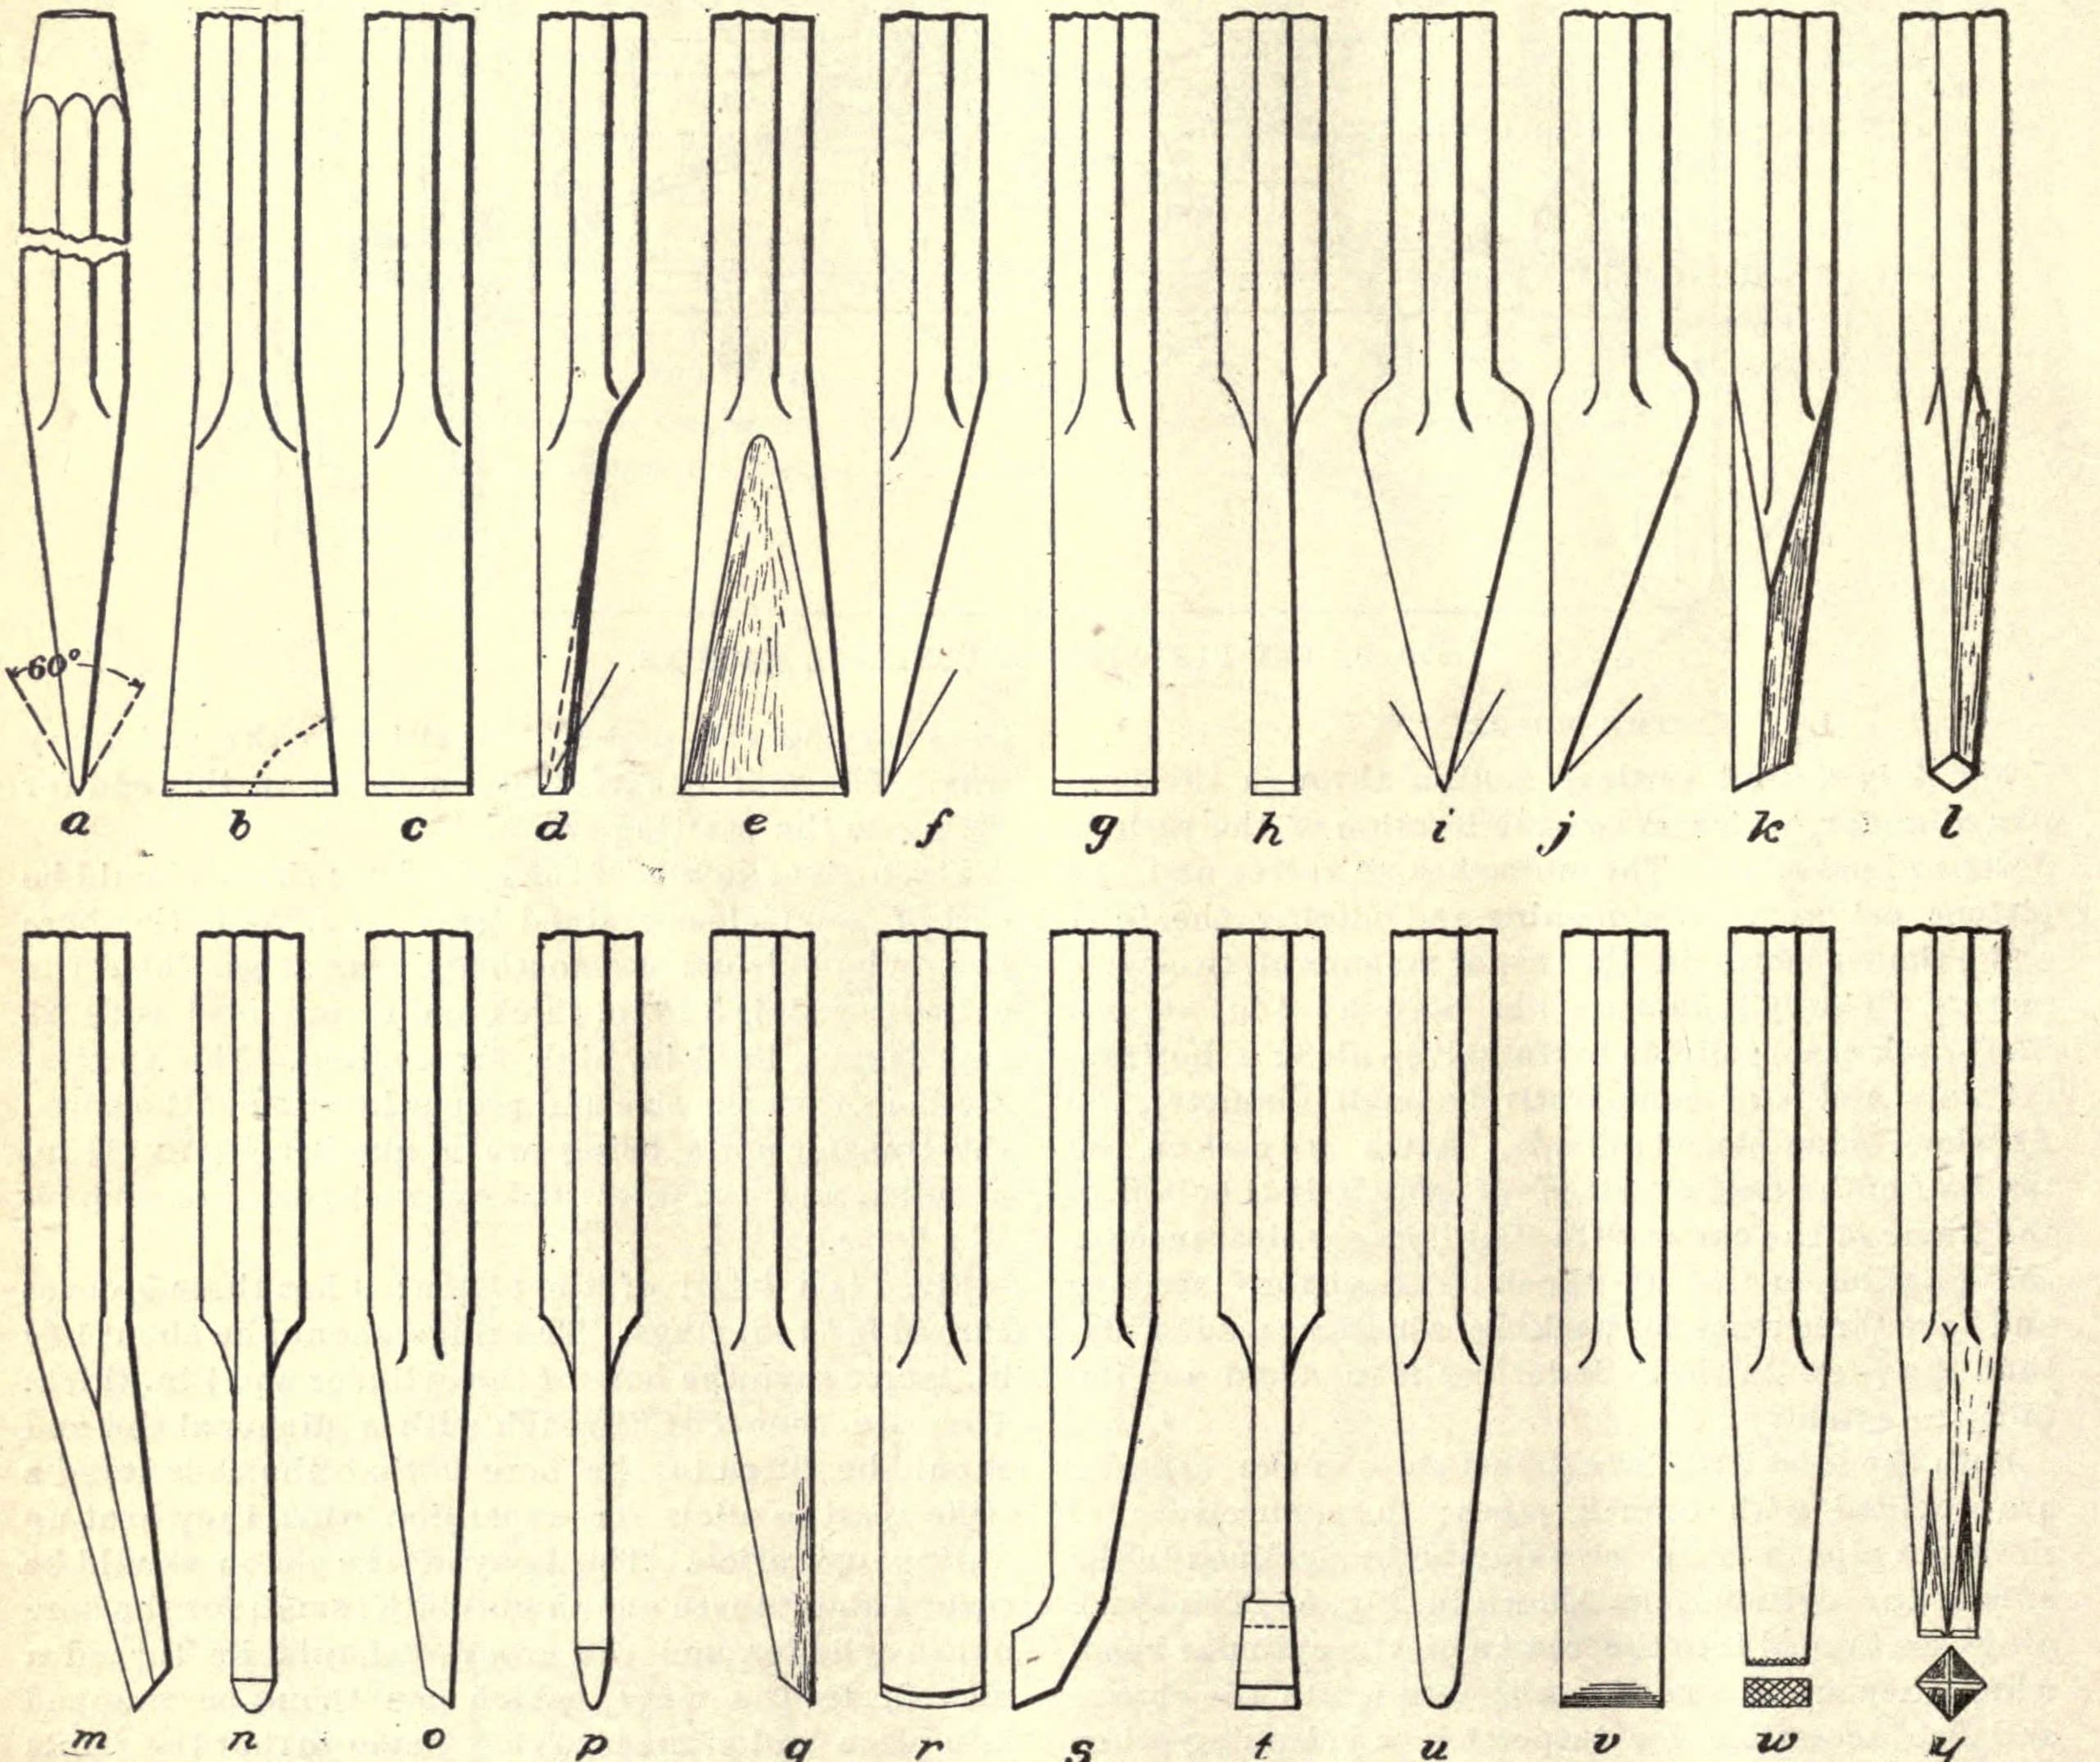
A Set of Cold Chisels: Flat, Gouge, Side, Cape, Diamond-Point and Round-Nose, Edge Hardened Only, Tempered Purple (Griswold, 1904)
autor: Forge
Obróbka metali
10
0
0
0
0
0
Half-Round Taper Reamer: Tool Steel Turned to the Taper, Filed Flat to the Centre Line, Hardened (Griswold, Amateur Work, 1905)
autor: Forge
Obróbka metali
9
0
0
0
0
0
CC0 Domena publiczna
Ten plan jest udostępniany na licencji CC0. Możesz go swobodnie kopiować, modyfikować, rozpowszechniać i wykorzystywać do dowolnych celów, bez konieczności uzyskiwania zgody.
Wesprzyj Makera kupując produkty przez jego plan, za co zarabia Prowizja Makera ustalony przez sprzedawców, lub stwórz nową iterację tego planu i dołącz go jako połączenie w swoim własnym planie, aby dzielić się przychodami.