Współpraca
SZTUKA
Piękno i dobre samopoczucie
RZEMIOSŁO
KULTURA I HISTORIA
ROZRYWKA
ŚRODOWISKO
JEDZENIE I NAPOJE
INŻYNIERIA ODWROTNA
NAUKI
LEKKOATLETYKA
TECHNOLOGIA
URZĄDZENIA DO NOSZENIA
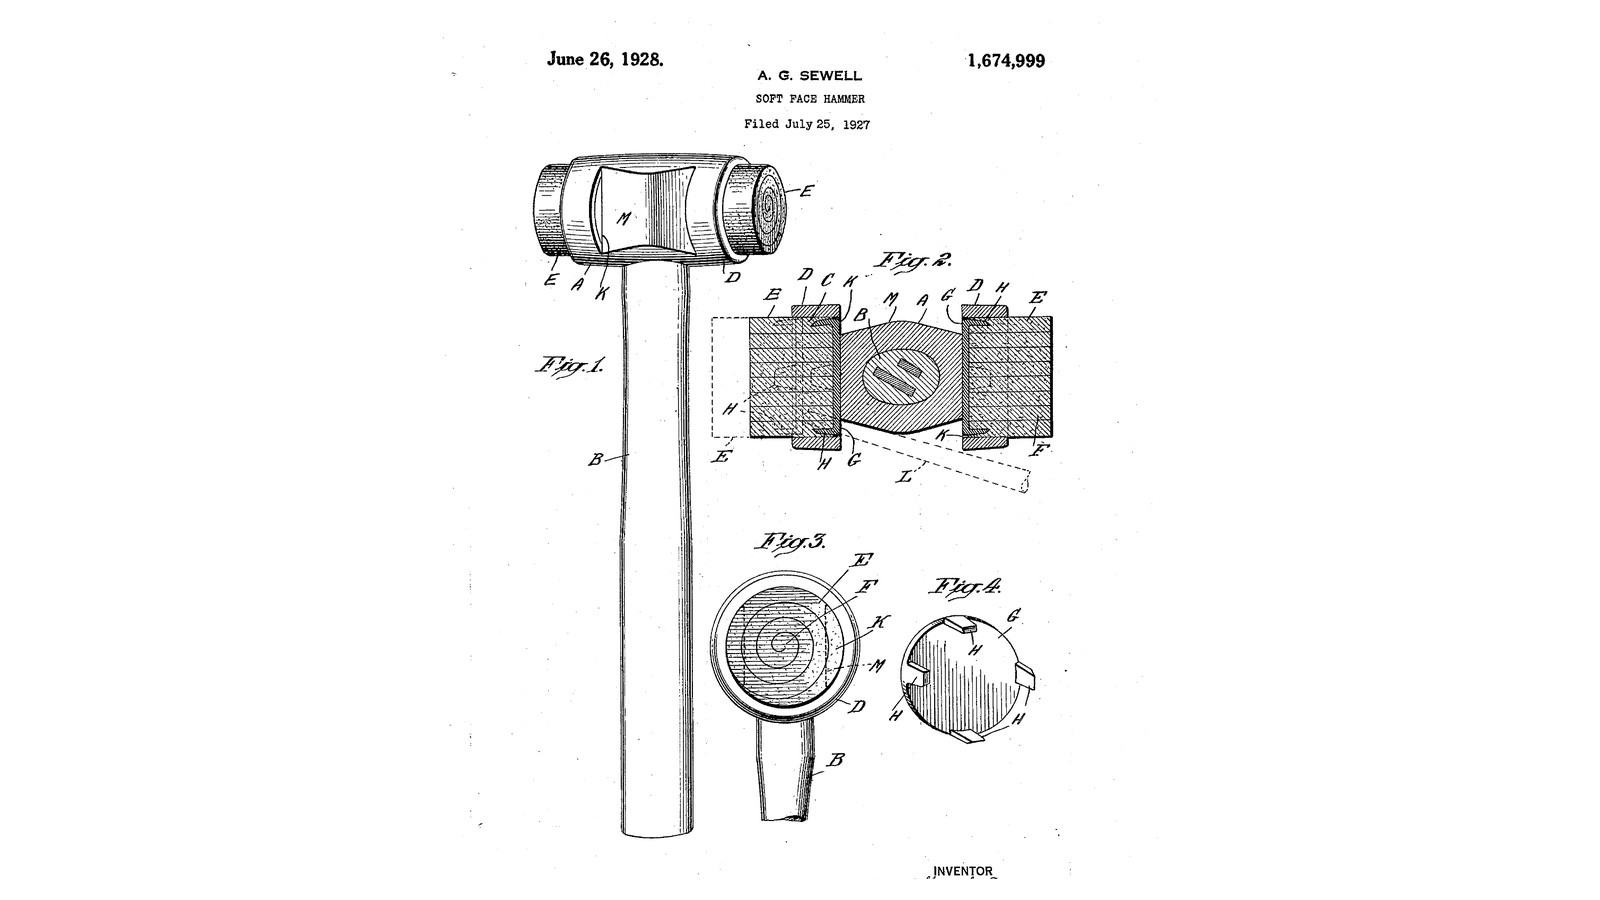


Renewable Rubber-Face Hammer: Rolled Faces Pressed Onto Pronged Discs, Driven Out Through a Notch When Worn (Sewell, 1928)
Albert G. Sewell received US 1,674,999, dated 26 June 1928, for a soft-face hammer whose worn faces can be renewed instead of throwing the hammer away. Each end of the head is a cup. A face rolled from a strip is pressed into the cup onto a loose sheet-metal disc whose prongs bite into it and wedge it tight. When a face is battered, a rod pushed through a notch at the bottom of the cup drives the disc and the face out together, and a new face goes in. He preferred rawhide and named rubber among face materials; ours are rolled from rubber sheet.
The patent gives no sizes; every size here is ours.
Średniozaawansowany
About 1 day
Instrukcje
1
1
Rolling a face plug
Rolling a face plug
Wczytywanie notatnika Jupyter…
2
2
Read US 1,674,999
Read US 1,674,999
"Thus, by hammering or otherwise thrusting a rod or suitable device against the wedging member, the latter, with the striking face member, can be forced or driven out of the socket or recess, after which a new striking face member may be forced into the socket, to be secured therein by the wedging member."
3
3
Turn the head
Turn the head
Grip 40 mm steel round bar in the chuck and turn a head 110 mm long: the two ends stay 40 mm across for 26 mm as the flanges D, and the middle is waisted to 30 mm. Bore each end 32 mm across and 22 mm deep for the sockets C, flat at the bottom. Drill a 20 mm eye B through the middle, square to the axis, in a V-block on the drill press.
Materiały do tego kroku:
 Pręt okrągły ze stali niskowęglowej1 sztuka
 Olej do cięcia1 sztuka
Potrzebne narzędzia:
 Tokarka do metalu
 Uchwyt tokarski 3-szczękowy
 Nóż tokarski
 Wytaczadło
 Przecinak tokarski
 Wiertarka stołowa
 Pryzma traserska
 Zestaw wierteł
 Suwmiarka cyfrowa 6 cali
 Okulary ochronne
4
4
Cut the notches K
Cut the notches K
On the handle's side of each flange, saw and file a notch 8 mm wide through the flange's wall at the very bottom of the socket, so a rod can be pushed in at a slant against the edge of the disc at the bottom.
Potrzebne narzędzia:
 Imadło warsztatowe
 Piła do metalu
 Zestaw pilników
 Punktak
5
5
Pronged discs G
Pronged discs G
Cut two discs of 1.5 mm steel sheet 31.5 mm across. At four places round each rim, snip two cuts 6 mm deep 5 mm apart and bend the tab between them up at a right angle with the pliers: the prongs H. Drop one disc loosely into the bottom of each socket, prongs out.
Materiały do tego kroku:
 Blacha ze stali miękkiej1 sztuka
Potrzebne narzędzia:
 Nożyce do blachy
 Szczypce płaskieImadło warsztatoweZestaw pilników
6
6
Roll and press in the faces E
Roll and press in the faces E
Cut two strips of 3 mm natural rubber sheet 32 mm wide and about 270 mm long. Roll each tightly into a coil, trimming the strip until the coil just enters a socket, and tie it. Press the coil into its socket in the vice, between soft packing, until it bottoms on the disc and its prongs bite in, leaving the face standing about 10 mm out. Cut the tie and trim the face flat with the knife.
Materiały do tego kroku:
 Płyta z kauczuku naturalnego1 sztuka
Potrzebne narzędzia:
 Nóż introligatorskiImadło warsztatoweSuwmiarka cyfrowa 6 cali
7
7
Handle
Handle
Turn an ash handle 300 mm long, its end a tight fit in the eye. Saw a slot down its end, drive it into the eye, and glue and drive a hardwood wedge into the slot; saw it off flush.
Materiały do tego kroku:
 Deska z drewna liściastego1 sztuka
 Klej do drewna1 sztuka
Potrzebne narzędzia:
 Tokarka do drewna
 Zestaw dłut tokarskich (HSS)Piła do metalu
 Młotek ślusarski z kulistym rąbem
8
8
Renew a face
Renew a face
When a face is worn, push a steel rod through the socket's notch against the disc's edge and tap it out with the hammer; the disc and the face come out together. Put the disc back, prongs out, and press in a new rolled face.
Potrzebne narzędzia:
Młotek ślusarski z kulistym rąbemImadło warsztatowe9
9
Troubleshooting
Troubleshooting
Soft-face hammer troubleshooting.
Flow
Loading...
10
10
History and honest limits
History and honest limits
**Albert G. Sewell**, US 1,674,999, dated 26 June 1928, filed 25 July 1927. He describes a head with a socket at each end formed by annular flanges, a striking face member of relatively soft material rolled from a strip and pressed in as a plug, a loose sheet-metal wedging disc with prongs in the socket's bottom, and openings through which a rod drives the disc and face out. He preferred rawhide and his head was cast iron; ours is turned steel with faces rolled from rubber sheet, which he lists among the face materials in use. He gives no sizes; every size here is ours.
Materiały
6- Zastępnik
- 1 sztukaZastępnik
- 1 sztukaZastępnik
- 1 sztukaZastępnik
- 1 sztukaZastępnik
- 1 sztukaZastępnik
Wymagane narzędzia
20- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
Według tego planu powstaje

Powiązane blueprinty
Te blueprinty dzielą się wiedzą — technikami, materiałami lub zasadami
CC0 Domena publiczna
Ten plan jest udostępniany na licencji CC0. Możesz go swobodnie kopiować, modyfikować, rozpowszechniać i wykorzystywać do dowolnych celów, bez konieczności uzyskiwania zgody.
Wesprzyj Makera kupując produkty przez jego plan, za co zarabia Prowizja Makera ustalony przez sprzedawców, lub stwórz nową iterację tego planu i dołącz go jako połączenie w swoim własnym planie, aby dzielić się przychodami.