
Współpraca
SZTUKA
Piękno i dobre samopoczucie
RZEMIOSŁO
KULTURA I HISTORIA
ROZRYWKA
ŚRODOWISKO
JEDZENIE I NAPOJE
INŻYNIERIA ODWROTNA
NAUKI
LEKKOATLETYKA
TECHNOLOGIA
URZĄDZENIA DO NOSZENIA
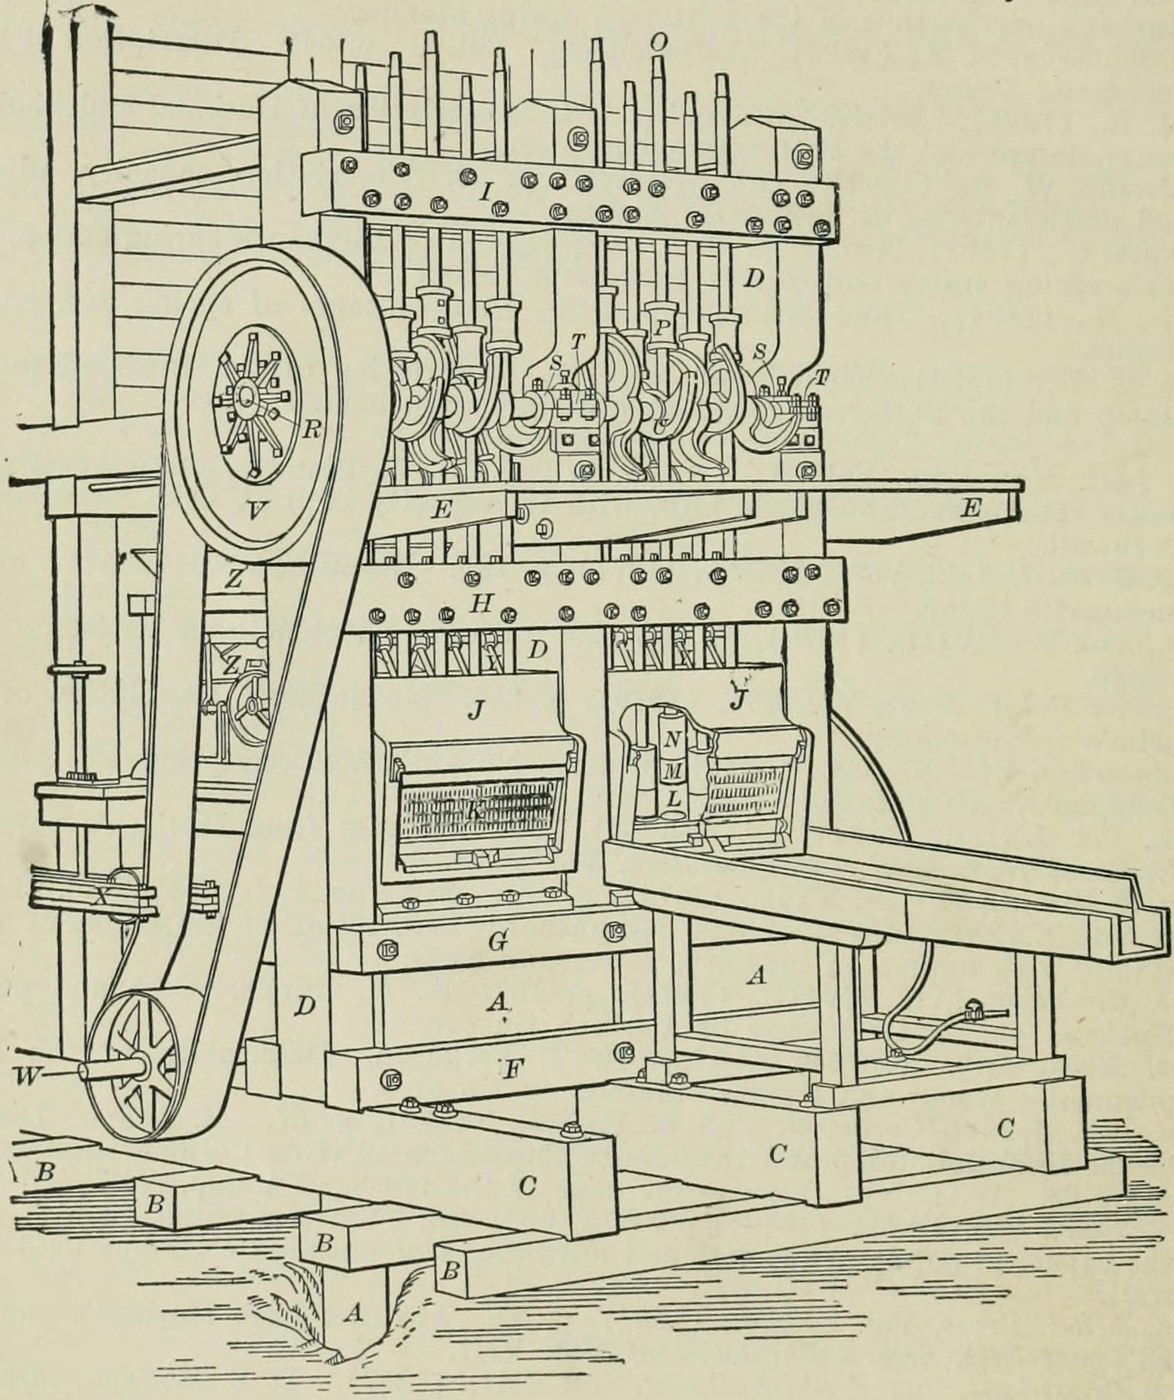
Stamp Mill: California Five-Stamp Battery (Richards, Ore Dressing 1903)
Forge

Autor

Forge

3. listopad 2026NO
15
0
0
0
0

Stamp Mill: California Five-Stamp Battery (Richards, Ore Dressing 1903)

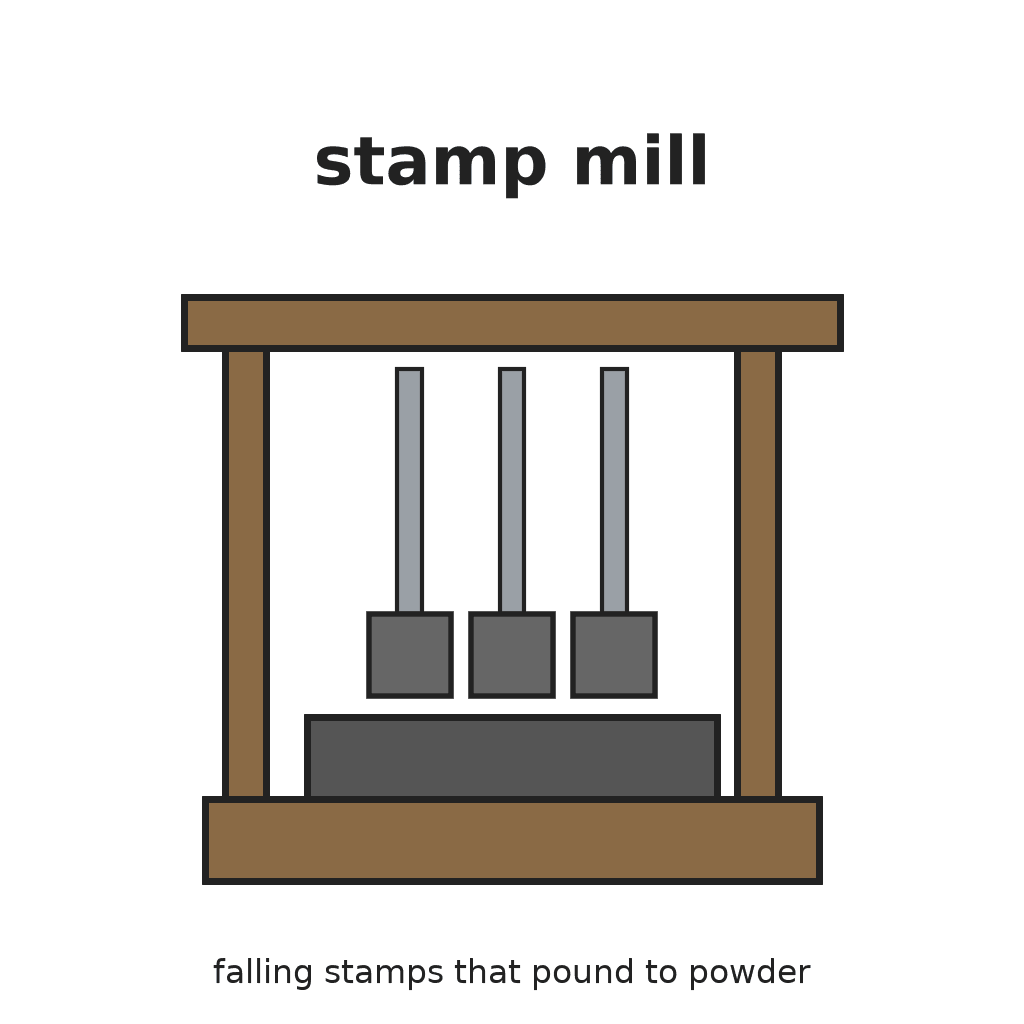
The gravity stamp mill: five heavy iron stamps stand in a cast-iron mortar on a timber block. Cams on a turning shaft lift each stamp by its tappet and let it fall by its own weight onto the ore on a die. Water washes the crushed ore out through a screen. Result: a stamp battery that pounds ore to sand, at 80 to 110 drops a minute. Source: R. H. Richards, Ore Dressing, vol. I (1903), Chapter V, Gravity Stamps. Unknown: one complete set of sizes; Richards gives the range found in the mills. Picture: Fig. 90 of the book.
Zaawansowany
Unknown

Instrukcje

1

Dig and level the foundation

Dig a trench in gravel, or blast one in rock, about 2 feet longer than the mortar block at each end and about 2 feet wider at each side. Level the bottom with tamped concrete, sand or clay. Concrete should be at least 30 inches thick, or it may crumble. Two layers of 2-inch plank spiked together may go on top.

Materiały do tego kroku:

BetonBeton1 levelling layer
Deska tartaDeska tarta1 two layers of 2-inch plank

Potrzebne narzędzia:
SzpadelSzpadel
MłotekMłotek
2

Stand the mortar block

Stand timbers or planks on end in the trench as the mortar block, sized for one five-stamp mortar. The mills used everything from 30 x 30 inch squared timbers to 2 x 12 inch planks bolted together. Set vertical bolts 3 to 4 feet long into the block to hold the mortar down. Not given: the bolts' metal.

Materiały do tego kroku:

Drewno kantoweDrewno kantowe1 mortar block
Nieznany metalNieznany metal1 hold-down bolts

Potrzebne narzędzia:
Zestaw kluczy płaskichZestaw kluczy płaskich
Nieznane wymiaryNieznane wymiary
3

Build the frame

On mud sills and cross sills, stand the posts (end posts 12 x 24 inches in most mills) with buckstaves, a platform, and lower and upper guide timbers. The guides keep the stamp stems vertical. Fit finger bars on a jack shaft between the posts, so each stamp can be propped up under its tappet. The frame carries the cam shaft and the drive.

Materiały do tego kroku:

Drewno kantoweDrewno kantowe1 sills, posts, guide timbers, platform
Nieznany metalNieznany metal1 bolts and jack shaft

Potrzebne narzędzia:

Zestaw kluczy płaskichZestaw kluczy płaskich
Nieznane wymiaryNieznane wymiary
4

Set the mortar, dies and screen

Bed the cast-iron mortar on tarred blankets or sheet rubber on the mortar block, for an even bearing, and bolt it down. Put the dies in its bottom: cylinders on square foot plates that fill the floor of the mortar. Mount a screen of punched Russia sheet iron in a wooden frame over the opening in front.

Materiały do tego kroku:

Odlewy żeliwneOdlewy żeliwne1 mortar and five dies
Płyta z kauczuku naturalnegoPłyta z kauczuku naturalnego1 packing
Blacha żelazna rosyjskaBlacha żelazna rosyjska1 screen

Potrzebne narzędzia:

Zestaw kluczy płaskichZestaw kluczy płaskich
5

Make the five stamps

Each stamp has four parts. The shoe is chilled cast iron, its butt cast in heavy chills and its shank in sand. The boss is tough cast iron, the shoe's diameter and often 18 inches long, with sockets for the shoe shank and the stem and two keyways for knock-out wedges. The stem is solid wrought iron or mild steel, turned true and tapered at both ends so it can be reversed. The tappet is cast iron, with a flange above and below, locked on the stem by a gib and keys. Put the extra weight in the boss. Louis designs for 11 to 14 pounds of stamp per square inch of die; the mills used stamps of 650 to 1,100 pounds.

Materiały do tego kroku:

Odlewy żeliwneOdlewy żeliwne1 shoes, bosses, tappets
Pręt z kutego żelazaPręt z kutego żelaza1 stems, gibs, keys

Potrzebne narzędzia:

Tokarka do metaluTokarka do metalu
Nieznane wymiaryNieznane wymiary
6

Fit the cam shaft and drive

Turn a wrought-iron or steel cam shaft true, with a key seat, and key on five cams. Each cam usually has two arms with spiral lifting faces, cast iron with chilled faces or cast steel. Drive the shaft by a rubber belt from the main shaft, over a pulley of wood built on a cast-iron hub and flanges, with a tightener. Not given: the engine or wheel that turns the main shaft.

Materiały do tego kroku:

Pręt z kutego żelazaPręt z kutego żelaza1 cam shaft
Odlewy żeliwneOdlewy żeliwne1 cams, pulley hub and flanges
Deska tartaDeska tarta1 pulley rim
Pas napędowyPas napędowy1 rubber belt

Potrzebne narzędzia:

Tokarka do metaluTokarka do metalu
Zestaw kluczy płaskichZestaw kluczy płaskich
7

Add the water and the feed

Run one or two 1-inch water pipes into the back of the mortar, each with a plug cock that stays where it is set. Feed ore from the bin by a chute to an automatic feeder. One stamp trips the feeder when the ore layer on its die gets too thin, and a hand screw adjusts the point where it trips. Ore can also be fed by hand with a shovel.

Materiały do tego kroku:

Rura wodociągowaRura wodociągowa1 water pipes
Nieznany zawórNieznany zawór1 plug cocks
Nieznany metalNieznany metal1 feeder and chute

Potrzebne narzędzia:

Zestaw kluczy płaskichZestaw kluczy płaskich

ŁopataŁopata
8

Set up each stamp

Lay a 3-inch plank on the dies and set the bosses on it. Lower the stems into them and tap each stem down with a hammer, a board guarding its top, then drop it a few times at a very low drop. Hoist the stamp, put the shoe in place with wooden staves around its shank, and drop it on the plank to drive the shoe home; the staves swell when wet and hold it. Swap the plank for a block as high as the drop. Slip the tappet on, turn the cam until the tappet rests on its point, drive the keys home and drop the stamp gently a few times.

Materiały do tego kroku:

Kliny drewnianeKliny drewniane1 staves

Potrzebne narzędzia:

Deska tartaDeska tarta
MłotekMłotek
WielokrążekWielokrążek
9

Run the battery

Drop the stamps in order 1, 3, 5, 2, 4 (numbered from the left, standing behind the battery), so no two neighbours fall one after the other. The California practice is 80 to 110 drops a minute with a 5 to 9 inch drop. The cams turn the stamps as they lift, which evens out wear on shoes and dies. Lubricate the cams; soft soap with graphite is best. As shoes and dies wear, reset the tappets to restore the drop, and keep the height of discharge, from die to screen, the same.

Potrzebne narzędzia:

Proszek grafitowyProszek grafitowy
Nieznany materiałNieznany materiał
Zestaw kluczy płaskichZestaw kluczy płaskich

Materiały

12

Wymagane narzędzia

10

Według tego planu powstaje

CC0 Domena publiczna

Ten plan jest udostępniany na licencji CC0. Możesz go swobodnie kopiować, modyfikować, rozpowszechniać i wykorzystywać do dowolnych celów, bez konieczności uzyskiwania zgody.

Wesprzyj Makera kupując produkty przez jego plan, za co zarabia Prowizja Makera ustalony przez sprzedawców, lub stwórz nową iterację tego planu i dołącz go jako połączenie w swoim własnym planie, aby dzielić się przychodami.

Dyskusja

(0)

Zaloguj się aby dołączyć do dyskusji

Ładowanie komentarzy...