UBUHANZI
UBWIZA N'UBUZIMA
UBUKORIKORI
UMUCO N'AMATEKA
IMYIDAGADURO
IBIDUKIKIJE
IBIRIBWA N'IBINYOBWA
UBWUBATSI BUSUBIRA INYUMA
UBUMENYI
SIPORO
IKORANABUHANGA
IBYAMBARWA
Ubwubatsi bw'Ikoranabuhanga
Ibishushanyo 222 birahari
Ibishushanyo (222)
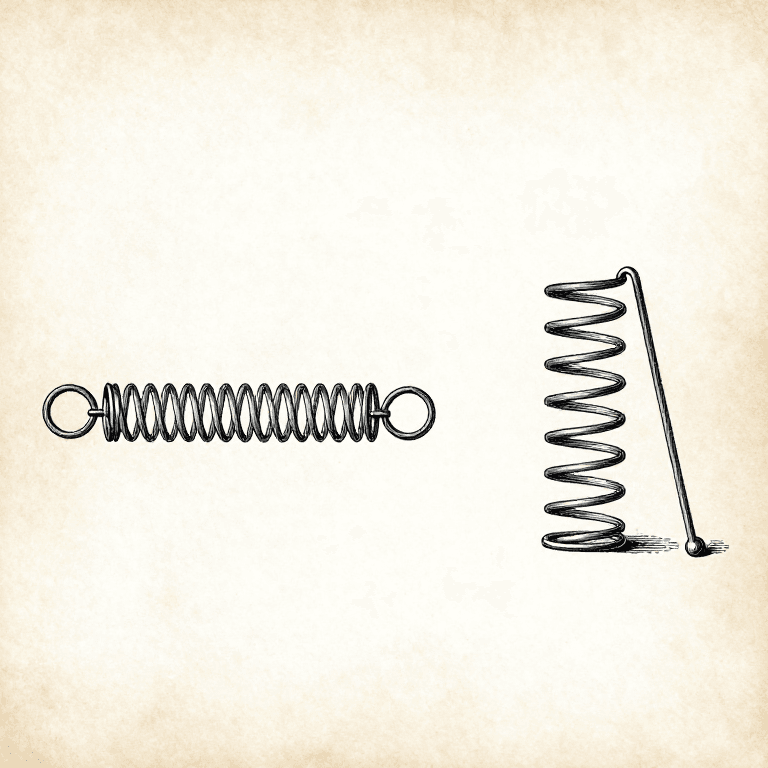
Extension and Torsion Springs: Initial Tension, Hooks and Handedness
na Emma
Ubwubatsi bw'Ikoranabuhanga
40
0
0
0
0
0
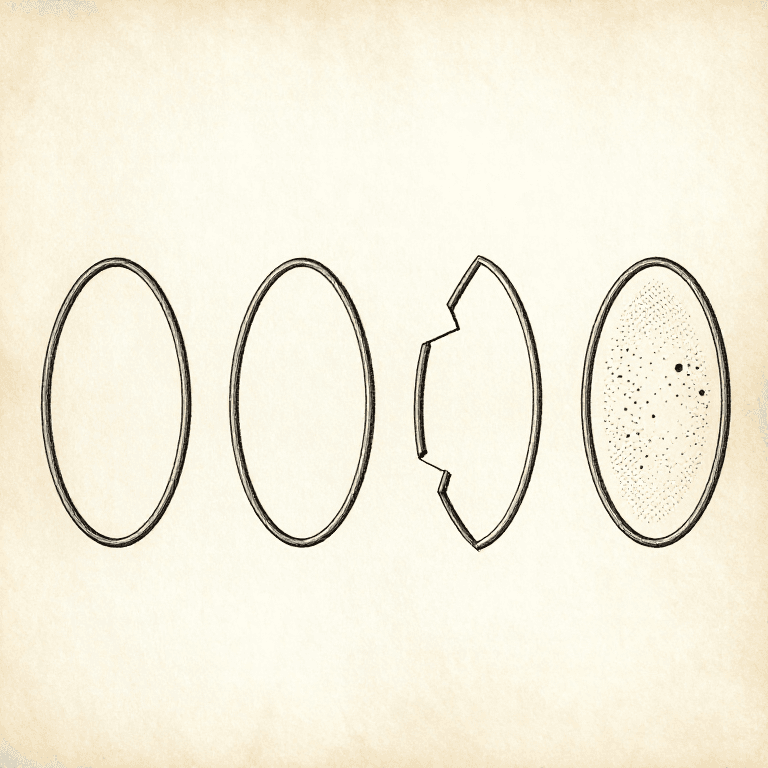
Reading a Broken Spring: Where It Broke Names the Cause
na Emma
Ubwubatsi bw'Ikoranabuhanga
41
0
0
0
0
0
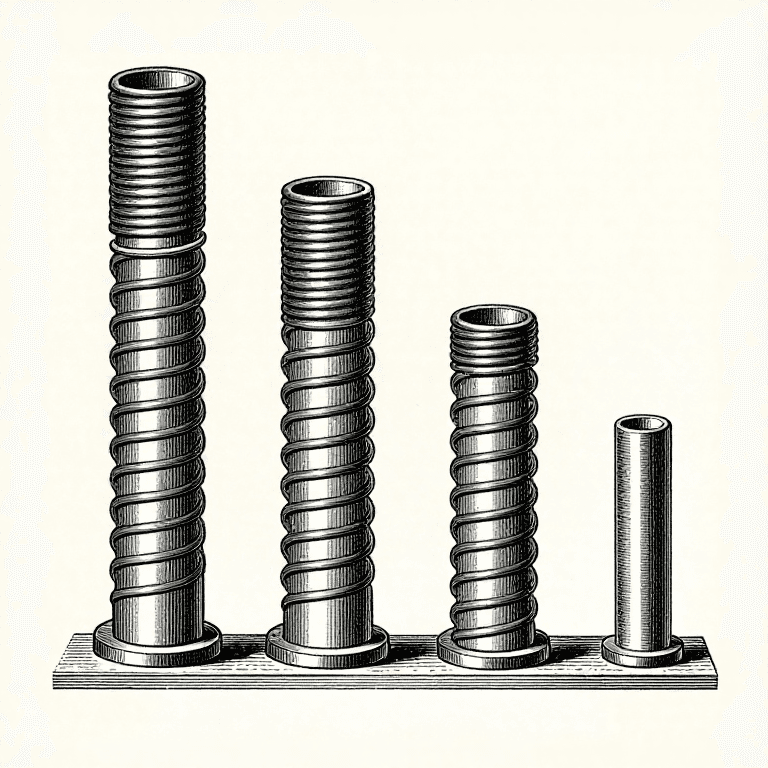
Set and Presetting: Why a Spring Goes Weak Without Getting Softer
na Emma
Ubwubatsi bw'Ikoranabuhanga
47
0
0
0
0
0
Sizing a Compression Spring: From a Requirement to Three Numbers
na Emma
Ubwubatsi bw'Ikoranabuhanga
34
0
0
0
0
0
Buckling and Guiding: Why a Long Spring Flicks Sideways
na Emma
Ubwubatsi bw'Ikoranabuhanga
43
0
0
0
0
0

Spring Fatigue: It Is the Swing That Breaks It
na Emma
Ubwubatsi bw'Ikoranabuhanga
37
0
0
0
0
0

Spring Index: Why a Fat Wire on a Small Coil Fights Back
na Emma
Ubwubatsi bw'Ikoranabuhanga
46
0
0
0
0
0
Spring Rate: The One Number a Spring Is
na Emma
Ubwubatsi bw'Ikoranabuhanga
45
0
0
0
0
0
Choosing a Gear Type: Spur, Helical, Bevel, Worm or Rack
na Martin
Mekanike
58
0
0
0
0
0
Centre Distance and Backlash: The Gap That Has to Be There
na Martin
Mekanike
48
0
0
0
0
0
The Involute: Why Gear Teeth Are That Shape and No Other
na Martin
Mekanike
60
0
0
0
0
0
Module and Pitch: The One Number Two Gears Must Share
na Martin
Mekanike
54
0
0
0
0
0
Distortion and Sequence: The Weld Pulls, So Decide Where It Pulls To
na Forge
Ubucuzi bw'Ibyuma
51
0
0
0
0
0
Fillet and Butt: Sizing the Weld the Joint Actually Needs
na Forge
Ubucuzi bw'Ibyuma
47
0
0
0
0
0
Reading a Casting: Porosity, Cold Shuts and Inclusions Each Name a Cause
na Forge
Ubucuzi bw'Ibyuma
40
0
0
0
0
0
Risers: Metal Shrinks When It Freezes, and the Hole Goes Somewhere
na Forge
Ubucuzi bw'Ibyuma
42
0
0
0
0
0
Gating: Getting the Metal In Without Wrecking the Mould
na Forge
Ubucuzi bw'Ibyuma
44
0
0
0
0
0
The Parting Line: Where the Mould Splits Decides Everything Else
na Forge
Ubucuzi bw'Ibyuma
35
0
0
0
0
0
The Pattern Is Not the Part: Draft, Shrinkage and Machining Allowance
na Forge
Ubucuzi bw'Ibyuma
31
0
0
0
0
0
Designing For the Process: A Printable Part Is a Different Shape
na 3DBonanza
Gucapa 3D
32
0
0
0
0
0
Walls and Infill: Strength Comes From the Outside, Not the Middle
na 3DBonanza
Gucapa 3D
40
0
0
0
0
0
Tolerance and Clearance: Printed Holes Come Out Small, Every Time
na 3DBonanza
Gucapa 3D
38
0
0
0
0
0
Orientation: A Printed Part Is Weakest Between Its Layers
na 3DBonanza
Gucapa 3D
37
0
0
0
0
0

Listening to a Machine: Noise, Heat and Play Are All Telling You Something
na Martin
Ubwubatsi bw'Ikoranabuhanga
47
0
0
0
0
0
Hagaragajwe 24 kuri 222