UBUHANZI
UBWIZA N'UBUZIMA
UBUKORIKORI
UMUCO N'AMATEKA
IMYIDAGADURO
IBIDUKIKIJE
IBIRIBWA N'IBINYOBWA
UBWUBATSI BUSUBIRA INYUMA
UBUMENYI
SIPORO
IKORANABUHANGA
IBYAMBARWA
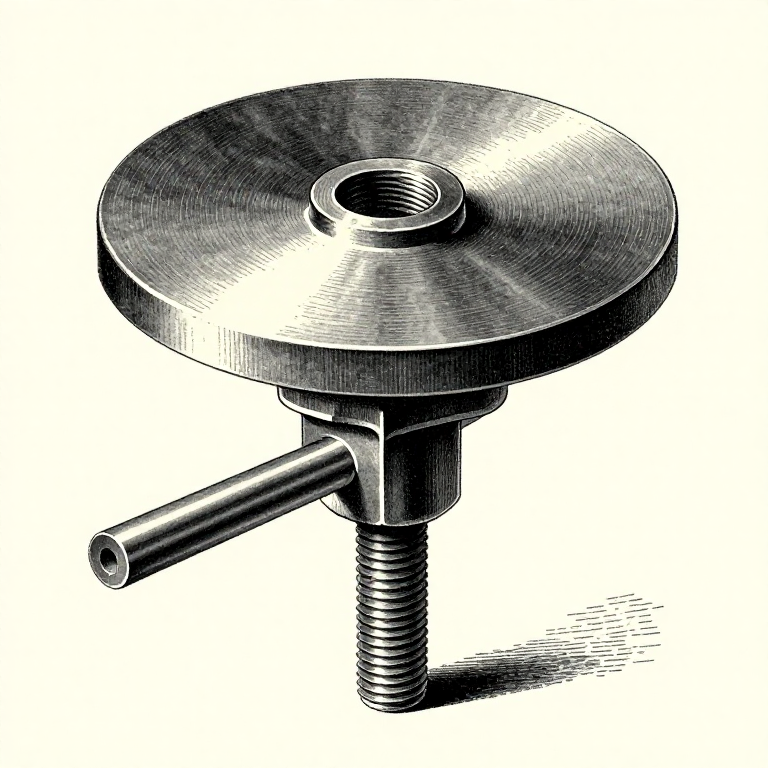

Cutting a Thread with a Die: Making Your Own Bolt
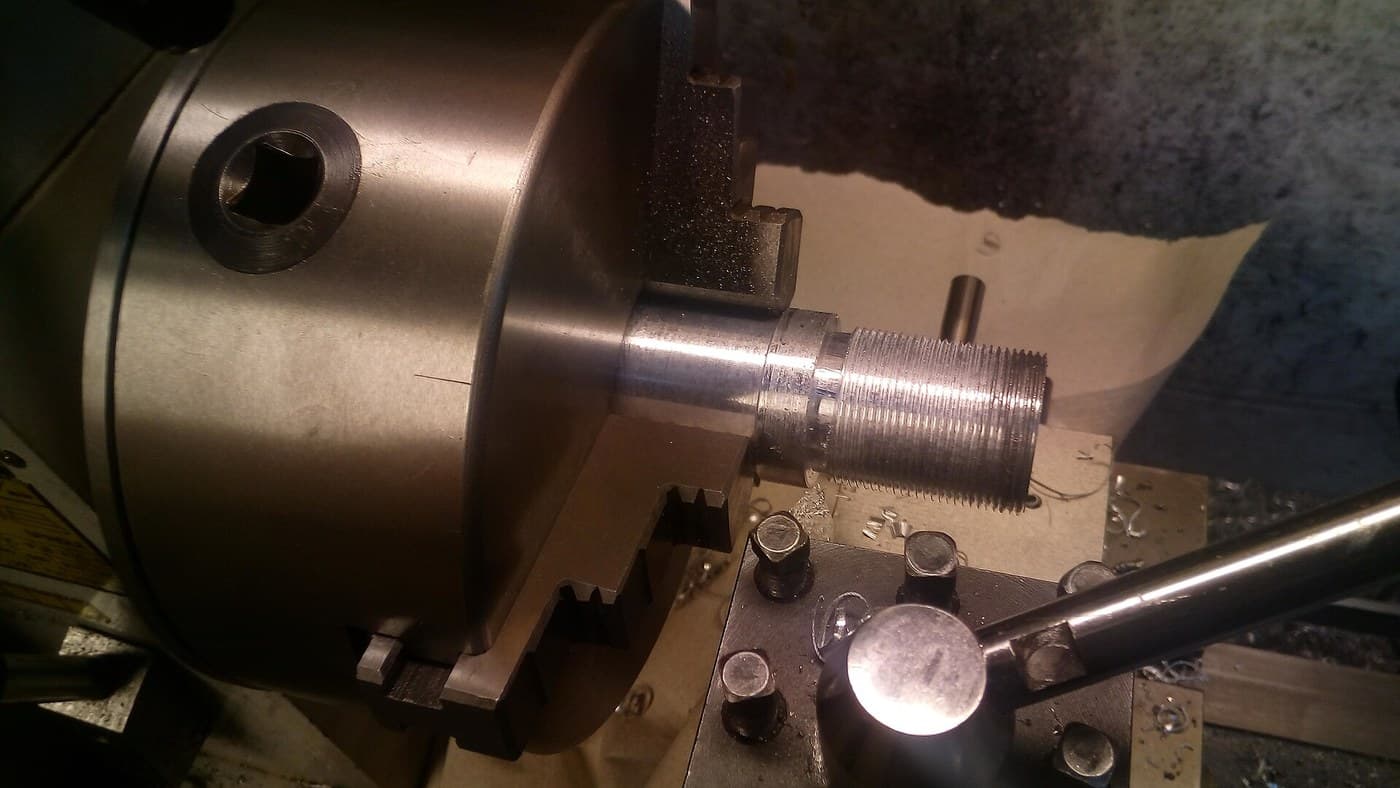
A die cuts a thread onto the outside of a bar — the mirror of what a tap does inside a hole, and the way to make a bolt, a stud or a threaded rod in exactly the length you need.
It is more forgiving than tapping in one way and less in another. A die cannot break off inside anything, so the worst outcome is a spoiled bar. But getting it square is harder, because there is no hole to guide it — the die will happily start at an angle and cut a drunken thread.
The preparation matters more than the cutting: the bar has to be the right size and it has to be chamfered.
Hagati
3 hours
Amabwiriza
1
1
The bar must be slightly UNDER nominal
The bar must be slightly UNDER nominal
An M8 thread wants a bar of about 7.8 to 7.9 mm, not 8.0. Commercial round bar sold as 8 mm is usually a little under already, which is why it works.
A bar at full nominal diameter forces the die to remove metal right at the crest of the thread, where it has the least clearance. The result is a tight, rough thread, high cutting torque, and a crest that tears rather than cuts. Turning or filing a few hundredths off first transforms the job.
Measure before you start. Bar stock varies, and a bar that is a tenth of a millimetre oversize is the difference between a die that cuts sweetly and one that has to be forced.
Ibikoresho by'iyi ntambwe:
 Umutsi w'icyuma cyoroshye1 igice
Ibikoresho bikenewe:
 Kalipe ya Vernier
 Amakariso (Ikariso ry'Intoki)
 Igifata gikomeye cy'ameza y'akazi
2
2
Chamfer the end — always
Chamfer the end — always
File or grind a 45 degree chamfer on the end of the bar, down to roughly the thread's minor diameter. The die then has a tapered surface to sit on and centres itself.
Without a chamfer, the die meets a flat square end and has nothing to align against. It will start crooked, and a crooked start on a die cannot be corrected at all — the thread that follows simply repeats the error down the bar.
The chamfer also becomes the lead-in of the finished thread, which is what lets the bolt start easily into a nut. A bolt with no chamfer is difficult to start and is the commonest cause of cross-threading.
Ibikoresho by'iyi ntambwe:
Umutsi w'icyuma cyoroshye1 igiceIbikoresho bikenewe:
Amakariso (Ikariso ry'Intoki)Igifata gikomeye cy'ameza y'akaziKalipe ya Vernier3
3
Which way up, and starting square
Which way up, and starting square
A die has a lead on ONE face — the first few threads are tapered — and that face goes against the work. Look for it; it is usually the side without the printed size, and putting the die on backwards means it cannot start at all.
Seat the die stock flat against the bar end and press down hard while turning. The pressure is doing the work for the first two turns; after that the thread pulls the die along on its own and you can ease off.
Check square after two turns exactly as with a tap. A round split die can also be adjusted slightly by its screws: opened out for a first roughing pass, closed for a second finishing pass. On a tough material that two-pass approach halves the torque and gives a better thread.
Ibikoresho bikenewe:
 Igifashi cyo guhindukiza umuyoboro wo hanze
 Agakoresho ko gukata imizingo y'ibyumaIgifata gikomeye cy'ameza y'akazi
 Irangi ry'ubururu ryo kuranga
4
4
Back off, oil, and test it on a real nut
Back off, oil, and test it on a real nut
Half a turn forward, a quarter back — the same rhythm as tapping and for the same reason. Use cutting oil generously; a die has far more cutting edges in contact than a tap and generates correspondingly more heat.
Cut to the length you need and no further. A thread run right up to a shoulder leaves no clearance and the nut will not seat, so stop two or three threads short.
Test the result by running a real nut down the full length by hand. It should turn with light finger pressure the whole way. If it tightens progressively, the bar was oversize or the die is closing; if it is loose and rocks, the die was opened too far. Both are diagnosed in ten seconds by the nut and by nothing else.
Ibikoresho by'iyi ntambwe:
 Amavuta yo gukata1 igiceUmutsi w'icyuma cyoroshye1 igice
Ibikoresho bikenewe:
Igifashi cyo guhindukiza umuyoboro wo hanze Icyegeranyo cy'ibyuma n'udukoni
 Umwenda w'Ipamba
 Amadarubindi Asobanutse yo Kwirinda
Ibikoresho
2- 1 igiceUmwanya
- 1 igiceUmwanya
Ibikoresho bikenewe
9- Umwanya
- Umwanya
Blueprint zijyanye
Izi blueprint zisangira ubumenyi — uburyo, ibikoresho cyangwa amahame
CC0 Umurenge rusange
Iyi blueprint yasohowe munsi ya CC0. Ushobora gukoporora, guhindura, gukwirakwiza no gukoresha nta kwemererwa.
Shyigikira Umuremyi ugura ibicuruzwa binyuze muri Blueprint ye Komisiyo y'Umuremyi byashyizweho n'Abacuruzi, cyangwa kora verisiyo nshya y'iyi Blueprint ukayinjiza nk'isano muri Blueprint yawe kugira ngo musangire inyungu.