Ubufatanye
UBUHANZI
UBWIZA N'UBUZIMA
UBUKORIKORI
UMUCO N'AMATEKA
IMYIDAGADURO
IBIDUKIKIJE
IBIRIBWA N'IBINYOBWA
UBWUBATSI BUSUBIRA INYUMA
UBUMENYI
SIPORO
IKORANABUHANGA
IBYAMBARWA
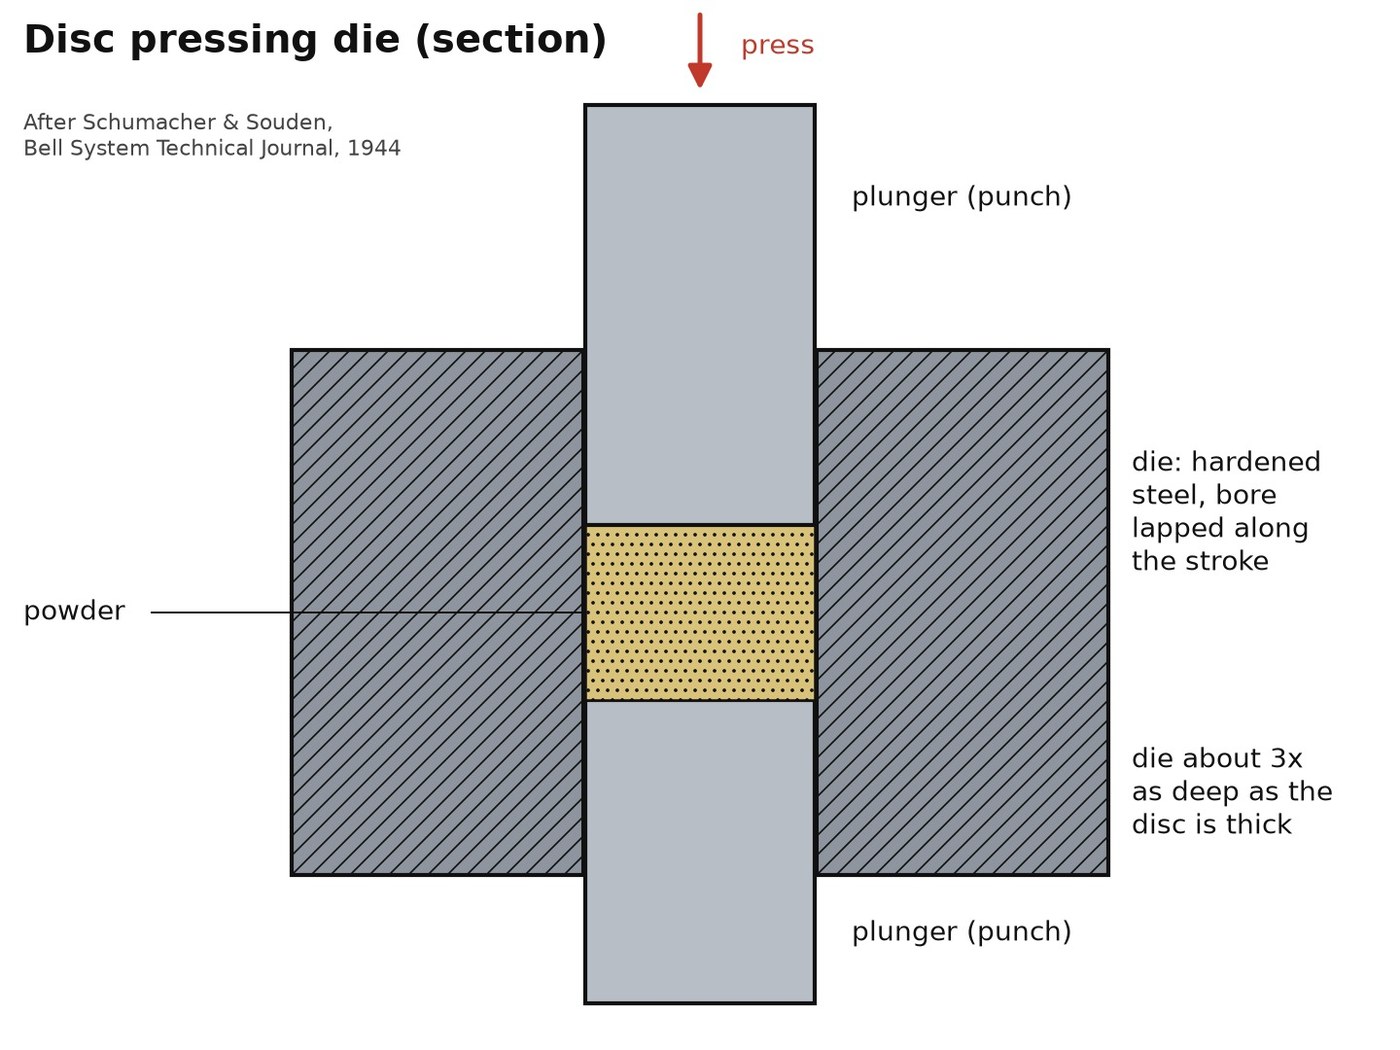

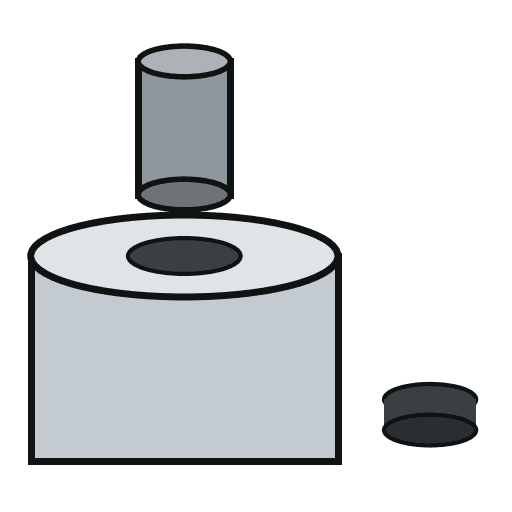
Disc Pressing Die: Hardened Steel, the Bore Lapped Along the Stroke (Schumacher & Souden, 1944)
The die in which powder is pressed into a flat disc: a block of hardened steel with a round bore, and close-fitting plungers that press the powder in it. The bore is lapped with rouge along the stroke, so its last fine scratches run the way the disc comes out.
Result: a die for pressing metal or ceramic powders into discs, at 5 to over 100 tons per square inch.
Source: E. E. Schumacher and A. G. Souden, Some Aspects of Powder Metallurgy, Bell System Technical Journal 23 (1944), pp. 431-433 and 454-455. Unknown: the steel, the hardening, sizes and clearances. Picture drawn by Youblob.
Hejuru
Unknown
Amabwiriza
1
1
Make the die and plungers
Make the die and plungers
Make the die of steel with a round bore through it, and plungers that fit the bore closely; there must be some clearance between them. Make the bore about three times as deep as the disc will be thick. Light, fluffy powders need a deeper die and longer plungers. Ours: tool steel for the die, and a lathe to bore and turn. Not given: the steel, sizes, clearance, the plungers' metal.
Ibikoresho by'iyi ntambwe:
 Inkoni ya kare y'icyuma cy'ibikoresho1 die
 Icyuma kitazwi1 plungers
Ibikoresho bikenewe:
 Imashini yo guhinguza icyuma
 Ingano zitazwi
2
2
Harden the die
Harden the die
Harden the die. For very abrasive powders, make the die of hard carbide or line it with carbide instead. Ours: a heat-treating oven and a quench. Not given: the hardening heat and quench.
Ibikoresho bikenewe:
 Itanura ryo gutunganya hakoreshejwe ubushyuhe
 Indobo yo gukonjesha
3
3
Lap the bore along the stroke
Lap the bore along the stroke
Polish the bore to a high finish by lapping with polishing rouge, moving the lap in the direction of the plunger stroke. The fine scratches that remain then run the way the pressed disc is pushed out, not across it.
Ibikoresho bikenewe:
 Umutuku w'umucuzi
4
4
Press a disc
Press a disc
Fill the bore with powder and press it with the plungers in a mechanical or hydraulic press, at 5 to over 100 tons per square inch. The powder hardly flows sideways, and friction at the die wall makes the pressure uneven: a part that is long for its width may come out with a soft, less dense middle. Push the disc out along the bore.
Ibikoresho bikenewe:
 Imashini ikanda ikoresha amazi
Ibikoresho
2- Umwanya
- 1 plungersUmwanya
Ibikoresho bikenewe
6- Umwanya
- Umwanya
- Umwanya
- Umwanya
Ibikoresho by'Ibishushanyo Bifitanye Isano
10% igabana
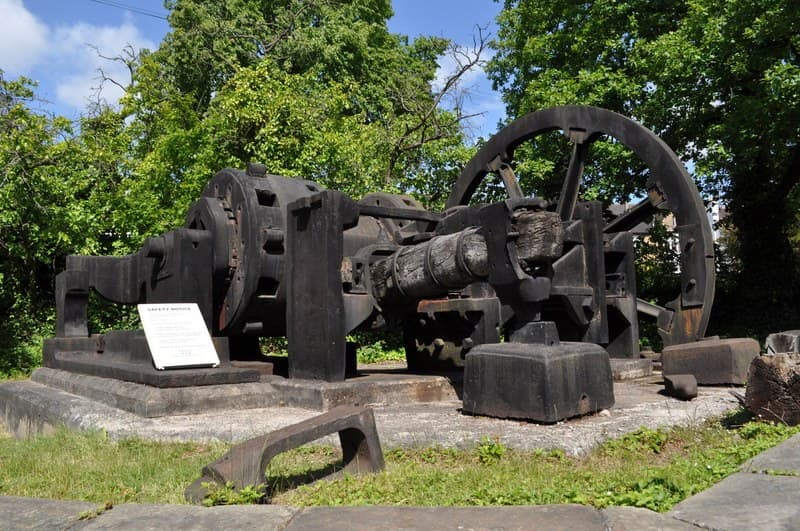
Tool-Steel Bar: Crucible Steel Drawn Out at a Cherry-Red Heat
na Forge
Umucuzi
32
0
0
0
5
0
10% igabana
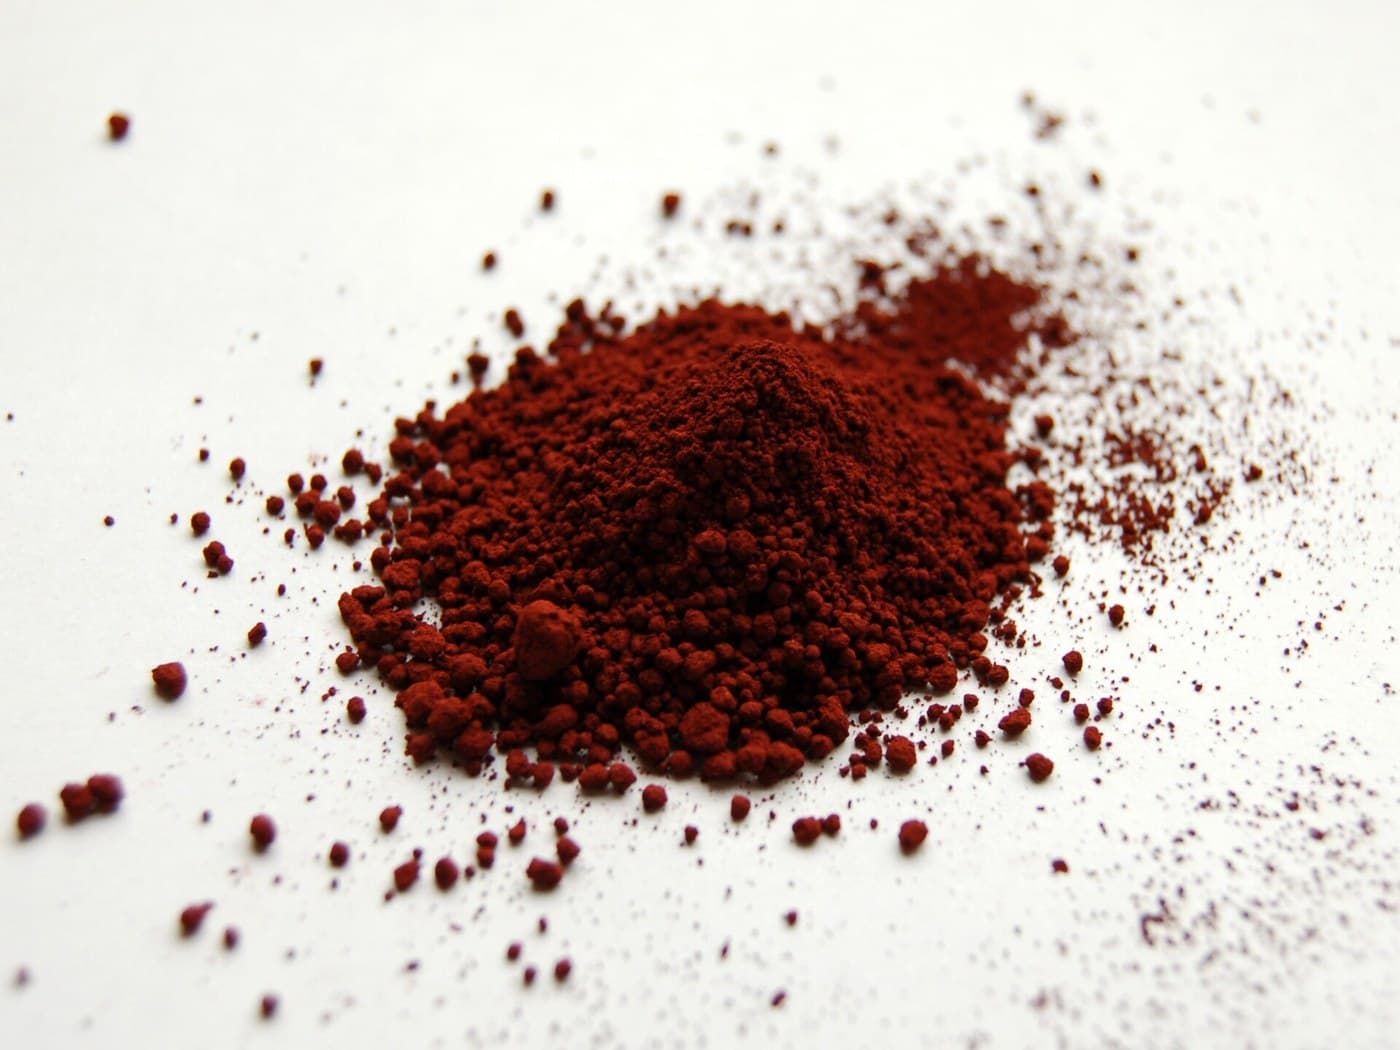
Jewellers' Rouge Precipitated from Copperas, Ure 1839
na Charlie
Bidafite Ubuzima
12
0
0
0
1
0
10% igabana
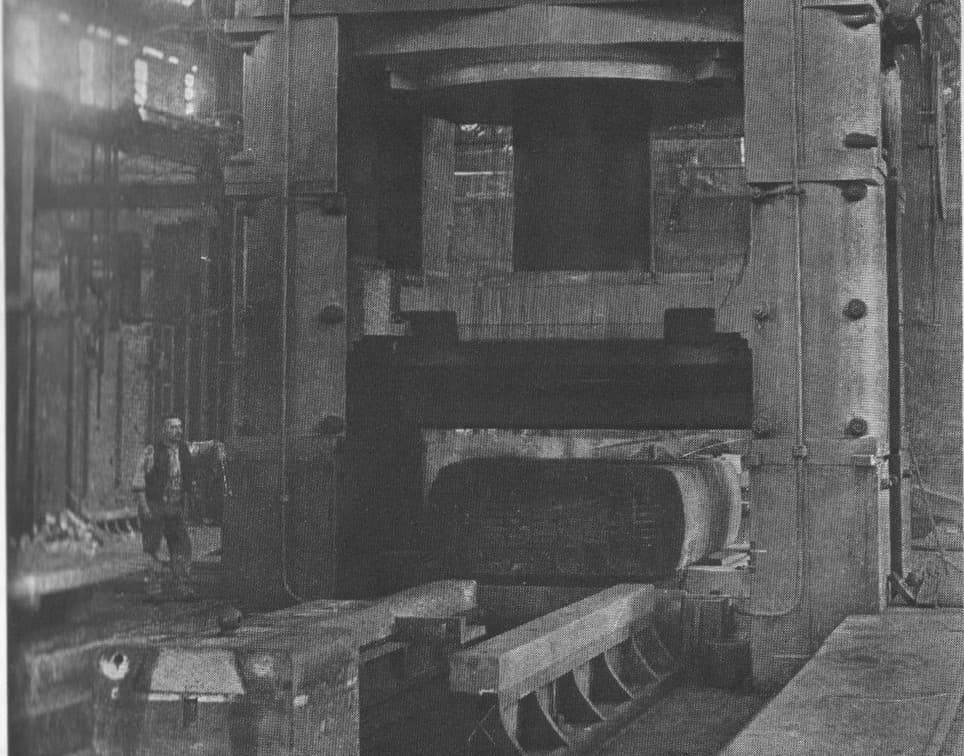
Hydraulic Press
na Emma
Ubucuzi bw'Ibyuma
54
0
0
0
10
0

10% igabana
Building a Screw-Cutting Lathe — The Machine That Makes Other Machines
na Gimli
Ubucuzi bw'Ibyuma
57
0
0
0
4
0
Iki gishushanyo gikora
CC0 Umurenge rusange
Iyi blueprint yasohowe munsi ya CC0. Ushobora gukoporora, guhindura, gukwirakwiza no gukoresha nta kwemererwa.
Shyigikira Umuremyi ugura ibicuruzwa binyuze muri Blueprint ye Komisiyo y'Umuremyi byashyizweho n'Abacuruzi, cyangwa kora verisiyo nshya y'iyi Blueprint ukayinjiza nk'isano muri Blueprint yawe kugira ngo musangire inyungu.