Ubufatanye
UBUHANZI
UBWIZA N'UBUZIMA
UBUKORIKORI
UMUCO N'AMATEKA
IMYIDAGADURO
IBIDUKIKIJE
IBIRIBWA N'IBINYOBWA
UBWUBATSI BUSUBIRA INYUMA
UBUMENYI
SIPORO
IKORANABUHANGA
IBYAMBARWA
English


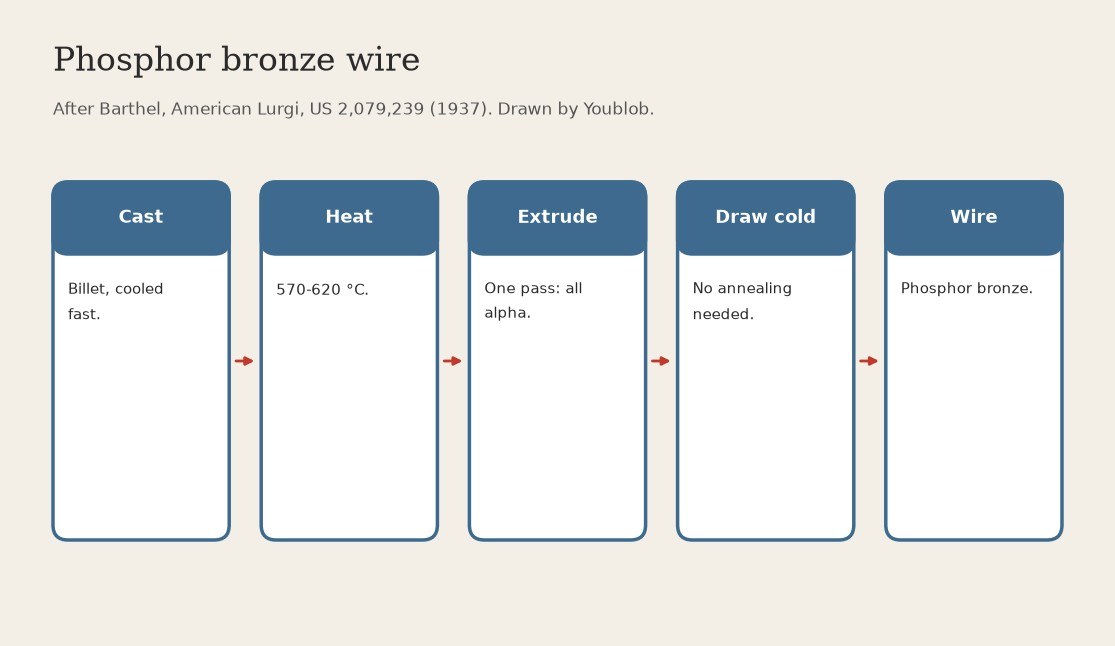
Phosphor Bronze Wire: Cast Billet Extruded at 570-620 °C, then Cold Drawn without Annealing (Barthel, Lurgi, US 2,079,239)
Cast phosphor bronze holds a brittle tin-rich phase that made wire drawing a long round of drawing and annealing. Barthel found that extruding the casting at 570-620 °C kneads it into one soft, even phase, after which it draws straight down to wire.
Result: phosphor bronze wire, drawn without intermediate annealing.
Source: Barthel, US 2,079,239 (American Lurgi, 1937). His temperature is for about 8 % tin; our ingot has about 9 %, so the same range is ours. Not given: extrusion ratio, die sizes. Picture drawn by Youblob.
Hejuru
2 days
Amabwiriza
1
1
Cast a billet and cool it fast
Cast a billet and cool it fast
Melt the phosphor bronze and cast it into a billet, cooling it rapidly. Ours: cast in an ingot mould and quench.
Ibikoresho by'iyi ntambwe:
 Ingoti y’umuringa wa fosifore1 as required
Ibikoresho bikenewe:
 Akabindi ka garafite n'ibumba
 Itanura ry'inkono yo gushongesheramo
 Imbumbe yo gusukamo icyuma gishongeye
 Indobo yo gukonjesha
2
2
Heat the billet to 570-620 °C
Heat the billet to 570-620 °C
Heat the billet to between about 570 and 620 °C (Barthel's range for about 8 % tin and 0.3 % phosphorus). Temperature: 500-650 °C overall; the less tin, the hotter (about 650 °C for 6 % tin).
Ibikoresho bikenewe:
 Ifuru ya muffle
 Pirometero
3
3
Extrude it in one pass
Extrude it in one pass
Extrude the hot billet in an extrusion press. The kneading makes the metal even all through, practically all alpha. For thick products with little reduction, cold-press the billet 10-20 % first.
Ibikoresho bikenewe:
 Ikandagira rya hidoroli ryo gusohora
4
4
Cold draw to wire without annealing
Cold draw to wire without annealing
Draw the extruded rod cold through dies down to wire; Barthel's metal needs no annealing between draws. Ours: a steel drawplate with drawing lubricant, one hole smaller each pass.
Ibikoresho bikenewe:
 Urubaho rwo gukurura insinga rw'icyuma
 Amavuta yo gukurura insinga
Ibikoresho
1- 1 as requiredUmwanya
Ibikoresho bikenewe
9- Umwanya
- Umwanya
- Umwanya
- Umwanya
Iki gishushanyo gikora
Blueprint zijyanye
Izi blueprint zisangira ubumenyi — uburyo, ibikoresho cyangwa amahame
CC0 Umurenge rusange
Iyi blueprint yasohowe munsi ya CC0. Ushobora gukoporora, guhindura, gukwirakwiza no gukoresha nta kwemererwa.
Shyigikira Umuremyi ugura ibicuruzwa binyuze muri Blueprint ye Komisiyo y'Umuremyi byashyizweho n'Abacuruzi, cyangwa kora verisiyo nshya y'iyi Blueprint ukayinjiza nk'isano muri Blueprint yawe kugira ngo musangire inyungu.