SANAT
GÜZELLİK & SAĞLIK
ZANAAT
KÜLTÜR & TARİH
EĞLENCE
ÇEVRE
YİYECEK & İÇECEK
TERS MÜHENDİSLİK
BİLİMLER
SPOR
TEKNOLOJİ
GİYİLEBİLİR ÜRÜNLER
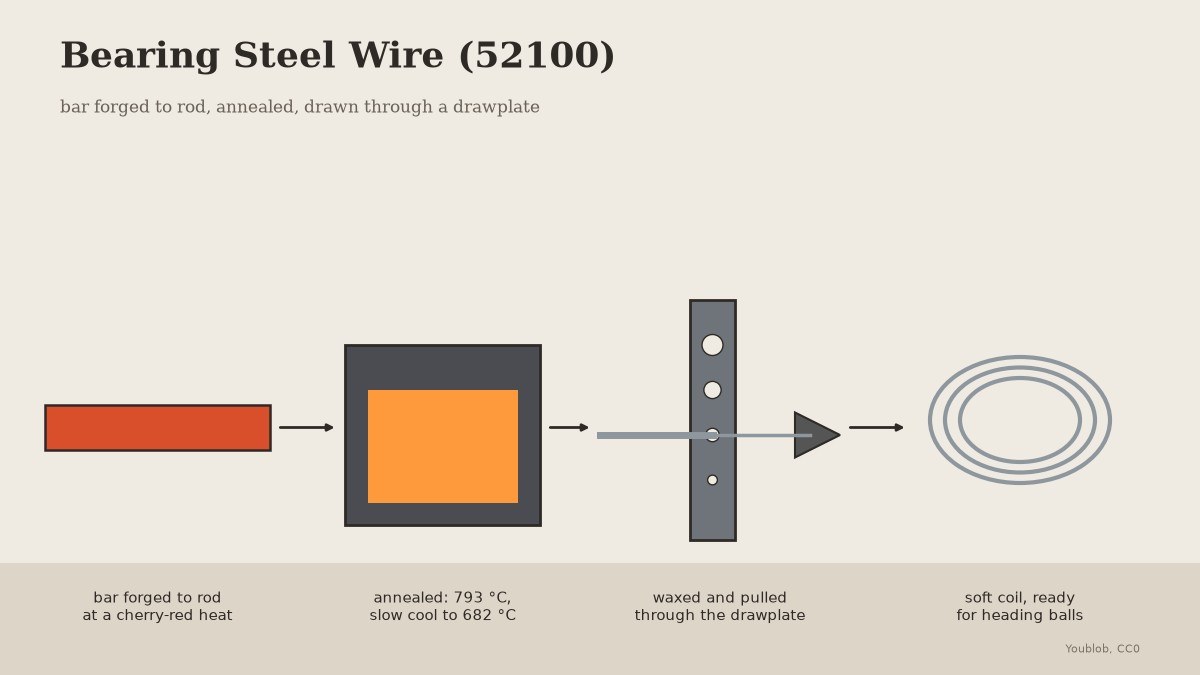


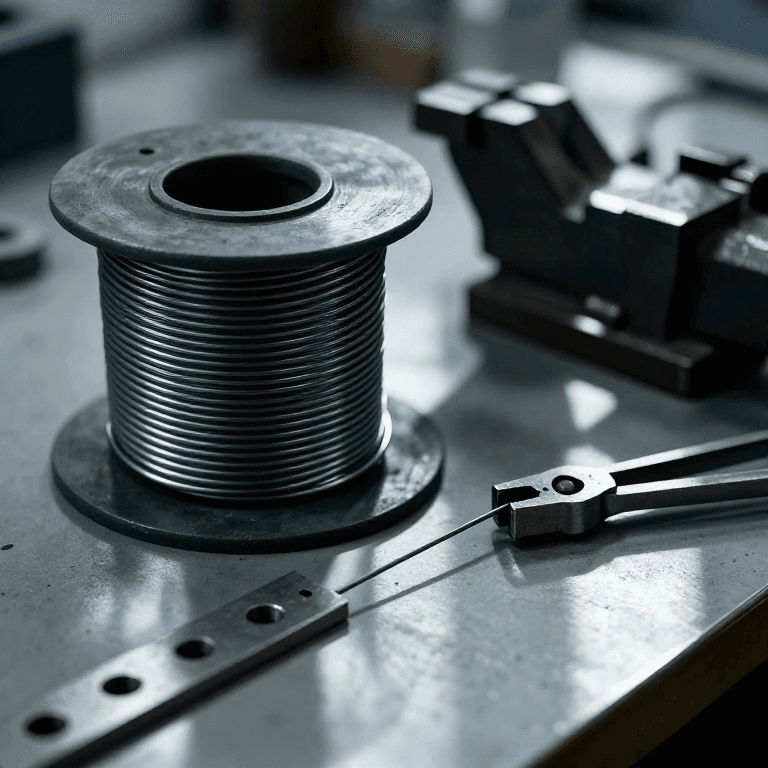
Bearing Steel Wire (52100): Drawn from Bar Through a Drawplate
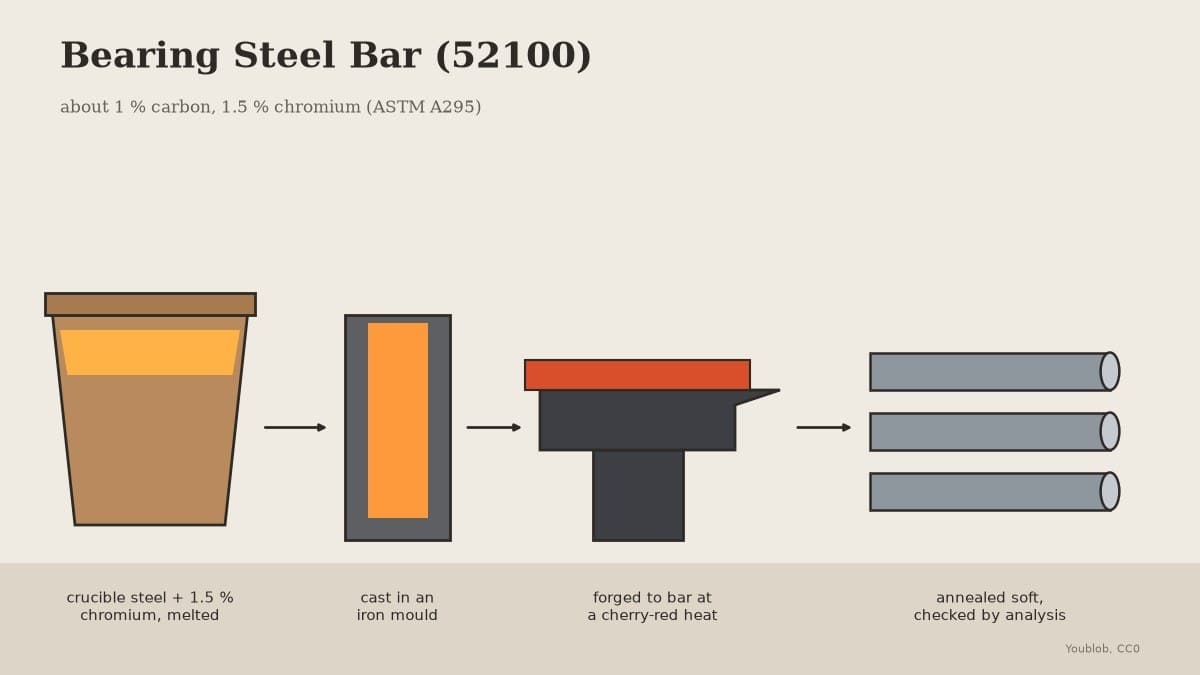
Bearing balls are headed from thick wire of 52100 steel. Here 52100 bar is forged to rod and drawn through a drawplate. At 1 % carbon it is much harder than mild steel, so it is annealed soft before drawing and again after every two holes, using the 52100 anneal Verhoeven recommends.
The picture: our drawing, bar to coil.
İleri
2 days
Talimatlar
1
1
Forge to rod
Forge to rod
Heat the bar to a cherry-red heat and no hotter, and draw it out round on the anvil to a rod a little thicker than the drawplate's largest hole.
Bu adım için malzemeler:
 Rulman çeliği çubuk (52100)1 kg
 Odun Kömürü1 as required
Gerekli aletler:
 Demirci ocağı
 Örs
 Enine keski başlı çekiç
 Demirci kerpeteni
 Kaynak eldivenleri
 Koruyucu gözlük
2
2
Anneal
Anneal
In the oven, hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
Gerekli aletler:
 Isıl işlem fırını
 Göstergeli ısıl çiftDemirci kerpeteniKaynak eldivenleri
3
3
Clean and taper
Clean and taper
Brush off all the scale, then file a long taper on the first 3 cm so it passes the first hole.
Gerekli aletler:
 Tel fırça seti
 Eğe Takımı
 Tezgah Mengenesi
4
4
Wax and draw
Wax and draw
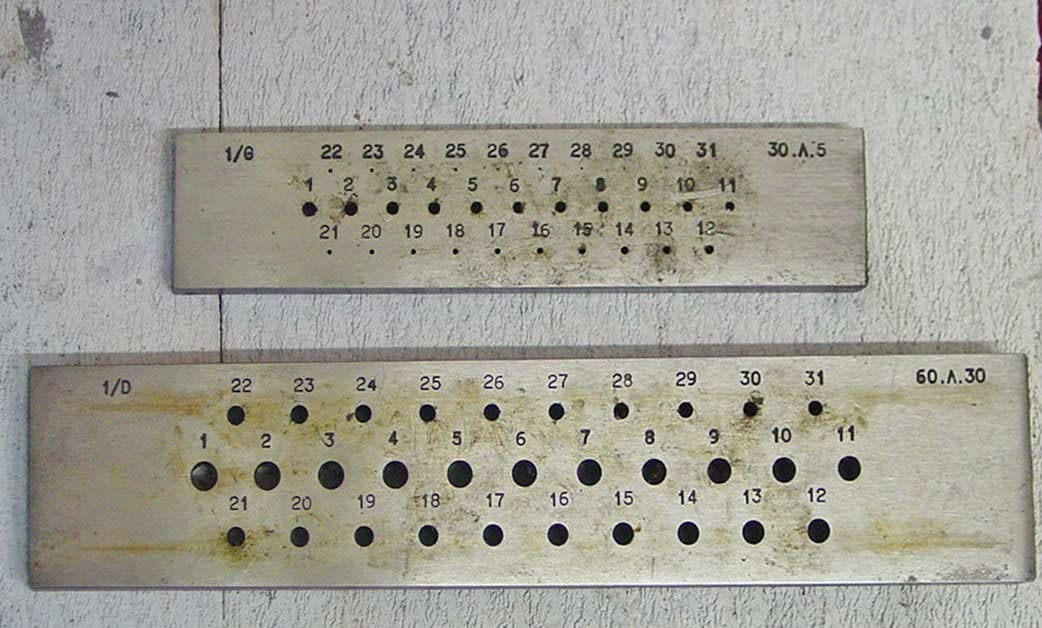
Clamp the drawplate in the vise. Wax the rod, push the taper through the first hole it does not slip through, and pull straight out with the draw tongs in one steady pull.
Bu adım için malzemeler:
 Balmumu20 g
Gerekli aletler:
 Çelik haddeleme plakası
 Çekme kerpeteniTezgah Mengenesi
 Deri İş Eldiveni
5
5
Anneal every two holes
Anneal every two holes
Draw through each next hole without skipping. After every two holes, coil the wire and anneal it again: hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
Bu adım için malzemeler:
Balmumu1 adetGerekli aletler:
Çelik haddeleme plakasıÇekme kerpeteniIsıl işlem fırınıGöstergeli ısıl çift6
6
Finish soft
Finish soft
Stop at the diameter your balls need, checked with the caliper, and give the coil a last anneal so it is soft for heading.
Gerekli aletler:
 Dijital Kumpas 6 İnçIsıl işlem fırınıGöstergeli ısıl çift
7
7
Troubleshooting
Troubleshooting
Bearing steel wire troubleshooting.
Flow
Loading...
Malzemeler
3- Yer Tutucu
- 1 as requiredYer Tutucu
- 1 adetYer Tutucu
Gerekli Aletler
15- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
Bu planla yapılan
İlgili Blueprint'ler
Bu blueprint'ler bilgi paylaşır — teknikler, malzemeler veya ilkeler
CC0 Kamu Malı
Bu plan CC0 lisansıyla yayınlanmıştır. İzin almadan kopyalayabilir, değiştirebilir, dağıtabilir ve herhangi bir amaçla kullanabilirsiniz.
Planı üzerinden ürün satın alarak Maker'ı destekleyin, böylece Maker Komisyonu Satıcılar tarafından belirlenen komisyonu kazanırlar veya bu Planın yeni bir versiyonunu oluşturun ve gelir paylaşımı için kendi Planınıza bağlantı olarak ekleyin.