SANAT
GÜZELLİK & SAĞLIK
ZANAAT
KÜLTÜR & TARİH
EĞLENCE
ÇEVRE
YİYECEK & İÇECEK
TERS MÜHENDİSLİK
BİLİMLER
SPOR
TEKNOLOJİ
GİYİLEBİLİR ÜRÜNLER


Tolerance and Clearance: Printed Holes Come Out Small, Every Time
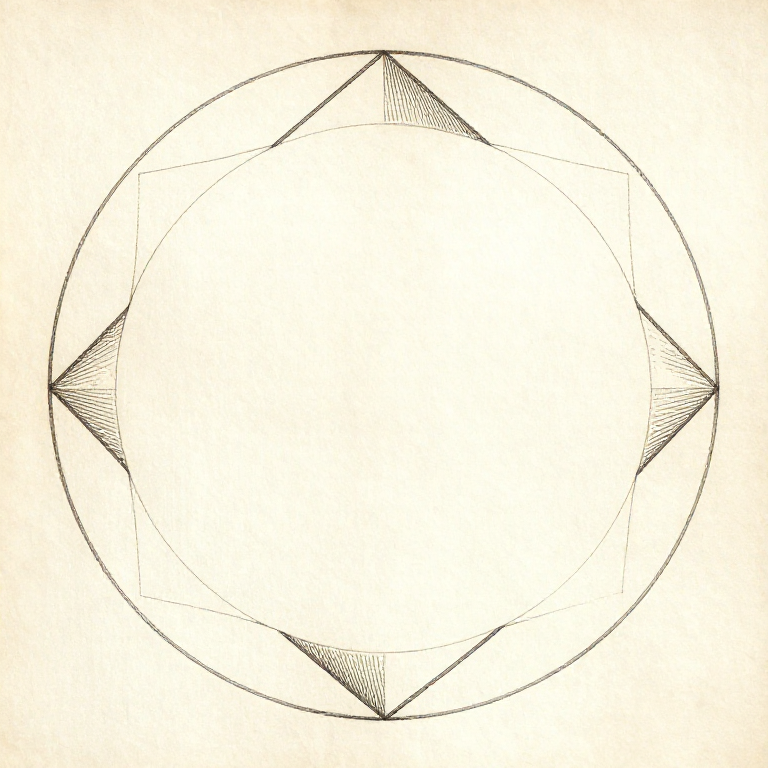
Model a 5 mm hole, print it, and a 5 mm pin will not go in. That is not a fault in the printer: it is what happens when a round hole is approximated by straight line segments laid inside its circumference, and when hot plastic shrinks as it cools.
Both effects run the same way, so printed holes come out SMALL and printed pegs come out LARGE. The error is a few tenths of a millimetre, consistently, in a predictable direction — which makes it correctable rather than annoying.
Which is the whole point: measure your printer's error once, on a test piece, and then design every hole and peg with it already allowed for.
Orta
3 hours
Talimatlar
1
1
Why it happens, and which way
Why it happens, and which way
A circular hole is printed as a many-sided polygon whose corners touch the circle, so the flats fall INSIDE it. The smaller the hole, the fewer segments and the worse the effect.
On top of that the nozzle pushes a line of plastic that spreads slightly, and the plastic shrinks as it cools. Both add material where the hole should be and remove it from outside surfaces — so holes shrink and pegs grow.
That means an interference fit and a clearance fit are not symmetrical on a printer, unlike on a lathe. A peg and hole modelled the same size will always be an interference fit, and usually a very tight one.
Bu adım için malzemeler:
 3D baskı filamenti (PLA)1 adet
Gerekli aletler:
 Dijital Kumpas 6 İnç
 Büyüteç Lupu
2
2
Measure your own printer's offset
Measure your own printer's offset
Jupyter defteri yükleniyor…
Bu adım için malzemeler:
3D baskı filamenti (PLA)1 adet ABS filament1 adet
Gerekli aletler:
Dijital Kumpas 6 İnç Masaüstü Bilgisayar
 FDM 3B yazıcı
3
3
Measure the same way every time
Measure the same way every time
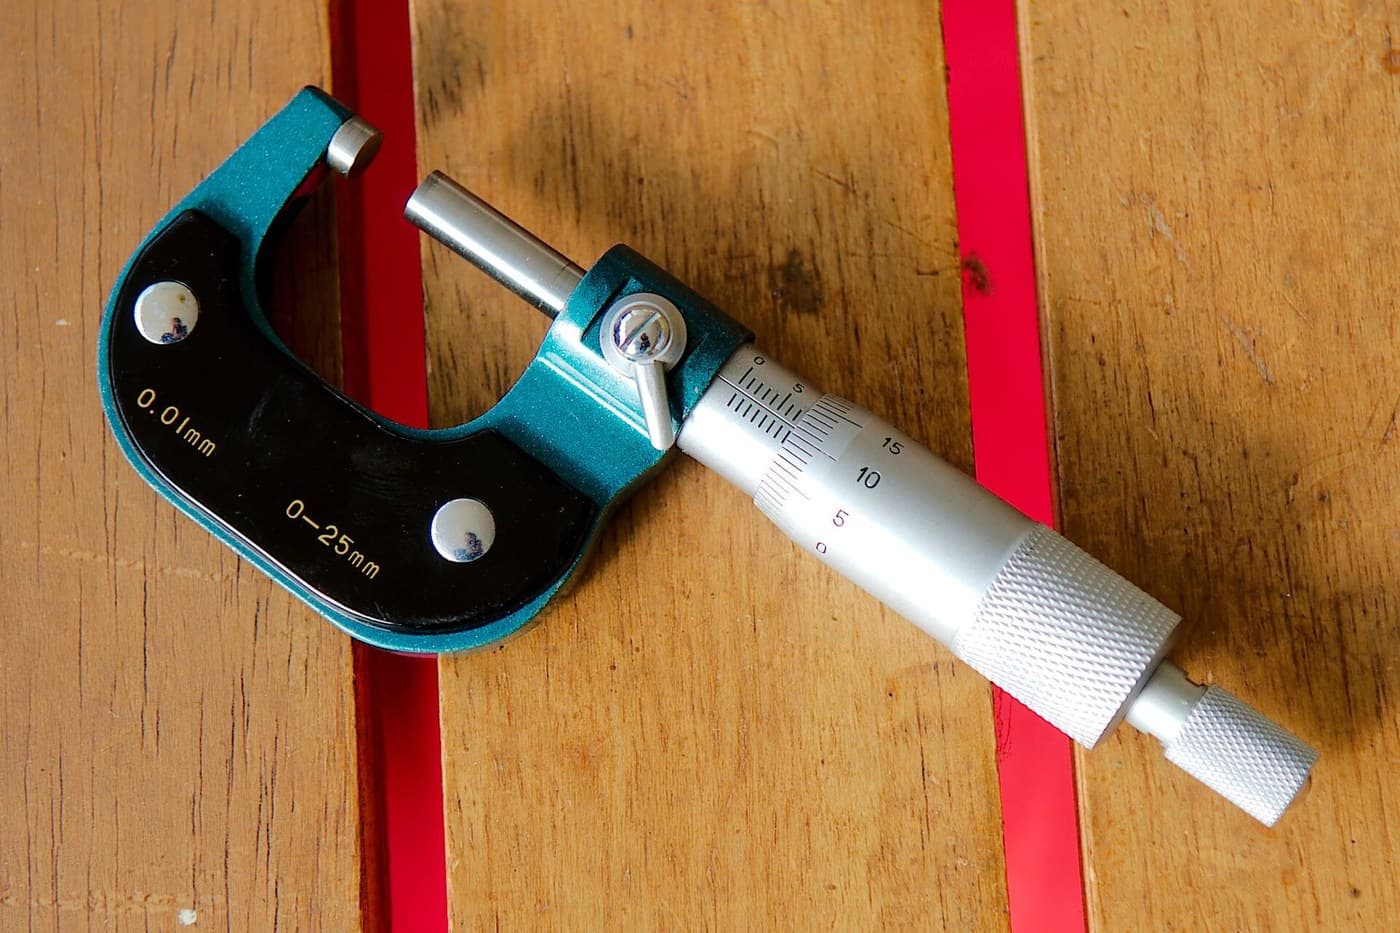
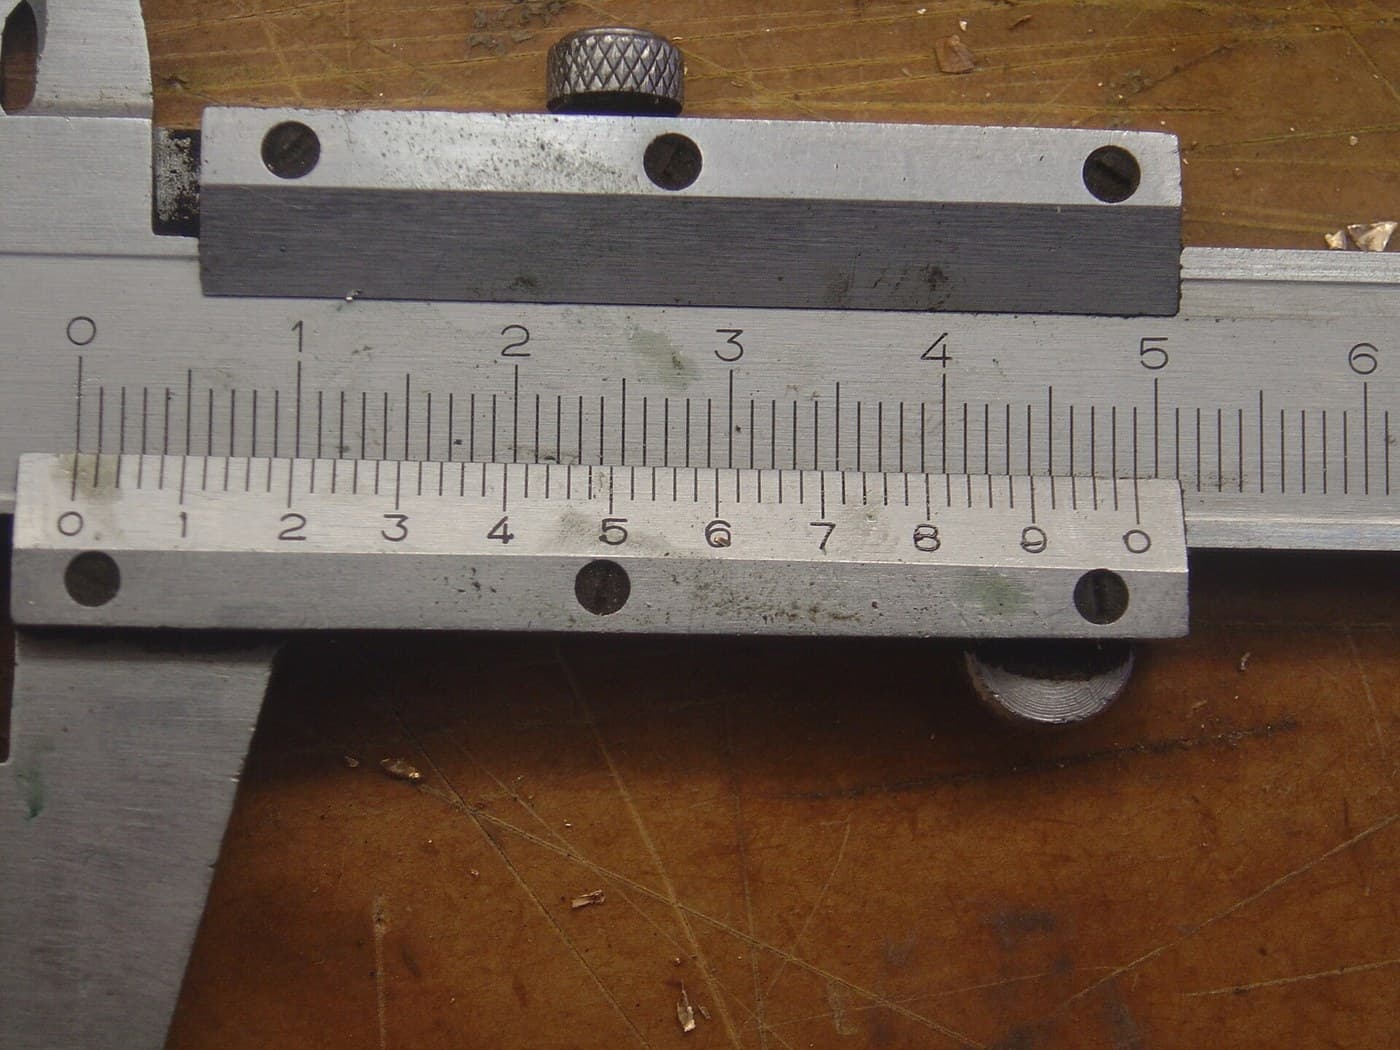
Measure across several diameters and at several heights. A printed hole is not round and not the same size top to bottom — the first layers are squashed wider and the seam where each layer starts leaves a small bump.
Take the smallest reading for a hole and the largest for a peg. Those are what actually decide whether the parts go together, and averaging hides exactly the feature that will stop them.
Deburr before measuring. The small ridge left where each layer starts, and the elephant-foot bulge on the bottom layers, both read as material that is not really in the way — and both come off in seconds with a deburring tool.
Bu adım için malzemeler:
3D baskı filamenti (PLA)1 adetGerekli aletler:
Dijital Kumpas 6 İnç Çapak alma aletiBüyüteç Lupu
4
4
Design so the fit does not have to be perfect
Design so the fit does not have to be perfect
The best answer to a tight tolerance is usually to remove the need for it. A slot instead of a hole, a chamfer at the entry, a split collar with a screw, a deliberate flexure — all of them turn a precise dimension into an adjustable one.
A CHAMFER on every hole and peg entry is nearly free and makes an imperfect fit assemble anyway. It also prints better, because the chamfer at the bottom removes the elephant-foot problem from the part that has to enter.
And where a real fit is needed, use a real part: a brass insert for a thread, a steel pin in a printed housing, a bearing pressed into a printed seat. Printing everything is a constraint nobody imposed.
Bu adım için malzemeler:
3D baskı filamenti (PLA)1 adetGerekli aletler:
Masaüstü BilgisayarDijital Kumpas 6 İnçÇapak alma aletiİlgili Blueprint'ler
Bu blueprint'ler bilgi paylaşır — teknikler, malzemeler veya ilkeler


CC0 Kamu Malı
Bu plan CC0 lisansıyla yayınlanmıştır. İzin almadan kopyalayabilir, değiştirebilir, dağıtabilir ve herhangi bir amaçla kullanabilirsiniz.
Planı üzerinden ürün satın alarak Maker'ı destekleyin, böylece Maker Komisyonu Satıcılar tarafından belirlenen komisyonu kazanırlar veya bu Planın yeni bir versiyonunu oluşturun ve gelir paylaşımı için kendi Planınıza bağlantı olarak ekleyin.