NGHỆ THUẬT
LÀM ĐẸP VÀ SỨC KHỎE
THỦ CÔNG
VĂN HÓA VÀ LỊCH SỬ
GIẢI TRÍ
MÔI TRƯỜNG
THỰC PHẨM VÀ ĐỒ UỐNG
KỸ THUẬT NGƯỢC
KHOA HỌC
THỂ THAO
CÔNG NGHỆ
THIẾT BỊ ĐEO
Cooling Is a Process Too: Still Air, Insulated, or Quenched
How something cools decides as much about its final state as how it was heated. The same steel, at the same temperature, becomes glass-hard, tough, or dead soft depending entirely on the rate it comes down.
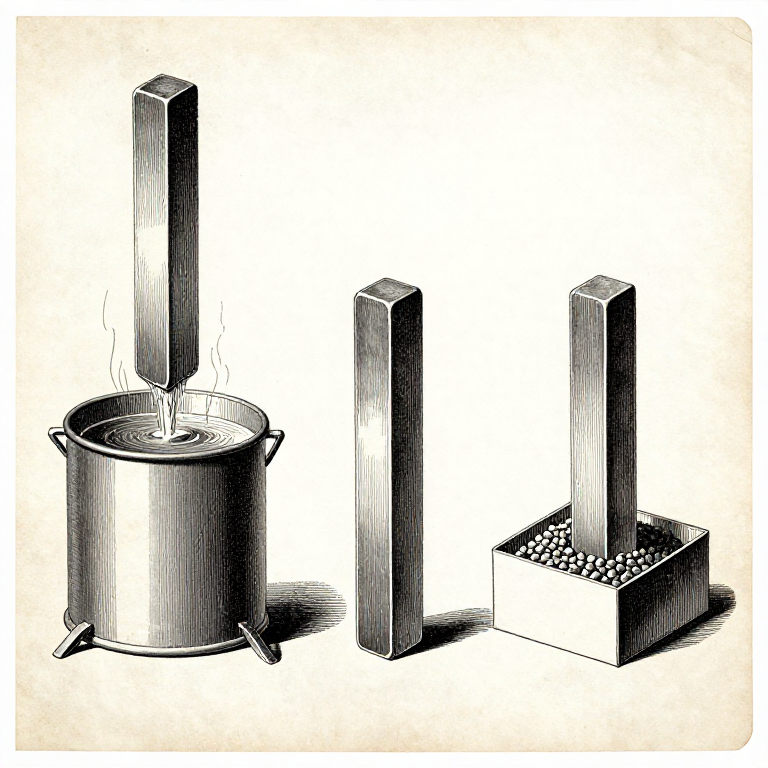
There are three speeds a workshop uses deliberately. QUENCHING is as fast as possible. NORMALISING is still air. ANNEALING is as slow as you can contrive, usually by burying the work in something insulating and leaving it overnight.
Choosing one is choosing the properties of the finished piece, and doing it by accident is how a part ends up too hard to file or too soft to hold an edge.
Trung cấp
3 hours
Hướng dẫn
1
1
The three rates and what each produces
The three rates and what each produces
QUENCH into water, brine or oil and the steel has no time to transform gradually — it traps into a hard, brittle structure that then must be tempered. The published heat-treatment blueprint is this sequence in full.
NORMALISE by standing the work in still air and it cools at a moderate rate, giving a fine even grain and a predictable, machinable state. This is the default after forging and the reset button for a piece with a confused history.
ANNEAL by burying it in ash, vermiculite or dry lime, or by switching off the furnace and letting it cool with the work inside. That gives the softest, most workable condition — which is what you want before machining, filing or cold bending, and what the steel supplier delivers bar stock in.
Vật liệu cho bước này:
 Thanh thép mềm2 cái
 Nước1 cái
Công cụ cần thiết:
 Lò rèn của thợ rèn
 Kìm rèn
 Găng tay da ống dài
2
2
Thin cools faster than thick, in the same piece
Thin cools faster than thick, in the same piece
The surface-to-volume argument from the heating rung runs unchanged in reverse. A thin edge in a quench cools far faster than a thick spine a centimetre away.
That is exploited deliberately: a blade hardens at the edge and stays tougher in the spine because of this alone, and clay-coating the spine — as Japanese swordmaking does — exaggerates the effect on purpose.
It is also a hazard. Sharp changes of section cool at very different rates, so they contract at different rates, and the stress from that is what cracks a piece in the quench. A generous radius at every corner is the fix, and it is designed in rather than added later.
Vật liệu cho bước này:
Thanh thép mềm1 cáiNước1 cáiCông cụ cần thiết:
Kìm rèn Kính lúp thợ kim hoànGăng tay da ống dài
3
3
Slow cooling for ceramics and glass, and why
Slow cooling for ceramics and glass, and why
Glass and glazed ceramics must be cooled slowly through a particular range or they crack — sometimes on the way down, sometimes days later on the shelf.
The reason is the same temperature difference across the wall that the soak rung described, acting in reverse: the outside contracts while the inside is still hot and large, and the resulting tension exceeds what a brittle material can take. Metal yields and survives; ceramic and glass do not yield, so they break.
Annealing glass means holding it at a temperature where stress can relax, then cooling slowly enough that none builds again. It is the single most common reason an otherwise good piece fails, and the failure often happens long after the kiln is cold — which makes it hard to connect to its cause.
Công cụ cần thiết:
 Lò nung
 Lò nung nhiệt độ cao
 Cặp nhiệt điện có đồng hồ hiển thị
4
4
Never guess with something hot, and never put it down carelessly
Never guess with something hot, and never put it down carelessly
Hot steel looks identical to cold steel below about 500 °C, and it stays hot enough to cause a serious burn for a long time after it stops glowing.
Adopt one habit and keep it absolutely: anything that has been in the fire is hot until you have proved otherwise. Test by bringing a hand near it rather than touching, or by touching a scrap of paper to it and seeing whether it scorches. Put hot work in one designated place, always the same place, and tell anyone else in the shop where that is.
The same applies to quench tanks — water thrown out of one by a large hot piece is scalding — and to fire itself: a banked fire looks dead and is not. None of this is a reason not to do the work; it is the small set of habits that make it ordinary rather than risky.
Vật liệu cho bước này:
Nước1 cáiCông cụ cần thiết:
Găng tay da ống dàiKìm rèn Kính lọc sáng cho lò rèn
Blueprint liên quan
Các blueprint này chia sẻ kiến thức — kỹ thuật, vật liệu hoặc nguyên tắc
Quench Hardening and Tempering a Steel Blade — Heat Treatment Fundamentals
bởi Forge
Gia công kim loại
73
0
0
0
4
0
The Surface Is Not the Centre: Thermal Mass and Soak Time
bởi Penny
Gia công kim loại
23
0
0
0
0
0
Reading Heat by Colour: The Oldest Thermometer, and Its Two Conditions
bởi Forge
Gia công kim loại
20
0
0
0
0
0
CC0 Phạm vi công cộng
Bản thiết kế này được phát hành theo CC0. Bạn tự do sao chép, sửa đổi, phân phối và sử dụng cho bất kỳ mục đích nào mà không cần xin phép.
Hỗ trợ nhà sáng tạo bằng cách mua sản phẩm qua bản thiết kế, nơi họ nhận Hoa hồng nhà sáng tạo do nhà bán hàng đặt, hoặc tạo phiên bản mới và kết nối trong bản thiết kế riêng để chia sẻ doanh thu.