UBUCIKO
UBUHLE NEMPILO
UBUCIKO BEZANDLA
AMASIKO NOMLANDO
EZOKUZIJABULISA
IMVELO
UKUDLA NEZIPHUZO
REVERSE ENGINEERING
IZAYENSI
EZEMIDLALO
UBUCHWEPHESHE
IZINTO EZIGQOKWAYO
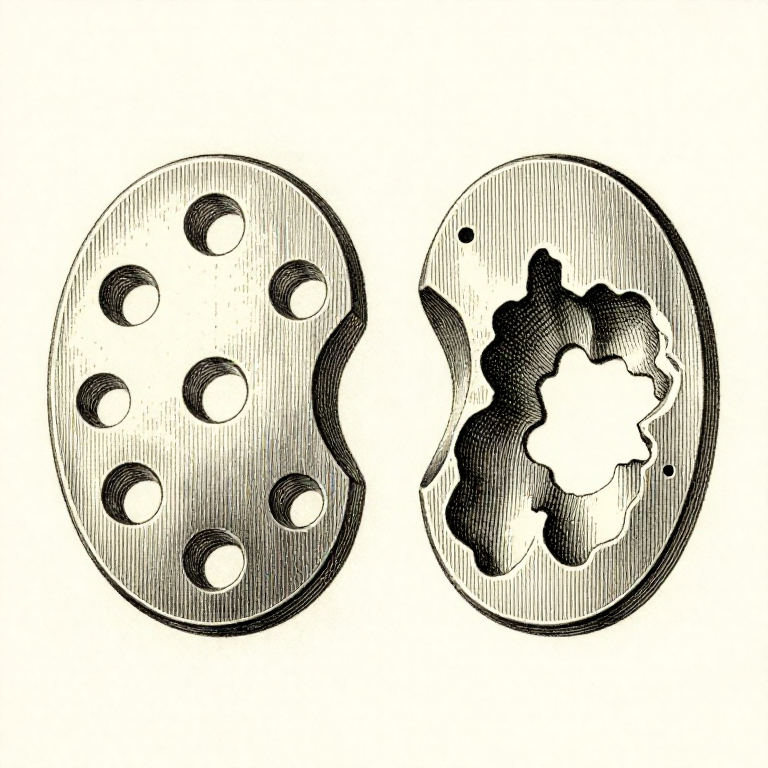


Reading a Casting: Porosity, Cold Shuts and Inclusions Each Name a Cause
A defective casting is a report on the process that made it. Where the defect is, what shape it is, and whether its surfaces are smooth or rough together identify which decision went wrong.
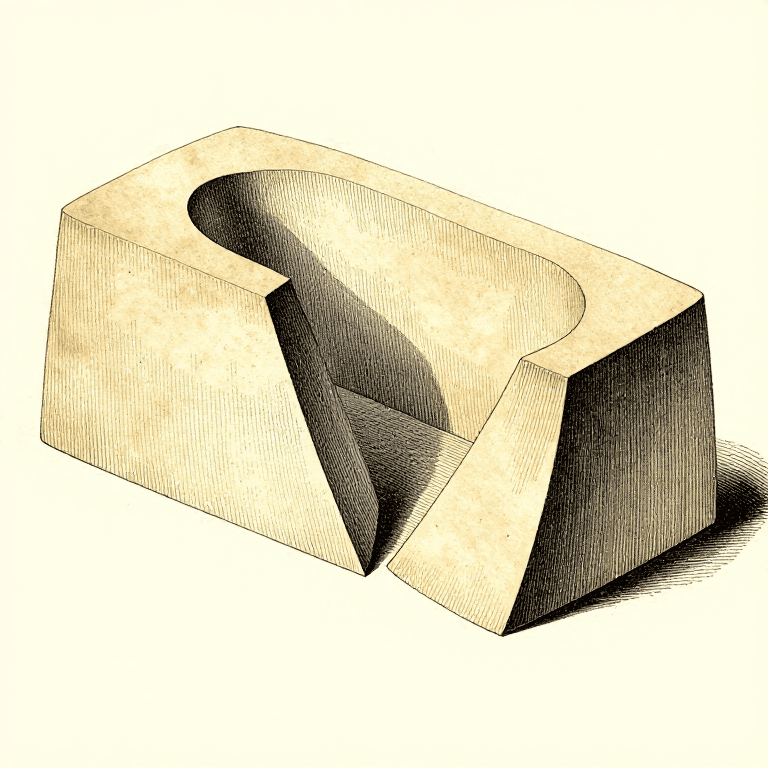
The two kinds of porosity are the clearest example. SHRINKAGE porosity is jagged, branching, and sits in the last place to freeze — a feeding failure. GAS porosity is round, smooth-walled and scattered — a gas failure. They look completely different under a loupe and they need opposite fixes.
Which makes cutting a failed casting open genuinely worth doing. Two minutes with a hacksaw answers a question that guessing cannot, and the answer changes the next mould rather than the next pour.
Osezingeni eliphezulu
3 hours
Imiyalelo
1
1
Round and smooth is gas; jagged and branching is shrinkage
Round and smooth is gas; jagged and branching is shrinkage
GAS porosity: round holes with smooth shiny walls, often scattered through a section or just under the surface. The metal dissolved gas when hot and released it on freezing. Causes: wet sand, damp charge, too much superheat, a turbulent pour, or an unvented core.
SHRINKAGE porosity: irregular, angular, branching cavities with rough dendritic walls, concentrated in the thickest section or under a riser neck. That is a feeding failure — the riser rung.
Their locations differ as much as their shapes. Gas porosity is often near the cope surface where gas collected; shrinkage is at the thermal centre. Both together usually mean too hot, since high superheat causes gas and worsens shrinkage at once.
Izinto zokwakha zalesi sinyathelo:
 Ingqimba yebhronzi1 ucezu
Amathuluzi adingekayo:
 Isaha Sensimbi
 I-Loupe Yokukhulisa
 Iqoqo Lamafayela
2
2
Misruns, cold shuts and the difference between them
Misruns, cold shuts and the difference between them
A MISRUN is a casting with a section simply missing, ending in a smooth rounded edge where the metal stopped and froze. Too cold, too slow, too thin a section, or not enough metal.
A COLD SHUT is a seam where two streams met and did not fuse — a smooth line with rounded edges on both sides, often looking like a crack but with no sharp root. Same causes, but it means the cavity DID fill, just not in time.
Both point at fluidity: pouring temperature, pouring speed, section thickness and gating. A cold shut in a thin web with everything else sound usually means the part needs a thicker web or a gate closer to it, not a hotter melt.
Izinto zokwakha zalesi sinyathelo:
Ingqimba yebhronzi1 ucezuAmathuluzi adingekayo:
I-Loupe Yokukhulisa I-Caliper Yedijithali Yamayintshi Ayi-6
3
3
Inclusions, penetration and veining come from the mould
Inclusions, penetration and veining come from the mould
SAND INCLUSIONS are grains embedded in the metal, usually near the cope surface because loose sand floats. Cause: a mould washed by turbulent metal, or a friable mould surface — which is the gating rung and the sand rung together.
PENETRATION is metal that has soaked into the sand, leaving a rough crusty surface that is hard to clean. Too hot, too coarse a sand, or under-rammed.
VEINING is thin raised fins on the casting, following cracks that opened in the sand as it expanded under heat. It is a sand problem, not a metal one, and it is worst on cores where the sand is surrounded by hot metal on every side.
Izinto zokwakha zalesi sinyathelo:
 Isihlabathi sokubumba1 kgIngqimba yebhronzi1 ucezu
Amathuluzi adingekayo:
I-Loupe YokukhulisaIqoqo Lamafayela4
4
Change one thing, and section the next one too
Change one thing, and section the next one too
Having named the defect, change ONE thing. Raise the vent count, or lower the pouring temperature, or enlarge the riser — not all three, or the next sound casting teaches nothing.
Section the next casting even if it looks perfect. A casting that is sound on the outside and has a cavity in the middle is the commonest expensive surprise, and finding it in the workshop is far better than finding it in service.
Photograph the cut faces and keep them with the mould notes. A file of sectioned castings next to their pouring temperatures and gating layouts is a foundry record in the same sense as a kiln log, and it is what turns a series of attempts into a process.
Izinto zokwakha zalesi sinyathelo:
Ingqimba yebhronzi1 ucezuAmathuluzi adingekayo:
Isaha SensimbiI-Loupe YokukhulisaI-Caliper Yedijithali Yamayintshi Ayi-6Ama-blueprint ahlobene
Lama-blueprint abelana ngolwazi — amasu, izinto noma izimiso
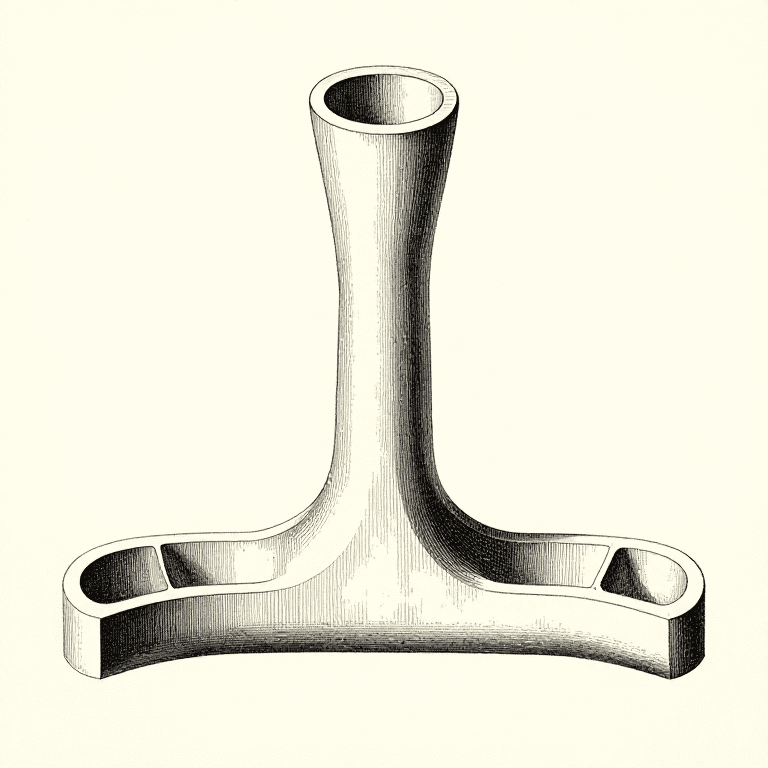
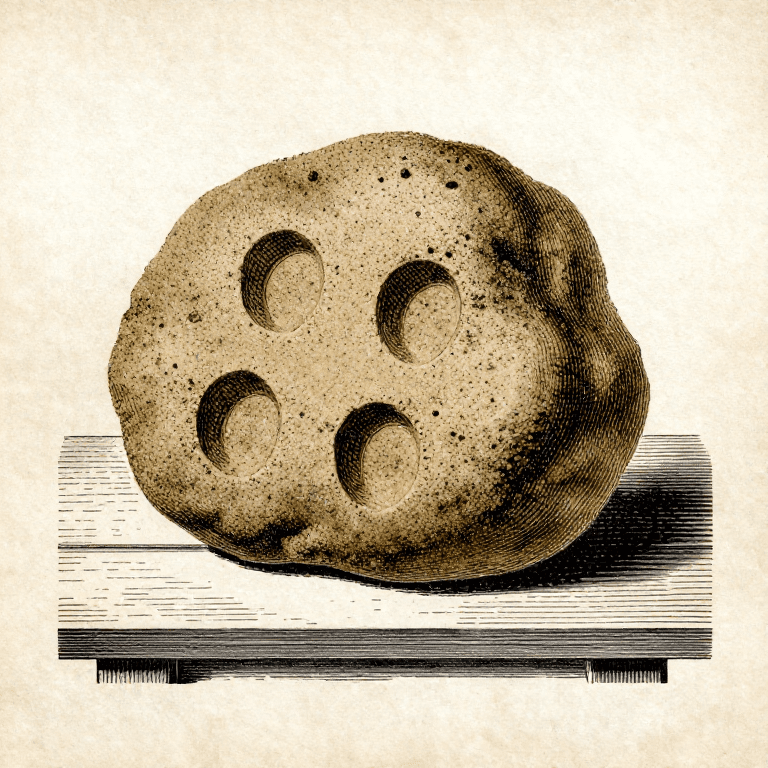
CC0 Isizinda Somphakathi
Le blueprint ikhishwe ngaphansi kwe-CC0. Ukhululekile ukukopisha, ukuguqula, ukusabalalisa, nokusebenzisa ngaphandle kwemvume.
Sekela uMenzi ngokuthenga imikhiqizo nge-Blueprint yabo IKhomishane Yomenzi kumiswe ngabathengisi, noma dala inguqulo entsha yale Blueprint bese uyifaka njengoxhumaniso ku-Blueprint yakho ukuze wabelane ngemali engenayo.