UBUCIKO
UBUHLE NEMPILO
UBUCIKO BEZANDLA
AMASIKO NOMLANDO
EZOKUZIJABULISA
IMVELO
UKUDLA NEZIPHUZO
REVERSE ENGINEERING
IZAYENSI
EZEMIDLALO
UBUCHWEPHESHE
IZINTO EZIGQOKWAYO
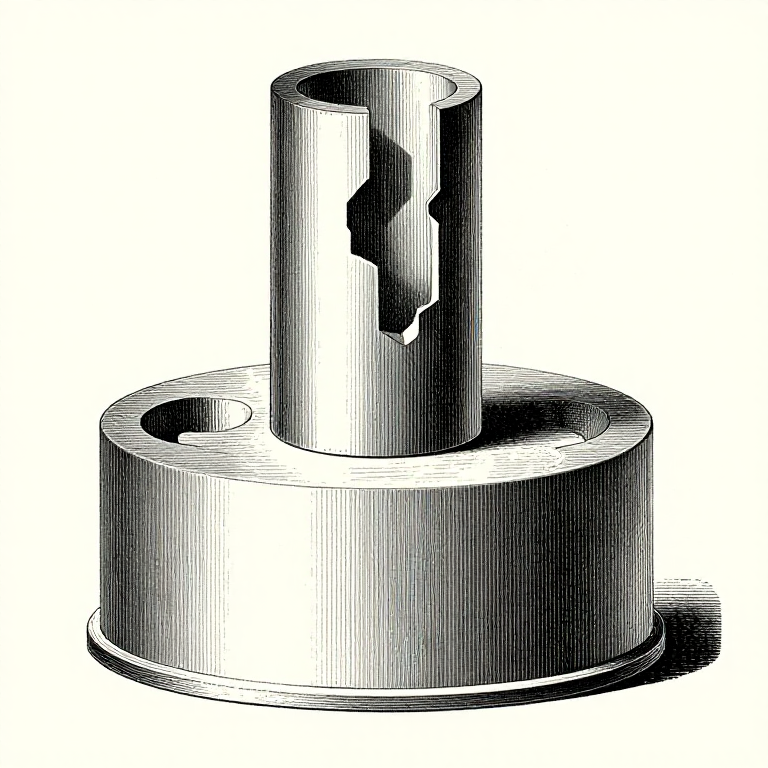


Risers: Metal Shrinks When It Freezes, and the Hole Goes Somewhere
Almost every metal occupies less space solid than liquid. Bronze loses about 5% of its volume on freezing, steel about 3%, aluminium about 6% — and that volume has to come from somewhere.
If there is no reservoir feeding the casting, it comes out of the casting itself: a cavity, usually in the last place to freeze, usually inside a thick section where it cannot be seen until the part is machined or breaks.
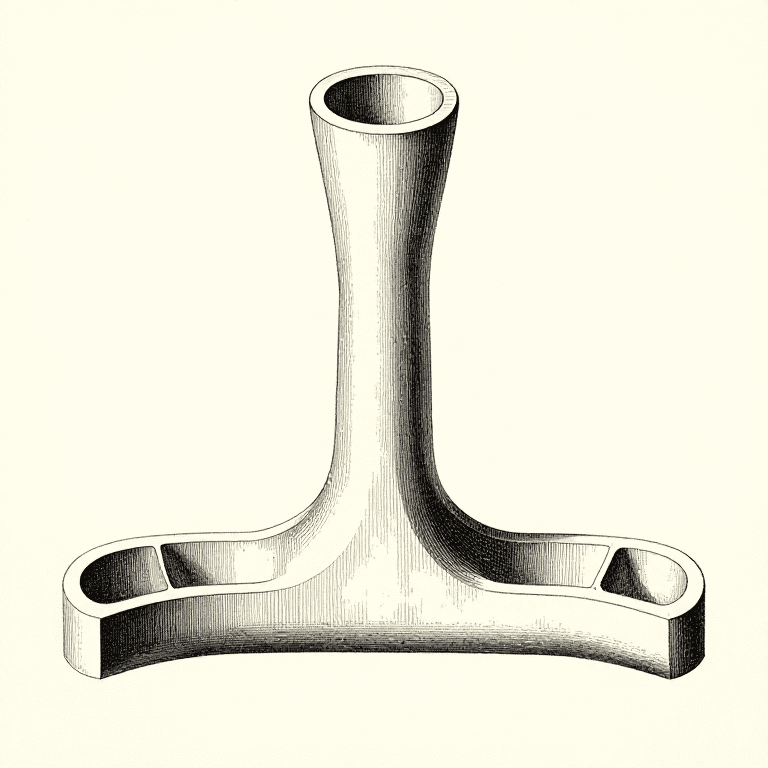
A RISER is that reservoir. It is a lump of extra metal, connected to the casting, designed to stay liquid LONGER than the part it feeds — so when the casting contracts, the hole forms in the riser and the riser is cut off and remelted.
Osezingeni eliphezulu
3 hours
Imiyalelo
1
1
The riser must freeze last, which means it must be chunkier
The riser must freeze last, which means it must be chunkier
Ilayisha incwadi ye-Jupyter…
Izinto zokwakha zalesi sinyathelo:
 Ingqimba yebhronzi1 ucezu
 Isihlabathi sokubumba1 kg
Amathuluzi adingekayo:
 Ikhompyutha Yasetafuleni
 I-Caliper Yedijithali Yamayintshi Ayi-6
 Ibhokisi lokubumba (elingaphezulu nelingaphansi)
2
2
Feed from the top, and keep the path open
Feed from the top, and keep the path open
Gravity does the feeding, so a riser feeds downward and sideways over a limited distance — roughly four times the section thickness along a plate, and less in alloys that freeze over a wide temperature range.
The connection between riser and casting — the riser NECK — must stay liquid until the casting has finished shrinking. A long thin neck freezes first and cuts the riser off from the part it was supposed to feed.
So the neck is short and generous, and the riser sits directly on or beside the heavy section. A riser placed at the end of a thin plate in the hope of feeding a boss at the other end feeds nothing at all.
Izinto zokwakha zalesi sinyathelo:
Isihlabathi sokubumba1 kgIngqimba yebhronzi1 ucezuAmathuluzi adingekayo:
Ibhokisi lokubumba (elingaphezulu nelingaphansi)I-Caliper Yedijithali Yamayintshi Ayi-63
3
Open risers, blind risers, and atmospheric pressure
Open risers, blind risers, and atmospheric pressure
An OPEN riser reaches the top of the mould, so air can push down on the metal as it feeds. It also lets you see when the mould is full and top it up at the end of the pour, which is genuinely useful.
A BLIND riser is enclosed in the sand. It stays hotter because it has no exposed surface, but as the metal drains out it needs air to replace it — otherwise a vacuum forms and stops the feeding.
That is what a WHISTLER or a permeable core in the riser top is for: a small passage that lets atmospheric pressure into the riser cavity. It is a small detail that makes the difference between a blind riser working and doing nothing at all.
Izinto zokwakha zalesi sinyathelo:
Isihlabathi sokubumba1 kgAmathuluzi adingekayo:
Ibhokisi lokubumba (elingaphezulu nelingaphansi) Irula
 I-Loupe Yokukhulisa
4
4
Budget the metal, including everything you cut off
Budget the metal, including everything you cut off
The gating and risers can easily weigh as much as the casting. That metal is not wasted — it is cut off and remelted — but it must be MELTED, and running out mid-pour ruins the casting and the mould together.
Weigh the pattern, multiply by the ratio of alloy density to pattern-material density, and add the gating and riser volumes. Then add a margin, because a crucible is never poured completely empty.
Write the actual numbers down after the pour: what went in, what came out as casting, what came off as gating. After a few pours those figures let you predict a melt accurately, which is the difference between a foundry that works and one that improvises.
Izinto zokwakha zalesi sinyathelo:
Ingqimba yebhronzi1 ucezu I-ingot ye-aluminium ecwengekile ngo-99,7 % engu-450 g1 ucezu
Amathuluzi adingekayo:
 Isikali Esinembile
 Imbiza Yokuncibilikisa
Izinto
3- 1 ucezuIsibambeli
- Isibambeli
- Isibambeli
Amathuluzi Adingekayo
7- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
Ama-blueprint ahlobene
Lama-blueprint abelana ngolwazi — amasu, izinto noma izimiso



CC0 Isizinda Somphakathi
Le blueprint ikhishwe ngaphansi kwe-CC0. Ukhululekile ukukopisha, ukuguqula, ukusabalalisa, nokusebenzisa ngaphandle kwemvume.
Sekela uMenzi ngokuthenga imikhiqizo nge-Blueprint yabo IKhomishane Yomenzi kumiswe ngabathengisi, noma dala inguqulo entsha yale Blueprint bese uyifaka njengoxhumaniso ku-Blueprint yakho ukuze wabelane ngemali engenayo.