སྒྱུ་རྩལ
མཛེས་སྡུག་དང་བདེ་ཐང
བཟོ་རིག
རིག་གནས་དང་ལོ་རྒྱུས
དགའ་སྟོན
ཁོར་ཡུག
ཟས་དང་བཏུང་རྫས
ཕྱིར་འཕྲུལ་རིག
ཚན་རིག
རྩེད་འགྲན
རིག་རྩལ
གྱོན་རུང
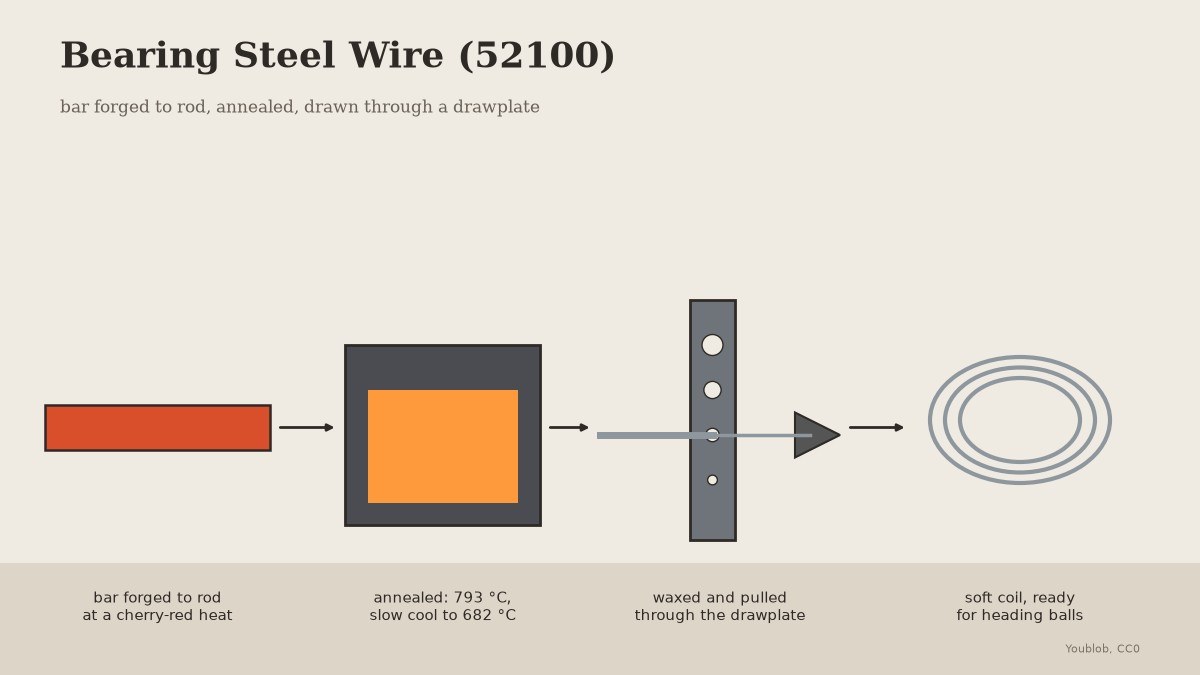


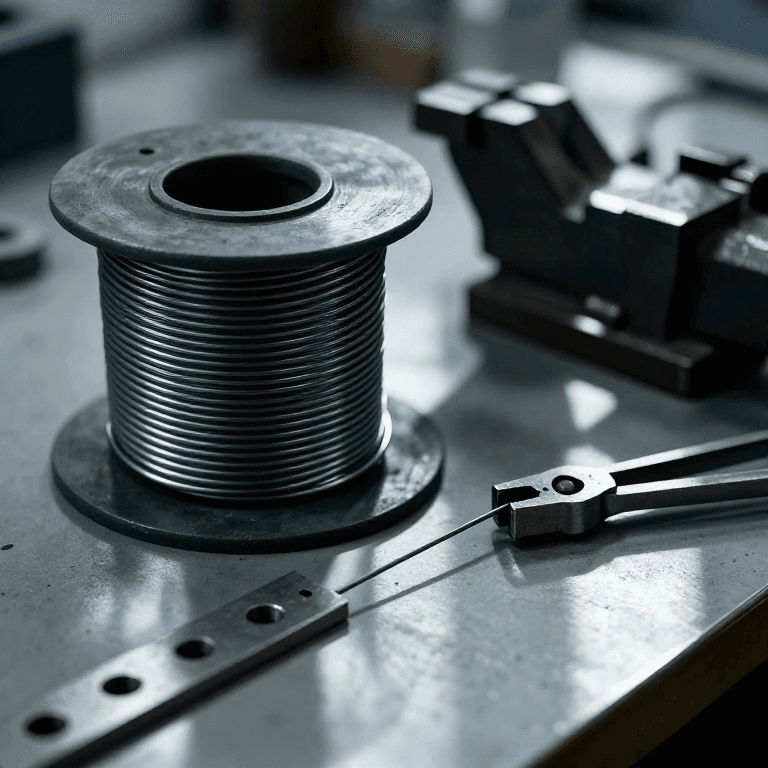
Bearing Steel Wire (52100): Drawn from Bar Through a Drawplate
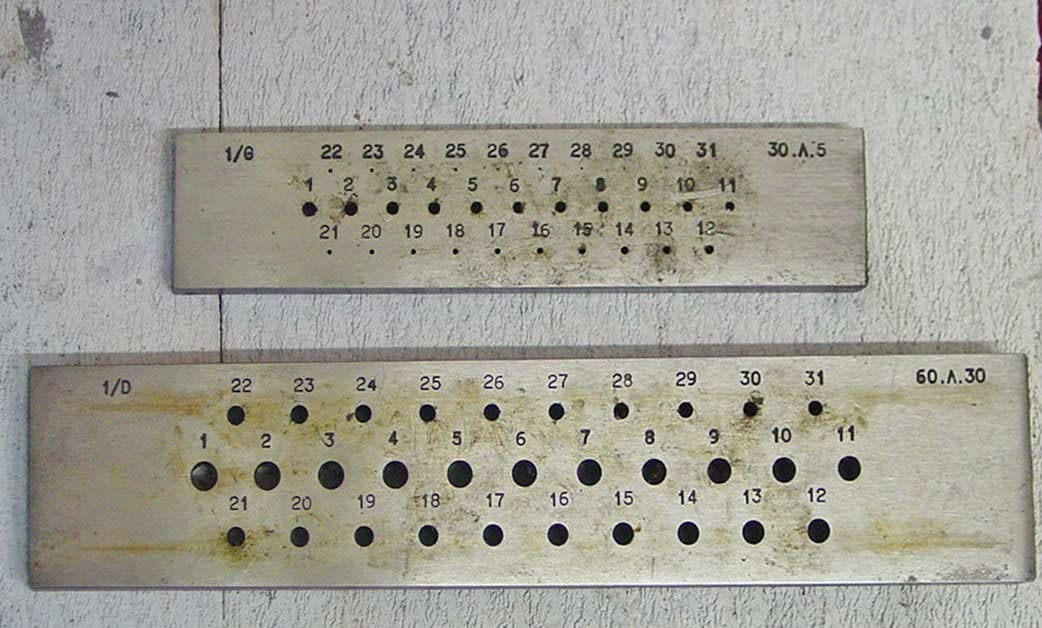
Bearing balls are headed from thick wire of 52100 steel. Here 52100 bar is forged to rod and drawn through a drawplate. At 1 % carbon it is much harder than mild steel, so it is annealed soft before drawing and again after every two holes, using the 52100 anneal Verhoeven recommends.
The picture: our drawing, bar to coil.
མཐོ་རིམ
2 days
ལམ་སྟོན
1
1
Forge to rod
Forge to rod
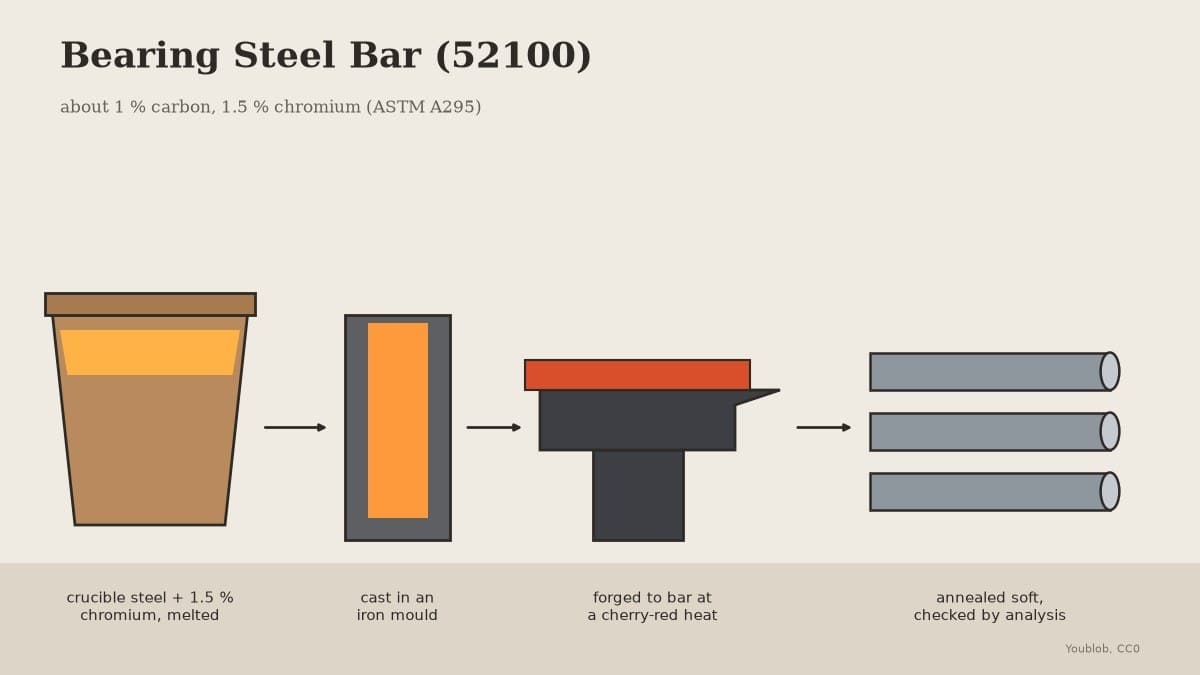
Heat the bar to a cherry-red heat and no hotter, and draw it out round on the anvil to a rod a little thicker than the drawplate's largest hole.
གོམ་པ་འདིའི་རྫས་རིགས:
 འཁོར་ལོ་གདན་ལྕགས་ཀྱི་ཤིང་རྡོ། (52100)1 kg
 སོལ་བ།1 as required
ལག་ཆས་དགོས་མཁོ:
 མགར་བའི་ཐབ་ཁུང་།
 མགར་བའི་རྡོ་ལེབ།
 རྒྱབ་ཐིག་གི་ཐོ་བ།
 མགར་བའི་ལག་བཟུང་།
 ཚག་གི་ལག་ཤུབས།
 ཉེན་སྲུང་མིག་ཤེལ།
2
2
Anneal
Anneal
In the oven, hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
ལག་ཆས་དགོས་མཁོ:
 ཚ་དྲོད་བཅོས་ཐབས་ཀྱི་ཐབ།
 ལྷག་ཆས་ཡོད་པའི་ཐར་མོ་ཀཔཱལ།མགར་བའི་ལག་བཟུང་།ཚག་གི་ལག་ཤུབས།
3
3
Clean and taper
Clean and taper
Brush off all the scale, then file a long taper on the first 3 cm so it passes the first hole.
ལག་ཆས་དགོས་མཁོ:
 ལྕགས་སྐུད་ཀྱི་ཕྱགས་མ་ཆ་ཚན།
 དར་མའི་ཚོགས་ཆས།
 ལས་ཅོག་གི་འཛིན་ཆས།
4
4
Wax and draw
Wax and draw
Clamp the drawplate in the vise. Wax the rod, push the taper through the first hole it does not slip through, and pull straight out with the draw tongs in one steady pull.
གོམ་པ་འདིའི་རྫས་རིགས:
 སྦྲང་ཞུན།20 g
ལག་ཆས་དགོས་མཁོ:
 ལྕགས་སྐུད་འཐེན་ནིའི་ལྕགས་ལེབ།
 འཐེན་ནིའི་ཀམ།ལས་ཅོག་གི་འཛིན་ཆས།
 ཀོ་བའི་ལས་ལག་ཤུབས།
5
5
Anneal every two holes
Anneal every two holes
Draw through each next hole without skipping. After every two holes, coil the wire and anneal it again: hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
གོམ་པ་འདིའི་རྫས་རིགས:
སྦྲང་ཞུན།1 དུམ་བུ།ལག་ཆས་དགོས་མཁོ:
ལྕགས་སྐུད་འཐེན་ནིའི་ལྕགས་ལེབ།འཐེན་ནིའི་ཀམ།ཚ་དྲོད་བཅོས་ཐབས་ཀྱི་ཐབ།ལྷག་ཆས་ཡོད་པའི་ཐར་མོ་ཀཔཱལ།6
6
Finish soft
Finish soft
Stop at the diameter your balls need, checked with the caliper, and give the coil a last anneal so it is soft for heading.
ལག་ཆས་དགོས་མཁོ:
 ཨང་རྟགས་ཚད་འཇལ་ཆས་ ཨིནཅི 6ཚ་དྲོད་བཅོས་ཐབས་ཀྱི་ཐབ།ལྷག་ཆས་ཡོད་པའི་ཐར་མོ་ཀཔཱལ།
7
7
Troubleshooting
Troubleshooting
Bearing steel wire troubleshooting.
Flow
Loading...
རྫས་རིགས
3- ས་ཆ་འཛིན
- 1 as requiredས་ཆ་འཛིན
- 1 དུམ་བུ།ས་ཆ་འཛིན
ལག་ཆས་དགོས་མཁོ
15- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
བིལུ་པིརིན་ཊི་འདི་གིས་བཟོ་མི
འབྲེལ་ཡོད་བིལུ་པིརིན་ཊི
བིལུ་པིརིན་ཊི་འདི་ཚུ་ཐབས་ལམ་དང་རྫས་རིགས། སྤྱི་ཆོས་བགོ་བཤའ་བྱེད
CC0 སྤྱི་དབང
བིལུ་པིརིན་ཊི་འདི་CC0 འོག་བཀྲམས་ཡོད། ཁྱེད་རང་གིས་ཆོག་མཆན་མ་བཞེས་པར་ཕབ་ལེན་དང་བཟོ་བཅོས། བགོ་བཤའ། དགོས་མཁོ་གང་ལའང་བཀོལ་སྤྱོད་བྱས་ཆོག
བཟོ་མཁན་ལ་རྒྱབ་སྐྱོར་བྱེད་པའི་ཆེད་ཁོང་ཚོའི་བིལུ་པིརིན་ཊི་བརྒྱུད་ཐོན་སྐྱེད་ཉོ། བཟོ་མཁན་གྱིས བཟོ་མཁན་གྱི་ཁེ་ཕོགས ཚོང་པས་གཏན་འཁེལ་བྱས་པ། ཡང་ན་བིལུ་པིརིན་ཊི་འདིའི་པར་གསར་བཟོས་ཏེ་ཁྱེད་རང་གི་བིལུ་པིརིན་ཊི་ནང་མཐུད་སྦྲེལ་བྱས་ཏེ་ཡོང་སྒོ་བགོ་བཤའ་བྱེད།