སྒྱུ་རྩལ
མཛེས་སྡུག་དང་བདེ་ཐང
བཟོ་རིག
རིག་གནས་དང་ལོ་རྒྱུས
དགའ་སྟོན
ཁོར་ཡུག
ཟས་དང་བཏུང་རྫས
ཕྱིར་འཕྲུལ་རིག
ཚན་རིག
རྩེད་འགྲན
རིག་རྩལ
གྱོན་རུང
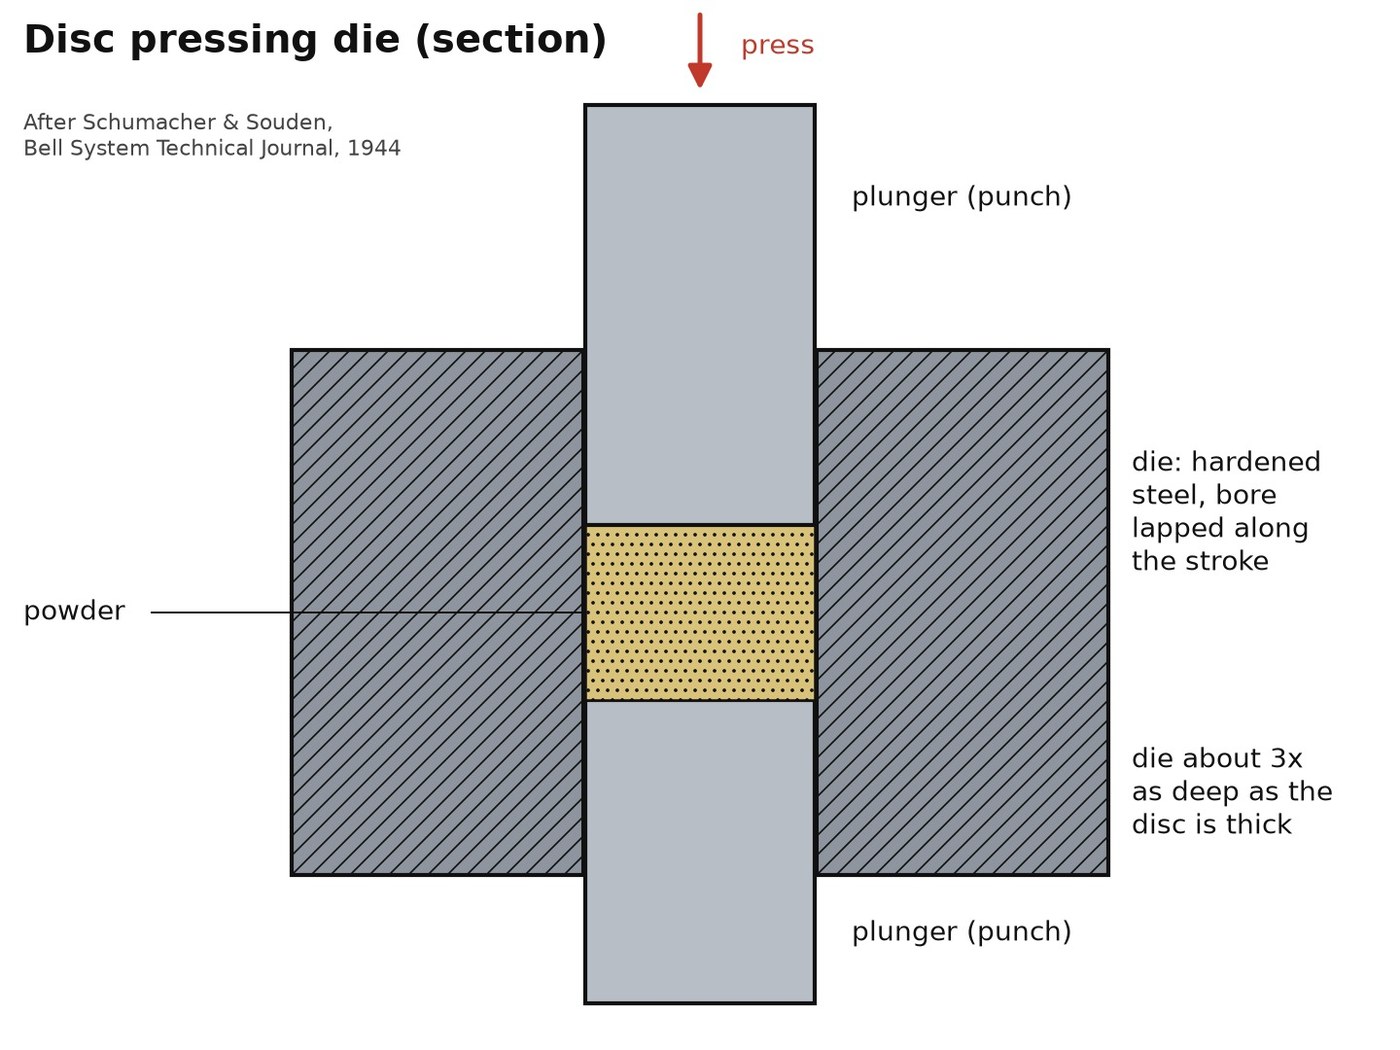

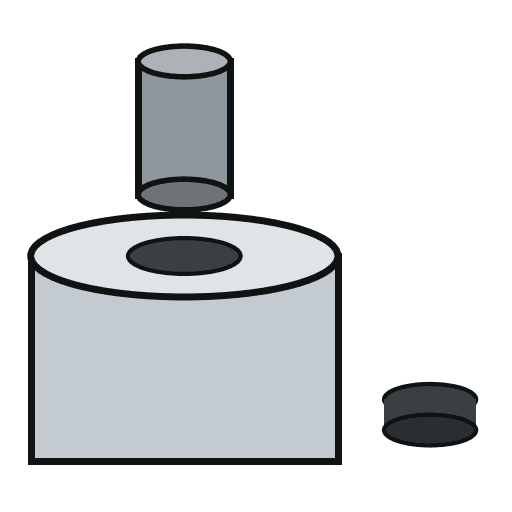
Disc Pressing Die: Hardened Steel, the Bore Lapped Along the Stroke (Schumacher & Souden, 1944)
The die in which powder is pressed into a flat disc: a block of hardened steel with a round bore, and close-fitting plungers that press the powder in it. The bore is lapped with rouge along the stroke, so its last fine scratches run the way the disc comes out.
Result: a die for pressing metal or ceramic powders into discs, at 5 to over 100 tons per square inch.
Source: E. E. Schumacher and A. G. Souden, Some Aspects of Powder Metallurgy, Bell System Technical Journal 23 (1944), pp. 431-433 and 454-455. Unknown: the steel, the hardening, sizes and clearances. Picture drawn by Youblob.
མཐོ་རིམ
Unknown
ལམ་སྟོན
1
1
Make the die and plungers
Make the die and plungers
Make the die of steel with a round bore through it, and plungers that fit the bore closely; there must be some clearance between them. Make the bore about three times as deep as the disc will be thick. Light, fluffy powders need a deeper die and longer plungers. Ours: tool steel for the die, and a lathe to bore and turn. Not given: the steel, sizes, clearance, the plungers' metal.
གོམ་པ་འདིའི་རྫས་རིགས:
 ལག་ཆས་ལྕགས་ཁར་གྱི་ཡུ་བ་གྲུ་བཞི།1 die
 མ་ཤེས་པའི་ལྕགས་རིགས།1 plungers
ལག་ཆས་དགོས་མཁོ:
 ལྕགས་ཀྱི་འཁྲུལ་འཁོར།
 མ་ཤེས་པའི་ཚད།
2
2
Harden the die
Harden the die
Harden the die. For very abrasive powders, make the die of hard carbide or line it with carbide instead. Ours: a heat-treating oven and a quench. Not given: the hardening heat and quench.
ལག་ཆས་དགོས་མཁོ:
 ཚ་དྲོད་བཅོས་ཐབས་ཀྱི་ཐབ།
 སྲ་བཟོའི་ཆུ་སྣོད།
3
3
Lap the bore along the stroke
Lap the bore along the stroke
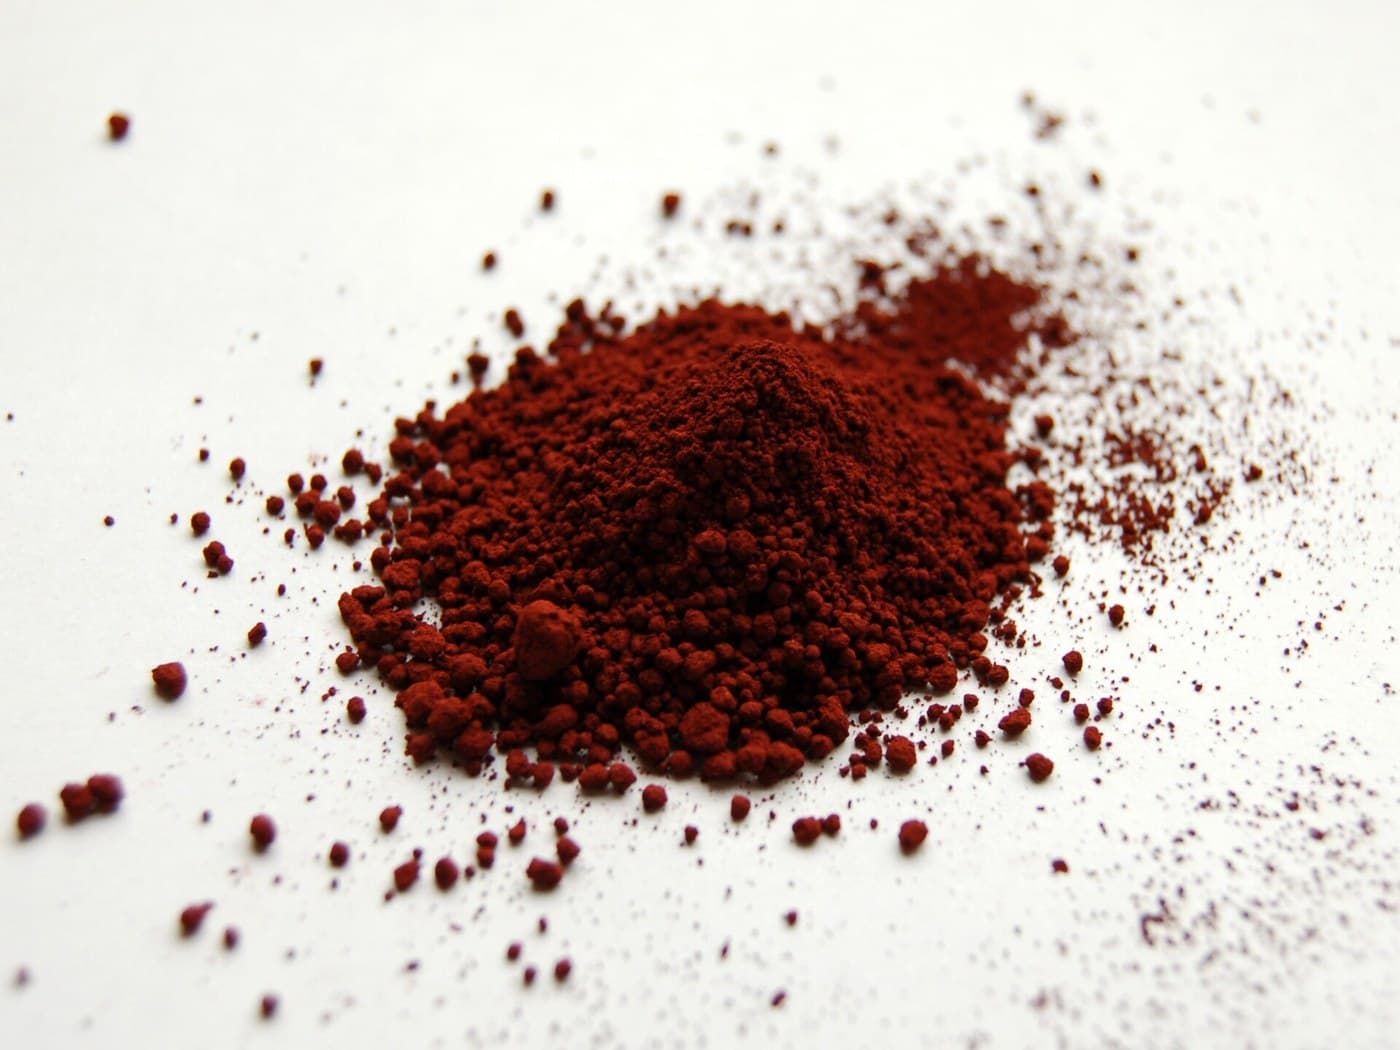
Polish the bore to a high finish by lapping with polishing rouge, moving the lap in the direction of the plunger stroke. The fine scratches that remain then run the way the pressed disc is pushed out, not across it.
ལག་ཆས་དགོས་མཁོ:
 གསེར་མགར་གྱི་འོད་བཟོ་ཚོས་དམར།
4
4
Press a disc
Press a disc
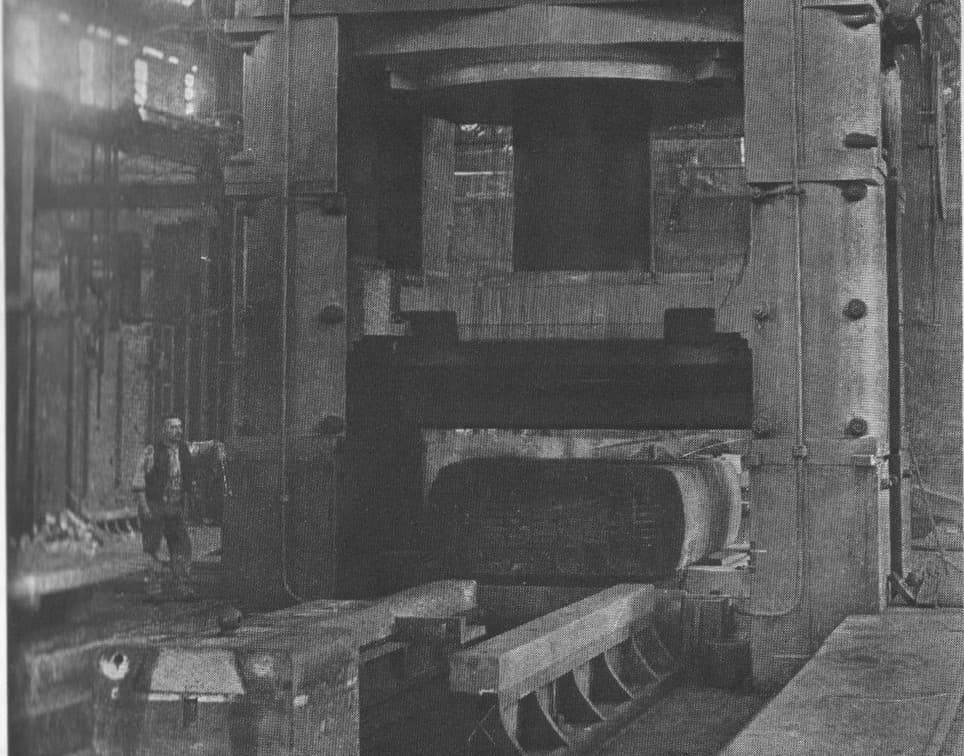
Fill the bore with powder and press it with the plungers in a mechanical or hydraulic press, at 5 to over 100 tons per square inch. The powder hardly flows sideways, and friction at the die wall makes the pressure uneven: a part that is long for its width may come out with a soft, less dense middle. Push the disc out along the bore.
ལག་ཆས་དགོས་མཁོ:
 ཧའི་ཌོ་ལིཀ་ནོན་འཕྲུལ།
རྫས་རིགས
2- ས་ཆ་འཛིན
- 1 plungersས་ཆ་འཛིན
ལག་ཆས་དགོས་མཁོ
6- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
མཐུད་སྦྲེལ་བིལུ་པིརིན་ཊི་རྫས་རིགས
འབུལ་ལམ 10%
Tool-Steel Bar: Crucible Steel Drawn Out at a Cherry-Red Heat
Forge གྱིས
མགར་བ།
༢༩
༠
༠
༠
༥
༠
འབུལ་ལམ 10%
Jewellers' Rouge Precipitated from Copperas, Ure 1839
Charlie གྱིས
སྲོག་མེད
༡༢
༠
༠
༠
༡
༠
འབུལ་ལམ 10%
Hydraulic Press
Emma གྱིས
ལྕགས་བཟོ
༥༠
༠
༠
༠
༡༠
༠

འབུལ་ལམ 10%
Building a Screw-Cutting Lathe — The Machine That Makes Other Machines
Gimli གྱིས
ལྕགས་བཟོ
༥༦
༠
༠
༠
༤
༠
བིལུ་པིརིན་ཊི་འདི་གིས་བཟོ་མི
CC0 སྤྱི་དབང
བིལུ་པིརིན་ཊི་འདི་CC0 འོག་བཀྲམས་ཡོད། ཁྱེད་རང་གིས་ཆོག་མཆན་མ་བཞེས་པར་ཕབ་ལེན་དང་བཟོ་བཅོས། བགོ་བཤའ། དགོས་མཁོ་གང་ལའང་བཀོལ་སྤྱོད་བྱས་ཆོག
བཟོ་མཁན་ལ་རྒྱབ་སྐྱོར་བྱེད་པའི་ཆེད་ཁོང་ཚོའི་བིལུ་པིརིན་ཊི་བརྒྱུད་ཐོན་སྐྱེད་ཉོ། བཟོ་མཁན་གྱིས བཟོ་མཁན་གྱི་ཁེ་ཕོགས ཚོང་པས་གཏན་འཁེལ་བྱས་པ། ཡང་ན་བིལུ་པིརིན་ཊི་འདིའི་པར་གསར་བཟོས་ཏེ་ཁྱེད་རང་གི་བིལུ་པིརིན་ཊི་ནང་མཐུད་སྦྲེལ་བྱས་ཏེ་ཡོང་སྒོ་བགོ་བཤའ་བྱེད།