
Zusammenarbeit
KUNST
SCHÖNHEIT & WELLNESS
HANDWERK
KULTUR & GESCHICHTE
UNTERHALTUNG
UMFELD
ESSEN & GETRÄNKE
REVERSE ENGINEERING
WISSENSCHAFTEN
SPORT
TECHNOLOGIE
WEARABLES
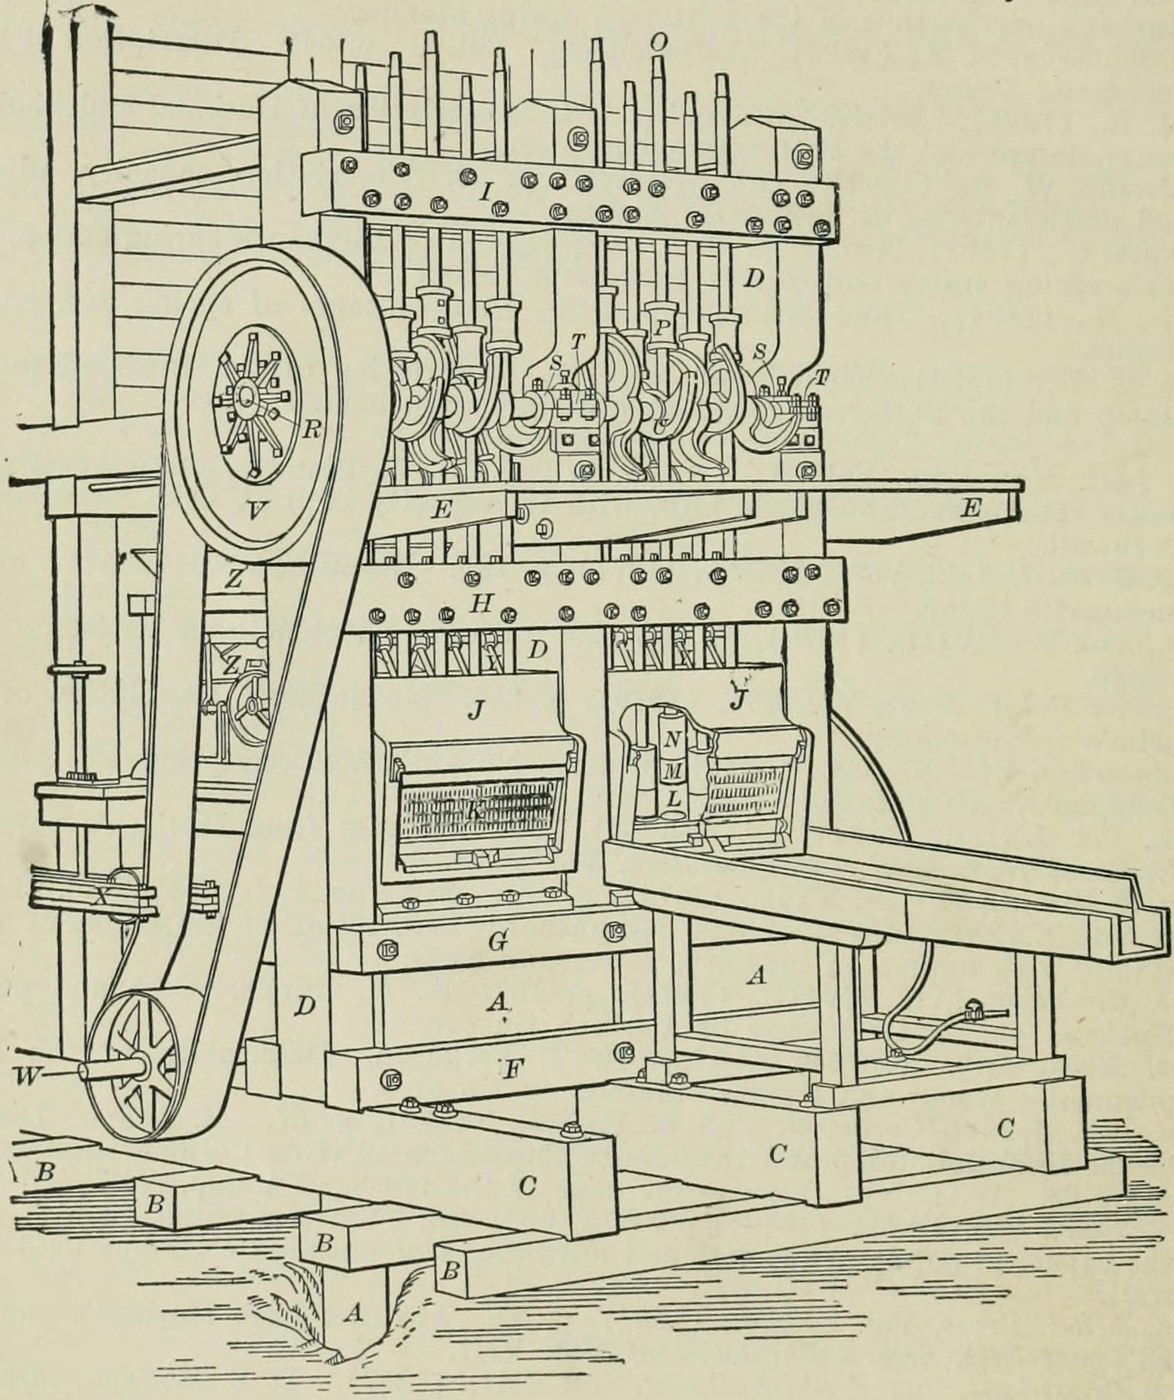
Stamp Mill: California Five-Stamp Battery (Richards, Ore Dressing 1903)
Forge

Erstellt von

Forge

3. November 2026NO
9
0
0
0
0

Stamp Mill: California Five-Stamp Battery (Richards, Ore Dressing 1903)

The gravity stamp mill: five heavy iron stamps stand in a cast-iron mortar on a timber block. Cams on a turning shaft lift each stamp by its tappet and let it fall by its own weight onto the ore on a die. Water washes the crushed ore out through a screen. Result: a stamp battery that pounds ore to sand, at 80 to 110 drops a minute. Source: R. H. Richards, Ore Dressing, vol. I (1903), Chapter V, Gravity Stamps. Unknown: one complete set of sizes; Richards gives the range found in the mills. Picture: Fig. 90 of the book.
Erfahren
Unknown

Anweisungen

1

Dig and level the foundation

Dig a trench in gravel, or blast one in rock, about 2 feet longer than the mortar block at each end and about 2 feet wider at each side. Level the bottom with tamped concrete, sand or clay. Concrete should be at least 30 inches thick, or it may crumble. Two layers of 2-inch plank spiked together may go on top.

Materialien für diesen Schritt:

BetonBeton1 levelling layer
BohleBohle1 two layers of 2-inch plank

Benötigte Werkzeuge:
SpatenSpaten
HammerHammer
2

Stand the mortar block

Stand timbers or planks on end in the trench as the mortar block, sized for one five-stamp mortar. The mills used everything from 30 x 30 inch squared timbers to 2 x 12 inch planks bolted together. Set vertical bolts 3 to 4 feet long into the block to hold the mortar down. Not given: the bolts' metal.

Materialien für diesen Schritt:

KantholzKantholz1 mortar block
Unbekanntes MetallUnbekanntes Metall1 hold-down bolts

Benötigte Werkzeuge:
MaulschlüsselsatzMaulschlüsselsatz
Unbekannte MaßeUnbekannte Maße
3

Build the frame

On mud sills and cross sills, stand the posts (end posts 12 x 24 inches in most mills) with buckstaves, a platform, and lower and upper guide timbers. The guides keep the stamp stems vertical. Fit finger bars on a jack shaft between the posts, so each stamp can be propped up under its tappet. The frame carries the cam shaft and the drive.

Materialien für diesen Schritt:

KantholzKantholz1 sills, posts, guide timbers, platform
Unbekanntes MetallUnbekanntes Metall1 bolts and jack shaft

Benötigte Werkzeuge:

MaulschlüsselsatzMaulschlüsselsatz
Unbekannte MaßeUnbekannte Maße
4

Set the mortar, dies and screen

Bed the cast-iron mortar on tarred blankets or sheet rubber on the mortar block, for an even bearing, and bolt it down. Put the dies in its bottom: cylinders on square foot plates that fill the floor of the mortar. Mount a screen of punched Russia sheet iron in a wooden frame over the opening in front.

Materialien für diesen Schritt:

EisengussteileEisengussteile1 mortar and five dies
NaturkautschukplatteNaturkautschukplatte1 packing
Russisches EisenblechRussisches Eisenblech1 screen

Benötigte Werkzeuge:

MaulschlüsselsatzMaulschlüsselsatz
5

Make the five stamps

Each stamp has four parts. The shoe is chilled cast iron, its butt cast in heavy chills and its shank in sand. The boss is tough cast iron, the shoe's diameter and often 18 inches long, with sockets for the shoe shank and the stem and two keyways for knock-out wedges. The stem is solid wrought iron or mild steel, turned true and tapered at both ends so it can be reversed. The tappet is cast iron, with a flange above and below, locked on the stem by a gib and keys. Put the extra weight in the boss. Louis designs for 11 to 14 pounds of stamp per square inch of die; the mills used stamps of 650 to 1,100 pounds.

Materialien für diesen Schritt:

EisengussteileEisengussteile1 shoes, bosses, tappets
SchmiedeeisenstangeSchmiedeeisenstange1 stems, gibs, keys

Benötigte Werkzeuge:

MetalldrehmaschineMetalldrehmaschine
Unbekannte MaßeUnbekannte Maße
6

Fit the cam shaft and drive

Turn a wrought-iron or steel cam shaft true, with a key seat, and key on five cams. Each cam usually has two arms with spiral lifting faces, cast iron with chilled faces or cast steel. Drive the shaft by a rubber belt from the main shaft, over a pulley of wood built on a cast-iron hub and flanges, with a tightener. Not given: the engine or wheel that turns the main shaft.

Materialien für diesen Schritt:

SchmiedeeisenstangeSchmiedeeisenstange1 cam shaft
EisengussteileEisengussteile1 cams, pulley hub and flanges
BohleBohle1 pulley rim
AntriebsriemenAntriebsriemen1 rubber belt

Benötigte Werkzeuge:

MetalldrehmaschineMetalldrehmaschine
MaulschlüsselsatzMaulschlüsselsatz
7

Add the water and the feed

Run one or two 1-inch water pipes into the back of the mortar, each with a plug cock that stays where it is set. Feed ore from the bin by a chute to an automatic feeder. One stamp trips the feeder when the ore layer on its die gets too thin, and a hand screw adjusts the point where it trips. Ore can also be fed by hand with a shovel.

Materialien für diesen Schritt:

WasserrohrWasserrohr1 water pipes
Unbekanntes VentilUnbekanntes Ventil1 plug cocks
Unbekanntes MetallUnbekanntes Metall1 feeder and chute

Benötigte Werkzeuge:

MaulschlüsselsatzMaulschlüsselsatz
SchaufelSchaufel
8

Set up each stamp

Lay a 3-inch plank on the dies and set the bosses on it. Lower the stems into them and tap each stem down with a hammer, a board guarding its top, then drop it a few times at a very low drop. Hoist the stamp, put the shoe in place with wooden staves around its shank, and drop it on the plank to drive the shoe home; the staves swell when wet and hold it. Swap the plank for a block as high as the drop. Slip the tappet on, turn the cam until the tappet rests on its point, drive the keys home and drop the stamp gently a few times.

Materialien für diesen Schritt:

HolzkeileHolzkeile1 staves

Benötigte Werkzeuge:

BohleBohle
HammerHammer
FlaschenzugFlaschenzug
9

Run the battery

Drop the stamps in order 1, 3, 5, 2, 4 (numbered from the left, standing behind the battery), so no two neighbours fall one after the other. The California practice is 80 to 110 drops a minute with a 5 to 9 inch drop. The cams turn the stamps as they lift, which evens out wear on shoes and dies. Lubricate the cams; soft soap with graphite is best. As shoes and dies wear, reset the tappets to restore the drop, and keep the height of discharge, from die to screen, the same.

Benötigte Werkzeuge:

GraphitpulverGraphitpulver
Unbekanntes MaterialUnbekanntes Material
MaulschlüsselsatzMaulschlüsselsatz

Materialien

12

Benötigte Werkzeuge

10

Dieser Bauplan stellt her

CC0 Gemeinfrei

Dieser Blueprint ist unter CC0 veröffentlicht. Sie dürfen dieses Werk für jeden Zweck frei kopieren, ändern, verbreiten und verwenden, ohne um Erlaubnis zu fragen.

Unterstützen Sie den Maker, indem Sie Produkte über seinen Blueprint kaufen, wo er eine Maker-Provision von Anbietern festgelegt, verdient. Oder erstellen Sie eine neue Iteration dieses Blueprints und verbinden Sie ihn in Ihrem eigenen Blueprint, um Einnahmen zu teilen.

Diskussion

(0)

Anmelden um an der Diskussion teilzunehmen

Kommentare werden geladen...