Colaboración
ARTE
BELLEZA Y BIENESTAR
ARTESANÍA
CULTURA E HISTORIA
ENTRETENIMIENTO
MEDIO AMBIENTE
COMIDA Y BEBIDAS
INGENIERÍA INVERSA
CIENCIAS
DEPORTES
TECNOLOGÍA
TECNOLOGÍA VESTIBLE
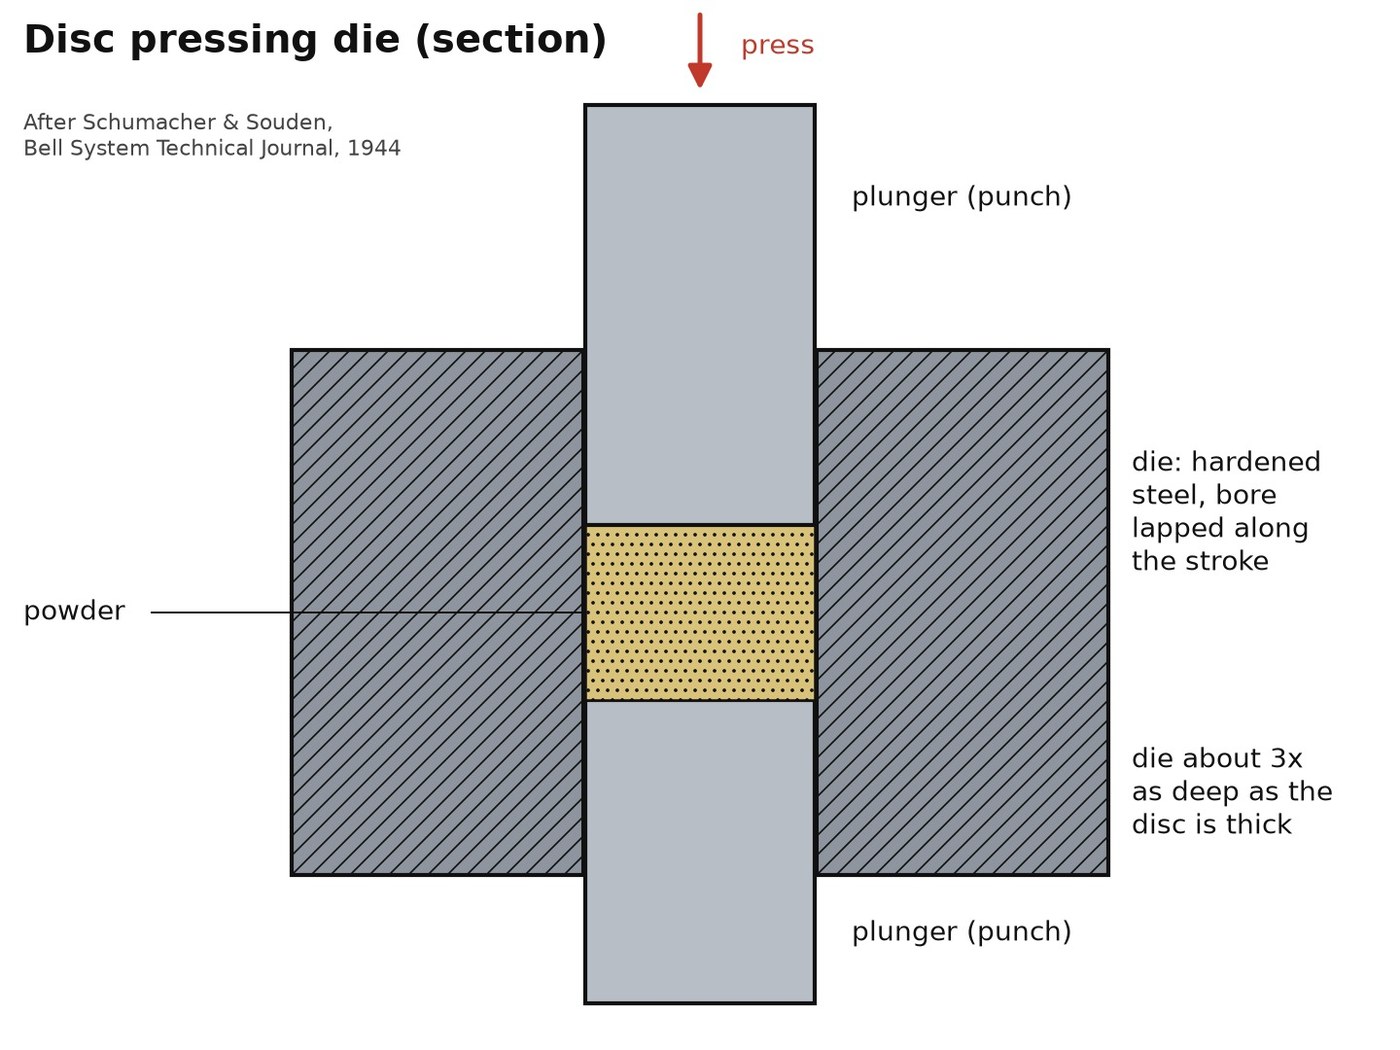

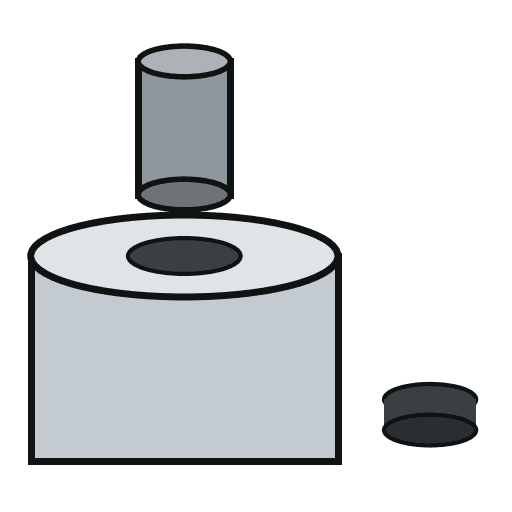
Disc Pressing Die: Hardened Steel, the Bore Lapped Along the Stroke (Schumacher & Souden, 1944)
The die in which powder is pressed into a flat disc: a block of hardened steel with a round bore, and close-fitting plungers that press the powder in it. The bore is lapped with rouge along the stroke, so its last fine scratches run the way the disc comes out.
Result: a die for pressing metal or ceramic powders into discs, at 5 to over 100 tons per square inch.
Source: E. E. Schumacher and A. G. Souden, Some Aspects of Powder Metallurgy, Bell System Technical Journal 23 (1944), pp. 431-433 and 454-455. Unknown: the steel, the hardening, sizes and clearances. Picture drawn by Youblob.
Avanzado
Unknown
Instrucciones
1
1
Make the die and plungers
Make the die and plungers
Make the die of steel with a round bore through it, and plungers that fit the bore closely; there must be some clearance between them. Make the bore about three times as deep as the disc will be thick. Light, fluffy powders need a deeper die and longer plungers. Ours: tool steel for the die, and a lathe to bore and turn. Not given: the steel, sizes, clearance, the plungers' metal.
Materiales para este paso:
 Barra cuadrada de acero para herramientas1 die
 Metal desconocido1 plungers
Herramientas necesarias:
 Torno de metal
 Dimensiones desconocidas
2
2
Harden the die
Harden the die
Harden the die. For very abrasive powders, make the die of hard carbide or line it with carbide instead. Ours: a heat-treating oven and a quench. Not given: the hardening heat and quench.
Herramientas necesarias:
 Horno de tratamiento térmico
 Cubo de temple
3
3
Lap the bore along the stroke
Lap the bore along the stroke
Polish the bore to a high finish by lapping with polishing rouge, moving the lap in the direction of the plunger stroke. The fine scratches that remain then run the way the pressed disc is pushed out, not across it.
Herramientas necesarias:
 Rojo de joyero
4
4
Press a disc
Press a disc
Fill the bore with powder and press it with the plungers in a mechanical or hydraulic press, at 5 to over 100 tons per square inch. The powder hardly flows sideways, and friction at the die wall makes the pressure uneven: a part that is long for its width may come out with a soft, less dense middle. Push the disc out along the bore.
Herramientas necesarias:
 Prensa hidráulica
Materiales
2- Marcador de posición
- 1 plungersMarcador de posición
Herramientas requeridas
6- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
Materiales de Blueprints conectados
10% de atribución
Tool-Steel Bar: Crucible Steel Drawn Out at a Cherry-Red Heat
por Forge
Herrero
32
0
0
0
5
0
10% de atribución
Jewellers' Rouge Precipitated from Copperas, Ure 1839
por Charlie
Inorgánico
12
0
0
0
1
0
10% de atribución
Hydraulic Press
por Emma
Trabajo en Metal
54
0
0
0
10
0

10% de atribución
Building a Screw-Cutting Lathe — The Machine That Makes Other Machines
por Gimli
Trabajo en Metal
57
0
0
0
4
0
Este plano hace
CC0 Dominio público
Este Blueprint se publica bajo CC0. Eres libre de copiar, modificar, distribuir y usar este trabajo para cualquier propósito, sin pedir permiso.
Apoya al Maker comprando productos a través de su Blueprint, donde gana una Comisión del Maker establecida por los vendedores, o crea una nueva iteración de este Blueprint e inclúyela como conexión en tu propio Blueprint para compartir ingresos.