
Collaboration
ART
BEAUTÉ ET BIEN-ÊTRE
ARTISANAT
CULTURE ET HISTOIRE
DIVERTISSEMENT
ENVIRONNEMENT
NOURRITURE ET BOISSONS
INGÉNIERIE INVERSE
SCIENCES
SPORTS
TECHNOLOGIE
TECHNOLOGIE PORTABLE
Forged Flat Drills: Tool Steel Drawn to Blade and Square Taper Head, Tempered by Colour for the Metal to Be Drilled (Edwinson, 1886)
Forge

Créé par

Forge

14. novembre 2026NO
8
0
0
0
0

Forged Flat Drills: Tool Steel Drawn to Blade and Square Taper Head, Tempered by Colour for the Metal to Be Drilled (Edwinson, 1886)

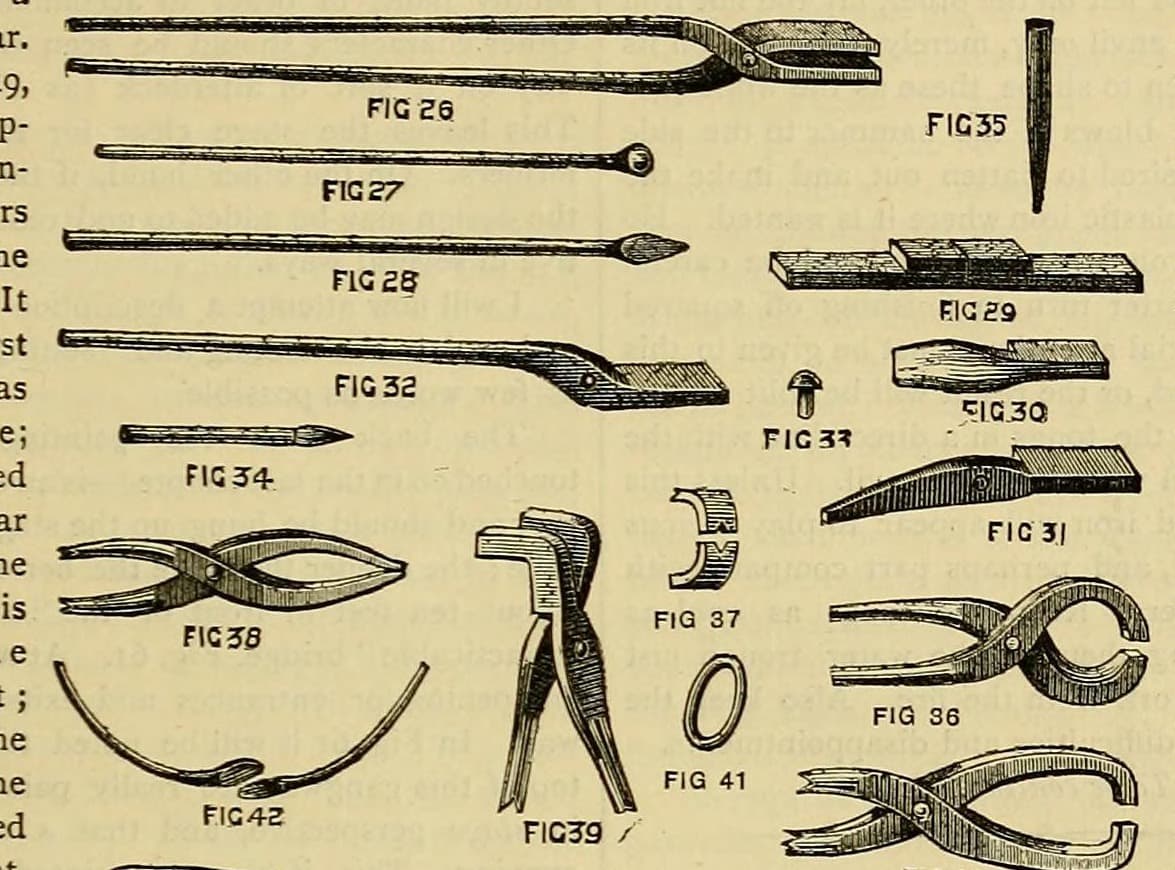
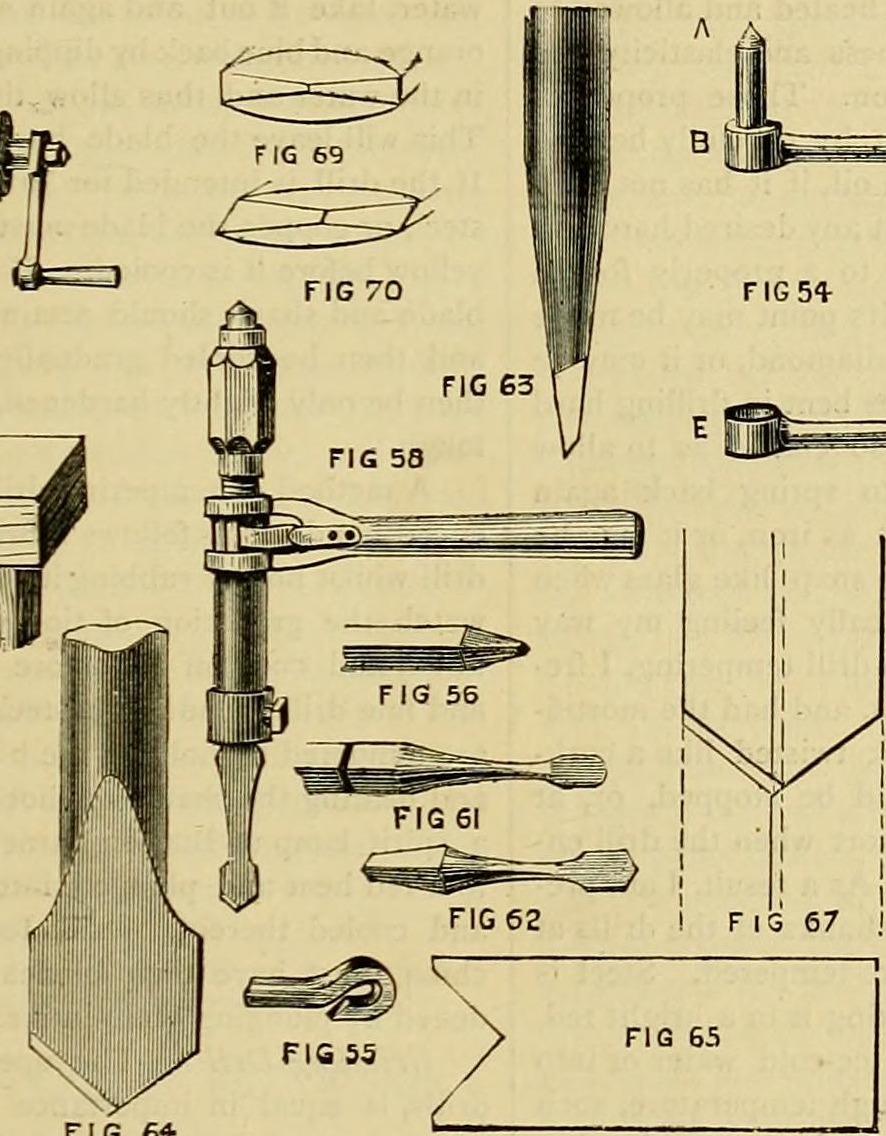
How a smith forged his own set of flat drills, from George Edwinson's series in Amateur Work (1886): 3/4 in. square tool steel drawn to a blade and shank with a square taper head, hardened in 45-50 F water and tempered by watching the colours run from a red-hot iron (pale straw for cast iron, orange yellow for wrought iron and copper, purplish yellow for wood), then ground to a notched gauge with clear corners.
Avancé
An hour or two per drill

Consignes

1

His sizes

Chargement du notebook Jupyter…
2

Read Edwinson

"A good drill may be made to turn out good work even when all other parts are indifferently made."
3

Draw the blade

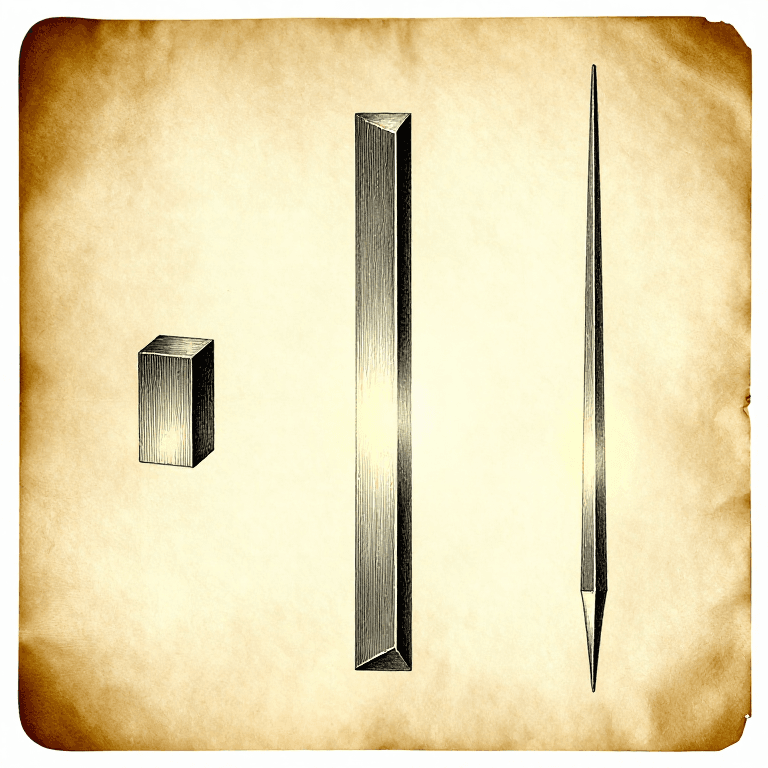
Cut a two-foot length of 3/4 in. (19 mm) square tool steel. Heat 3 in. to blood red in a clean fire, never hotter, and hammer only down to a dull red before reheating. Draw out the blade and shank first (fig. 61), close to shape.

Matériaux pour cette étape :

Barre d'acier à outilsBarre d'acier à outils1 pièce

Outils nécessaires :

Forge de forgeronForge de forgeron
EnclumeEnclume
MarteauMarteau
Pinces de forgeronPinces de forgeron
4

Forge the head

Cut off the length for the head, hold the blade and shank in grooved flat-bit tongs, and forge a square taper head to fit your brace socket, sides equal, shank and blade central. Finish at a dull red, set true, cool.

Outils nécessaires :

Tranche à chaudTranche à chaud
Forge de forgeronForge de forgeron
EnclumeEnclume
MarteauMarteau
Pinces de forgeronPinces de forgeron
5

Shape and substance

Taper gradually from head to shank, keep the shank even for an inch or two, then let the blade swell out and thin toward the point (figs. 62, 63). Blade about 1/16 in. at the point and 1/8 in. at the corners for a 1/4 in. drill, up to 3/16 in. for 1/2 or 3/4 in.; a 1/4 in. drill's shank half as thick as a 1/2 in. blade. Leave blades a little full for grinding.

Outils nécessaires :

Forge de forgeronForge de forgeron
EnclumeEnclume
MarteauMarteau
6

Harden

Heat to red and plunge the drill straight down into cool water of 45-50 F (7-10 C), holding it until cold: icy water makes the edges brittle. Brighten the blade and part of the shank on a brick or grit-stone.

Matériaux pour cette étape :

EauEau1 pièce

Outils nécessaires :

Forge de forgeronForge de forgeron
SeauSeau
ThermomètreThermomètre
Pierre à aiguiserPierre à aiguiser
7

Temper by colour

Lay the shank across a red-hot piece of stout iron and watch the tints run toward the blade: straw, yellow, orange yellow, purplish yellow, purple, blues. For cast iron and hard brass stop when pale straw reaches the blade, dipping the blade to hold the later colours back while the shank cools in air. For wrought iron, soft steel or copper let the blade reach orange yellow. For wood only, let blade and shank reach purplish yellow and cool slowly.

Matériaux pour cette étape :

EauEau1 pièce

Outils nécessaires :

Forge de forgeronForge de forgeron
Plaque de ferPlaque de fer
SeauSeau
8

Grind to a gauge

Cut gauges from thin sheet brass with notches at the point angles (figs. 65, 66): very obtuse for cast iron and hard brass, more acute for wrought iron, tough steel and copper. Grind both edges equal with the point on the centre line, and give the corners clearance (fig. 70). Grind each blade to its finished size.

Matériaux pour cette étape :

Feuille de laitonFeuille de laiton1 pièce

Outils nécessaires :

Limes (lime à main)Limes (lime à main)
Pierre à aiguiser à rouePierre à aiguiser à roue
9

Troubleshooting

Drill troubleshooting.

Flow

Loading...
10

History and honest limits

From George Edwinson, "Smithing and Forging" IV, **Amateur Work, Illustrated**, vol. V (1886), pp. 348-351 and figs. 54-70 (checked on the archive.org scan amateurworkillus05lond; the scan reads 3/4 in. bar where the OCR text says 1/2). He also hardened glass and china drills in mercury: left out here (mercury is a poison). Metric figures, the brass gauge stock and the thermometer are ours.

Matériaux

3

Outils requis

11

CC0 Domaine public

Ce blueprint est publié sous CC0. Vous êtes libre de copier, modifier, distribuer et utiliser ce travail pour tout usage, sans demander la permission.

Soutenez le Maker en achetant des produits via son Blueprint où il perçoit une Commission Maker définie par les Vendeurs, ou créez une nouvelle itération de ce Blueprint et incluez-le comme connexion dans votre propre Blueprint pour partager les revenus.

Commentaires

(0)

Se connecter pour participer à la discussion

Chargement des commentaires...