
Collaboration
ART
BEAUTÉ ET BIEN-ÊTRE
ARTISANAT
CULTURE ET HISTOIRE
DIVERTISSEMENT
ENVIRONNEMENT
NOURRITURE ET BOISSONS
INGÉNIERIE INVERSE
SCIENCES
SPORTS
TECHNOLOGIE
TECHNOLOGIE PORTABLE
V-Slide Tubing Cutter: Two Slide Halves Held on the Ways by One Spring Clip, a Reamer on the Frame (Thewes, 1938)
Forge

Créé par

Forge

13. novembre 2026NO
13
0
0
0
0

V-Slide Tubing Cutter: Two Slide Halves Held on the Ways by One Spring Clip, a Reamer on the Frame (Thewes, 1938)

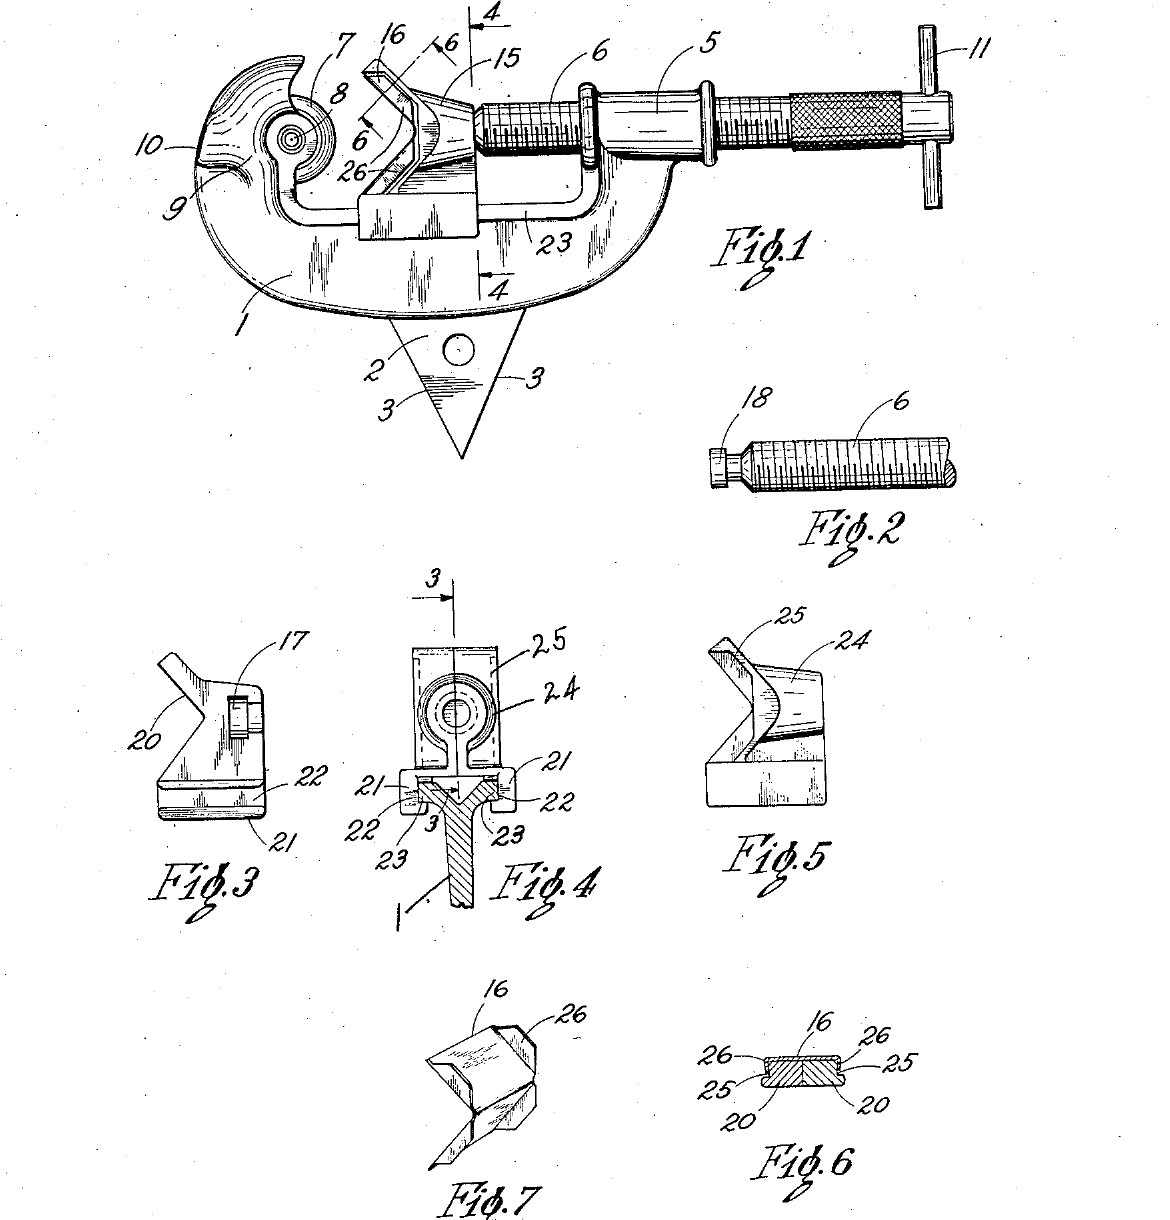
William O. Thewes of North Ridgeville, Ohio, received US 2,130,934, dated 20 September 1938 and assigned to The Ridge Tool Company, for a cutter for thin copper and brass tubing. A C-frame carries a cutting wheel at one end and a feed screw at the other. The screw pushes a V-slide that holds the tube against the wheel. The slide is two halves on ways along the frame, held together by one V-shaped spring clip, which is also the face the tube bears on. A triangular reamer on the side of the frame cleans the cut end, and the frame is its handle. We saw the frame from steel plate and pin the reamer in. His parts were die cast. All sizes are ours.
Intermédiaire
About 3 days

Consignes

1

Where the tube sits

Chargement du notebook Jupyter…
2

Read US 2,130,934

"With my improved cutter the ways or guides are integral with the frame and are uninterrupted throughout the length of the frame, and the slide is held in close sliding engagement on the ways without the use of bolts or rivets."
3

Print the template

Frame, slide half, end section, reamer and clip blank at 1:1 on A4, with the 8 and 28 mm tubes drawn in. print at 100 % (check the 50 mm bar).
Fichier de designPDFCC0 - Free
4

Saw out the frame

Glue the frame outline on 16 mm plate. Drill a row of holes inside the C, saw to them, and file to the line. Saw the 7 mm wheel slot down through the wheel post with two cuts, break out the middle and file it flat. Drill the 5 mm wheel pin and 4 mm tie pin holes across the slot. Drill 8.5 mm along the screw axis through the other post and tap it M10.

Matériaux pour cette étape :

Plaque d'acier douxPlaque d'acier doux1 pièce

Outils nécessaires :

Scie à métauxScie à métaux
Jeu de limesJeu de limes
Perceuse à colonnePerceuse à colonne
Étau de machineÉtau de machine
Jeu de foretsJeu de forets
Jeu de tarauds et filièresJeu de tarauds et filières
PointeauPointeau
Pointe à tracerPointe à tracer
Étau d'établiÉtau d'établi
Huile de coupeHuile de coupe
5

File the ways

Along the bottom bar, between the posts, file a groove 2 mm deep and 4 mm high in both faces, 3 mm below the top edge. This leaves a T-shaped rib along the top: the ways. Keep it straight and the same all along, so the slide runs smoothly from end to end.

Outils nécessaires :

Jeu de limesJeu de limes
Jeu de limes aiguillesJeu de limes aiguilles
Étau d'établiÉtau d'établi
Pied à coulisse numérique 6 poucesPied à coulisse numérique 6 pouces
6

Turn the cutting wheel

Chuck a tool steel bar and face it. Turn the end to 20 mm across for 10 mm, centre drill and drill a 5 mm hole 10 mm deep, and turn the edge to a 50 degree vee, 25 degrees each side, sharp in the middle of the 6 mm width. Part it off 6 mm long and take the burr off the hole.

Matériaux pour cette étape :

Barre d'acier à outilsBarre d'acier à outils1 pièce

Outils nécessaires :

Tour à métauxTour à métaux
Mandrin de tour à 3 morsMandrin de tour à 3 mors
Outil de coupe pour tourOutil de coupe pour tour
Bédane de tronçonnageBédane de tronçonnage
Jeu de forets à centrerJeu de forets à centrer
Jeu de foretsJeu de forets
Pied à coulisse numérique 6 poucesPied à coulisse numérique 6 pouces
Lunettes de sécuritéLunettes de sécurité
7

Make the reamer

Saw a triangle with 22 mm sides from 3 mm flat tool steel and drill its 4 mm hole. Grind each edge to a 60 degree bevel from both sides, so all three edges cut. Saw a 3 mm wide slot, 22 mm long and 8 mm deep, in the middle of the frame's bottom edge, 50 mm from the wheel end, and drill the 4 mm pin hole across it.

Matériaux pour cette étape :

Barre plate en acier à outilsBarre plate en acier à outils1 pièce

Outils nécessaires :

Scie à métauxScie à métaux
Touret à meulerTouret à meuler
Perceuse à colonnePerceuse à colonne
Jeu de foretsJeu de forets
Jeu de limesJeu de limes
Lunettes de sécuritéLunettes de sécurité
8

Harden and temper

Heat the wheel and the reamer to a cherry red, until a magnet no longer sticks, and quench it in water, moving it about. Rub it bright with a stone, warm it on a piece of steel plate over the fire, and quench again as soon as it turns a light straw colour.

Outils nécessaires :

ForgeForge
Tenailles de forgeTenailles de forge
Petit aimantPetit aimant
Baquet de trempeBaquet de trempe
EauEau
Pierre à aiguiserPierre à aiguiser
Gants de soudeurGants de soudeur
Lunettes de sécuritéLunettes de sécurité
9

Make the slide halves

Saw two pieces of 10 mm plate to the slide outline, one the mirror of the other, and file the V. On the inner face of each, saw and file a pocket for half the screw head and a slot for its neck. Saw and file a step along the bottom edge of each half so its lip fits the groove under the ways (end section on the template). File a shallow notch in the outer face of each half, beside the V, for the clip's tongues.

Matériaux pour cette étape :

Plaque d'acier douxPlaque d'acier doux1 pièce

Outils nécessaires :

Scie à métauxScie à métaux
Jeu de limesJeu de limes
Jeu de limes aiguillesJeu de limes aiguilles
Étau d'établiÉtau d'établi
Pied à coulisse numérique 6 poucesPied à coulisse numérique 6 pouces
Pointe à tracerPointe à tracer
10

Bend the V clip

Cut the clip blank from 0.5 mm spring steel strip. Bend the four tongues up at right angles, then fold the blank to 90 degrees on the dashed line, over the slide's V.

Matériaux pour cette étape :

Feuillard d'acier à ressortFeuillard d'acier à ressort1 pièce

Outils nécessaires :

Scie à métauxScie à métaux
Jeu de limesJeu de limes
Étau d'établiÉtau d'établi
Marteau à panne bombéeMarteau à panne bombée
11

Make the feed screw

Cut 120 mm of M10 threaded rod. Chuck it and turn the end to a 9 mm head 4 mm long on a 6 mm neck 3 mm long. Drill a 6 mm hole across the other end and push a 70 mm piece of 6 mm rod through it for the T-handle. Peen it both sides so it stays put.

Matériaux pour cette étape :

Tige filetéeTige filetée1 pièce
Rond en acier douxRond en acier doux1 pièce

Outils nécessaires :

Tour à métauxTour à métaux
Mandrin de tour à 3 morsMandrin de tour à 3 mors
Outil de coupe pour tourOutil de coupe pour tour
Bédane de tronçonnageBédane de tronçonnage
Perceuse à colonnePerceuse à colonne
Jeu de foretsJeu de forets
Marteau à panne bombéeMarteau à panne bombée
Scie à métauxScie à métaux
12

Assemble

Fit the wheel in its slot with the 5 mm pin, and the 4 mm tie pin above it, peened. Tap the reamer into its slot and pin it. Screw the feed screw through the boss. Put the halves on the ways from the sides, closing them round the screw head, and spring the clip over their V so its tongues snap into the notches. Oil the ways and the screw.

Matériaux pour cette étape :

Goupille cylindrique en acierGoupille cylindrique en acier3 pièces

Outils nécessaires :

Marteau à panne bombéeMarteau à panne bombée
PointeauPointeau
Étau d'établiÉtau d'établi
Huile de coupeHuile de coupe
13

Cut a copper tube

Mark a copper tube and hold it in a vice with soft jaws, or by hand for small tubes. Open the screw, drop the cutter over the tube, and screw the slide in until the wheel just touches. Turn the cutter once round, give the screw about a quarter turn, and go on until the tube parts. The wheel should run in its own groove; the end should be square and not squeezed oval. Clean the inside of the end with a deburring tool.

Matériaux pour cette étape :

Tube de cuivreTube de cuivre1 pièce

Outils nécessaires :

Étau d'établiÉtau d'établi

ÉbavureurÉbavureur
Pied à coulisse numérique 6 poucesPied à coulisse numérique 6 pouces
14

Ream the end

Hold the frame like a T-handle, put the reamer's point in the cut end, and turn it a few times to take off the fin the wheel has turned in.

Outils nécessaires :

Étau d'établiÉtau d'établi
15

Troubleshooting

Tubing cutter troubleshooting.

Flow

Loading...
16

History and honest limits

**William O. Thewes** of North Ridgeville, Ohio, US 2,130,934, dated 20 September 1938, filed 4 November 1935, assigned to The Ridge Tool Company. Earlier slides needed notched ways, which weaken the frame, or bolts that come loose; he claimed "a V block reciprocable on the guideway and comprising two sections, and a face plate clamping said sections together". A later certificate corrects "same" to "frame" and "base" to "boss". His frame and slide were die cast and the reamer cast into the frame; ours are sawn from plate and the reamer is pinned. The patent gives no sizes; all of ours are ours.

Matériaux

8

Outils requis

28

Fichiers de conception

1

CC0 Domaine public

Ce blueprint est publié sous CC0. Vous êtes libre de copier, modifier, distribuer et utiliser ce travail pour tout usage, sans demander la permission.

Soutenez le Maker en achetant des produits via son Blueprint où il perçoit une Commission Maker définie par les Vendeurs, ou créez une nouvelle itération de ce Blueprint et incluez-le comme connexion dans votre propre Blueprint pour partager les revenus.

Commentaires

(0)

Se connecter pour participer à la discussion

Chargement des commentaires...