همکاری
هنر
زیبایی و سلامت
صنایع دستی
فرهنگ و تاریخ
سرگرمی
محیط زیست
غذا و نوشیدنی
مهندسی معکوس
علوم
ورزش
فناوری
پوشیدنیها
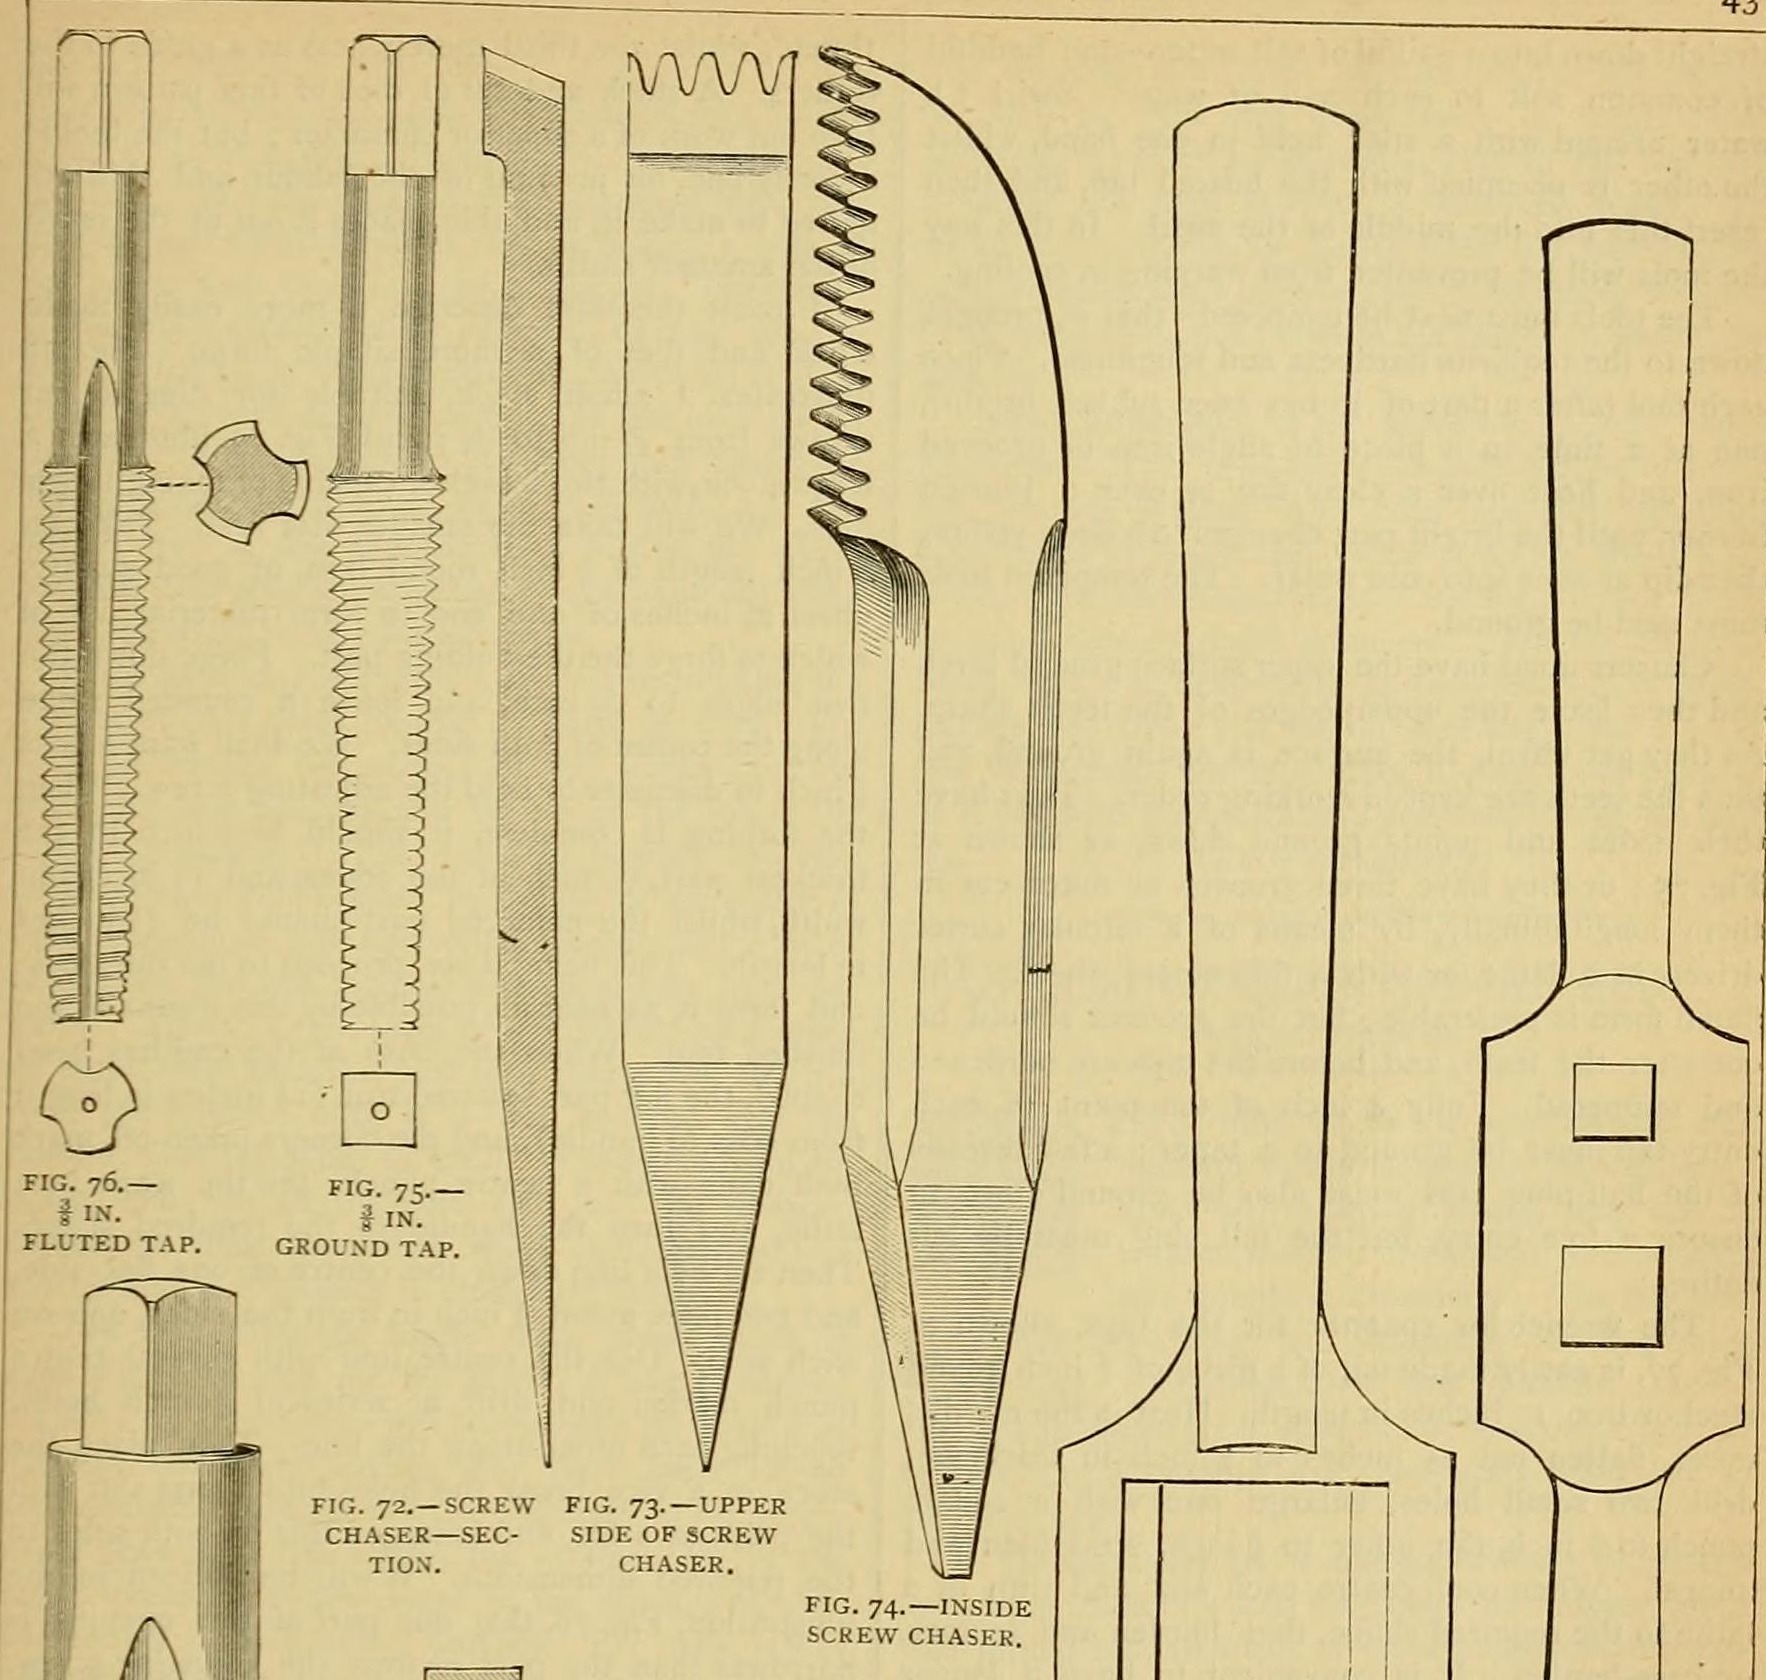


Whitworth Taps from Cast Tool Steel: Turned, Chased, Fluted and Hardened in Salt Water, with Their Wrench (Edwinson, 1886)
George Edwinson's instructions (Amateur Work, 1886) for a home-made set of Whitworth taps, 3/16 to 1 inch, in entry, half-plug and full-plug form: cast tool steel annealed, turned, roughed with a single-point tool and finished with home-made chasers in a screw-cutting lathe, fluted, hardened in swirled salt water and tempered deep yellow; plus the two-hole tap wrench. The dies and stock are in the companion blueprint.
پیشرفته
Several days for a set of thirty
دستورالعملها
1
1
His tables
His tables
در حال بارگذاری دفترچهٔ Jupyter…
2
2
Read Edwinson
Read Edwinson
"There is only one perfect method of making a good tap, and that is by turning the metal ... and cutting the thread in a screw-cutting lathe."
3
3
Cut and anneal the blanks
Cut and anneal the blanks
Cut the best 1 in. square cast tool steel into 3 1/2 in. lengths for the large taps, and 1/2 in. steel into 3 in. lengths for the small ones (a full set takes 5 ft 6 in. of the first and 3 ft of the second). Anneal: blood red, cooled slowly in hot ashes. File the ends square, centre-punch, and drill the centres 1/16 in. (small) or 1/8 in. (large) deep.
مواد مورد نیاز این مرحله:
 میلگرد فولاد ابزار1 قطعه
ابزارهای مورد نیاز:
 قلم داغ
 کورهٔ آهنگری
 سوهان (سوهان دستی)
 سنبهٔ نشانهگذاری
 دریل ستونی
4
4
Rough out the taps
Rough out the taps
Turn the corners off. Mark each tap: entry 1/2 in. head, 3/4 in. shank; half plug 1/2 in. head, 1 in. shank; full plug 1/2 in. head, 1 1/4 in. shank; the rest is thread (for the 1 in. set; 7/8 the same, smaller sets in proportion with shanks turned down for clearance). Below 1/2 in. make the square heads 3/8 or 3/16 in. to fit the wrench. Anneal again, turn true and smooth, and finish with a fine file.
ابزارهای مورد نیاز:
 تراش فلزسوهان (سوهان دستی)کورهٔ آهنگری
5
5
Make the chasers
Make the chasers
From flat tool steel forge one chaser per size, the largest 1 in. wide, 1/4 in. thick and 5 in. long, the rest a little smaller, with 3 1/2 or 4 1/2 teeth across the width and a tang for a wooden handle (fig. 72). Upset the point, grind, anneal, file the teeth, and finish them by running the chaser against a full plug tap or hub of that pitch in the lathe. Inside chasers: against a left-handed hub, or file off the lower leading edge of each tooth (fig. 74).
مواد مورد نیاز این مرحله:
میلگرد فولاد ابزار1 قطعهابزارهای مورد نیاز:
کورهٔ آهنگری سندان
 چکشسوهان (سوهان دستی)تراش فلز
6
6
Cut the threads
Cut the threads
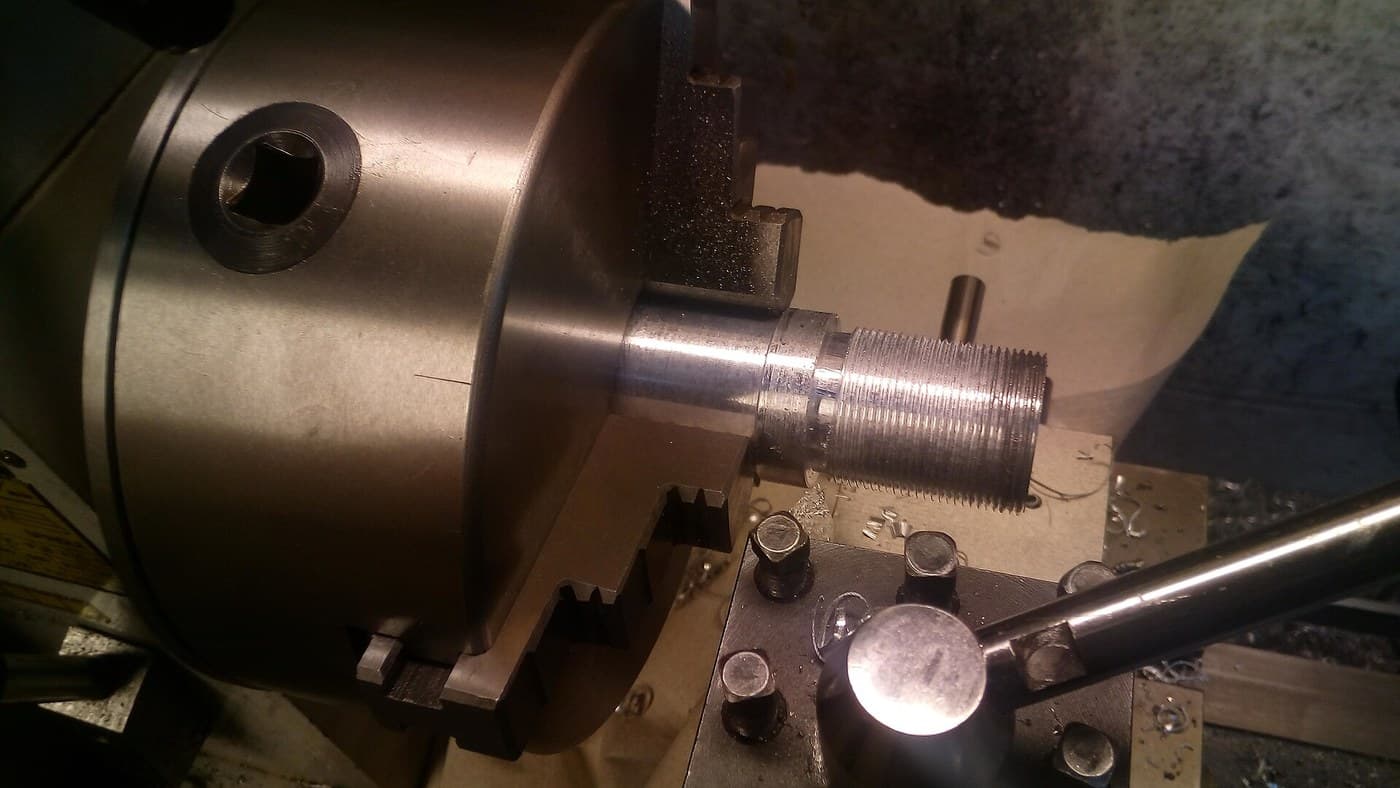
Rough each thread with a single fine-point tool in the slide rest of a screw-cutting lathe, set with the change wheels for its pitch (notebook), then finish with the chaser. Whitworth form: 55 degree angle, one-sixth rounded off top and bottom. Stamp each tap with its size and threads per inch.
ابزارهای مورد نیاز:
تراش فلزچکش7
7
Flute and point
Flute and point
Cut three flutes along each tap with a circular cutter in the lathe or a thin emery wheel (before hardening), or grind the sides flat (fig. 75). Grind fully 1/2 in. of each entry tap to a taper and the first few threads of the half plug; leave the full plug entire.
ابزارهای مورد نیاز:
تراش فلز سنگسنبادهٔ رومیزی
8
8
Harden and temper
Harden and temper
Heat each tap or chaser to blood red and plunge it straight down into a pail of water with a handful of common salt, swirled with a stick, into the middle of the swirl so it does not warp. Rub part bright, lay it in angle or grooved iron over a clear fire or a Bunsen burner until the bright part is deep yellow, then dip it in cold water. Grind the chaser tops level.
مواد مورد نیاز این مرحله:
 نمک1 قطعه
 آب1 قطعه
ابزارهای مورد نیاز:
کورهٔ آهنگری سطل
 چراغ بونزنسنگسنبادهٔ رومیزی
9
9
Make the tap wrench
Make the tap wrench
Take 10 in. of 3/4 in. round steel or iron. Heat the middle, upset it and flatten 2 1/2 in. to 1/2 in. thick. Drill two small holes and open them with a square punch, one to 3/8 in. and one to 1/4 in. Straighten, anneal, centre the ends and turn them in the lathe, then harden and temper. A longer, heavier wrench with one 1/2 in. hole suits the big taps.
مواد مورد نیاز این مرحله:
میلگرد فولاد ابزار1 قطعهابزارهای مورد نیاز:
کورهٔ آهنگریسندان پتکدریل ستونیتراش فلز
10
10
Troubleshooting
Troubleshooting
Tap troubleshooting.
Flow
Loading...
11
11
History and honest limits
History and honest limits
From George Edwinson, "Smithing and Forging" V, **Amateur Work, Illustrated**, vol. V (1886), pp. 434-438 and figs. 71-77 (checked on the archive.org scan amateurworkillus05lond). He himself advised buying Whitworth gear rather than making it. Metric conversions and the tools listed are ours.
این نقشه میسازد
نقشههای مرتبط
این نقشهها دانش مشترکی دارند — تکنیکها، مواد یا اصول

CC0 مالکیت عمومی
این نقشه تحت مجوز CC0 منتشر شده است. شما آزاد هستید آن را کپی، ویرایش، توزیع و برای هر هدفی بدون نیاز به اجازه استفاده کنید.
با خرید محصولات از طریق نقشه از سازنده حمایت کنید و او کمیسیون سازنده تعیین شده توسط فروشندگان، دریافت میکند یا یک نسخه جدید از این نقشه ایجاد کنید و آن را به عنوان اتصال در نقشه خود قرار دهید تا درآمد به اشتراک گذاشته شود.