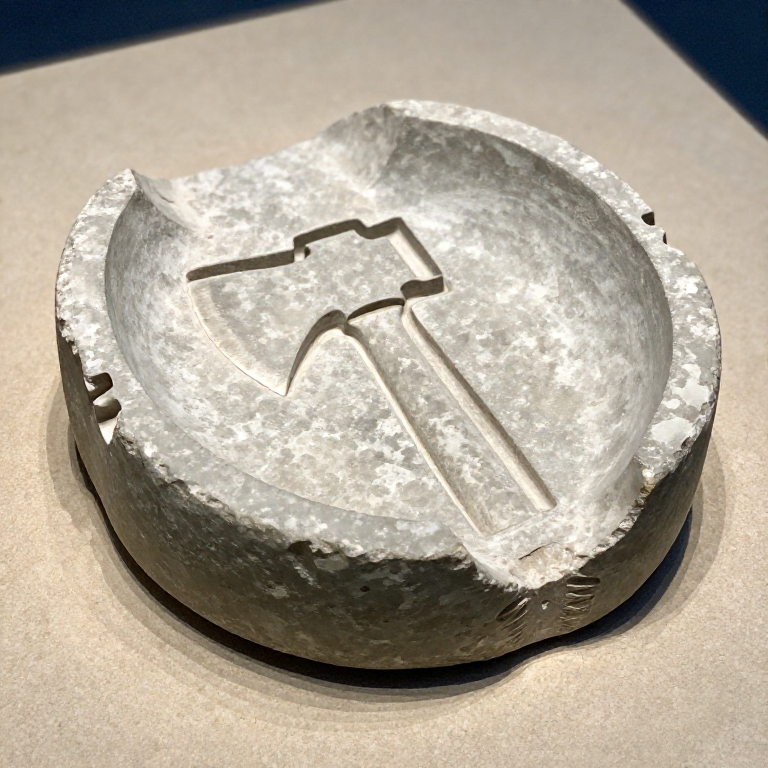


Carving a Stone Mould for Bronze Casting — Open-Face and Bivalve Moulds
Before lost-wax casting existed, Bronze Age metalworkers carved moulds directly into stone. Soapstone (steatite) was the preferred material — soft enough to carve with flint tools, yet heat-resistant enough to survive repeated pours of molten bronze at 1,000 °C.
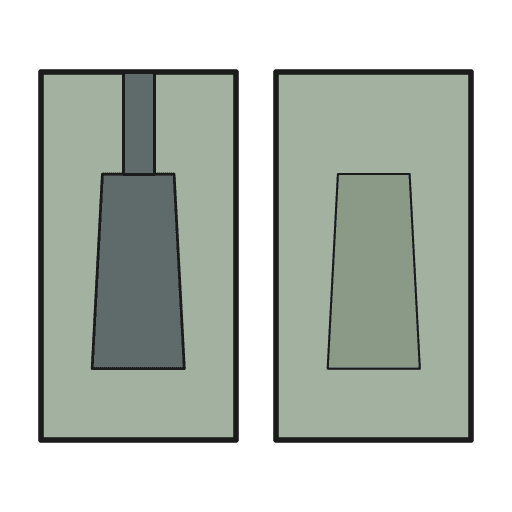
This blueprint covers both the simple open-face mould (one half, open top) and the more advanced bivalve mould (two matched halves clamped together for fully enclosed castings). The open-face mould produces flat-backed tools like axe heads and ingots. The bivalve mould produces symmetrical three-dimensional objects like spearheads and pins.
Alignment notches, vent channels, and pouring funnels are carved to ensure clean castings. A soot or tallow release coating prevents the bronze from bonding to the stone. A well-made stone mould can survive dozens of pours.
手順
Select a soapstone block
Select a soapstone block
このステップの材料:
 ソープストーンのブロック1 個
Flatten the mould face
Flatten the mould face
このステップの材料:
 砂岩(研磨材)1 個
Draw the object outline
Draw the object outline
Carve the cavity with flint tools
Carve the cavity with flint tools
必要な工具:
 敲石(ハンマーストーン)
Carve alignment notches (bivalve only)
Carve alignment notches (bivalve only)
Cut the pouring funnel
Cut the pouring funnel
Cut vent channels
Cut vent channels
Smooth the cavity surfaces
Smooth the cavity surfaces
このステップの材料:
 細砂100 g
必要な工具:
 なめらかな石
Apply release coating
Apply release coating
このステップの材料:
 動物脂(ヘット)50 g
Pre-heat the mould
Pre-heat the mould
Clamp and pour (bivalve)
Clamp and pour (bivalve)
Cool and demould
Cool and demould
接続ブループリントの材料
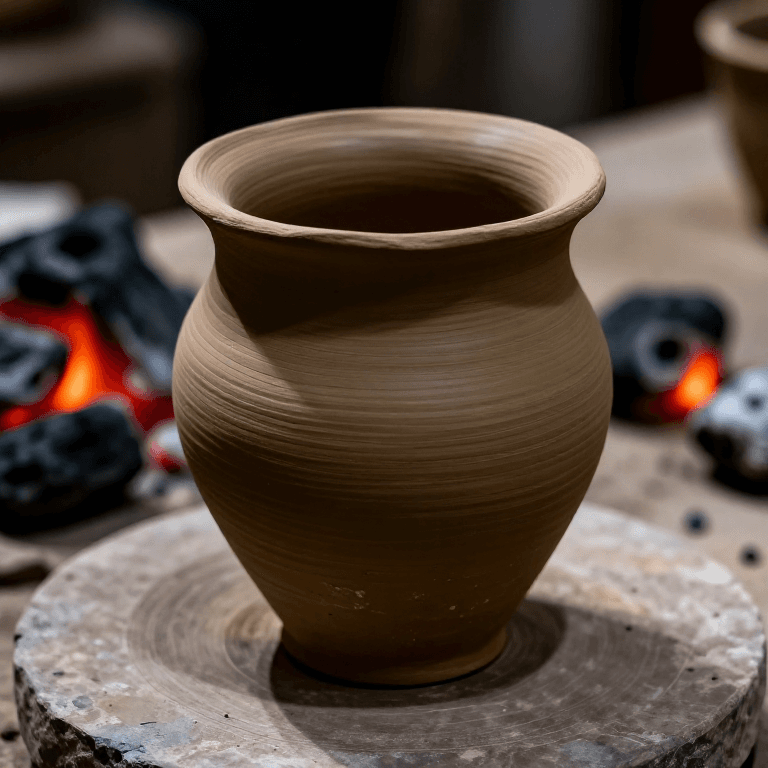
この設計図で作るもの
関連ブループリント
これらのブループリントは知識を共有しています — 技術、材料、原理
CC0 パブリックドメイン
このブループリントはCC0で公開されています。許可を求めずに、自由にコピー、修正、配布、あらゆる目的で使用できます。
メイカーを応援するには、ブループリント経由で製品を購入してください。メイカーには メイカーコミッション がベンダーにより設定されています。または、このブループリントの新しいイテレーションを作成し、自分のブループリントにコネクションとして含めて収益を共有できます。