アート
美容とウェルネス
工芸
文化と歴史
エンターテインメント
環境
食品と飲料
リバースエンジニアリング
科学
スポーツ
テクノロジー
ウェアラブル
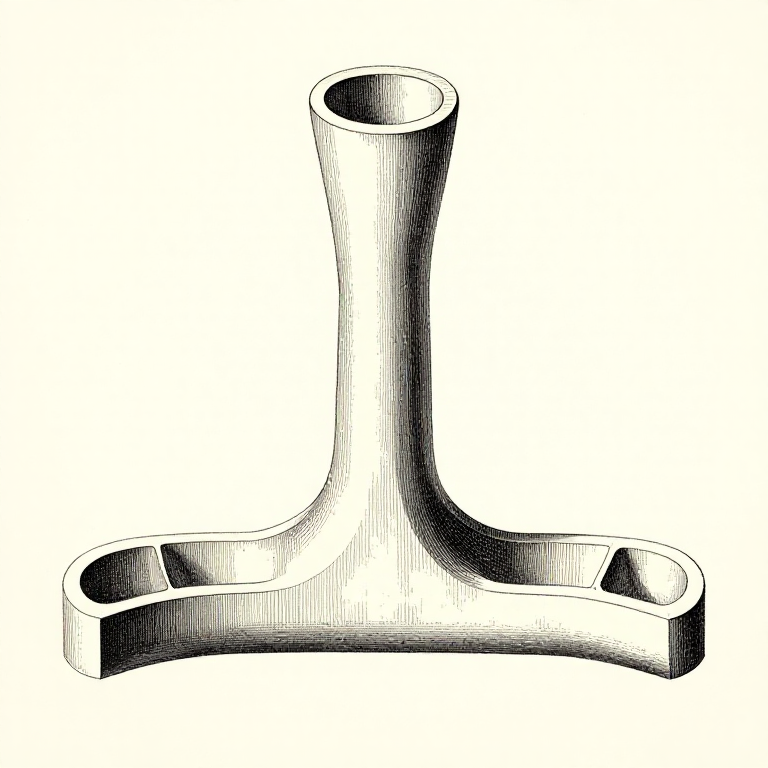


Gating: Getting the Metal In Without Wrecking the Mould
Molten metal poured straight into a cavity arrives fast, turbulent and full of air. It washes sand off the mould walls, folds oxide skin into itself, and the casting is full of inclusions before it has even frozen.
The GATING SYSTEM exists to prevent that. A sprue to take the metal down, a runner to carry it sideways and slow it, and gates to let it into the cavity smoothly — each part doing one job.
The governing principle is that the system should fill and stay full. A gating system running only partly full drags air in with the metal, which is precisely what it was built to avoid.
上級者
3 hours
手順
1
1
Sprue, runner, gate — three parts, three jobs
Sprue, runner, gate — three parts, three jobs
The SPRUE is the vertical channel the metal is poured into. It should be TAPERED, wider at the top, because falling metal accelerates and narrows — a parallel sprue leaves a gap around the stream that sucks in air.
The RUNNER is the horizontal channel at the bottom. It distributes metal and slows it down, and it is usually in the drag with the gates in the cope so that any floating dross stays in the runner.
The GATES are the small openings from runner into cavity. Several small gates fill more gently than one large one and let the mould fill from more than one place, which matters on anything long or thin.
このステップの材料:
 鋳物砂1 kg
必要な工具:
 鋳型枠(上型と下型)
 定規
 デジタルノギス 6インチ
2
2
Choke the system, and where
Choke the system, and where
Jupyter ノートブックを読み込み中…
このステップの材料:
 青銅のインゴット1 個鋳物砂1 kg
必要な工具:
 デスクトップパソコンデジタルノギス 6インチ鋳型枠(上型と下型)
3
3
Traps, filters and a pouring basin
Traps, filters and a pouring basin
A POURING BASIN at the top of the sprue lets you fill it and keep it full, so the sprue never runs empty mid-pour. Pouring straight into a bare sprue hole guarantees an interrupted, air-entraining stream at the start.
A runner extension beyond the last gate — a DIRT TRAP — gives the first, dirtiest metal somewhere to go that is not the casting. It costs a few centimetres of runner and catches the slag that came down the sprue first.
Ceramic foam FILTERS do the same job far better and are cheap. They also slow and smooth the flow, which is why a filter often improves a casting for two reasons at once.
このステップの材料:
鋳物砂1 kg必要な工具:
鋳型枠(上型と下型)定規 目の細かいあく取り
4
4
Pour steadily and keep the basin full
Pour steadily and keep the basin full
Start the pour and bring the basin up to full quickly, then hold it there until the mould is full. A pour that starts timidly and then speeds up entrains air at the very start, which is the metal that ends up deepest in the casting.
Never stop and restart. A pause lets the stream break, lets air in, and can leave a COLD SHUT where the metal that stopped has skinned over before the rest arrives.
Have enough metal melted before you start. Running out halfway is the single most avoidable failure in a foundry, and it is prevented by weighing the pattern, multiplying by the alloy's density ratio, and adding a generous allowance for the gating and risers — which is usually a third of the total again.
このステップの材料:
青銅のインゴット1 個 塊炭(木炭)1 個
必要な工具:
 鋳造用の柄杓
 るつぼばさみ
 鍛冶用遮光ゴーグル
 革製ガントレット手袋
関連ブループリント
これらのブループリントは知識を共有しています — 技術、材料、原理


CC0 パブリックドメイン
このブループリントはCC0で公開されています。許可を求めずに、自由にコピー、修正、配布、あらゆる目的で使用できます。
メイカーを応援するには、ブループリント経由で製品を購入してください。メイカーには メイカーコミッション がベンダーにより設定されています。または、このブループリントの新しいイテレーションを作成し、自分のブループリントにコネクションとして含めて収益を共有できます。