Ushirikiano
SANAA
UREMBO NA USTAWI
UJANJA
UTAMADUNI NA HISTORIA
BURUDANI
MAZINGIRA
CHAKULA NA VINYWAJI
UHANDISI WA KINYUME
SAYANSI
MICHEZO
TEKNOLOJIA
VAZI
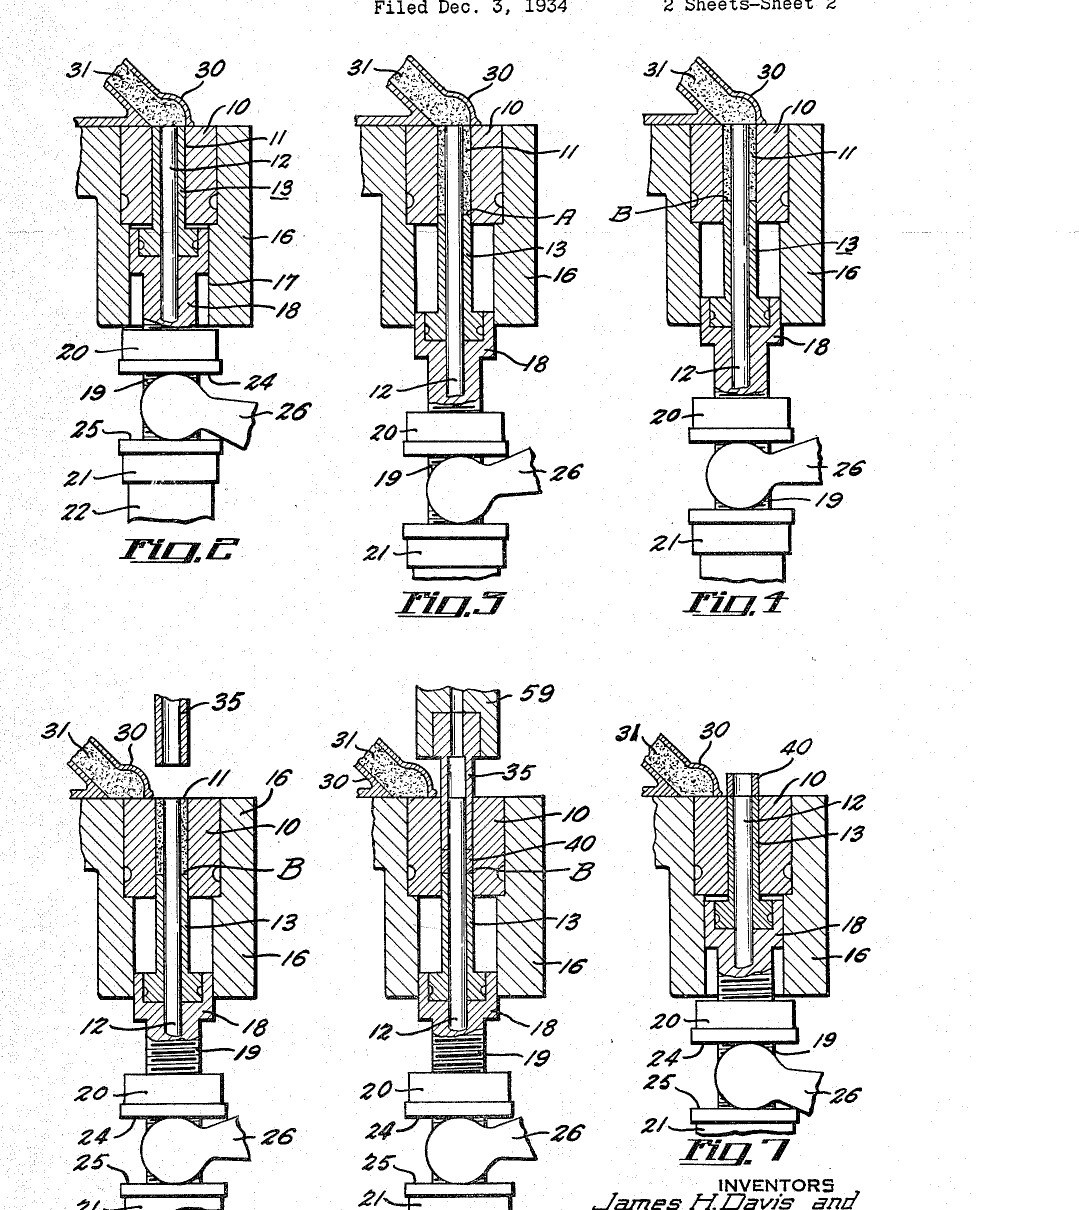

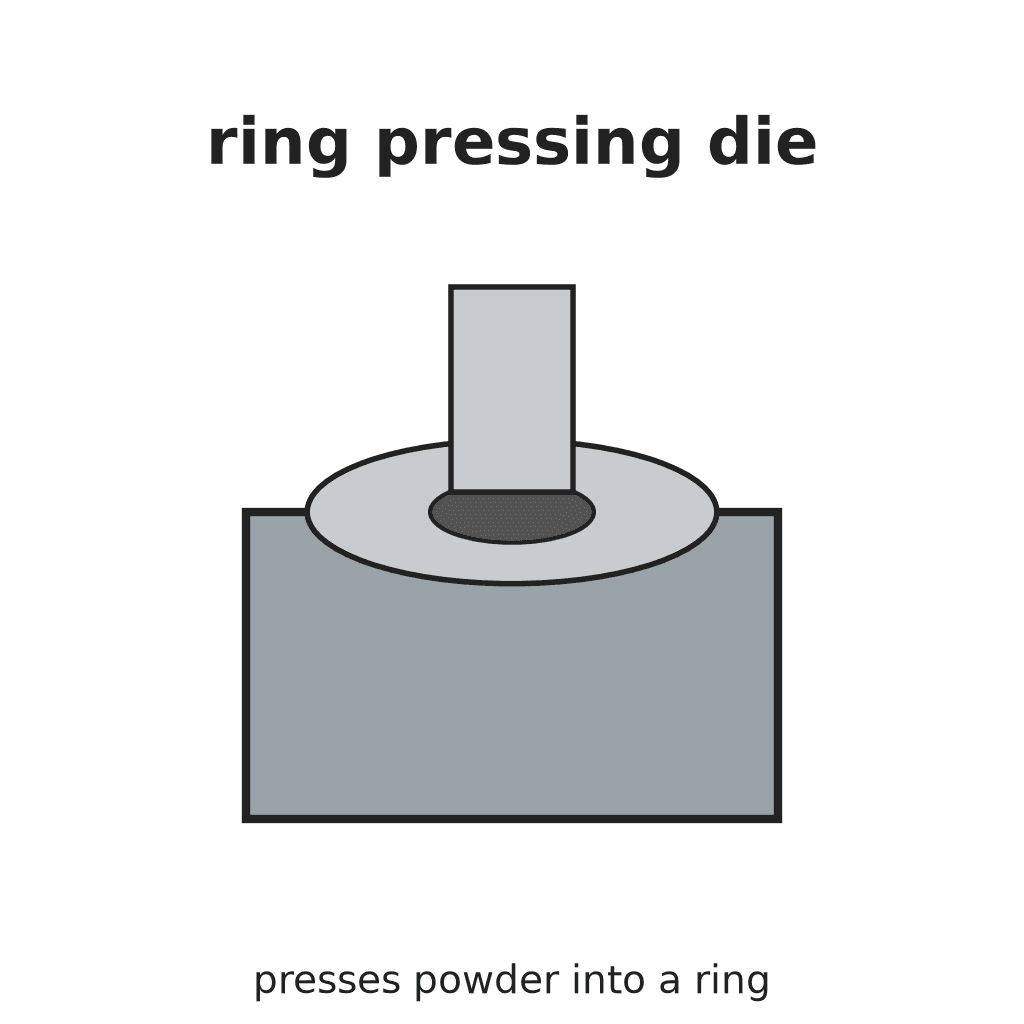
Ring Pressing Die: Core-Rod Die with Tubular Punches and Overfill Filling (Davis & Lemming, GM, US 2,127,994, 1938)
The die set for pressing metal or other powder into rings (bushings, ring cores). A die with a round cavity has a fixed core rod standing up through its middle, so the cavity is ring-shaped; a tube-shaped lower plunger slides up and down round the core rod, and a tube-shaped upper punch comes down to press. Filling is the trick: the lower plunger drops past the pressing point under a shaking shoe of powder, then rises a little to push the surplus back, so every ring gets the same charge with no trapped air.
Result: a die that presses powder into rings of even weight and density, ejected flush with the die top.
Source: J. H. Davis and J. C. Lemming (General Motors), US 2,127,994 (1938). Unknown: steels, sizes, clearances, pressure. Picture: the patent drawing.
Juu
Unknown
Maagizo
1
1
Make the die, core rod and punches
Make the die, core rod and punches
Make a die block with a straight round cavity open at both ends. Make a core rod that stands up through the middle of the cavity, its top flush with the die top, threaded at its foot to be anchored in the base with a lock nut. Make a tube-shaped lower plunger that slides in the cavity round the core rod, and a tube-shaped upper punch to match. Not given: the steel, sizes, clearances. Ours: tool steel, turned and threaded on the lathe.
Vifaa kwa hatua hii:
 Kipande cha mraba cha feleji ya zana1 die, core rod, punches
 Metali isiyojulikana1 lock nut
Zana zinazohitajika:
 Kereza ya Chuma
 Seti ya kukata nyuzi za skrubu
 Vipimo visivyojulikana
2
2
Harden and finish
Harden and finish
The powder wears the cavity wall, so harden the die and punches and polish the working faces. Not given: the hardening or finish. Ours: a heat-treating oven and quench, then lapping with rouge along the stroke as for the disc die.
Zana zinazohitajika:
 Tanuri ya kutibu kwa joto
 Ndoo ya kupoza chuma
 Rangi nyekundu ya sonara
3
3
Set it in the press
Set it in the press
Fix the die in a heavy table, anchor the core rod in the base through the lower plunger, and drive the lower plunger up and down by a cam lever. Fix the upper punch to the press crosshead. Beside the die, pivot a filling shoe full of powder that can swing over the cavity and shake. Ours: a punch press.
Zana zinazohitajika:
 Mkandamizo wa kutoboa
4
4
Fill, press and eject
Fill, press and eject
Start with the lower plunger right up, filling the cavity. Swing the shaking shoe over and lower the plunger: the powder falls in after it by gravity and suction, so no air is trapped. Take the plunger below the pressing position, then raise it to the pressing position, pushing the surplus back into the shoe so every charge is the same. Swing the shoe away, bring down the upper punch to press the ring between the punches, lift the punch and raise the lower plunger to push the ring out flush with the die top; the returning shoe sweeps it aside. Sinter the rings afterwards.
Zana zinazohitajika:
Mkandamizo wa kutoboaVifaa
2- 1 die, core rod, punchesKishikilia Nafasi
- 1 lock nutKishikilia Nafasi
Zana Zinazohitajika
7- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
- Kishikilia Nafasi
Vifaa vya Michoro Iliyounganishwa
Usambazaji 10%
Tool-Steel Bar: Crucible Steel Drawn Out at a Cherry-Red Heat
na Forge
Mhunzi
32
0
0
0
5
0

Usambazaji 10%
Building a Screw-Cutting Lathe — The Machine That Makes Other Machines
na Gimli
Uchimbaji chuma
57
0
0
0
4
0

Usambazaji 10%
Taps and Dies Cut on the Lathe, with Wrench and Stock
na Martin
Uchimbaji chuma
25
0
0
0
6
0
Mchoro huu unatengeneza
CC0 Umma Wote
Mchoro huu umetolewa chini ya CC0. Uko huru kunakili, kubadilisha, kusambaza, na kutumia kazi hii kwa madhumuni yoyote, bila kuomba ruhusa.
Saidia Mtengenezaji kwa kununua bidhaa kupitia Mchoro wao ambapo wanapata Kamisheni ya Mtengenezaji iliyowekwa na Wachuuzi, au unda marudio mapya ya Mchoro huu na uiunganishe kama kiungo katika Mchoro wako kuchangia mapato.