កិច្ចសហប្រតិបត្តិការ
សិល្បៈ
សម្រស់ និង សុខុមាលភាព
សិប្បកម្ម
វប្បធម៌ និង ប្រវត្តិសាស្ត្រ
ការកម្សាន្ត
បរិស្ថាន
ម្ហូប និង ភេសជ្ជៈ
វិស្វកម្មបញ្ច្រាស
វិទ្យាសាស្ត្រ
កីឡា
បច្ចេកវិទ្យា
ប្រដាប់ដែលស្លៀក
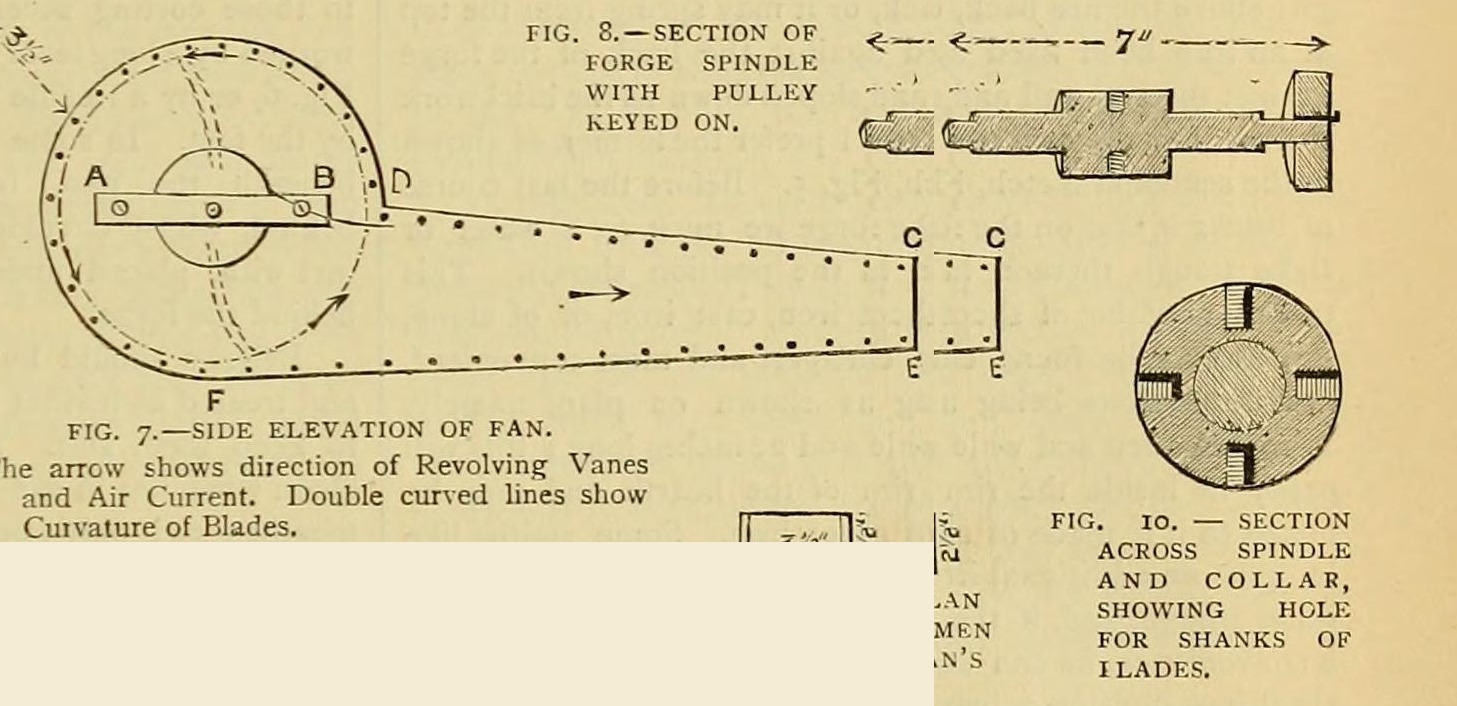

Forge Blast Fan: Riveted Sheet-Iron Drum, Shrunk-Collar Spindle and Four Screwed Blades, Belt-Driven at 360 rpm (Edwinson, 1886)
George Edwinson's home-made forge fan (Amateur Work, 1886), which he preferred to bellows: two 1/8 in. sheet-iron sides with a 3 1/2 in. intake, a riveted 1/16 in. casing, a turned 3/4 in. spindle with a shrunk-on collar holding four forged, slightly scooped blades, brass bearings, and a 2 in. pulley driven from a 2 ft hand wheel at 30 rpm for 360 rpm.
កម្រិតខ្ពស់
Three to four days
ការណែនាំ
1
1
His sizes
His sizes
កំពុងផ្ទុកសៀវភៅ Jupyter…
2
2
Read Edwinson
Read Edwinson
"Under no circumstances should I advise an amateur to make his own bellows, but he may be able to make a fan."
3
3
Cut the sides
Cut the sides
Cut two sides from 1/8 in. sheet iron to his fig. 7: 9 in. across at the widest, 2 1/2 in. at the narrowest, 2 ft long. Cut a 3 1/2 in. hole in each for the spindle and air intake, drill two 3/8 in. holes for bolts A and B (filed square), and drill the rivet holes round the edge.
សម្ភារៈសម្រាប់ជំហាននេះ៖
 សន្លឹកដែកថែបទន់1 ដុំ
ឧបករណ៍ដែលត្រូវការ៖
 កន្ត្រៃកាត់សន្លឹកលោហៈ
 ម៉ាស៊ីនចោះឈរ
 ដែកឆាប (ដែកឆាបដៃ)
 ដែកគូសចំណុចកណ្តាល
4
4
Rivet the casing
Rivet the casing
Cut 5 in. strips of 1/16 in. sheet with 3/4 in. margins bent down (4 in. clear): 14 in. from C to D, 20 in. from E to F, and about 22 in. round the drum from D to F (measure it). Mark the rivet holes through the side holes, nick between holes so the drum strip bends without buckling, and rivet, backing each head with stout iron. Leave a foot of the drum strip open. (Easier: make the sides 2 in. larger with outward flanges and rivet the strips to them.)
សម្ភារៈសម្រាប់ជំហាននេះ៖
សន្លឹកដែកថែបទន់1 ដុំ ដែកគោលដែក1 ដុំ
ឧបករណ៍ដែលត្រូវការ៖
កន្ត្រៃកាត់សន្លឹកលោហៈម៉ាស៊ីនចោះឈរ ឈុតគោលរីវេត
 ញញួរ
 ខ្សែវាស់
5
5
Turn the spindle
Turn the spindle
Turn 7 in. of 3/4 in. round iron smooth. Turn one end to 1/2 in. for 5/8 in. and the other to 1/2 in. for 2 1/8 in., with sharp shoulders. Bore a 2 x 2 in. collar a shade under size, heat it red and slip it on 1 in. in from a shoulder, then cool it in water to shrink it tight.
សម្ភារៈសម្រាប់ជំហាននេះ៖
 ដំបងដែកវាយ1 ដុំ
 ទឹក1 ដុំ
ឧបករណ៍ដែលត្រូវការ៖
 ម៉ាស៊ីនកាត់ដែក (ទ័រ)
 ឡជាងដែក
 ដង្កៀបជាងដែក
6
6
Drill the collar
Drill the collar
Drill four 5/16 in. holes 5/8 in. deep at quarters round the middle of the collar and tap them 3/8 in. (fig. 10).
ឧបករណ៍ដែលត្រូវការ៖
ម៉ាស៊ីនចោះឈរ ដែកស្វានវីសដៃ (tap)
 ដងបង្វិលដែកកាត់ខ្សែវីសខាងក្នុង
7
7
Forge the blades
Forge the blades
Forge four blades (fig. 9) from 5/8 or 3/4 in. round iron, upsetting and flattening the ends to 1/16 in. thick (or weld 1/4 in. plate to 5/8 in. arms and thin it). Thread the arm ends to fit the collar, curve the blades slightly into a scoop, and bend the arms a little off concentric for a steadier blast.
សម្ភារៈសម្រាប់ជំហាននេះ៖
ដំបងដែកវាយ1 ដុំឧបករណ៍ដែលត្រូវការ៖
ឡជាងដែក ទាំងជល់ (កំណាត់ដែក)ញញួរដែកស្វានវីសដៃ (tap)
8
8
Bearings and assembly
Bearings and assembly
Bolt a 1/2 in. brass bar at least 1 1/4 in. wide across each intake hole (A-B) and bore it true for the spindle. Fit one bearing, pass the spindle in, fit the other and bolt up. Screw the blades in through the open part of the drum, each slightly askew, check they turn without touching, and close the drum with thin-headed bolts, nuts outside.
សម្ភារៈសម្រាប់ជំហាននេះ៖
 ដុំស្ពាន់លឿង1 ដុំ
 ការប្រមូលផ្ដុំប៊ូឡុងប្រាំមួយជ្រុង1 ដុំ
ឧបករណ៍ដែលត្រូវការ៖
ម៉ាស៊ីនចោះឈរម៉ាស៊ីនកាត់ដែក (ទ័រ)ដែកឆាប (ដែកឆាបដៃ)9
9
Drive it
Drive it
File a flat on the 1 1/2 in. of spindle that stands out on the pulley side and key a 2 in. pulley with a 1 1/2 in. face to it. Belt it from a 2 ft wheel turned at 30 rpm: the fan runs at 360 rpm. Put the crank by the forge head, worked by hand or a foot lever (ours: details left to the reader in the source), and pipe the 3 1/2 x 2 1/2 in. mouth to the tuyere.
សម្ភារៈសម្រាប់ជំហាននេះ៖
 រ៉ក1 ដុំ
 ខ្សែក្រវាត់បញ្ជូនចលនា1 ដុំ
ឧបករណ៍ដែលត្រូវការ៖
ដែកឆាប (ដែកឆាបដៃ)ញញួរ10
10
Troubleshooting
Troubleshooting
Fan troubleshooting.
Flow
Loading...
11
11
History and honest limits
History and honest limits
From George Edwinson, "Smithing and Forging" I, **Amateur Work, Illustrated**, vol. V (1886), pp. 162-164 and figs. 7-11 (checked on the archive.org scan amateurworkillus05lond). He leaves the crank, wheel frame and pipe to the reader; the metric figures and tools are ours.
សម្ភារៈ
8- 1 ដុំកន្លែងទុក
- 1 ដុំកន្លែងទុក
- 1 ដុំកន្លែងទុក
- 1 ដុំកន្លែងទុក
- 1 ដុំកន្លែងទុក
- កន្លែងទុក
- 1 ដុំកន្លែងទុក
- កន្លែងទុក
ឧបករណ៍ចាំបាច់
13- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- 1 vendor sell this, none ship to you yetកន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
- កន្លែងទុក
ប្លង់នេះធ្វើ

ប្លង់ពាក់ព័ន្ធ
ប្លង់ទាំងនេះចែករំលែកចំណេះដឹង — បច្ចេកទេស សម្ភារៈ ឬគោលការណ៍
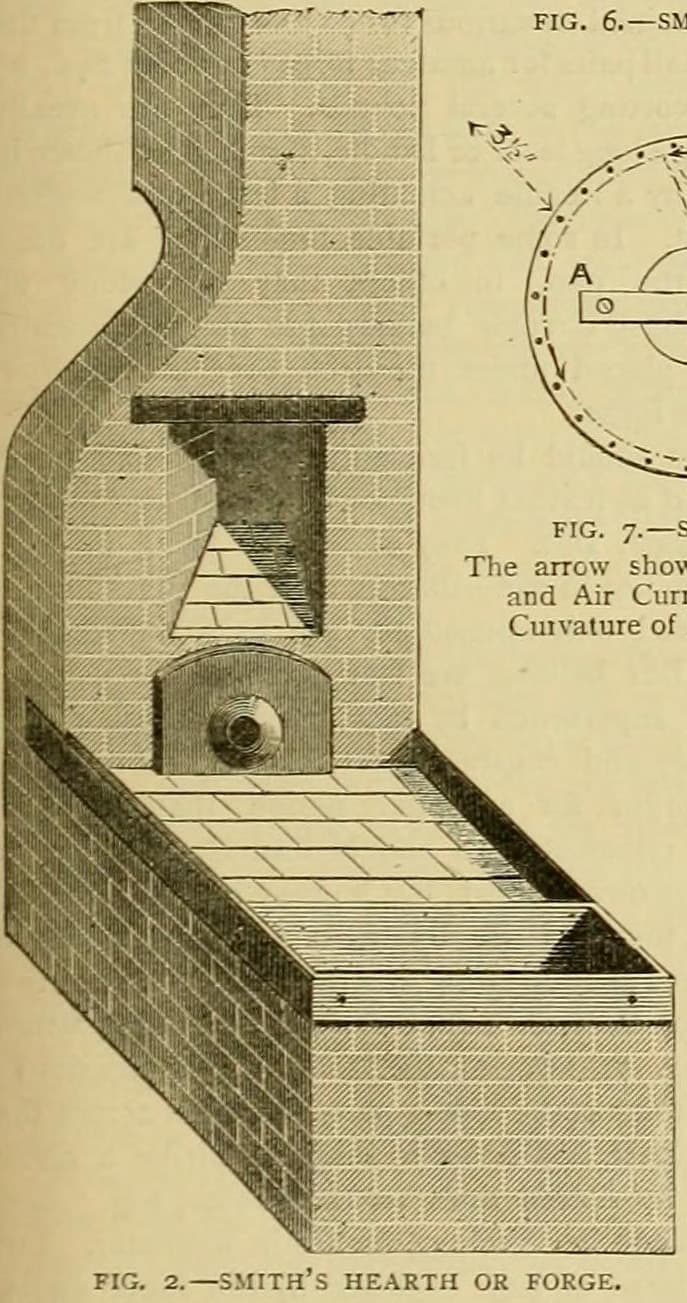
Brick Smith's Hearth: Stone Base, Firebrick Top in an Iron Rim, a Cannon-Shot Tuyere and a Slake Trough (Edwinson, 1886)
ដោយ Forge
ការធ្វើការលោហៈ
8
0
0
0
0
0
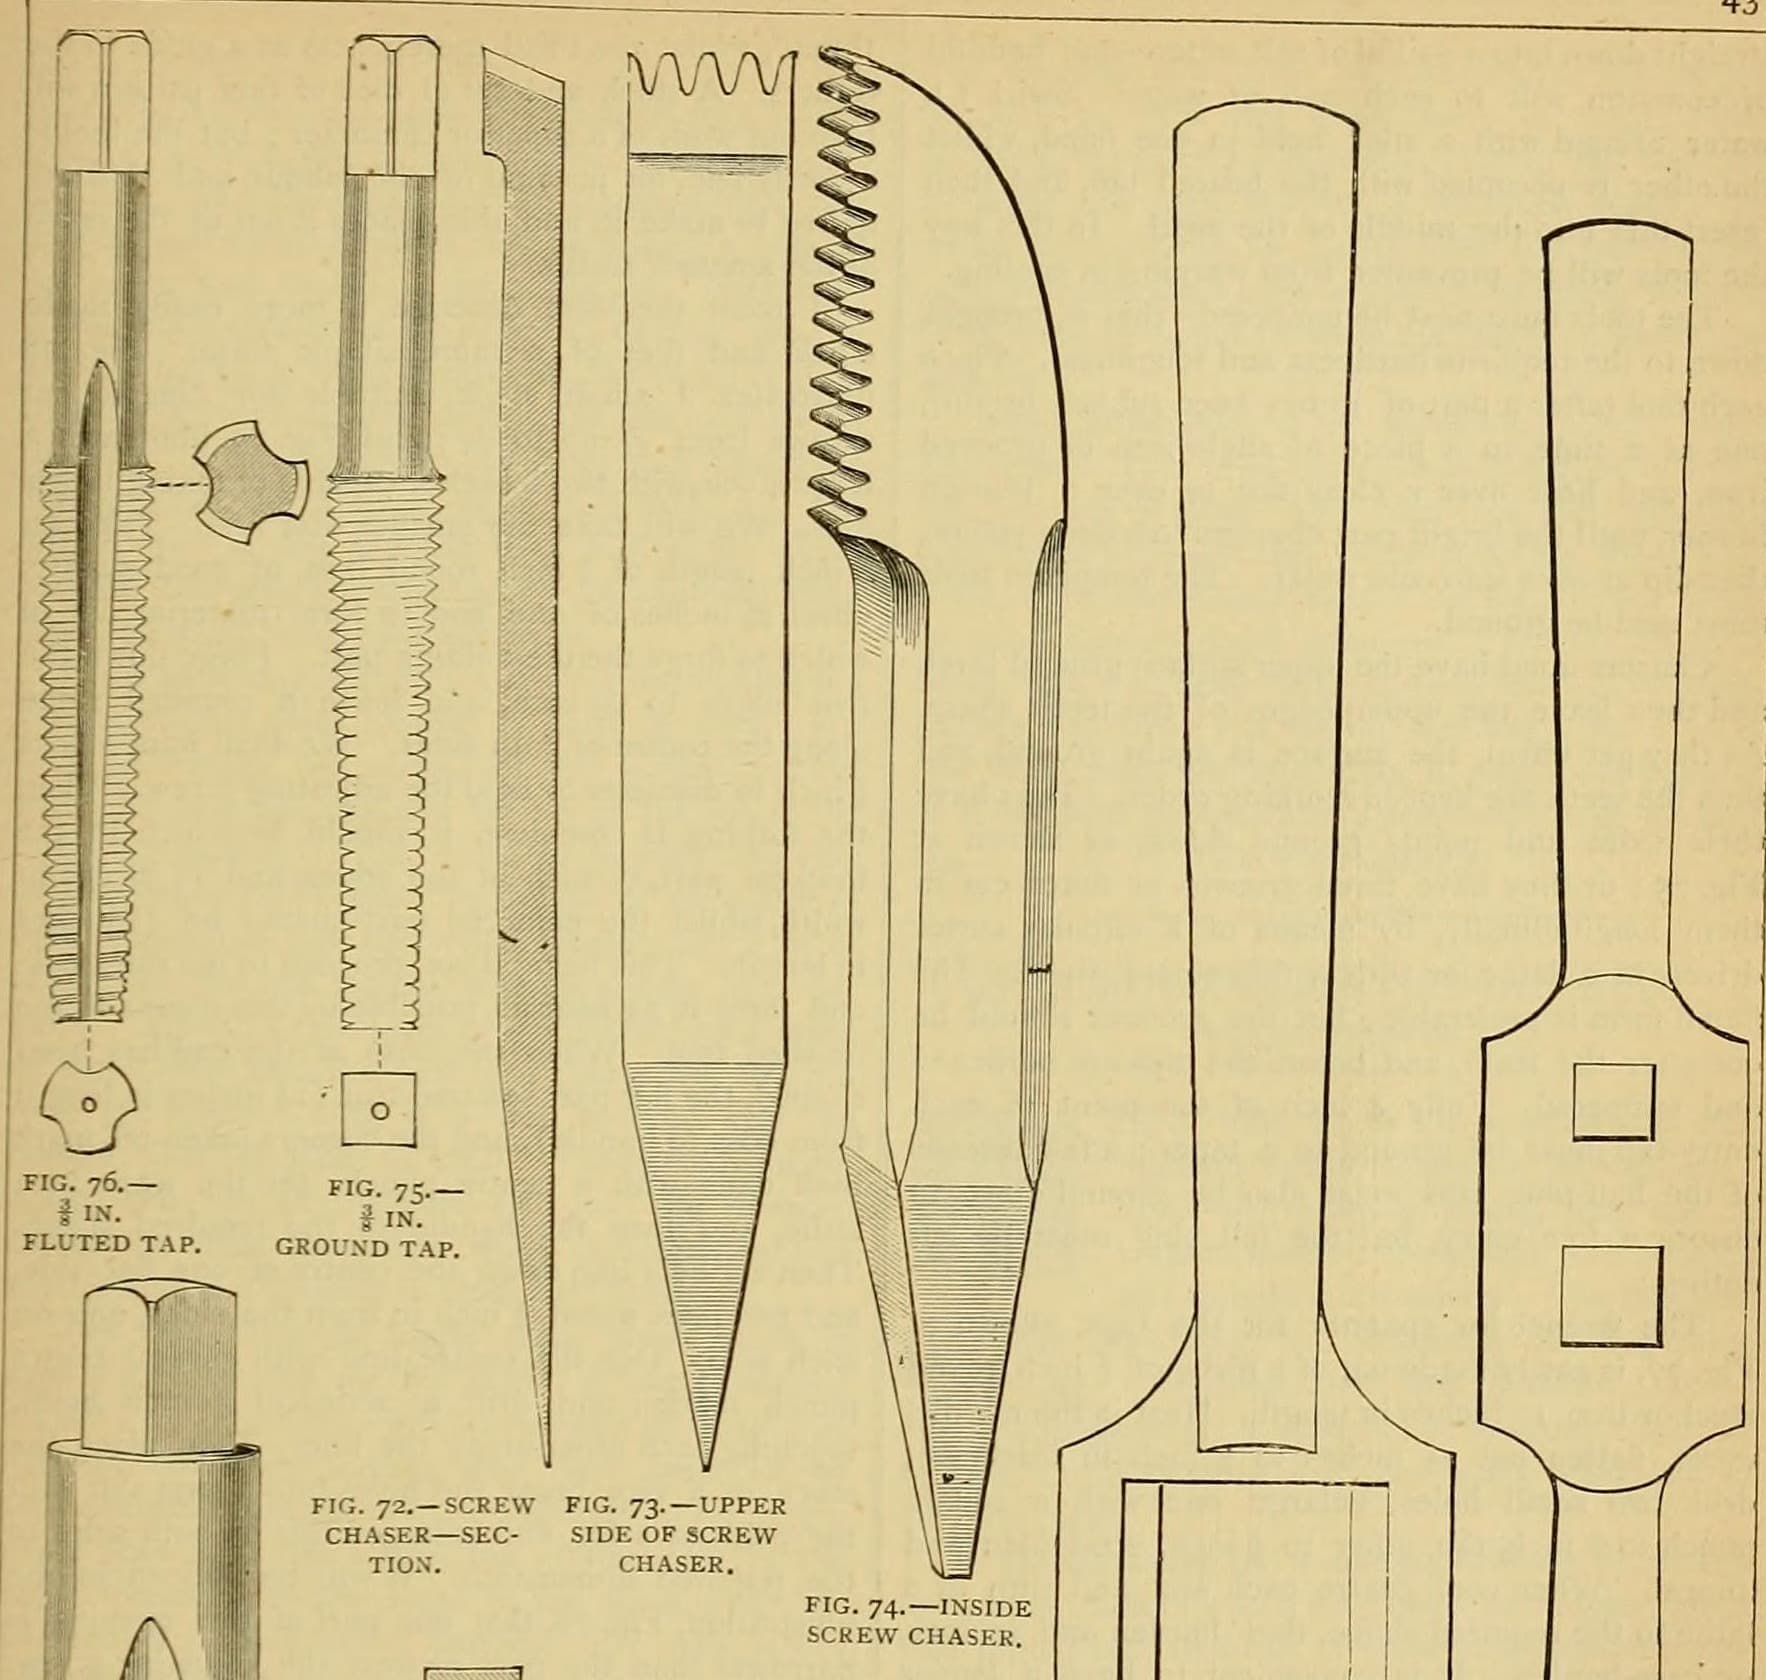
Whitworth Taps from Cast Tool Steel: Turned, Chased, Fluted and Hardened in Salt Water, with Their Wrench (Edwinson, 1886)
ដោយ Forge
ការធ្វើការលោហៈ
11
0
0
0
0
0
CC0 សាធារណៈ
ប្លង់នេះត្រូវបានចេញផ្សាយក្រោម CC0។ អ្នកមានសិទ្ធិចម្លង កែប្រែ ចែកចាយ និងប្រើប្រាស់ដោយមិនចាំបាច់សុំអនុញ្ញាត។
គាំទ្រអ្នកបង្កើតដោយទិញផលិតផលតាមរយៈប្លង់របស់ពួកគេ ដែលពួកគេទទួលបាន កម្រៃជើងសារអ្នកបង្កើត កំណត់ដោយអ្នកលក់ ឬបង្កើតកំណែថ្មីនៃប្លង់នេះ ហើយបញ្ចូលជាការតភ្ជាប់ក្នុងប្លង់របស់អ្នកដើម្បីចែករំលែកចំណូល។