IṢẸ́ ỌNÀ
ẸWÀ ÀTI ÌLERA
IṢẸ́ ỌWỌ́
ÀṢÀ ÀTI ÌTÀN
ÌṢERÉ
ÀYÍKÁ
OÚNJẸ ÀTI OHUN MÍMU
REVERSE ENGINEERING
SÁYẸ́ǸSÌ
ERÉ ÌDÁRAYÁ
ÌMỌ̀-Ẹ̀RỌ
ÀWỌN OHUN WÍWỌ̀
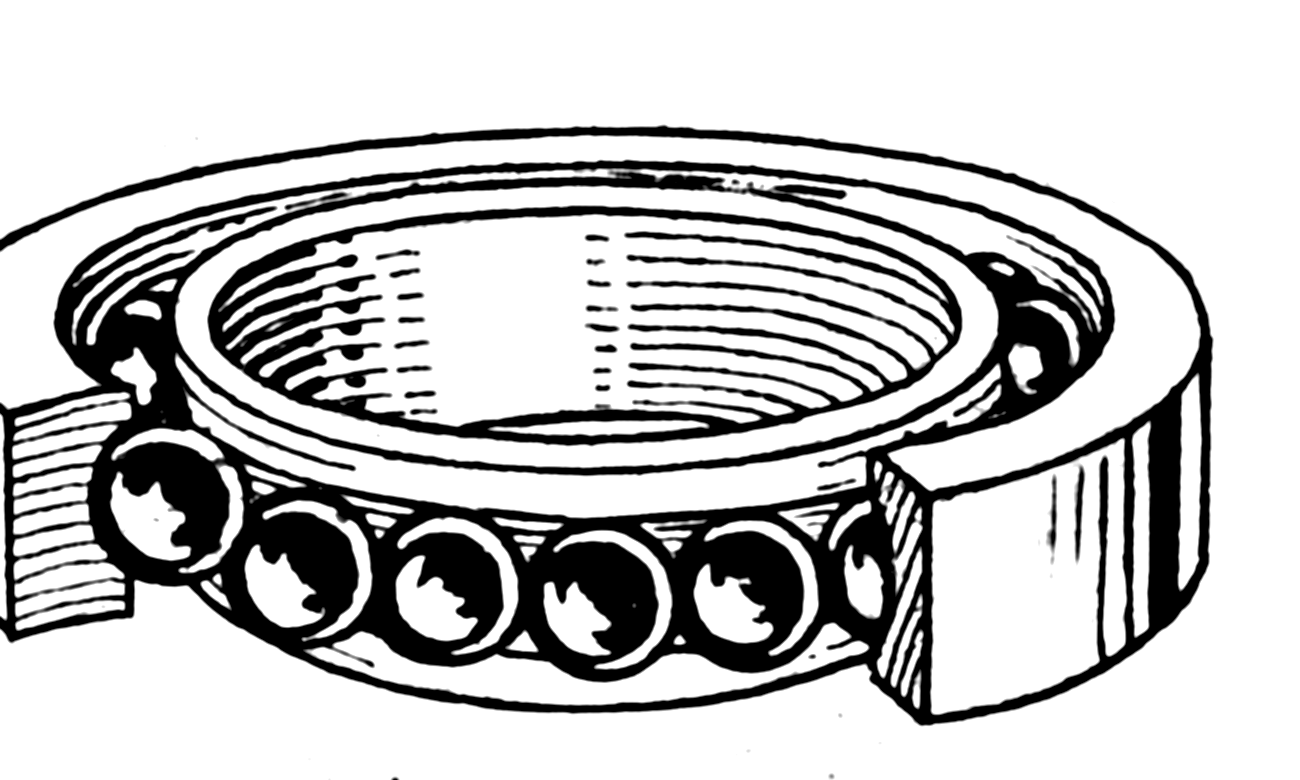

Ball Bearings: Races, Balls and Cage
A ball bearing has four parts: an outer race, an inner race, the balls that roll between them, and a cage that keeps the balls evenly spaced. Almost all of it is steel, usually 52100 (1% chromium, 1% carbon), which can be made very hard and tough by heat treating; 440C stainless is used where rust is a problem. The races are turned from tubing, the balls are cold headed from thick wire, both are hardened, tempered, ground and lapped to an almost mirror finish, and the cage is stamped from thin sheet. Even an inexpensive bearing's balls may be out of round by no more than 25 millionths of an inch; precision bearings allow five millionths.
Ilọsíwájú
Factory process
Ìlànà
1
1
Turn the races
Turn the races
Cut the basic shape of both races from steel tubing on automatic lathe-like machines, leaving every dimension slightly oversize: the steel usually warps in heat treatment.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Páìpù irin bearing (52100)1 as required
Àwọn irinṣẹ́ tí a nílò:
 Ẹ̀rọ ìyí aládàáṣe
2
2
Harden and temper the races
Harden and temper the races
Heat to about 843 °C (1,550 °F) for up to several hours depending on size, then quench in oil: hard but brittle. Temper at about 149 °C (300 °F) and let cool in air: hard and tough.
Àwọn irinṣẹ́ tí a nílò:
 Ìléru ìmúle ìtẹ̀síwájú pẹ̀lú ìtutù epo
 Ààrò àtúnṣe líle
3
3
Grind and lap the races
Grind and lap the races
The hardened steel is too hard to cut, so grind almost every surface: the fitting surfaces round, the sides flat. Grind the ball track, then lap it for several hours with a very fine abrasive slurry to an almost mirror finish.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Àpòpọ̀ ìdán1 as required
Àwọn irinṣẹ́ tí a nílò:
 Ẹ̀rọ ìlọ òrùka bearing
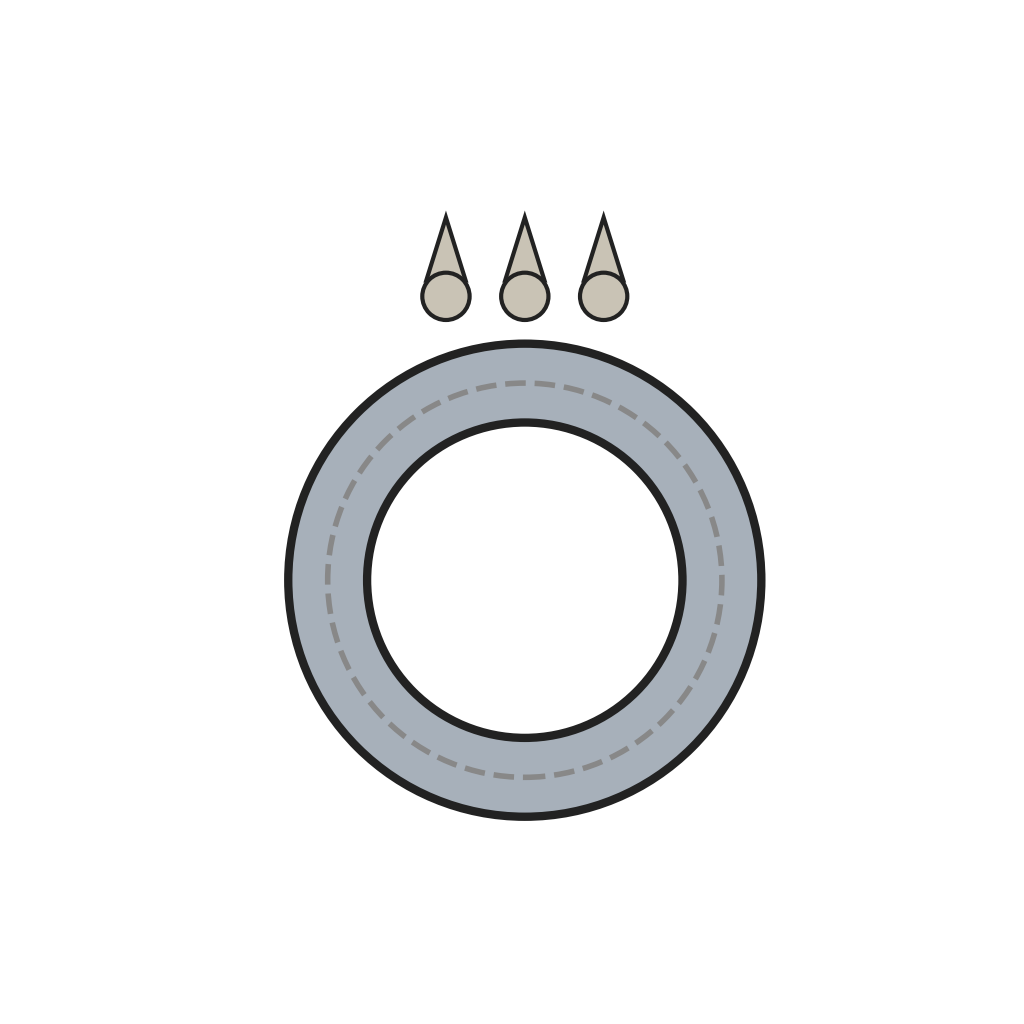 Ẹ̀rọ ìdán ọ̀nà bọ́ọ̀lù
4
4
Cold head the balls
Cold head the balls
Feed thick wire from a roll into a machine that cuts off a short piece and smashes both ends in toward the middle between two dies, without heating. The ball comes out with a ring of "flash" round its middle.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Wáyà irin bearing (52100)1 as required
Àwọn irinṣẹ́ tí a nílò:
 Ẹ̀rọ ìlù orí tútù
5
5
Remove the flash
Remove the flash
Run the balls many times round rough grooves between two cast-iron discs, one turning and one fixed, until the flash is gone and they are nearly round. Leave about 0.008 in (0.2 mm) for finishing.
Àwọn irinṣẹ́ tí a nílò:
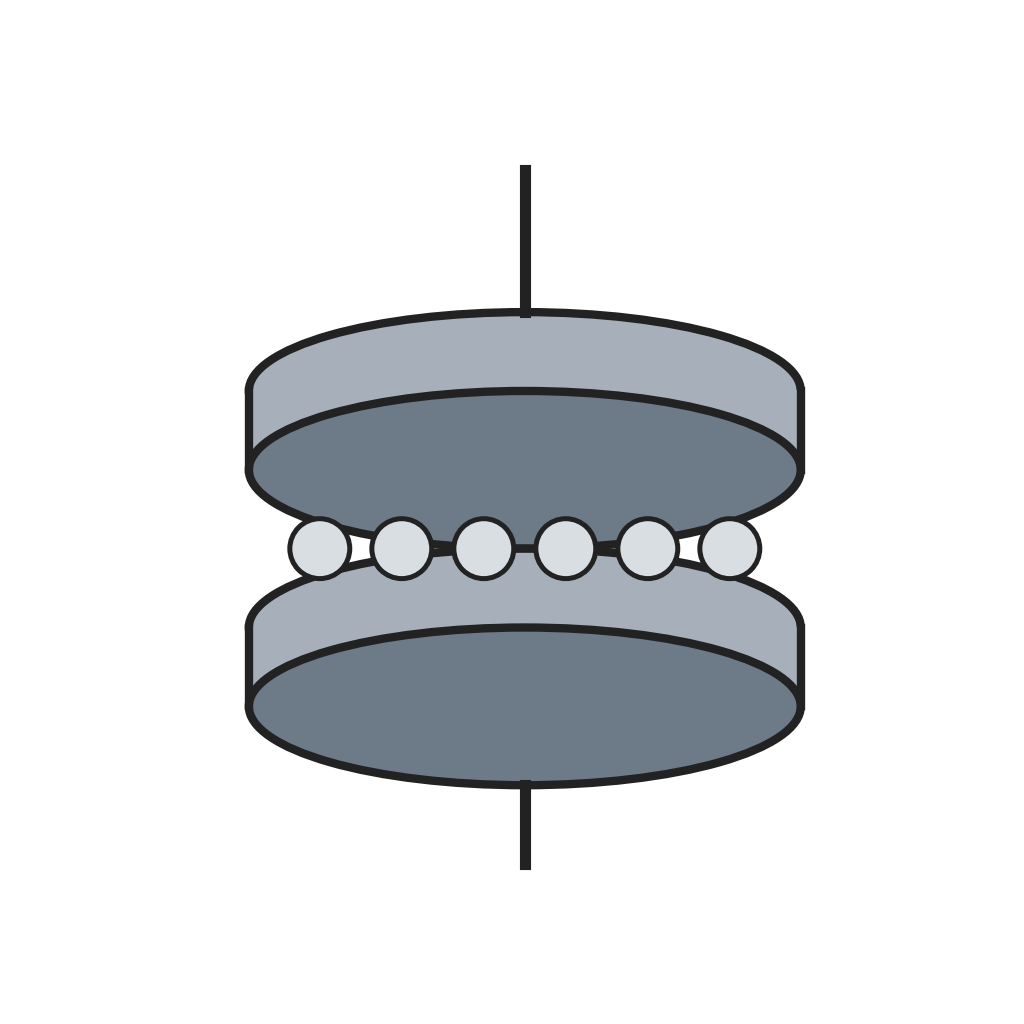 Ẹ̀rọ ìyọ etí bọ́ọ̀lù
6
6
Harden, grind and lap the balls
Harden, grind and lap the balls
Heat treat and temper the balls like the races. Grind them in the same kind of disc machine with grinding wheels to within a few ten-thousandths of an inch, then lap them 8–10 hours on cast-iron wheels with lapping compound.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
Àpòpọ̀ ìdán1 as requiredÀwọn irinṣẹ́ tí a nílò:
Ìléru ìmúle ìtẹ̀síwájú pẹ̀lú ìtutù epoÀàrò àtúnṣe líle Ẹ̀rọ ìlọ bọ́ọ̀lù
 Ẹ̀rọ ìdán bọ́ọ̀lù
7
7
Stamp the cage
Stamp the cage
Stamp the cage halves from thin steel sheet and bend them to shape in a die. (Plastic cages are injection moulded instead.)
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Àwo irin1 as required
Àwọn irinṣẹ́ tí a nílò:
 Ẹ̀rọ ìtẹ̀ àwo irin
8
8
Assemble
Assemble
Put the inner race inside the outer race, pushed as far to one side as it goes, and drop the balls into the gap opposite. Centre the races and spread the balls evenly, fit the cage (steel cages riveted, plastic ones snapped in) and coat the bearing with rust preventive.
Àwọn ohun èlò fún ìgbésẹ̀ yìí:
 Ìṣó irin1 as required
 Olùdènà ìpẹtà1 as required
Àwọn ohun-èlò
6- 1 as requiredÀyè
- 2 as requiredÀyè
- 1 as requiredÀyè
- 1 as requiredÀyè
- 1 as requiredÀyè
- 1 as requiredÀyè
Ìtọ́nisọ́nà yìí ń ṣe
Blueprint tó jọra
Àwọn blueprint wọ̀nyí pín ìmọ̀ — ọ̀nà, ohun-èlò tàbí ìlànà
CC0 Àgbègbè Gbogbogbò
Blueprint yìí ti jáde lábẹ́ CC0. O lè ṣe àdàkọ, yí padà, pín, àti lò láìsí ìyọ̀ǹda.
Ṣàtìlẹ́yìn Olùṣẹ́dá nípa rírà àwọn ọjà nipasẹ̀ Blueprint wọn Ẹ̀san Olùṣẹ́dá tí àwọn Olùtajà gbé kalẹ̀, tàbí ṣẹ̀dá àtúnṣe tuntun ti Blueprint yìí kí o sì fi sínú Blueprint rẹ gẹ́gẹ́ bí ìsopọ̀ láti pín owó-wíwọlé.