IṢẸ́ ỌNÀ
ẸWÀ ÀTI ÌLERA
IṢẸ́ ỌWỌ́
ÀṢÀ ÀTI ÌTÀN
ÌṢERÉ
ÀYÍKÁ
OÚNJẸ ÀTI OHUN MÍMU
REVERSE ENGINEERING
SÁYẸ́ǸSÌ
ERÉ ÌDÁRAYÁ
ÌMỌ̀-Ẹ̀RỌ
ÀWỌN OHUN WÍWỌ̀
Iṣẹ́ Irin
Ìtọ́nisọ́nà 500 wà • Ẹ̀ka kékeré 8
Ṣàwárí Àwọn Ẹ̀ka Kékeré
Àwọn Ìtọ́nisọ́nà (500)
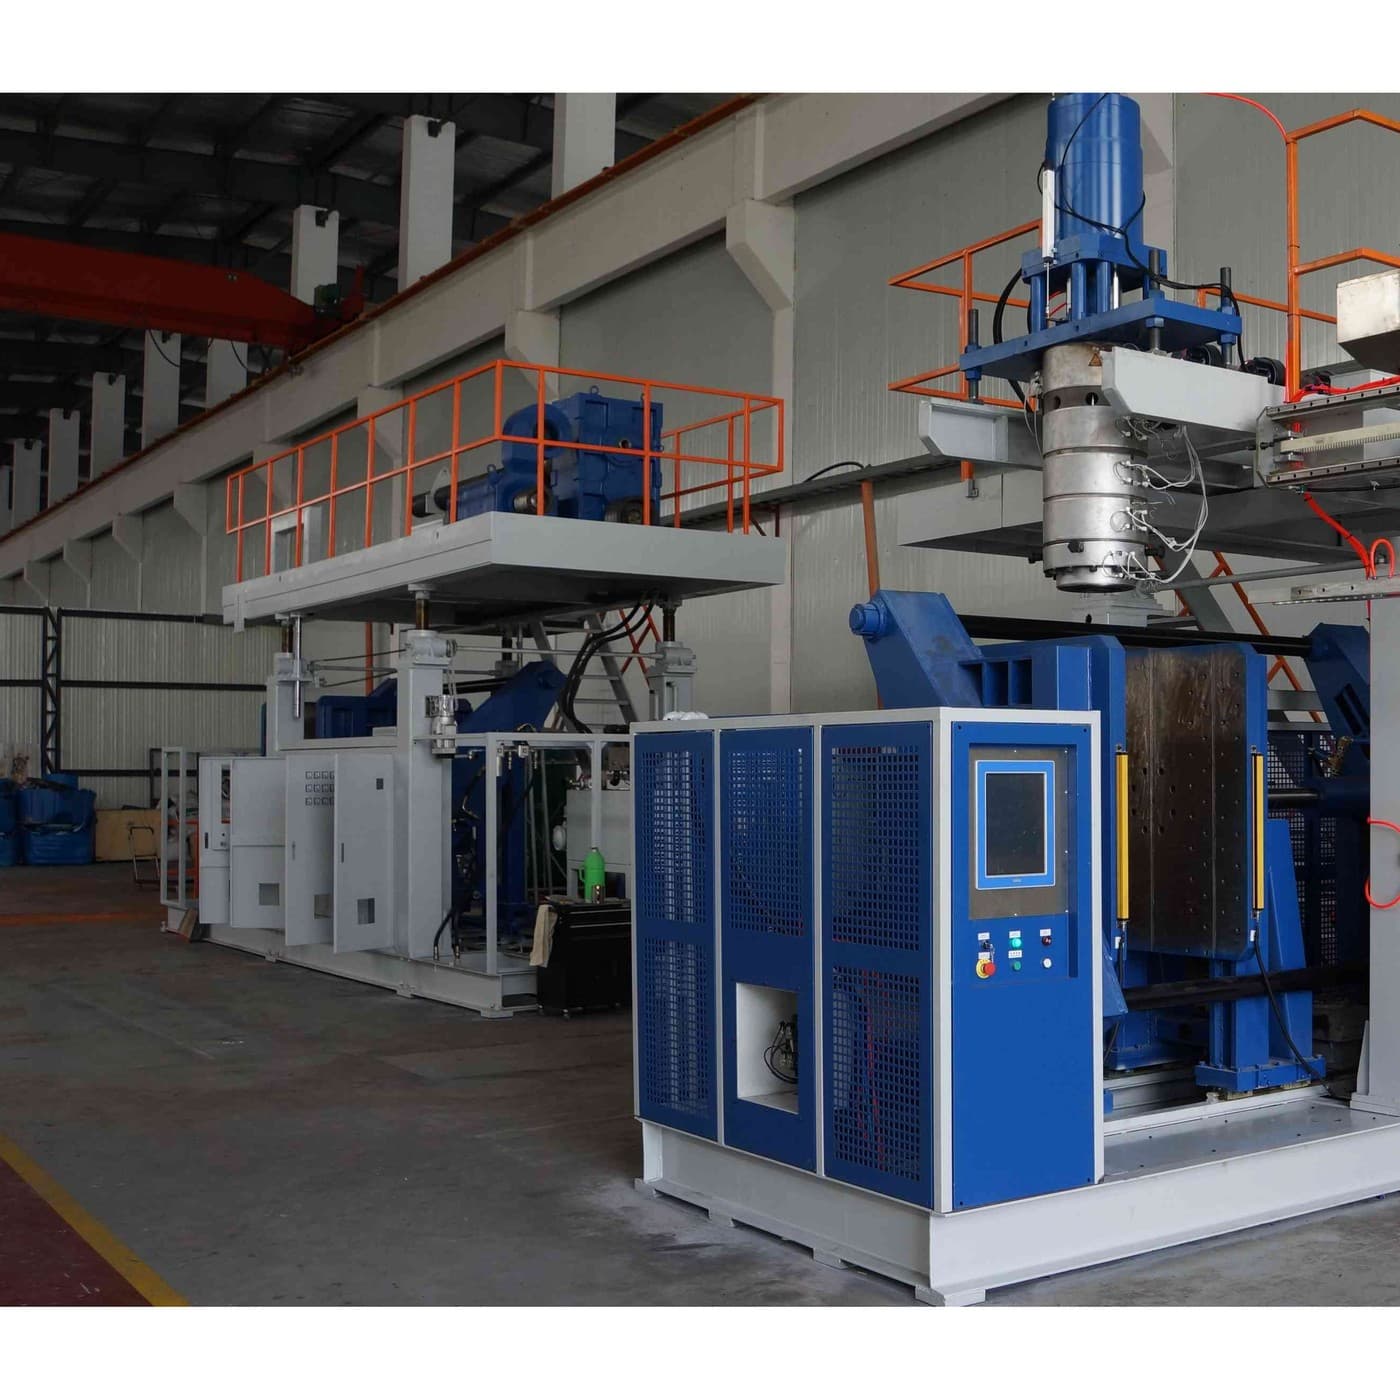
Blowing a Hollow Part: When There Is No Core
láti ọwọ́ Emma
Ìmọ̀-ẹ̀rọ
26
0
0
0
0
0
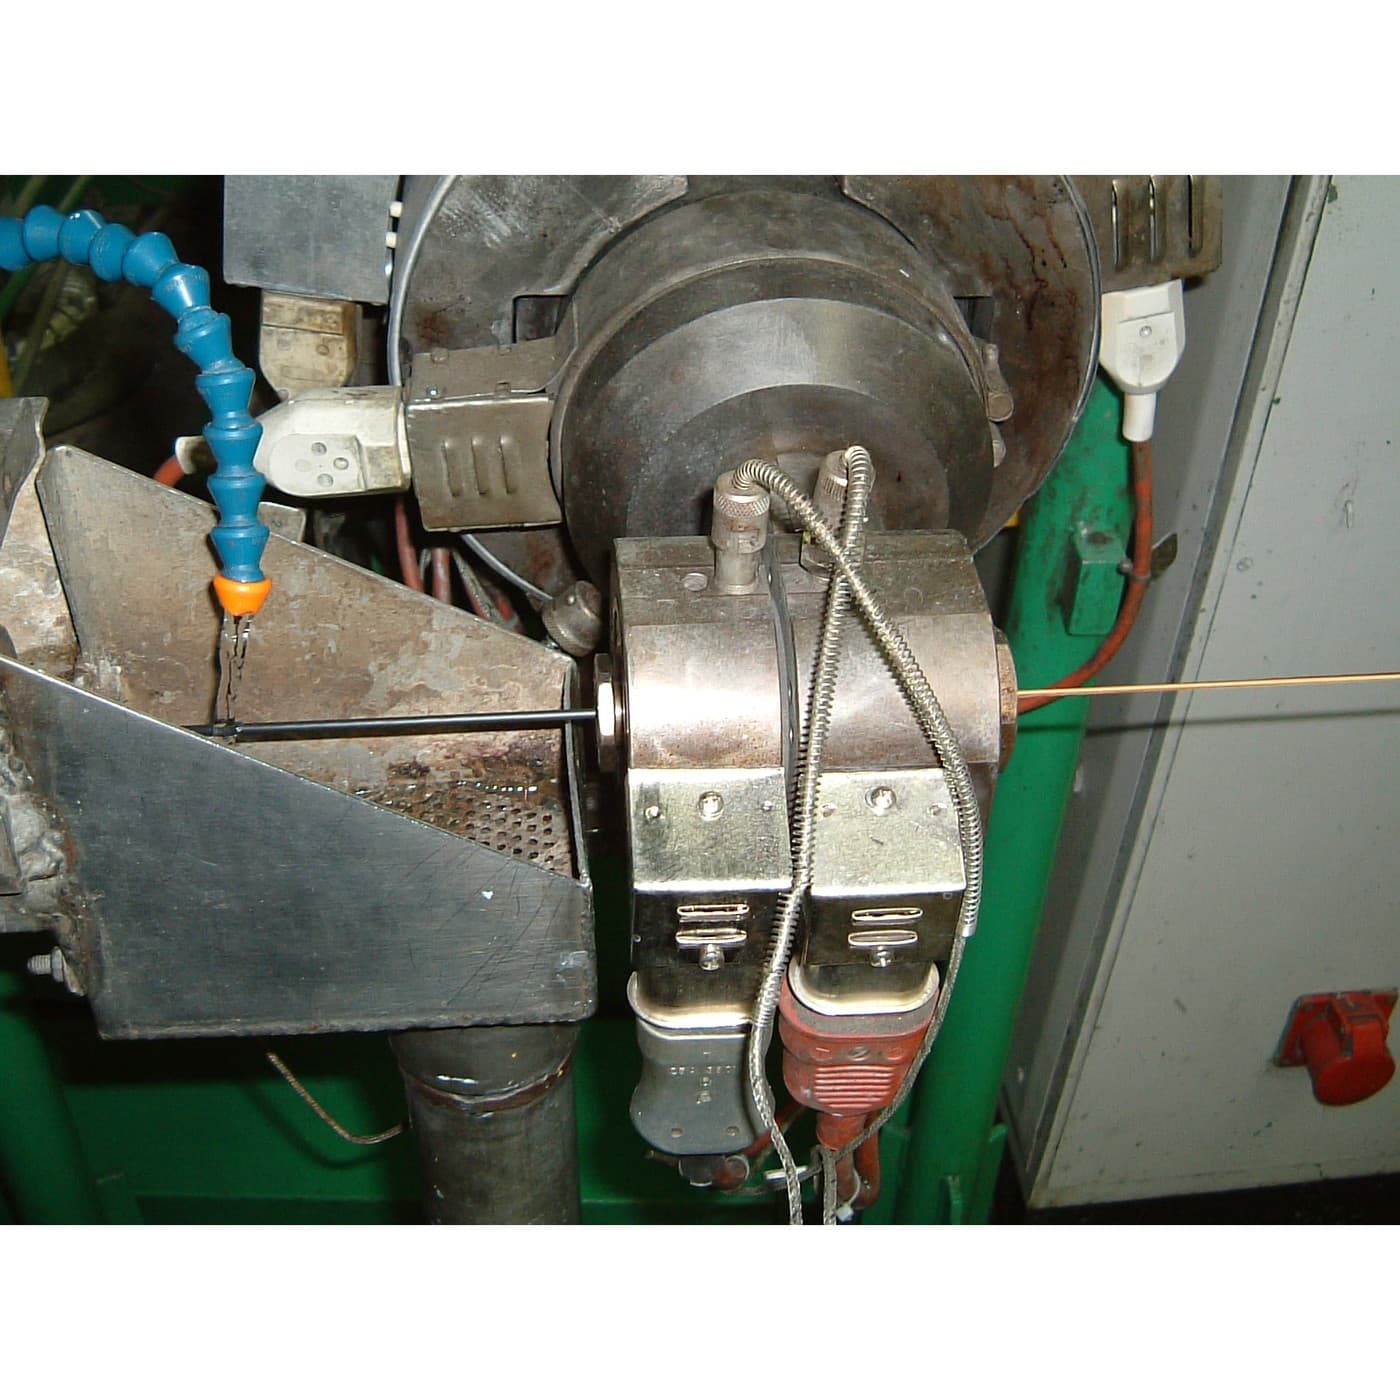
Extruding a Profile, and Blowing Film
láti ọwọ́ Emma
Ìmọ̀-ẹ̀rọ
33
0
0
0
0
0
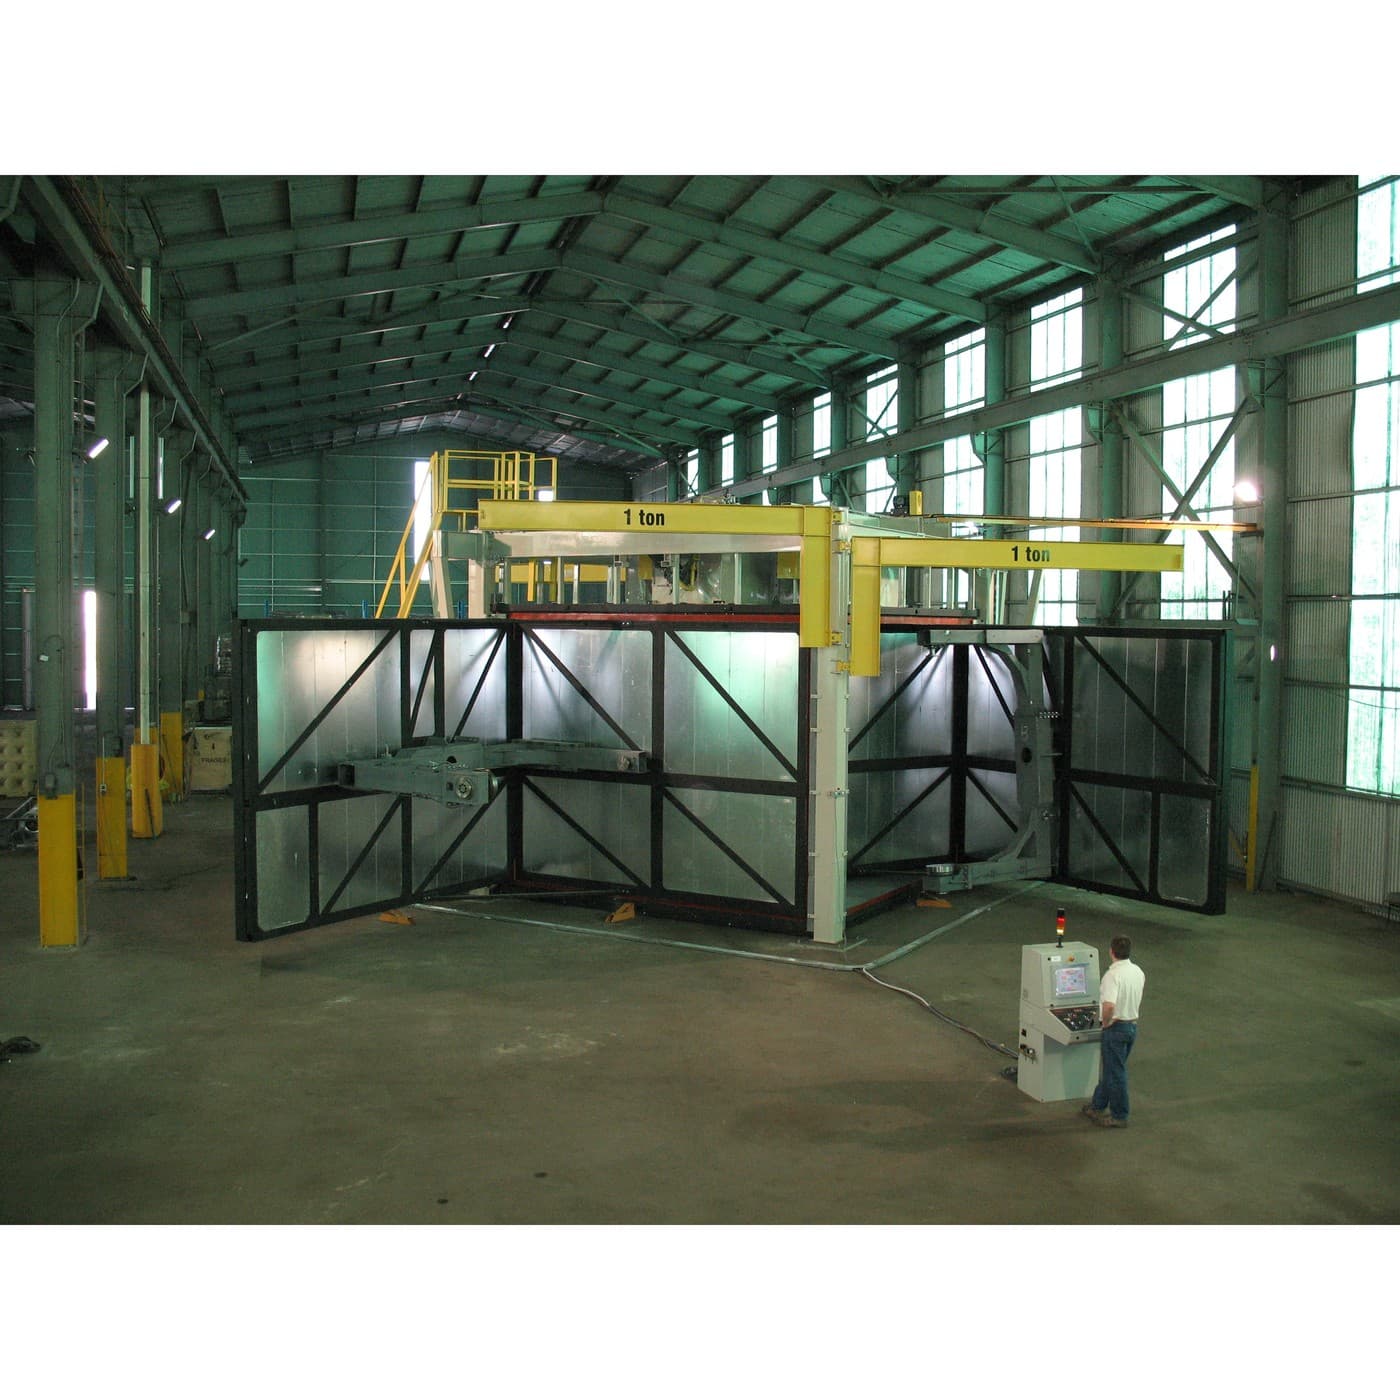
Rotational Moulding: No Pressure At All
láti ọwọ́ Emma
Ìmọ̀-ẹ̀rọ
25
0
0
0
0
0
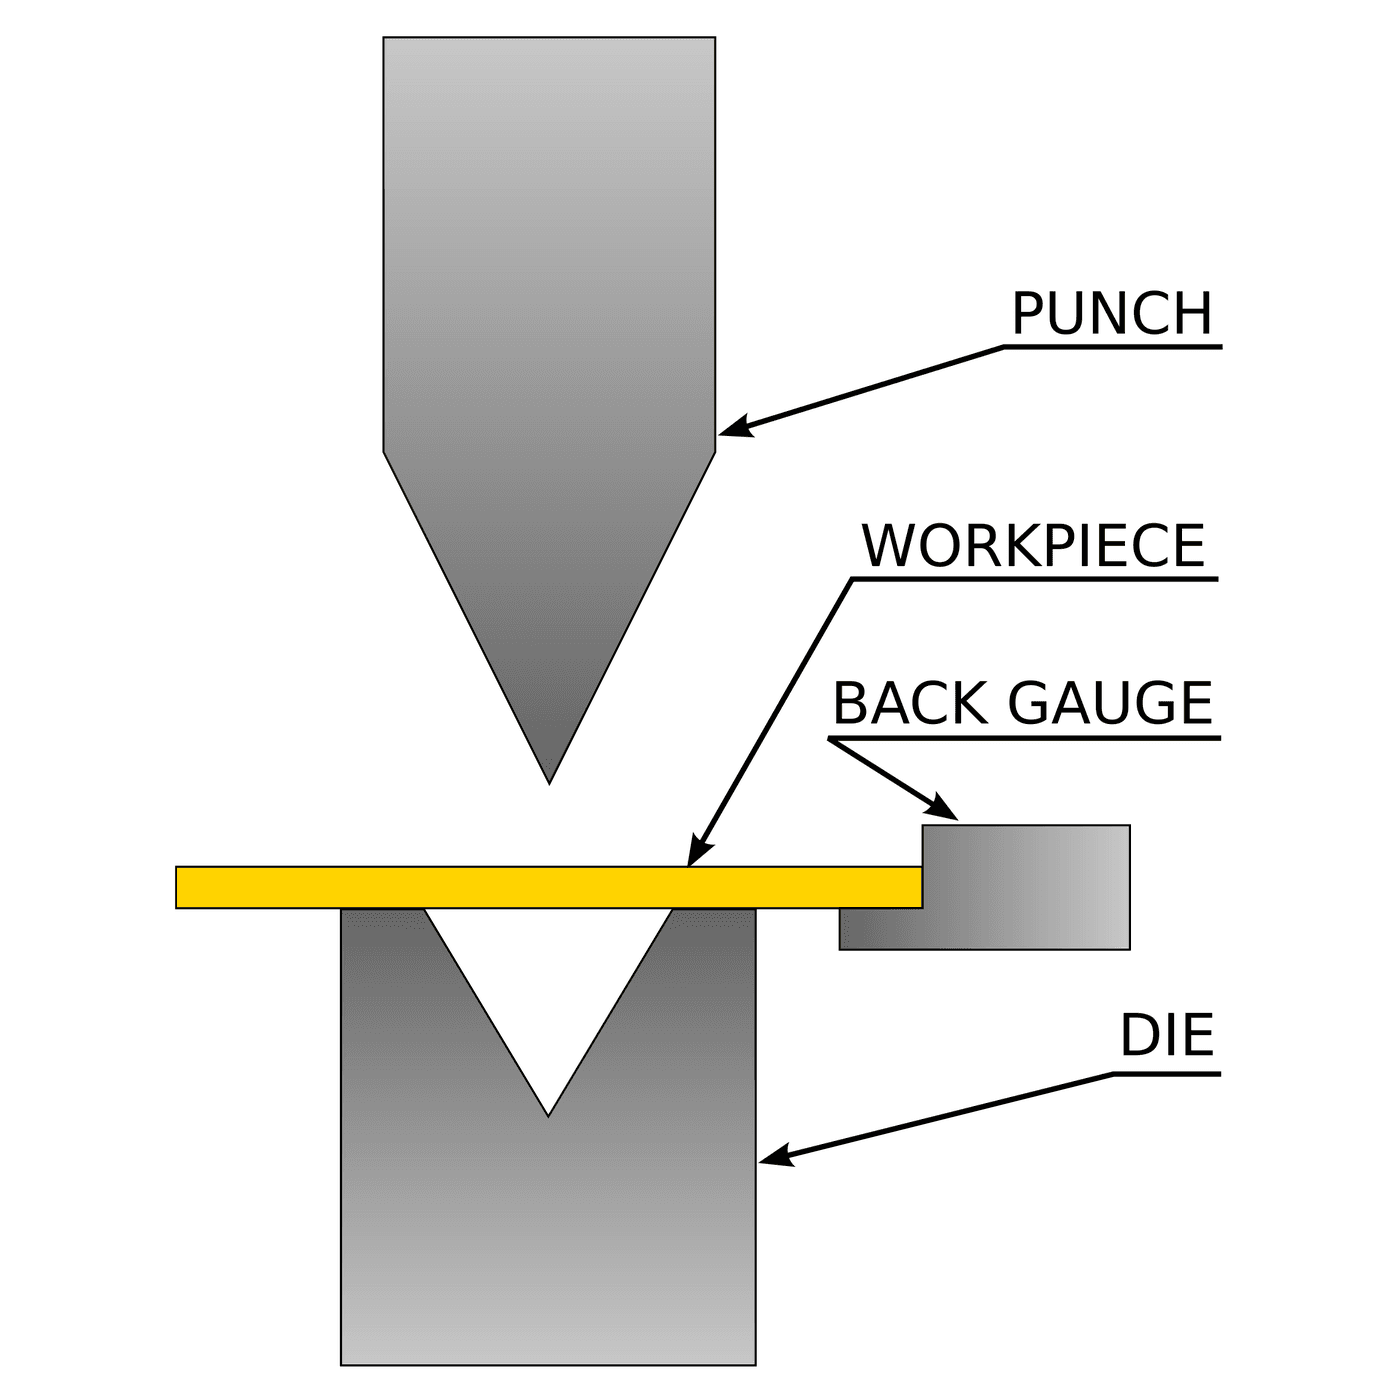
Bending: Where the Metal Goes, and How Much Comes Back
láti ọwọ́ Emma
Ìmọ̀-ẹ̀rọ
34
0
0
0
0
0
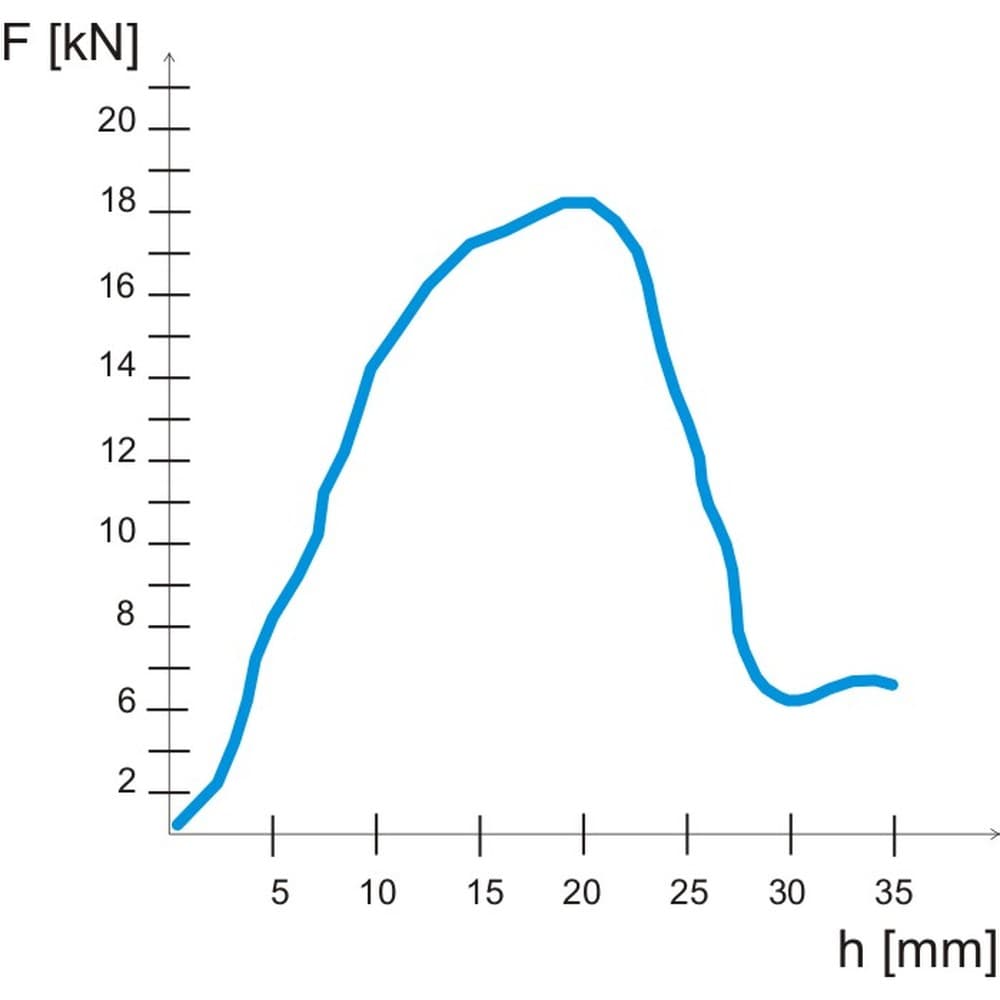
Reading a Sheet-Metal Fault
láti ọwọ́ Emma
Iṣẹ́ Irin
30
0
0
0
0
0
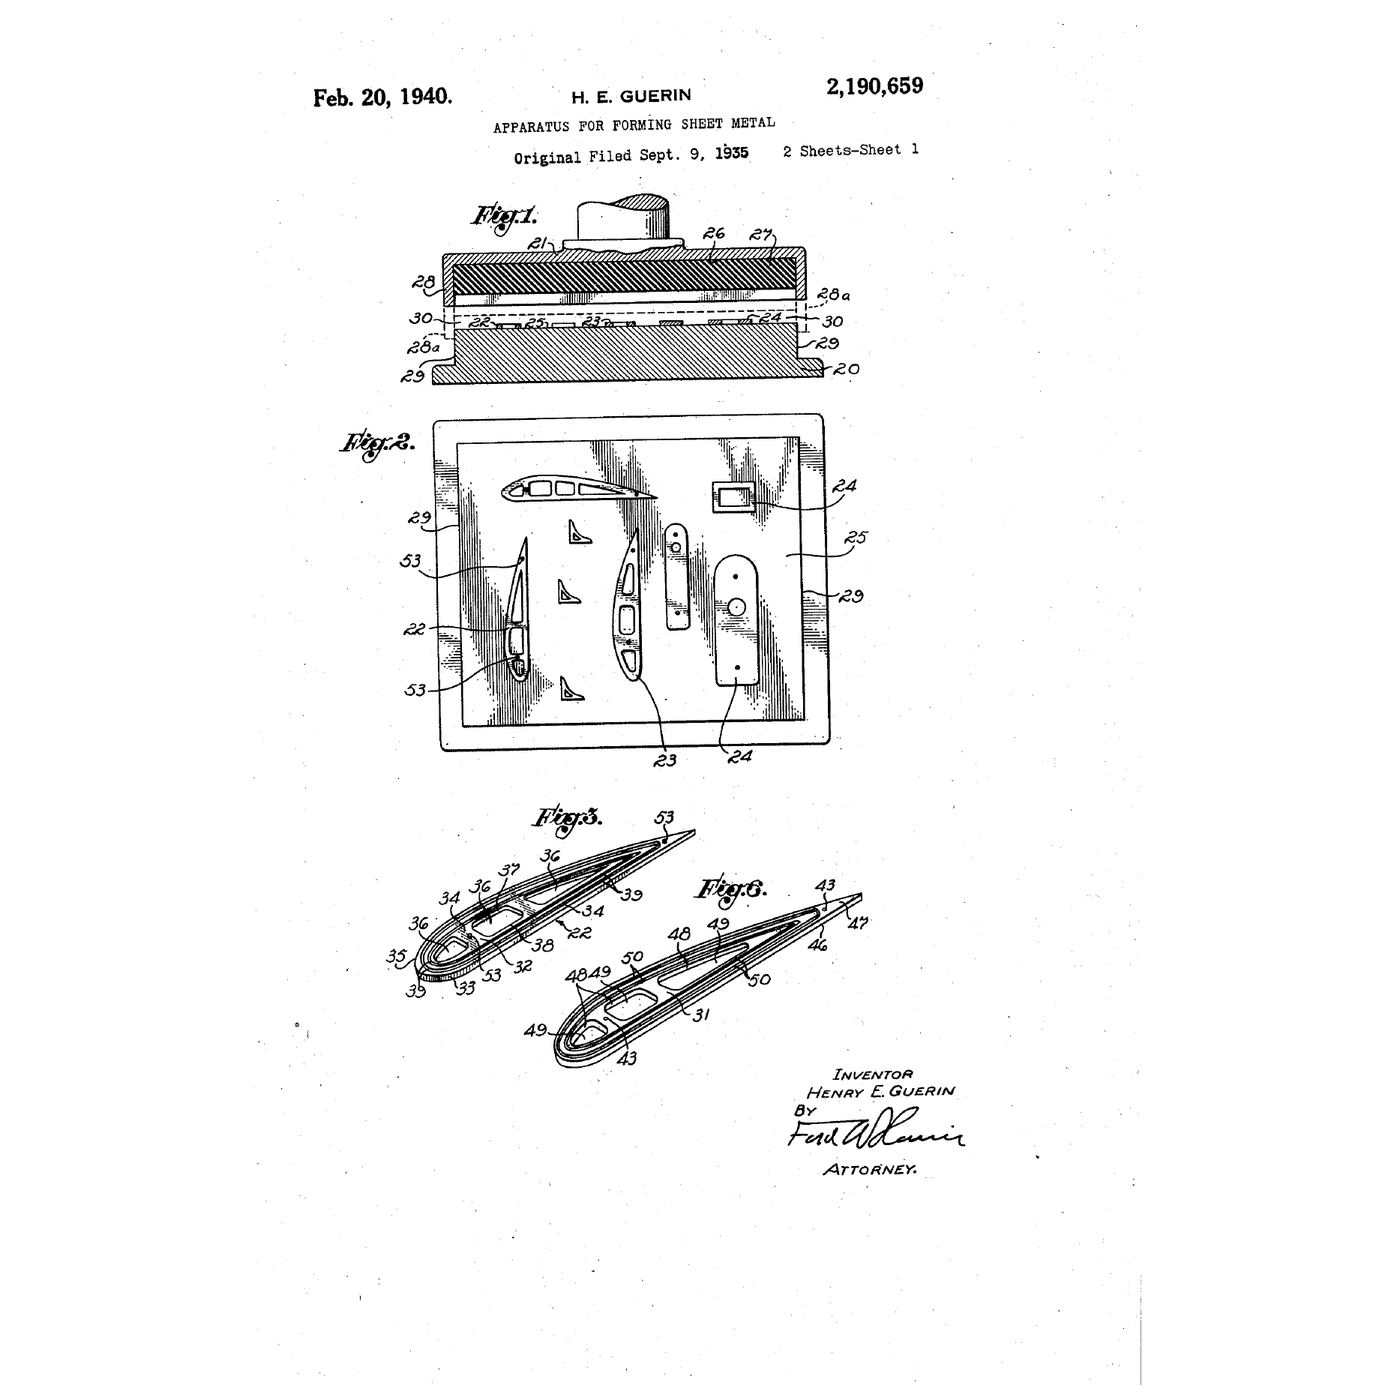
One Die Instead of Two: Forming Sheet Against Rubber
láti ọwọ́ Emma
Ìmọ̀-ẹ̀rọ
37
0
0
0
0
0
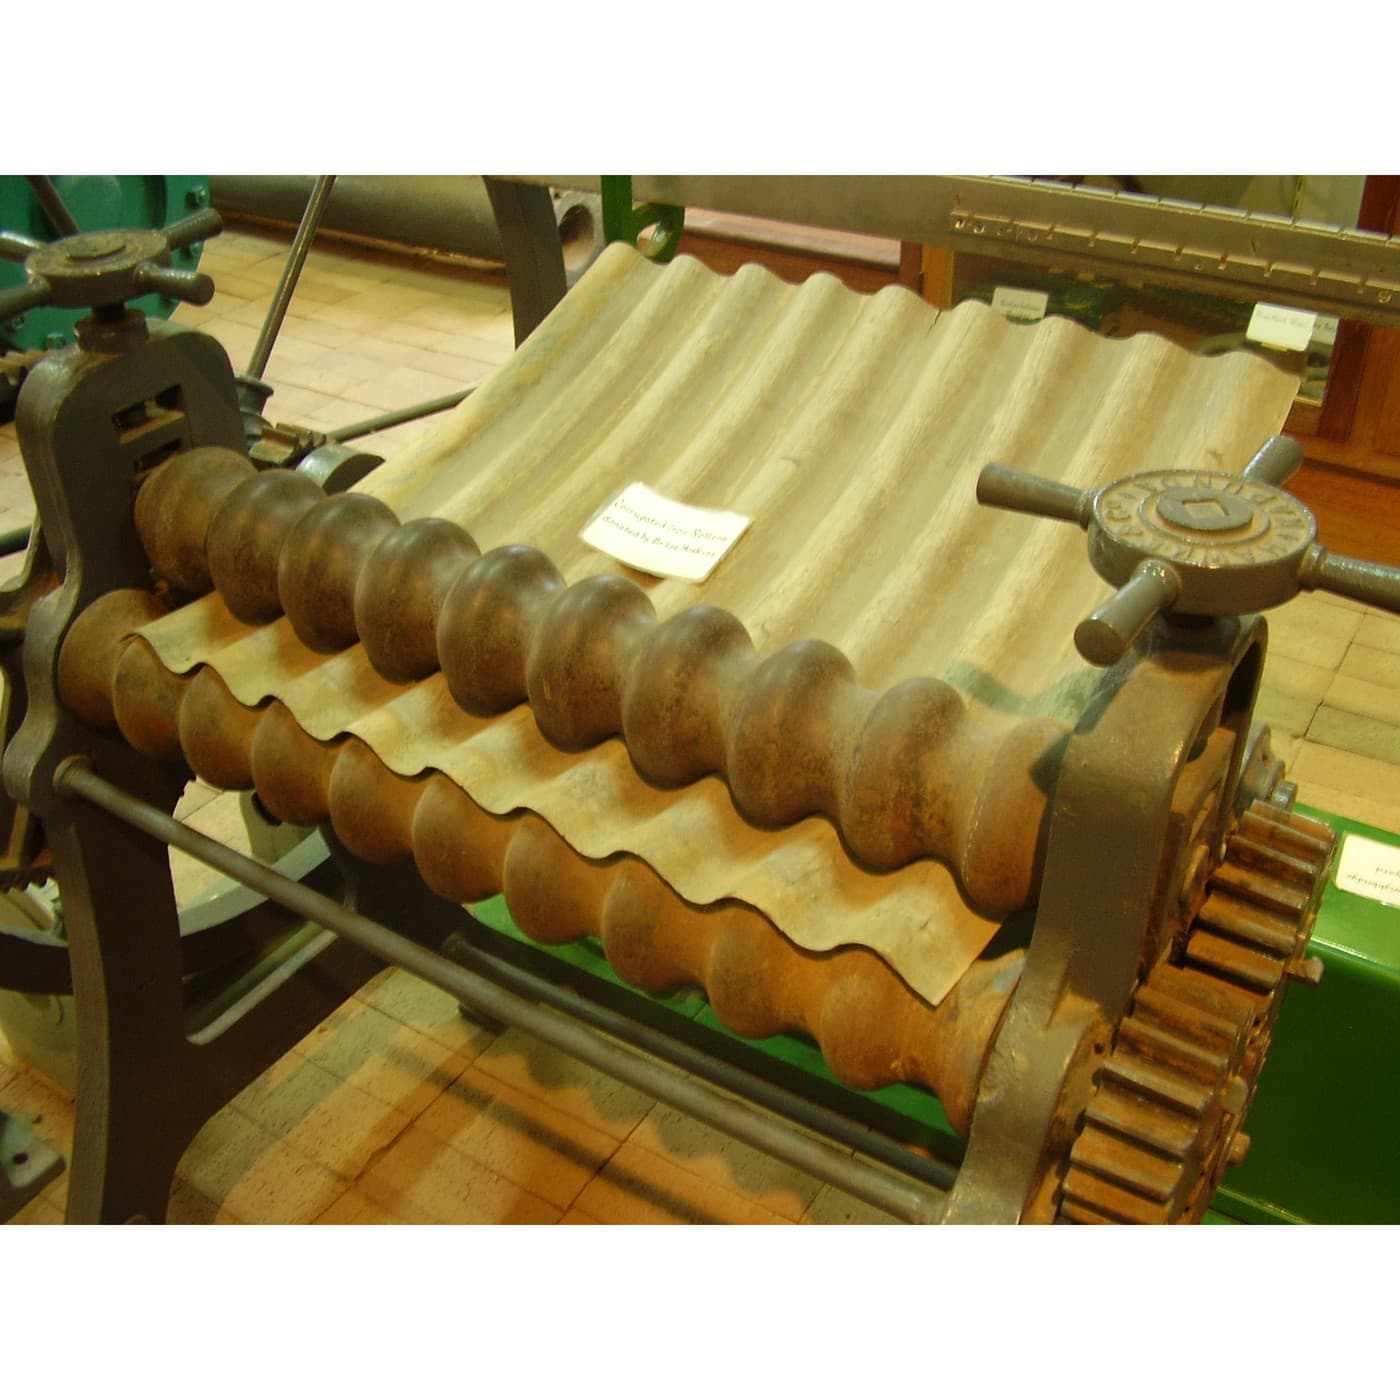
Stiffness Out of Shape: Corrugating, Beading and the Turned Edge
láti ọwọ́ Emma
Ìmọ̀-ẹ̀rọ
34
0
0
0
0
0

Blanking: The Punch, the Die, and the Gap Between Them
láti ọwọ́ Forge
Iṣẹ́ Irin
28
0
0
0
0
0
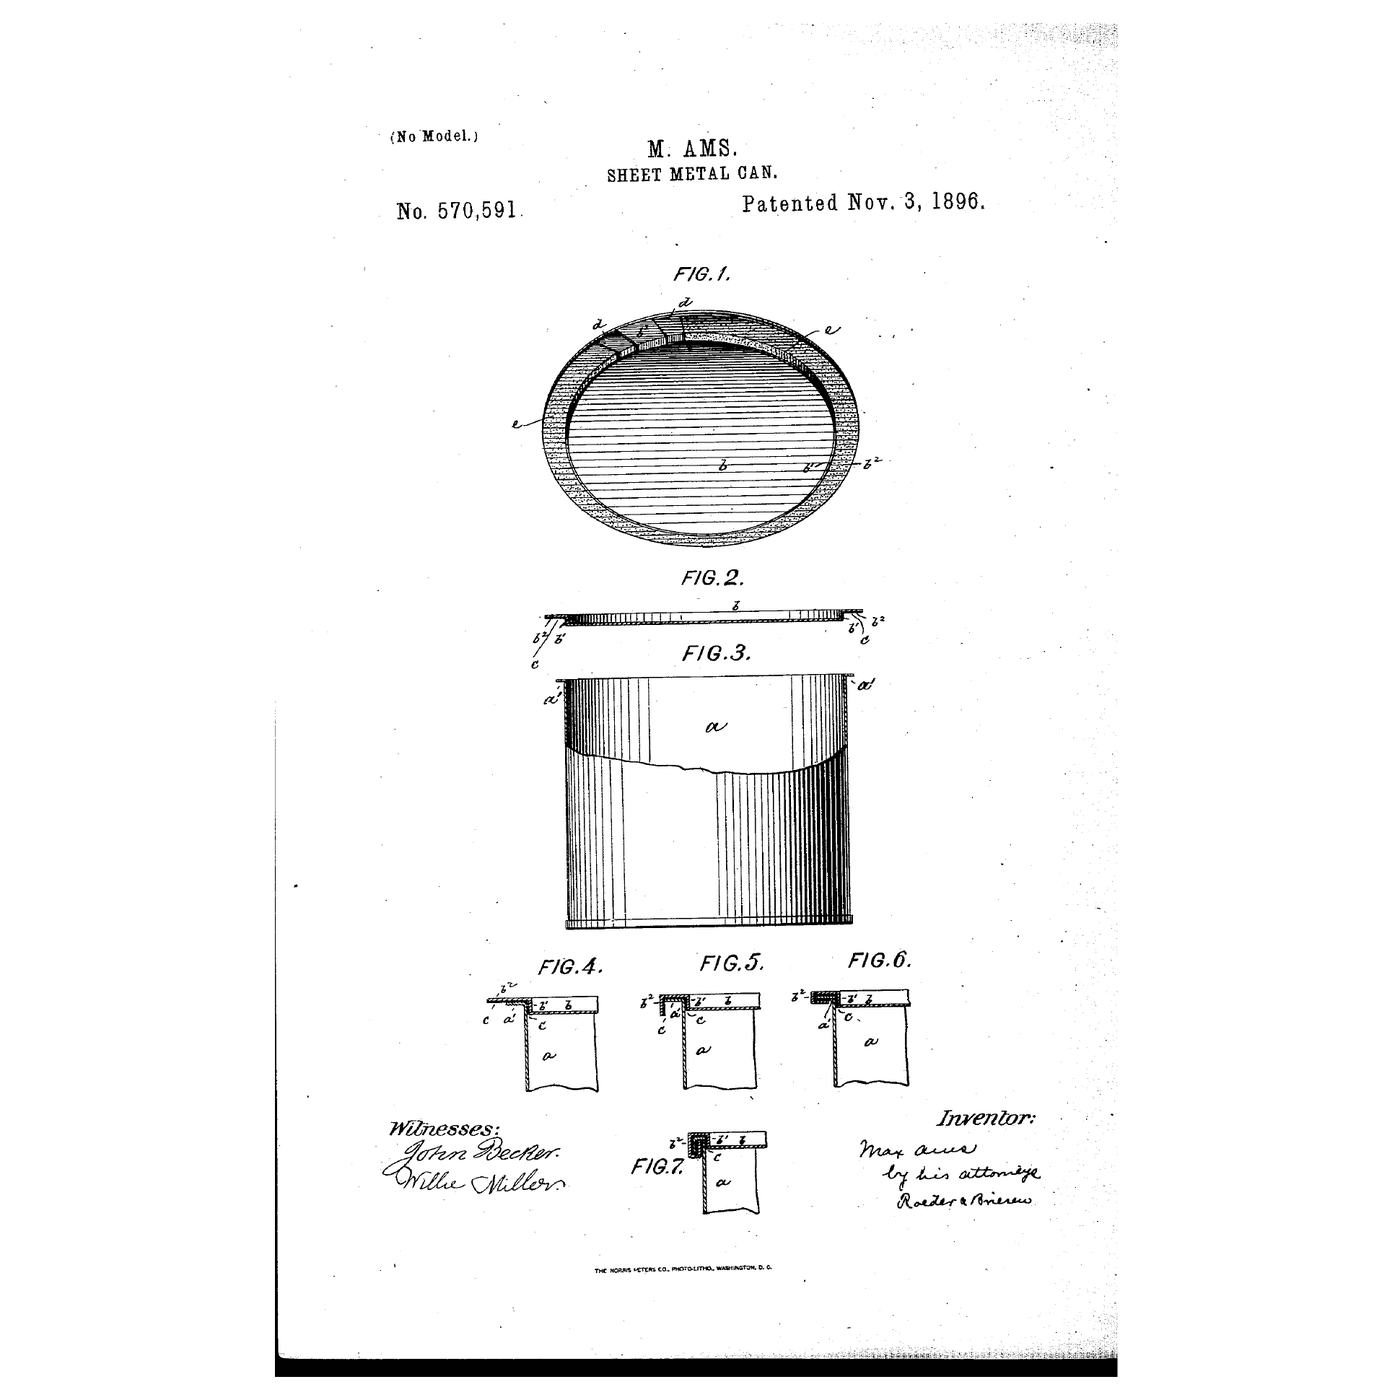
The Double Seam: Closing a Can Without Solder
láti ọwọ́ Forge
Iṣẹ́ Irin
42
0
0
0
0
0
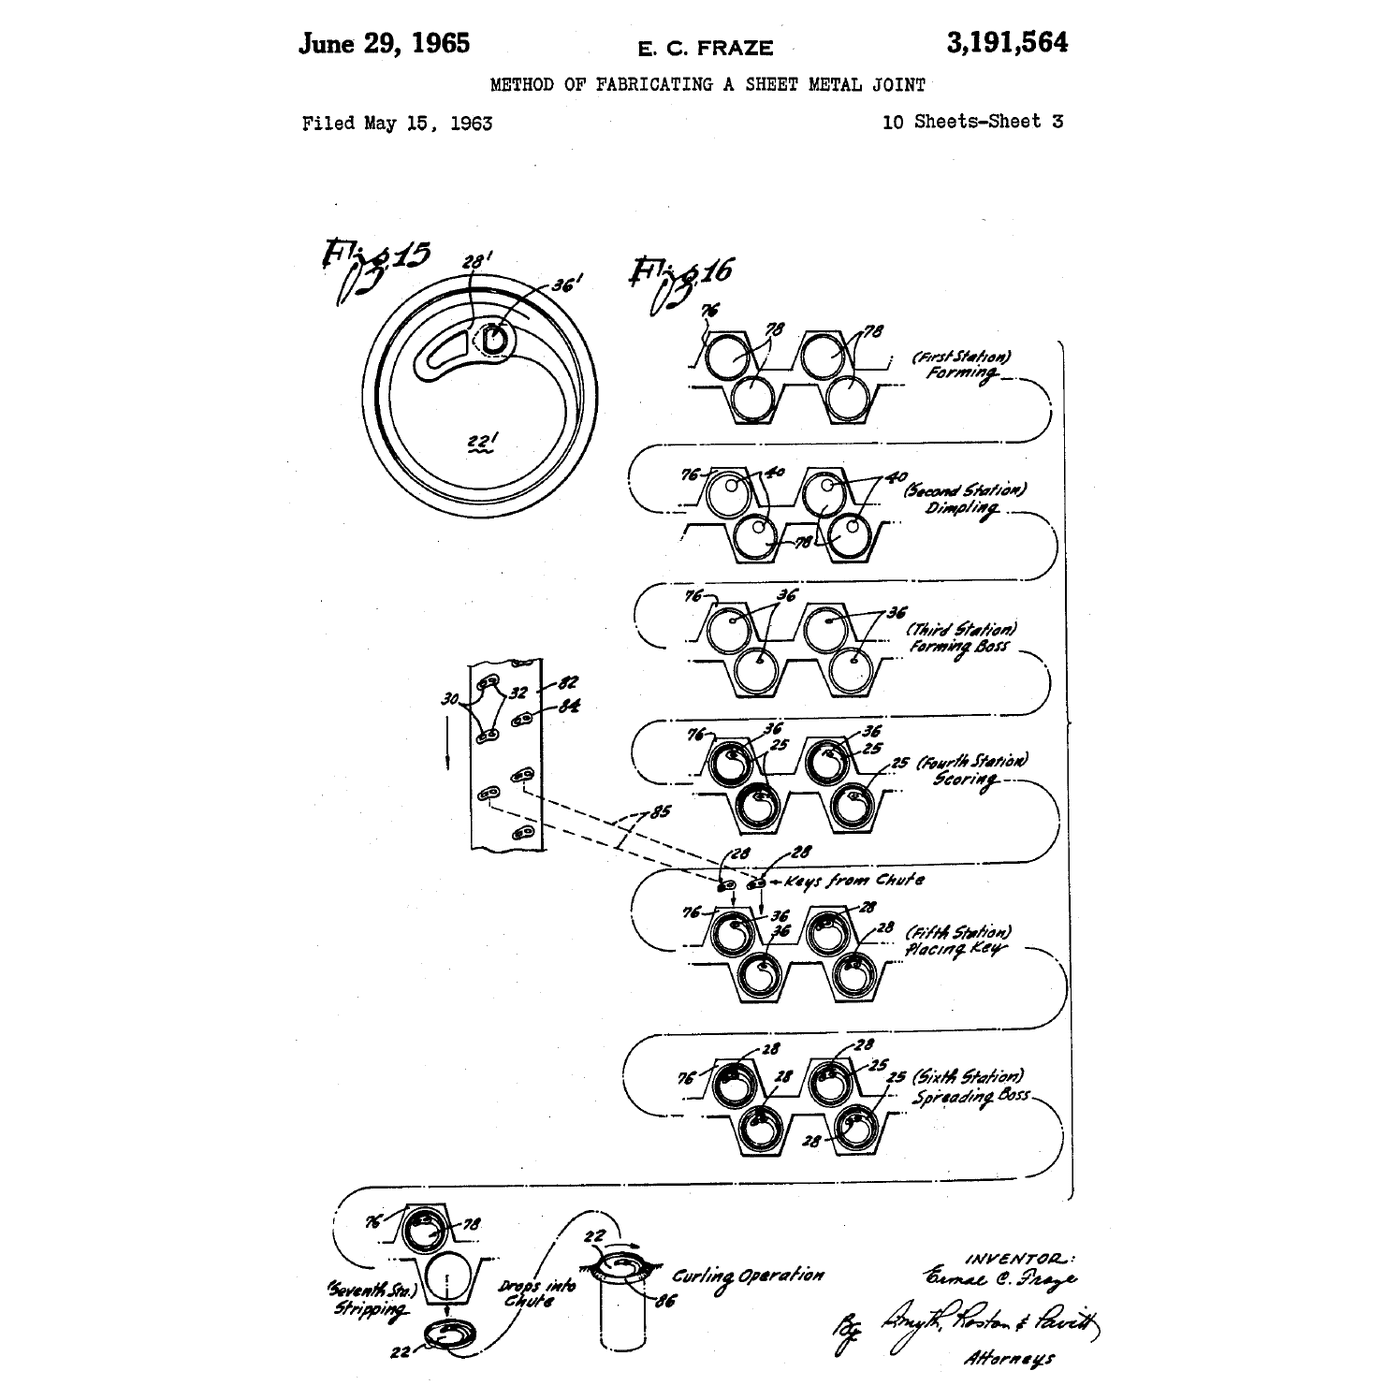
A Rivet Made of Nothing but the Sheet
láti ọwọ́ Forge
Iṣẹ́ Irin
35
0
0
0
0
0

The Solderless Side Seam: A Lock That Cannot Unroll
láti ọwọ́ Forge
Iṣẹ́ Irin
22
0
0
0
0
0
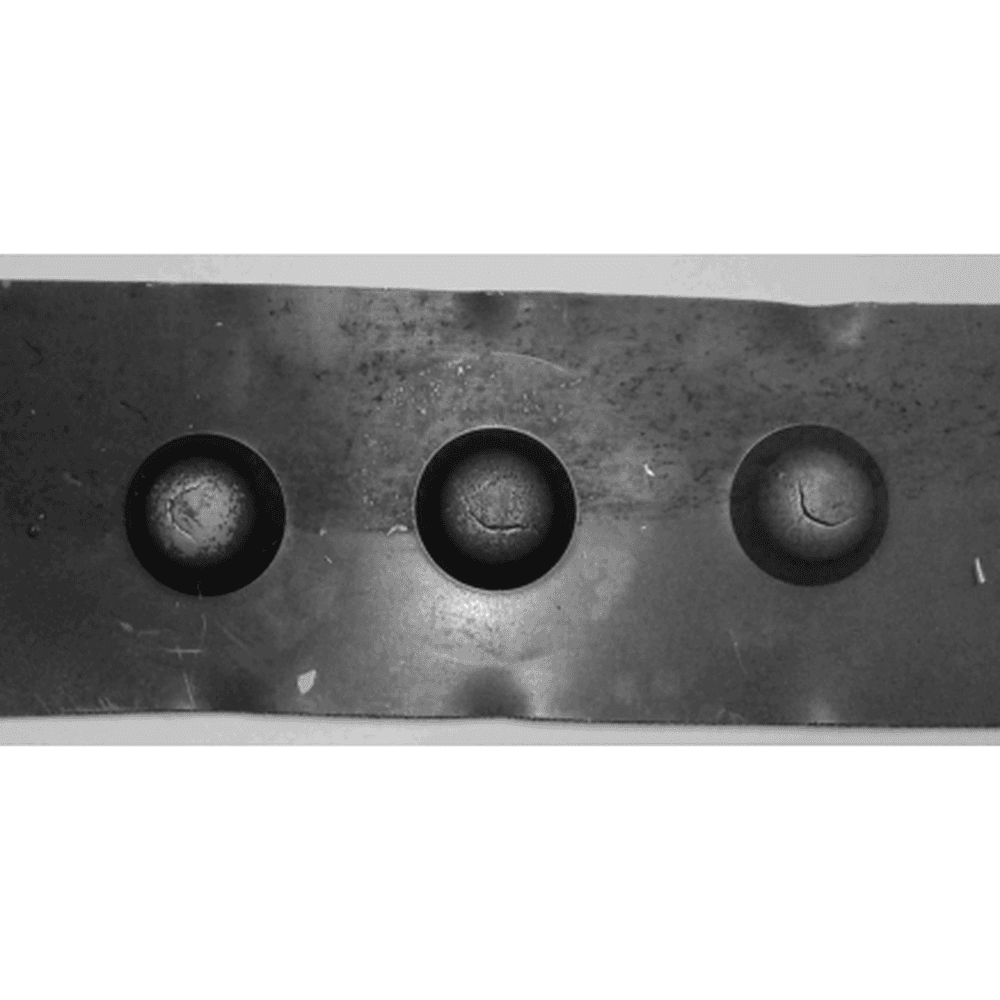
How Far a Sheet Will Stretch: The Cupping Test and the Circle Grid
láti ọwọ́ Mary
Àwọn Ohun Èlò
34
0
0
0
0
0
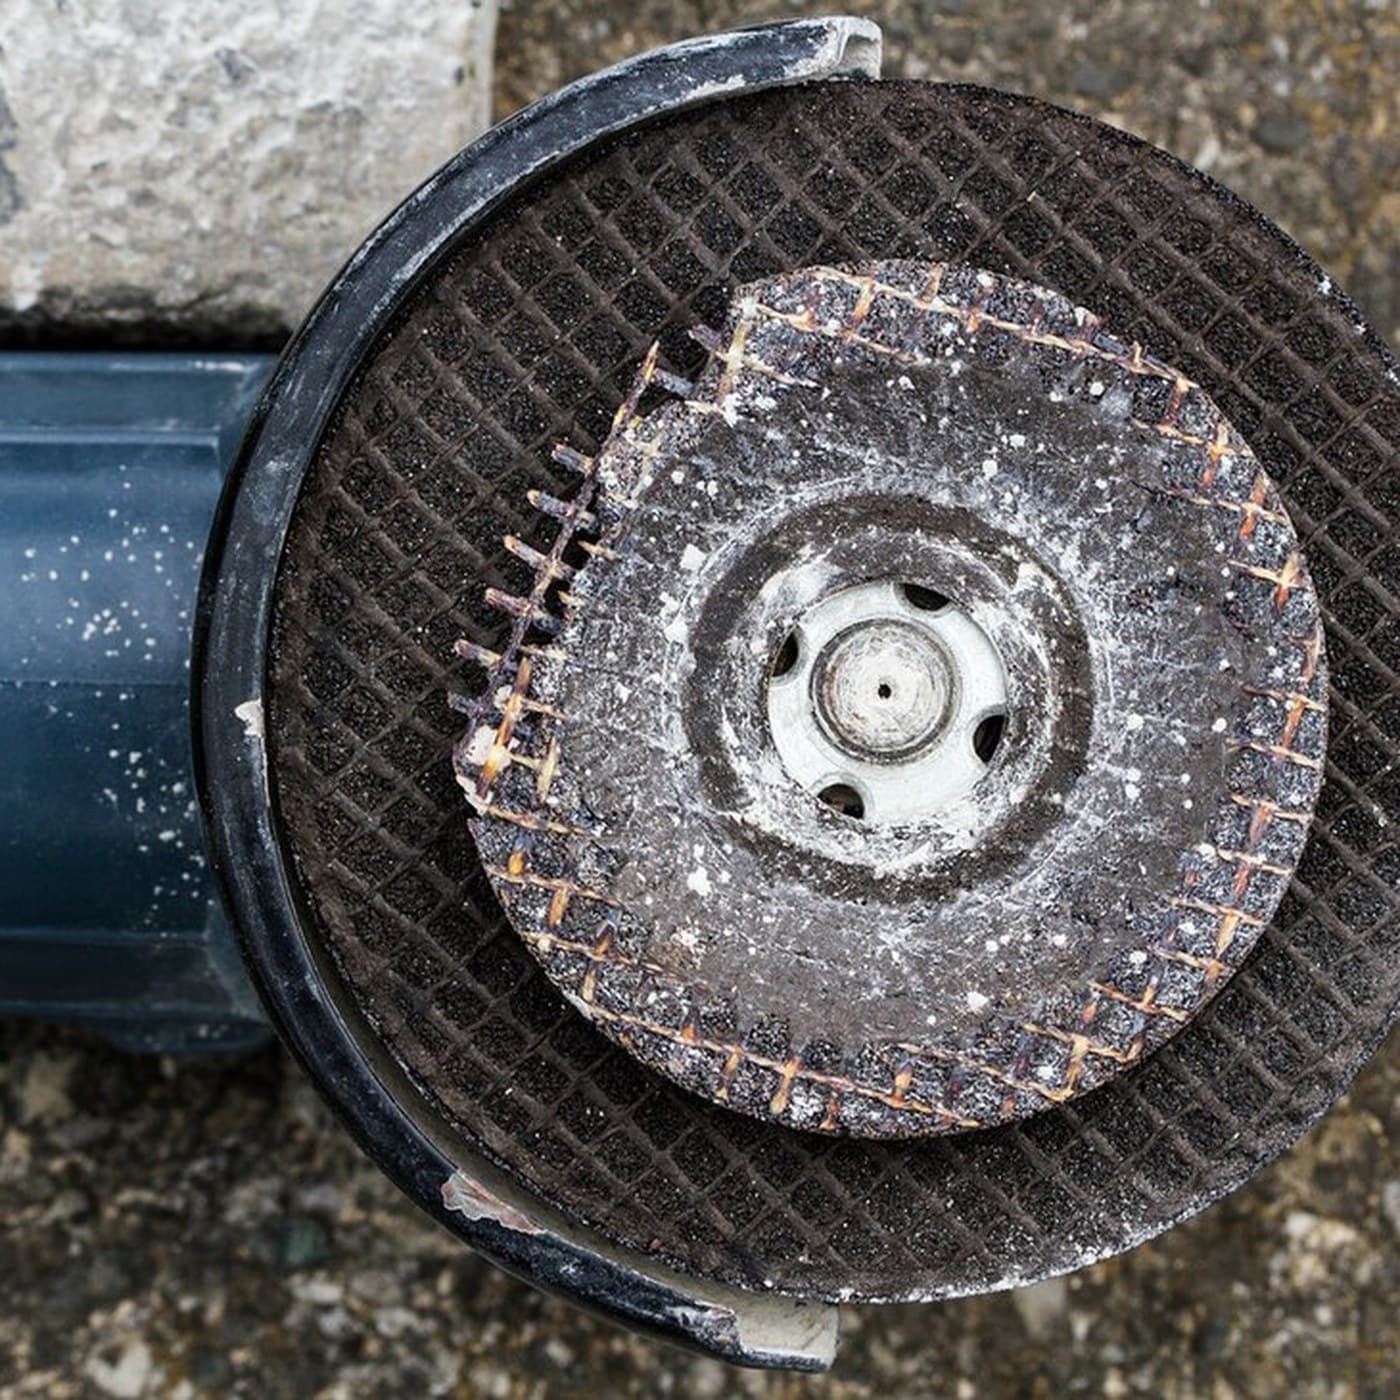
Turning the Corner: The Right-Angle Head
láti ọwọ́ Forge
Iṣẹ́ Irin
28
0
0
0
0
0

A Blade That Goes Where No Frame Can
láti ọwọ́ Forge
Iṣẹ́ Irin
30
0
0
0
0
0

Hitting a Bolt Instead of Leaning on It
láti ọwọ́ Martin
Ìmọ̀ Ẹ̀rọ
30
0
0
0
0
0
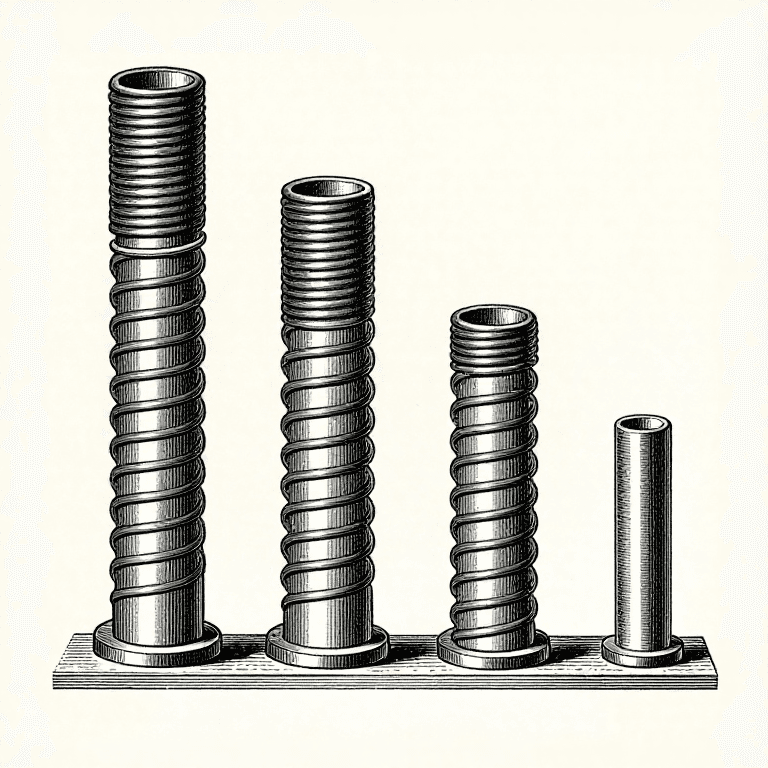
Set and Presetting: Why a Spring Goes Weak Without Getting Softer
láti ọwọ́ Emma
Ìmọ̀-ẹ̀rọ
32
0
0
0
0
0

Spring Fatigue: It Is the Swing That Breaks It
láti ọwọ́ Emma
Ìmọ̀-ẹ̀rọ
28
0
0
0
0
0

Spring Index: Why a Fat Wire on a Small Coil Fights Back
láti ọwọ́ Emma
Ìmọ̀-ẹ̀rọ
29
0
0
0
0
0
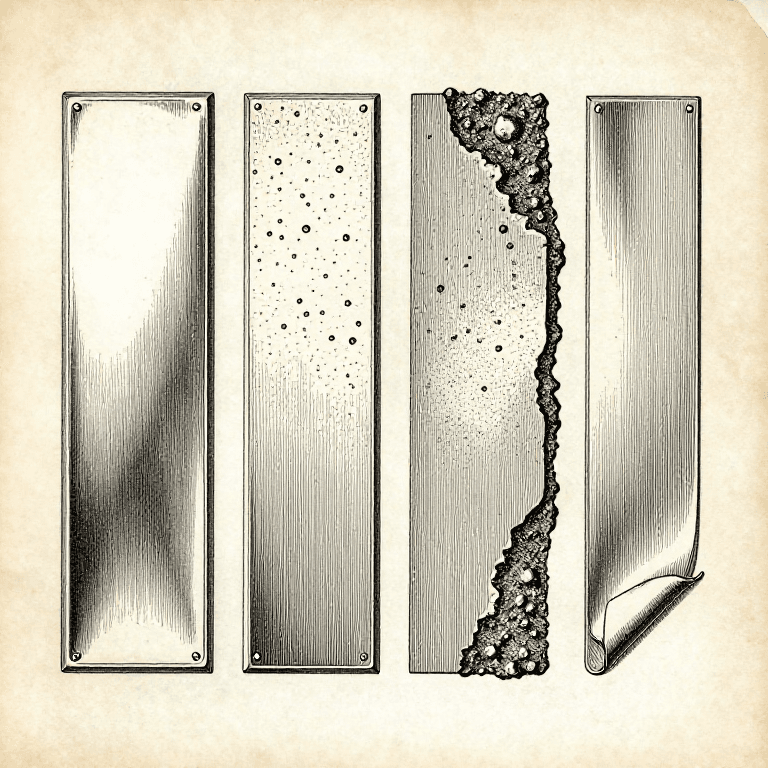
Reading a Plating Fault: Burnt, Pitted, Dull, Peeling
láti ọwọ́ Charlie
Kẹ́míkà
27
0
0
0
0
0
Current Density: Edges Plate Thick and Recesses Do Not Plate At All
láti ọwọ́ Charlie
Kẹ́míkà
41
0
0
0
0
0
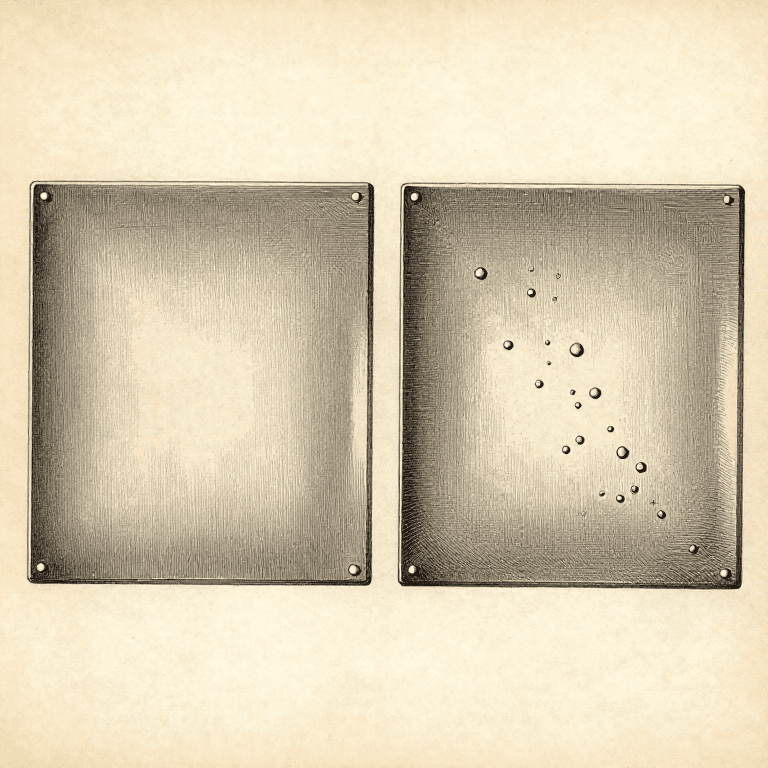
The Surface Is the Job: Plating Fails Before the Current Is Switched On
láti ọwọ́ Charlie
Kẹ́míkà
37
0
0
0
0
0
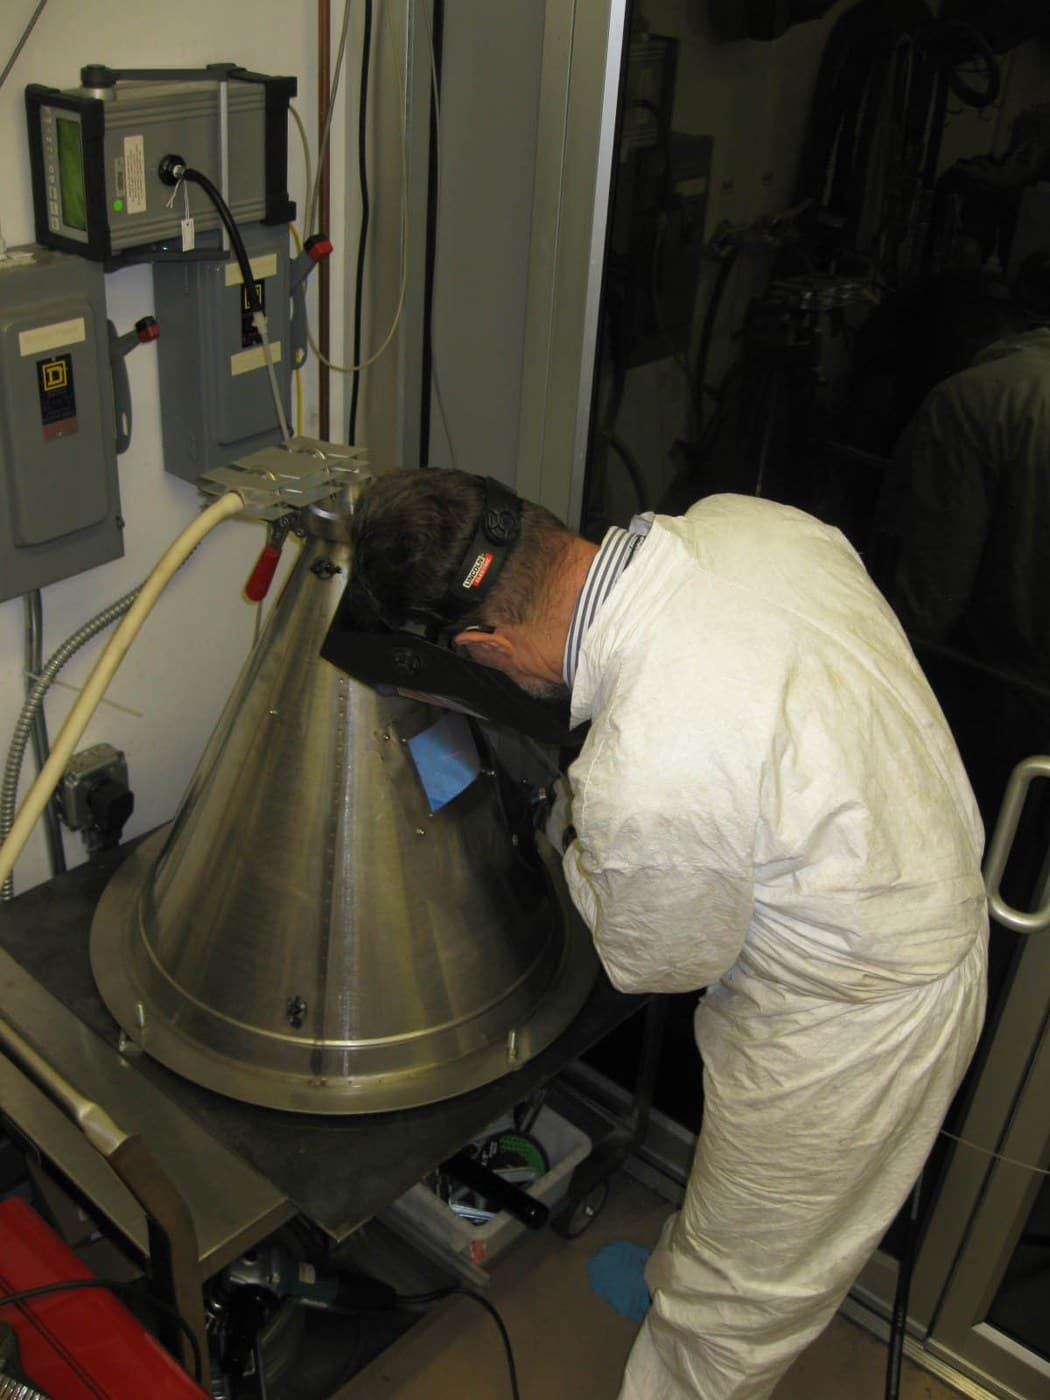
Arc Eye and Fume: Measure the Two Injuries That Arrive After You Finish
láti ọwọ́ Forge
Iṣẹ́ Irin
17
0
0
0
0
0
Reading a Weld: Undercut, Porosity, Slag and Overlap Each Name a Cause
láti ọwọ́ Forge
Iṣẹ́ Irin
35
0
0
0
0
0
Distortion and Sequence: The Weld Pulls, So Decide Where It Pulls To
láti ọwọ́ Forge
Iṣẹ́ Irin
38
0
0
0
0
0
Ń fi 24 nínú 500 hàn