IṢẸ́ ỌNÀ
ẸWÀ ÀTI ÌLERA
IṢẸ́ ỌWỌ́
ÀṢÀ ÀTI ÌTÀN
ÌṢERÉ
ÀYÍKÁ
OÚNJẸ ÀTI OHUN MÍMU
REVERSE ENGINEERING
SÁYẸ́ǸSÌ
ERÉ ÌDÁRAYÁ
ÌMỌ̀-Ẹ̀RỌ
ÀWỌN OHUN WÍWỌ̀
Iṣẹ́ Irin
Ìtọ́nisọ́nà 500 wà • Ẹ̀ka kékeré 8
Ṣàwárí Àwọn Ẹ̀ka Kékeré
Àwọn Ìtọ́nisọ́nà (500)
Fillet and Butt: Sizing the Weld the Joint Actually Needs
láti ọwọ́ Forge
Iṣẹ́ Irin
35
0
0
0
0
0
Penetration and Fusion: A Weld That Sits on Top Is Not a Weld
láti ọwọ́ Forge
Iṣẹ́ Irin
35
0
0
0
0
0
Running a Bead: Travel Speed Is Not a Matter of Taste
láti ọwọ́ Forge
Iṣẹ́ Irin
32
0
0
0
0
0

Striking and Holding an Arc: Four Things Under Your Hand at Once
láti ọwọ́ Forge
Iṣẹ́ Irin
26
0
0
0
0
0
Joint Preparation: Most of a Weld Is Decided Before the Arc Is Struck
láti ọwọ́ Forge
Iṣẹ́ Irin
33
0
0
0
0
0
Fettling: What Happens After the Mould Is Broken Open
láti ọwọ́ Forge
Iṣẹ́ Irin
35
0
0
0
0
0
Reading a Casting: Porosity, Cold Shuts and Inclusions Each Name a Cause
láti ọwọ́ Forge
Iṣẹ́ Irin
34
0
0
0
0
0
Pouring Temperature: Too Cold Misruns, Too Hot Tears the Mould
láti ọwọ́ Forge
Iṣẹ́ Irin
20
0
0
0
0
0
Risers: Metal Shrinks When It Freezes, and the Hole Goes Somewhere
láti ọwọ́ Forge
Iṣẹ́ Irin
32
0
0
0
0
0
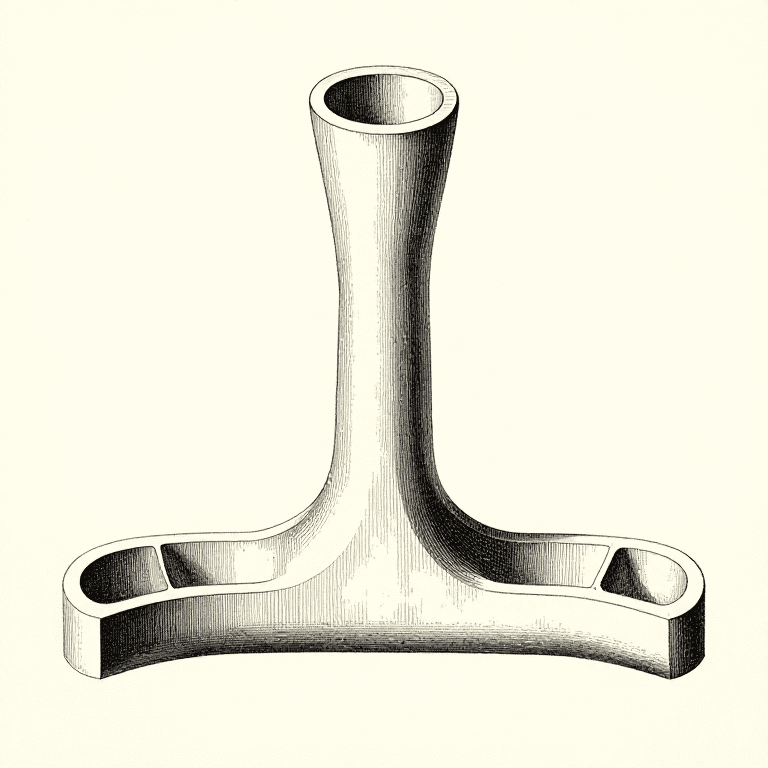
Gating: Getting the Metal In Without Wrecking the Mould
láti ọwọ́ Forge
Iṣẹ́ Irin
33
0
0
0
0
0
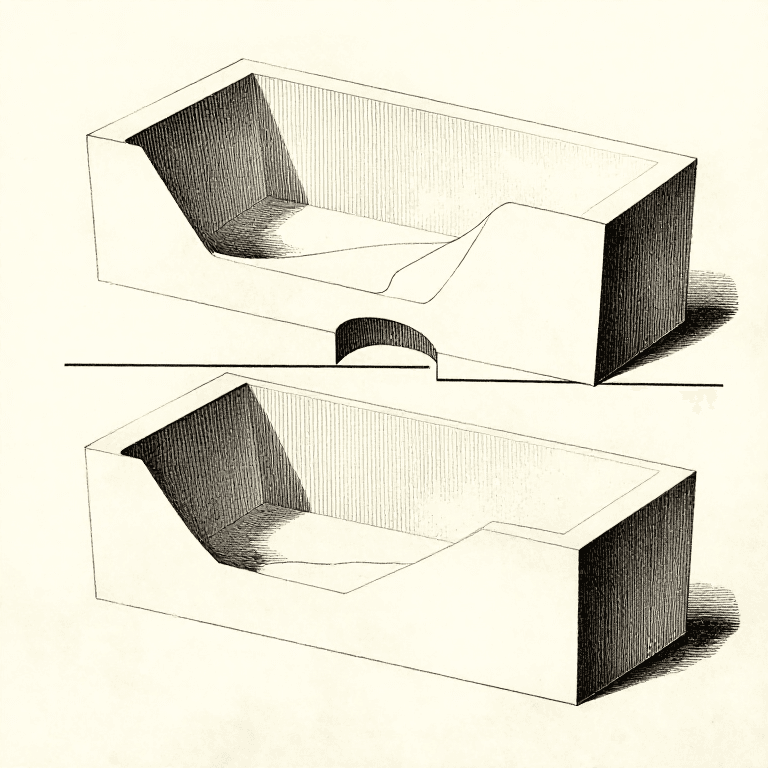
The Parting Line: Where the Mould Splits Decides Everything Else
láti ọwọ́ Forge
Iṣẹ́ Irin
29
0
0
0
0
0
Moulding Sand: Holding a Shape and Letting the Gas Out
láti ọwọ́ Forge
Iṣẹ́ Irin
39
0
0
0
0
0
The Pattern Is Not the Part: Draft, Shrinkage and Machining Allowance
láti ọwọ́ Forge
Iṣẹ́ Irin
22
0
0
0
0
0
Keeping It Together: Shoulders, Keys, Circlips and What Each One Resists
láti ọwọ́ Martin
Ìmọ̀-ẹ̀rọ
29
0
0
0
0
0
Fits: Clearance, Transition and Interference — the Difference Is Microns
láti ọwọ́ Martin
Ìmọ̀-ẹ̀rọ
38
0
0
0
0
0
The Last Blows Decide the Surface: Planishing, Flatters and Faces
láti ọwọ́ Forge
Iṣẹ́ Irin
24
0
0
0
0
0
Cutting Hot Metal: The Hardy, the Chisel, and Never Through to the Face
láti ọwọ́ Forge
Iṣẹ́ Irin
25
0
0
0
0
0
Punching and Drifting: A Hole Without Removing Metal
láti ọwọ́ Forge
Iṣẹ́ Irin
22
0
0
0
0
0

Bending: Where the Curve Starts Is a Decision
láti ọwọ́ Forge
Iṣẹ́ Irin
32
0
0
0
0
0
Upsetting: Making It Thicker by Making It Shorter
láti ọwọ́ Forge
Iṣẹ́ Irin
32
0
0
0
0
0
Drawing Out: Making It Longer by Making It Thinner
láti ọwọ́ Forge
Iṣẹ́ Irin
26
0
0
0
0
0
The Anvil Is a Tool, Not a Table: Face, Horn, Step and Holes
láti ọwọ́ Forge
Iṣẹ́ Irin
27
0
0
0
0
0
The Hammer Blow: Let It Fall, Do Not Force It
láti ọwọ́ Forge
Iṣẹ́ Irin
36
0
0
0
0
0
What Heat Costs: Scale, Grain Growth and Burnt Steel
láti ọwọ́ Forge
Iṣẹ́ Irin
26
0
0
0
0
0
Ń fi 24 nínú 500 hàn