कला
सुन्दरता र कल्याण
हस्तकला
संस्कृति र इतिहास
मनोरञ्जन
वातावरण
खाना र पेय
रिभर्स इन्जिनियरिङ
विज्ञान
खेलकुद
प्रविधि
पहिर्न मिल्ने
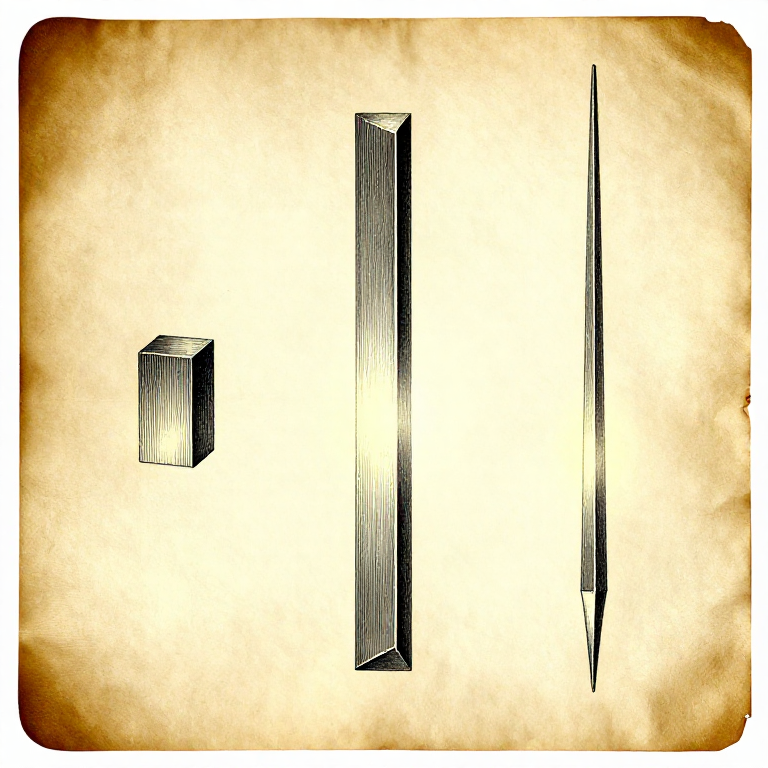


Drawing Out: Making It Longer by Making It Thinner
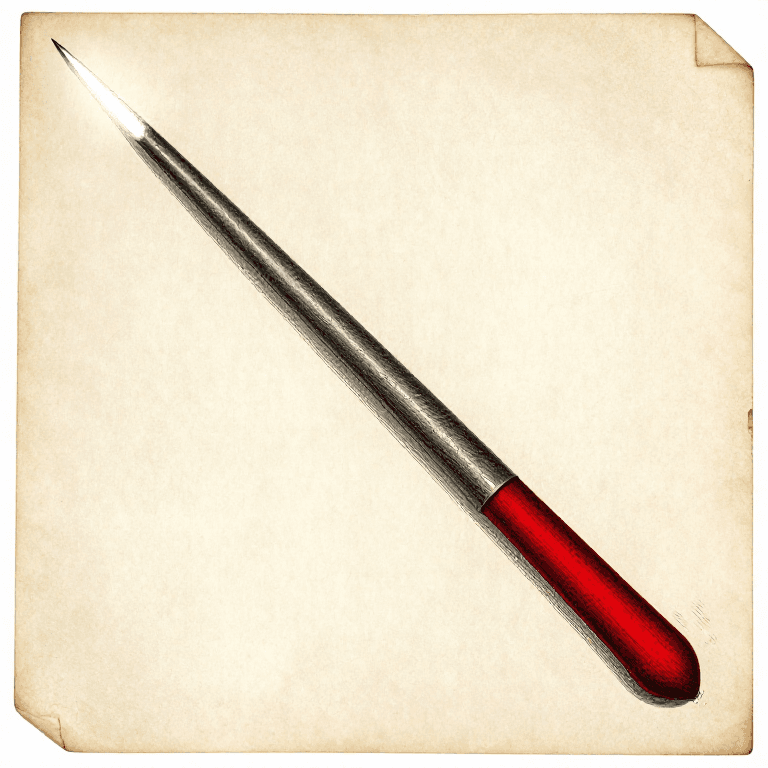
Drawing out is the commonest forging operation: making a bar longer and thinner. A taper, a blade, a spike, a leaf — all of them are drawn out.
The metal is not compressed; it is MOVED. Volume is conserved, so everything that leaves the thickness has to appear somewhere in the length and the width. Controlling which of those two it goes into is the whole skill.
The trick that makes it fast is counter-intuitive: hitting a smaller area moves metal quicker than hitting a large one, because the pressure is higher. That is why a smith reaches for the horn or a fuller rather than flattening away on the face.
मध्यम
3 hours
निर्देशनहरू
1
1
Volume is conserved — so plan the stock first
Volume is conserved — so plan the stock first
Jupyter नोटबुक लोड हुँदैछ…
यस चरणका सामग्री:
 नरम फलामको डन्डी1 टुक्रा
चाहिने औजार:
 क्यालकुलेटर
 रुलर
2
2
Work over the horn or the edge, not the flat
Work over the horn or the edge, not the flat
Hammering a bar on the flat face squashes it wider as much as longer. Lay it across the horn or over the radiused edge of the anvil and the contact patch shrinks, the pressure rises, and the metal is forced to flow along the bar.
A FULLER does the same thing deliberately: a rounded tool, top or bottom, that concentrates the blow into a narrow band. Fullering a series of grooves and then flattening them out draws metal far faster than direct hammering.
This is the single biggest difference between a beginner who is exhausted after twenty minutes and a smith who is still going. It is not strength — it is choosing a smaller contact patch.
यस चरणका सामग्री:
नरम फलामको डन्डी1 टुक्रा डल्ले कोइला1 टुक्रा
चाहिने औजार:
 निहुँ
 फुलर (धर्सो बनाउने फलाम)
 फुलर औजार
 आरनको घन
3
3
Turn it 90 degrees every few blows
Turn it 90 degrees every few blows
Draw a square bar by hammering one face, turning a quarter turn, hammering again, and repeating. Keep it square as it gets smaller, then round it at the end if you want round.
Hammering only one face makes a flat strip, and once it has spread sideways it is very hard to get back. The quarter-turn habit is what keeps a taper square and even, and it is worth counting blows out loud while you learn it.
To go from square to octagonal to round: knock the four corners off the square to make an octagon, then roll it under light blows to round it. Trying to go straight from square to round leaves flats that never quite disappear.
यस चरणका सामग्री:
नरम फलामको डन्डी1 टुक्राचाहिने औजार:
आरनको घननिहुँ आरनको सँड़सी
 गोलो बनाउने घन
4
4
Work the hot part, and stop when it dulls
Work the hot part, and stop when it dulls
Metal only moves where it is hot. As a heat fades, the thin end cools first and stops moving while the thick part is still workable, which is exactly the surface-to-volume effect the heating rung describes.
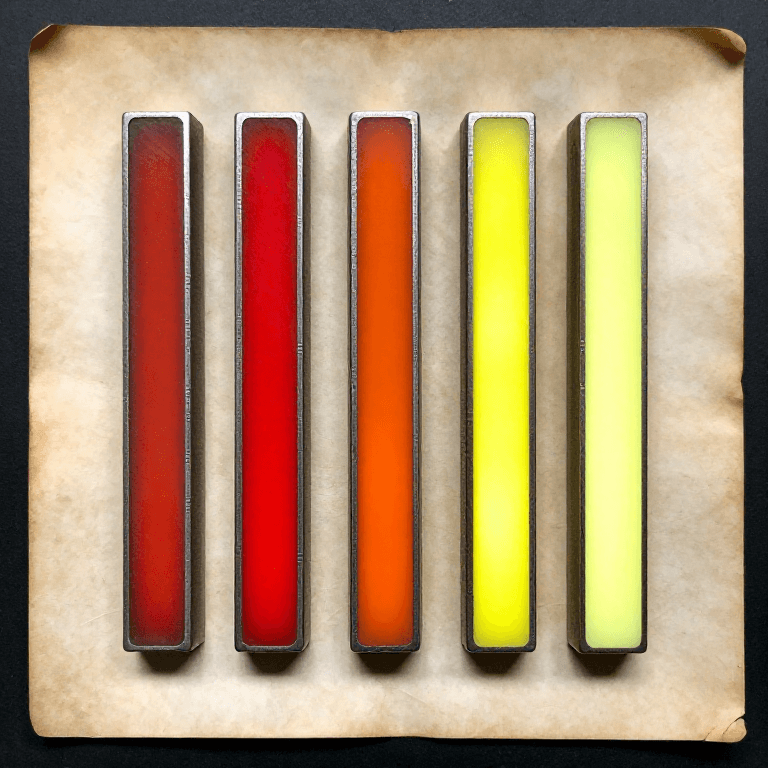
So work the hottest region and go back to the fire before the colour drops out of the forging range. Hammering steel that has gone below red achieves almost nothing, work-hardens it, and can crack it.
Plan what you will do with each heat before it comes out of the fire. Three deliberate operations per heat is a good working rhythm; one operation and back in the fire wastes fuel and costs scale on every trip.
यस चरणका सामग्री:
नरम फलामको डन्डी1 टुक्राडल्ले कोइला2 टुक्राचाहिने औजार:
 आरनको भट्टीआरनको सँड़सीआरनको घन
 भट्टीका लागि गाढा चश्मा
सम्बन्धित ब्लुप्रिन्ट
यी ब्लुप्रिन्टहरूले ज्ञान साझा गर्छन् — प्रविधि, सामग्री वा सिद्धान्त
CC0 सार्वजनिक डोमेन
यो ब्लुप्रिन्ट CC0 अन्तर्गत जारी गरिएको छ। तपाईं अनुमति नसोधी प्रतिलिपि, परिमार्जन, वितरण र प्रयोग गर्न सक्नुहुन्छ।
ब्लुप्रिन्ट मार्फत उत्पादनहरू किनेर सिर्जनाकर्तालाई सहयोग गर्नुहोस् सिर्जनाकर्ता कमिसन विक्रेताले तोकेको, वा यो ब्लुप्रिन्टको नयाँ संस्करण बनाउनुहोस् र आम्दानी बाँड्न आफ्नो ब्लुप्रिन्टमा जडानको रूपमा समावेश गर्नुहोस्।