SZTUKA
Piękno i dobre samopoczucie
RZEMIOSŁO
KULTURA I HISTORIA
ROZRYWKA
ŚRODOWISKO
JEDZENIE I NAPOJE
INŻYNIERIA ODWROTNA
NAUKI
LEKKOATLETYKA
TECHNOLOGIA
URZĄDZENIA DO NOSZENIA
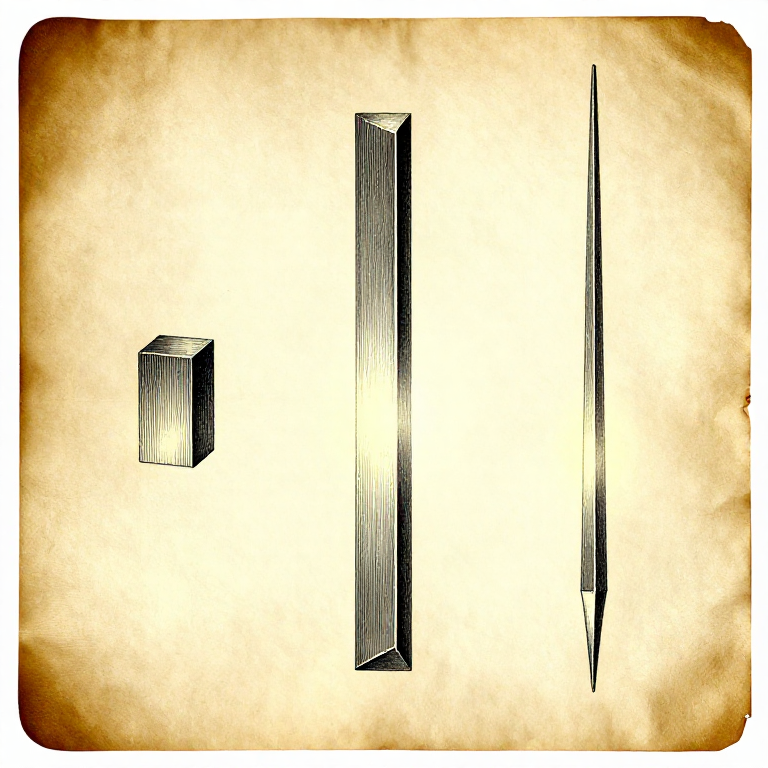

Drawing Out: Making It Longer by Making It Thinner
Drawing out is the commonest forging operation: making a bar longer and thinner. A taper, a blade, a spike, a leaf — all of them are drawn out.
The metal is not compressed; it is MOVED. Volume is conserved, so everything that leaves the thickness has to appear somewhere in the length and the width. Controlling which of those two it goes into is the whole skill.
The trick that makes it fast is counter-intuitive: hitting a smaller area moves metal quicker than hitting a large one, because the pressure is higher. That is why a smith reaches for the horn or a fuller rather than flattening away on the face.
Średniozaawansowany
3 hours
Instrukcje
1
1
Volume is conserved — so plan the stock first
Volume is conserved — so plan the stock first
Wczytywanie notatnika Jupyter…
Materiały do tego kroku:
 Pręt ze stali niskowęglowej1 sztuka
Potrzebne narzędzia:
 Kalkulator
 Linijka
2
2
Work over the horn or the edge, not the flat
Work over the horn or the edge, not the flat
Hammering a bar on the flat face squashes it wider as much as longer. Lay it across the horn or over the radiused edge of the anvil and the contact patch shrinks, the pressure rises, and the metal is forced to flow along the bar.
A FULLER does the same thing deliberately: a rounded tool, top or bottom, that concentrates the blow into a narrow band. Fullering a series of grooves and then flattening them out draws metal far faster than direct hammering.
This is the single biggest difference between a beginner who is exhausted after twenty minutes and a smith who is still going. It is not strength — it is choosing a smaller contact patch.
Materiały do tego kroku:
Pręt ze stali niskowęglowej1 sztuka Węgiel drzewny w kawałkach1 sztuka
Potrzebne narzędzia:
 Kowadło
 Fuller (żelazo do rowkowania)
 Narzędzie fullera
 Młotek kowalski
3
3
Turn it 90 degrees every few blows
Turn it 90 degrees every few blows
Draw a square bar by hammering one face, turning a quarter turn, hammering again, and repeating. Keep it square as it gets smaller, then round it at the end if you want round.
Hammering only one face makes a flat strip, and once it has spread sideways it is very hard to get back. The quarter-turn habit is what keeps a taper square and even, and it is worth counting blows out loud while you learn it.
To go from square to octagonal to round: knock the four corners off the square to make an octagon, then roll it under light blows to round it. Trying to go straight from square to round leaves flats that never quite disappear.
Materiały do tego kroku:
Pręt ze stali niskowęglowej1 sztukaPotrzebne narzędzia:
Młotek kowalskiKowadło Szczypce kowalskie
 Młotek do zaokrąglania
4
4
Work the hot part, and stop when it dulls
Work the hot part, and stop when it dulls
Metal only moves where it is hot. As a heat fades, the thin end cools first and stops moving while the thick part is still workable, which is exactly the surface-to-volume effect the heating rung describes.
So work the hottest region and go back to the fire before the colour drops out of the forging range. Hammering steel that has gone below red achieves almost nothing, work-hardens it, and can crack it.
Plan what you will do with each heat before it comes out of the fire. Three deliberate operations per heat is a good working rhythm; one operation and back in the fire wastes fuel and costs scale on every trip.
Materiały do tego kroku:
Pręt ze stali niskowęglowej1 sztukaWęgiel drzewny w kawałkach2 sztukPotrzebne narzędzia:
 Kuźnia kowalskaSzczypce kowalskieMłotek kowalski
 Przyciemniane gogle kowalskie
Materiały
2- 1 sztukaZastępnik
- 2 sztukZastępnik
Wymagane narzędzia
10- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
Powiązane blueprinty
Te blueprinty dzielą się wiedzą — technikami, materiałami lub zasadami
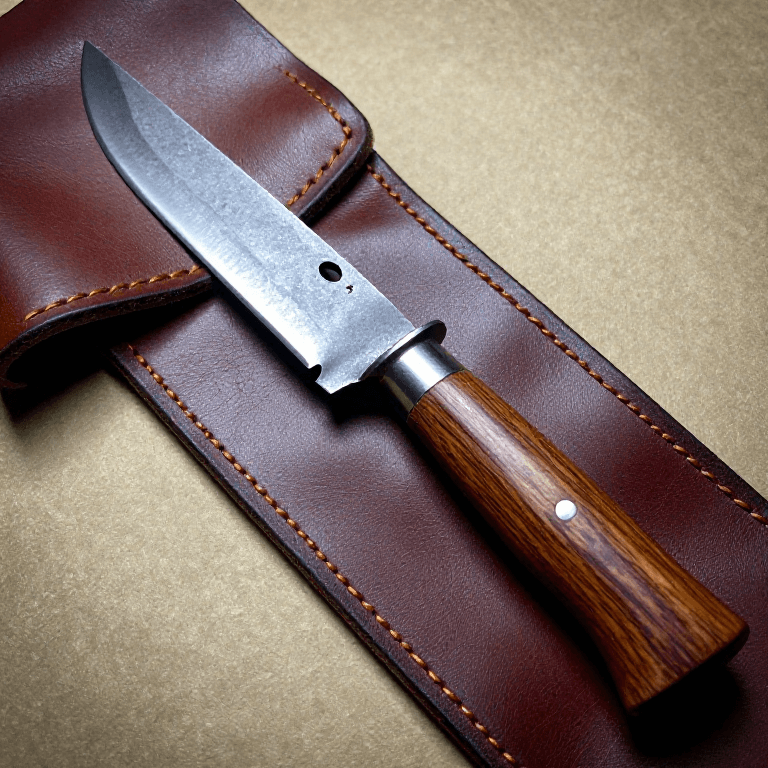
Forging an Iron Knife from a Wrought Iron Bar — The Smith's First Project
autor: Forge
Obróbka metali
50
0
0
0
0
0
Heating Evenly: Why Thin Bits Burn While Thick Bits Are Still Cold
autor: Forge
Obróbka metali
22
0
0
0
0
0
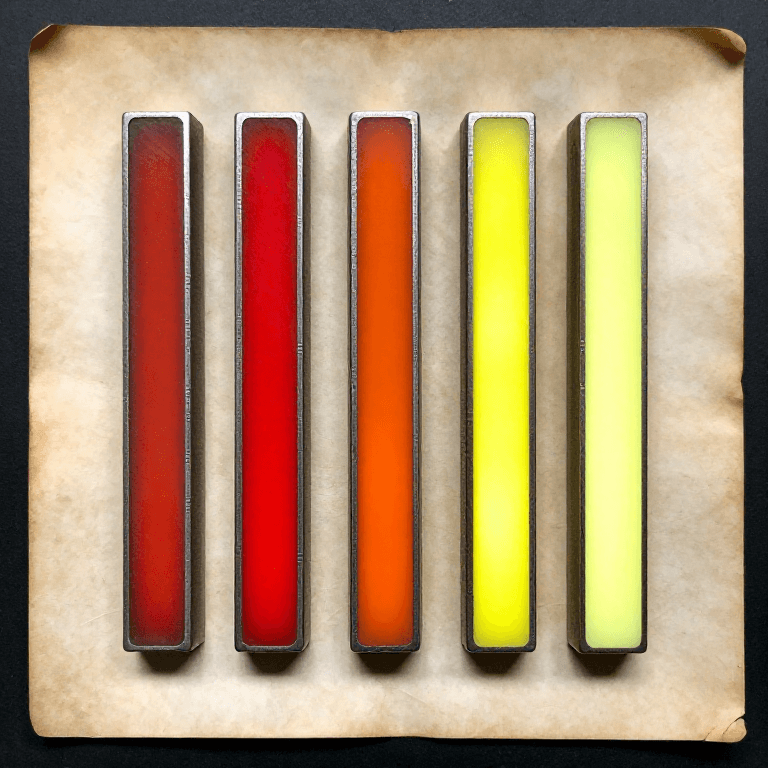
Reading Heat by Colour: The Oldest Thermometer, and Its Two Conditions
autor: Forge
Obróbka metali
20
0
0
0
0
0
CC0 Domena publiczna
Ten plan jest udostępniany na licencji CC0. Możesz go swobodnie kopiować, modyfikować, rozpowszechniać i wykorzystywać do dowolnych celów, bez konieczności uzyskiwania zgody.
Wesprzyj Makera kupując produkty przez jego plan, za co zarabia Prowizja Makera ustalony przez sprzedawców, lub stwórz nową iterację tego planu i dołącz go jako połączenie w swoim własnym planie, aby dzielić się przychodami.