UBUHANZI
UBWIZA N'UBUZIMA
UBUKORIKORI
UMUCO N'AMATEKA
IMYIDAGADURO
IBIDUKIKIJE
IBIRIBWA N'IBINYOBWA
UBWUBATSI BUSUBIRA INYUMA
UBUMENYI
SIPORO
IKORANABUHANGA
IBYAMBARWA
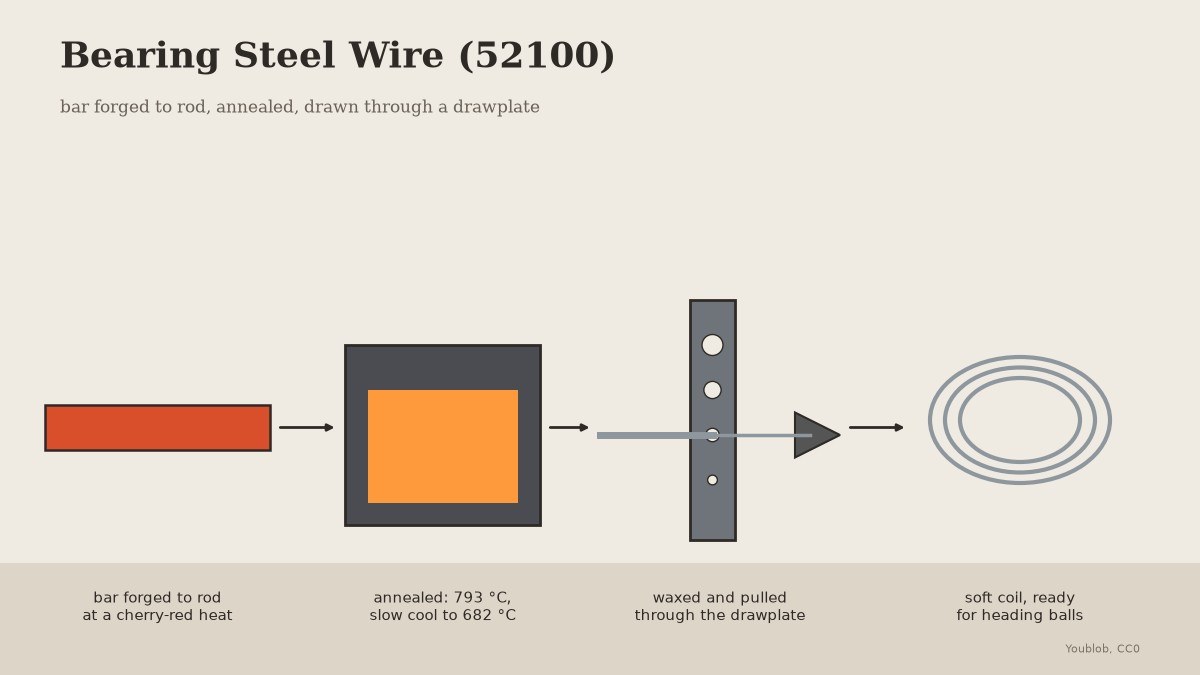


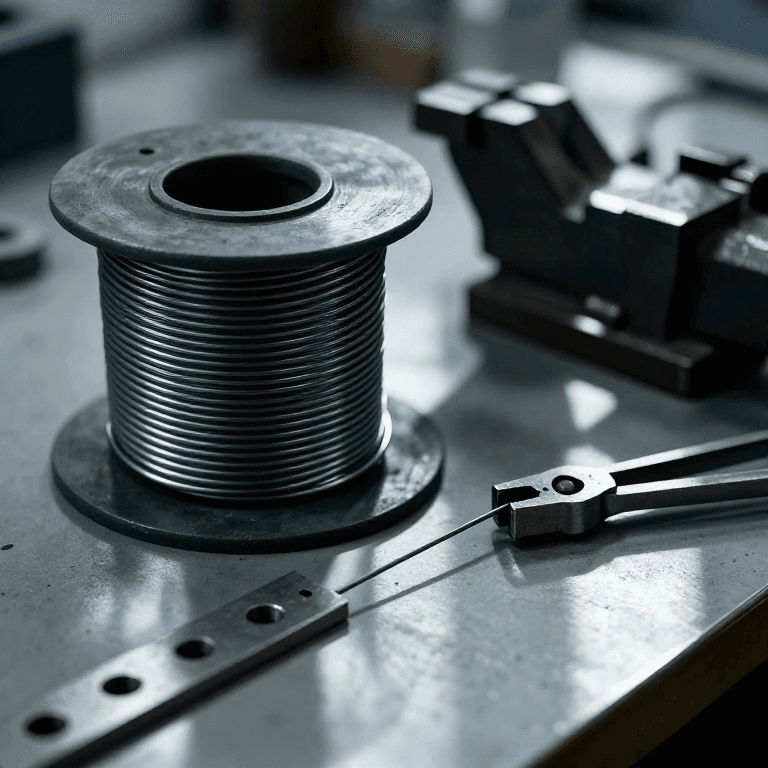
Bearing Steel Wire (52100): Drawn from Bar Through a Drawplate
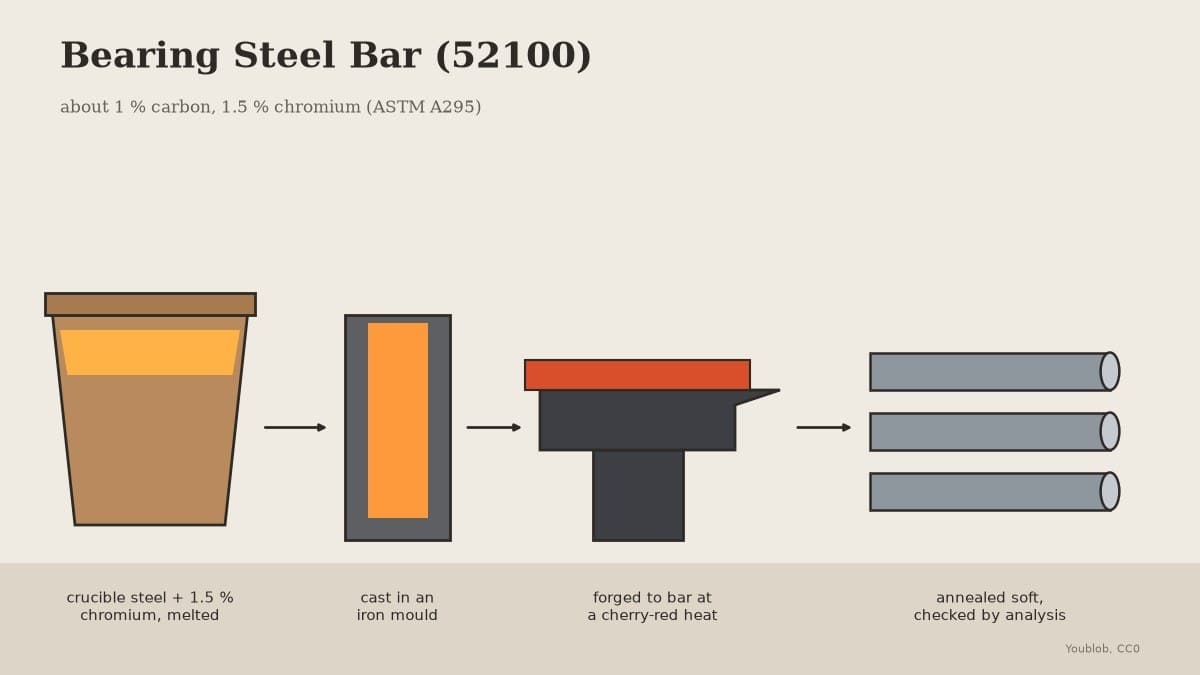
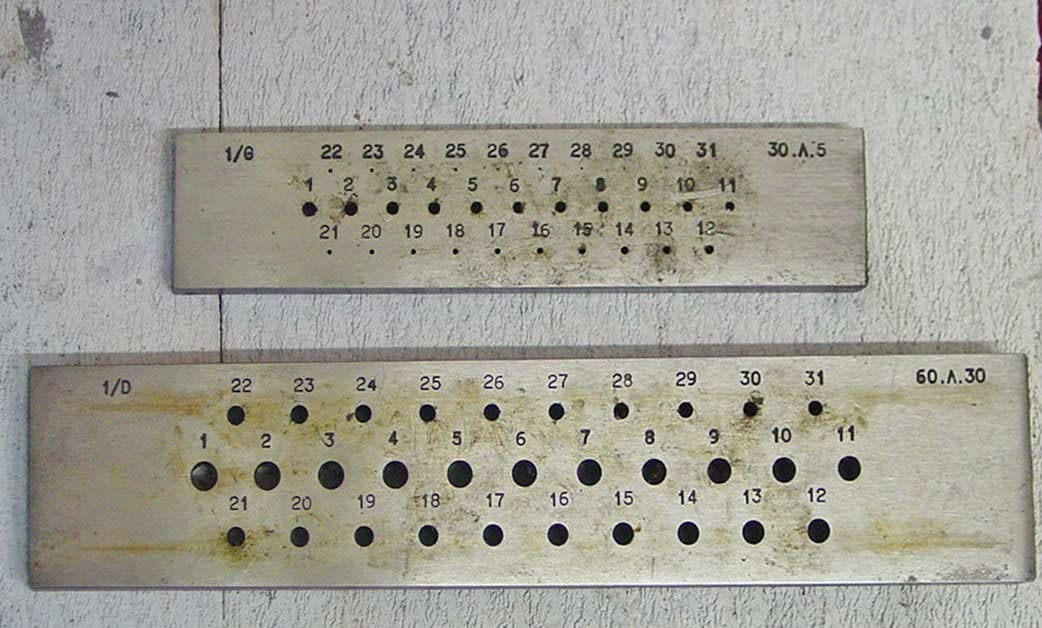
Bearing balls are headed from thick wire of 52100 steel. Here 52100 bar is forged to rod and drawn through a drawplate. At 1 % carbon it is much harder than mild steel, so it is annealed soft before drawing and again after every two holes, using the 52100 anneal Verhoeven recommends.
The picture: our drawing, bar to coil.
Hejuru
2 days
Amabwiriza
1
1
Forge to rod
Forge to rod
Heat the bar to a cherry-red heat and no hotter, and draw it out round on the anvil to a rod a little thicker than the drawplate's largest hole.
Ibikoresho by'iyi ntambwe:
 Umuhini w'icyuma cya roulement (52100)1 kg
 Amakara1 as required
Ibikoresho bikenewe:
 Uruganda rw'umucuzi
 Ingoyi
 Inyundo ifite umutwe utambitse
 Amafashi y'umucuzi
 Uturindantoki two gukomeza ibyuma
 Amadarubindi y'umutekano
2
2
Anneal
Anneal
In the oven, hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
Ibikoresho bikenewe:
 Itanura ryo gutunganya hakoreshejwe ubushyuhe
 Termokupuli ifite igaragazaAmafashi y'umucuziUturindantoki two gukomeza ibyuma
3
3
Clean and taper
Clean and taper
Brush off all the scale, then file a long taper on the first 3 cm so it passes the first hole.
Ibikoresho bikenewe:
 Ibikoresho by'uburoso bw'insinga
 Amakariso Menshi
 Ifatiro ry'Ameza
4
4
Wax and draw
Wax and draw
Clamp the drawplate in the vise. Wax the rod, push the taper through the first hole it does not slip through, and pull straight out with the draw tongs in one steady pull.
Ibikoresho by'iyi ntambwe:
 Igishashara20 g
Ibikoresho bikenewe:
 Urubaho rwo gukurura insinga rw'icyuma
 Koleyo yo gukurura insingaIfatiro ry'Ameza
 Uturindantoki tw'uruhu tw'akazi
5
5
Anneal every two holes
Anneal every two holes
Draw through each next hole without skipping. After every two holes, coil the wire and anneal it again: hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
Ibikoresho by'iyi ntambwe:
Igishashara1 igiceIbikoresho bikenewe:
Urubaho rwo gukurura insinga rw'icyumaKoleyo yo gukurura insingaItanura ryo gutunganya hakoreshejwe ubushyuheTermokupuli ifite igaragaza6
6
Finish soft
Finish soft
Stop at the diameter your balls need, checked with the caliper, and give the coil a last anneal so it is soft for heading.
Ibikoresho bikenewe:
 Ikigereranyo cya Digitale cy'Amasentimetero 6Itanura ryo gutunganya hakoreshejwe ubushyuheTermokupuli ifite igaragaza
7
7
Troubleshooting
Troubleshooting
Bearing steel wire troubleshooting.
Flow
Loading...
Ibikoresho
3- Umwanya
- 1 as requiredUmwanya
- 1 igiceUmwanya
Ibikoresho bikenewe
15- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
Iki gishushanyo gikora
Blueprint zijyanye
Izi blueprint zisangira ubumenyi — uburyo, ibikoresho cyangwa amahame
CC0 Umurenge rusange
Iyi blueprint yasohowe munsi ya CC0. Ushobora gukoporora, guhindura, gukwirakwiza no gukoresha nta kwemererwa.
Shyigikira Umuremyi ugura ibicuruzwa binyuze muri Blueprint ye Komisiyo y'Umuremyi byashyizweho n'Abacuruzi, cyangwa kora verisiyo nshya y'iyi Blueprint ukayinjiza nk'isano muri Blueprint yawe kugira ngo musangire inyungu.